corrosion resistant magnetic pump
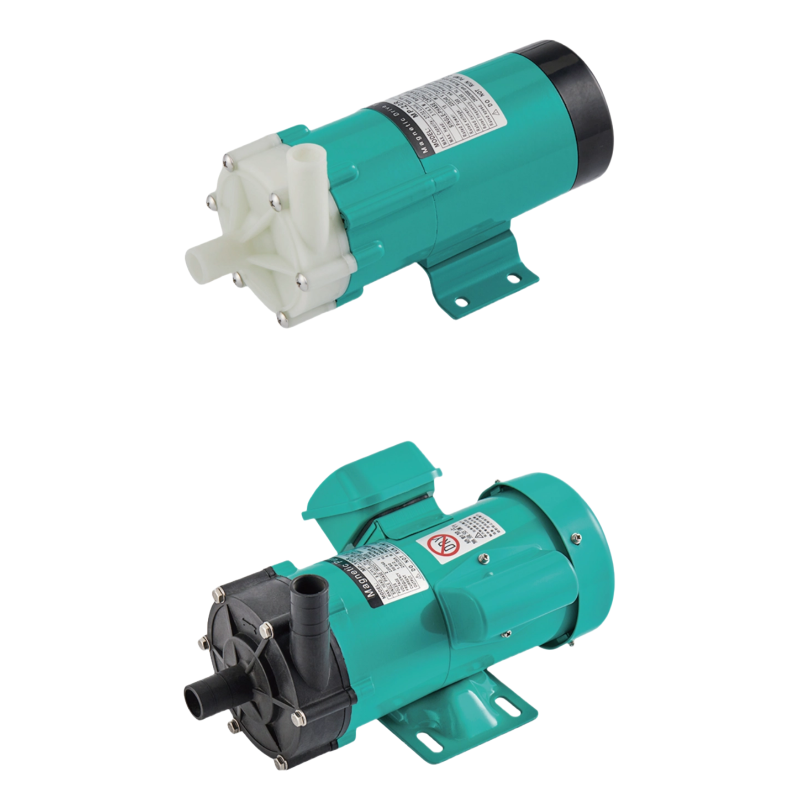
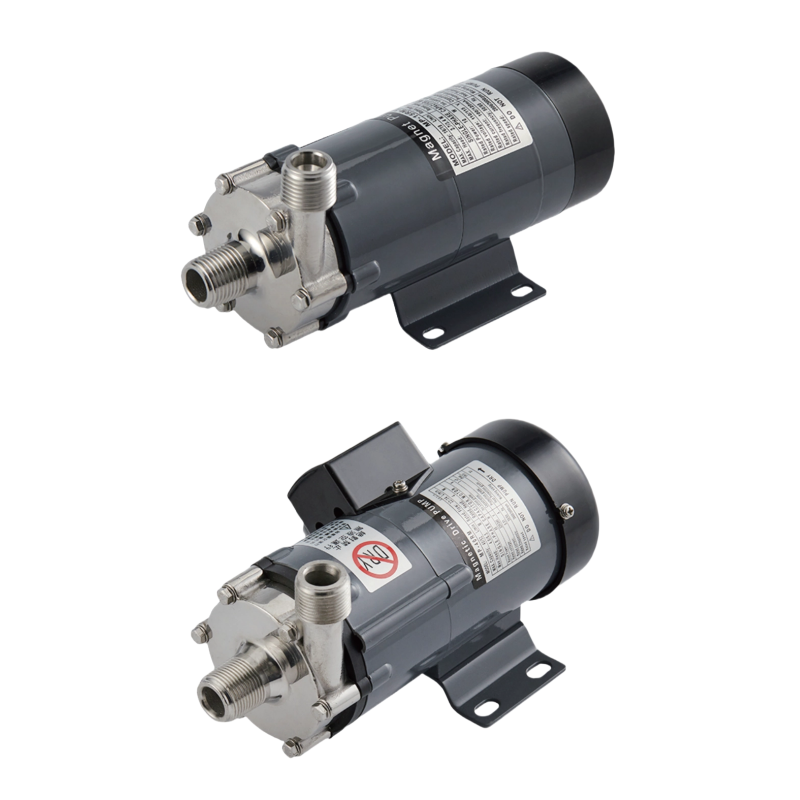
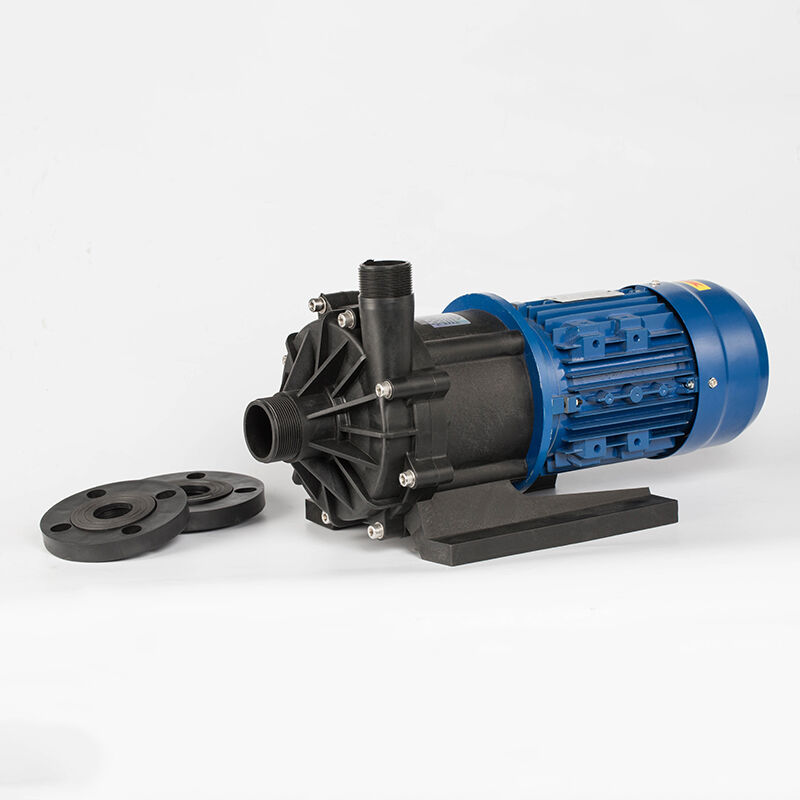
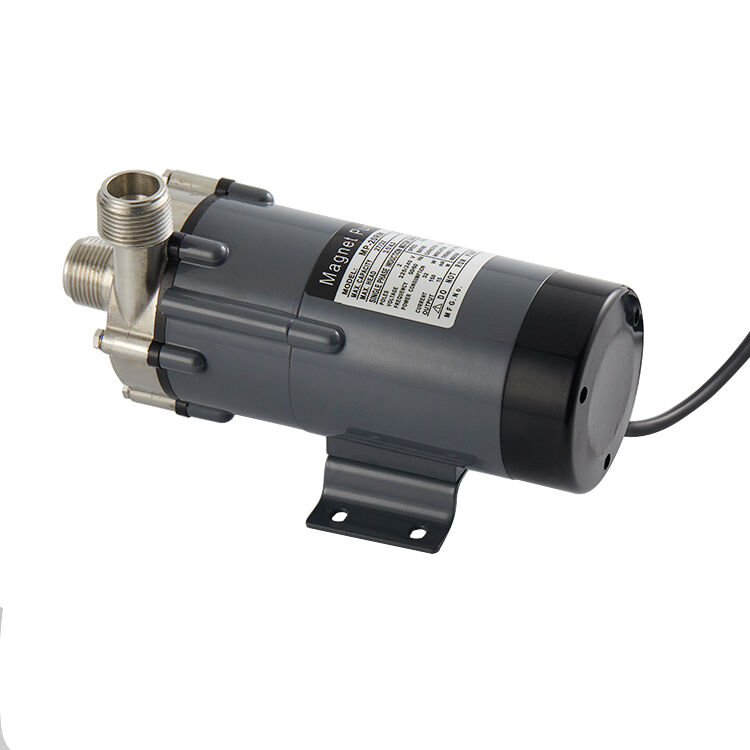
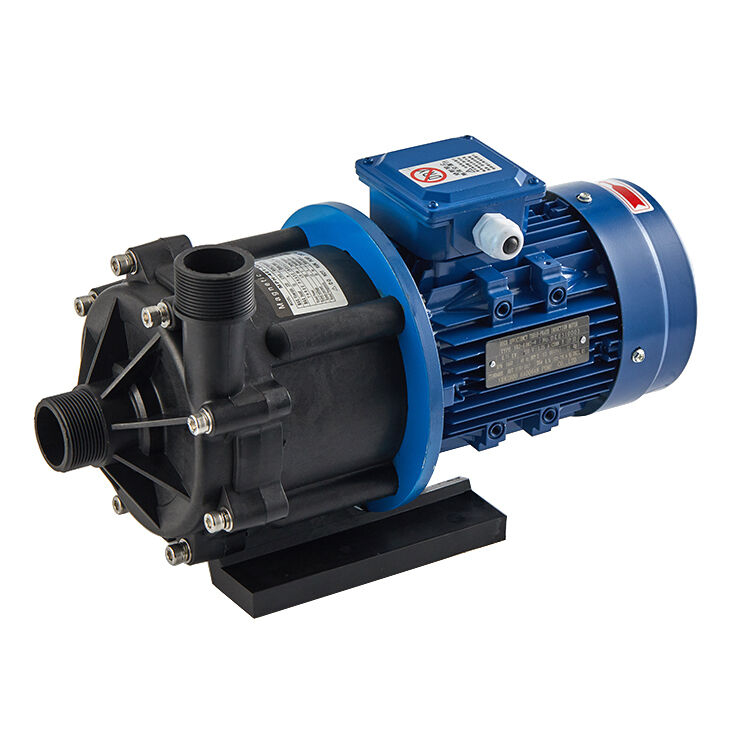
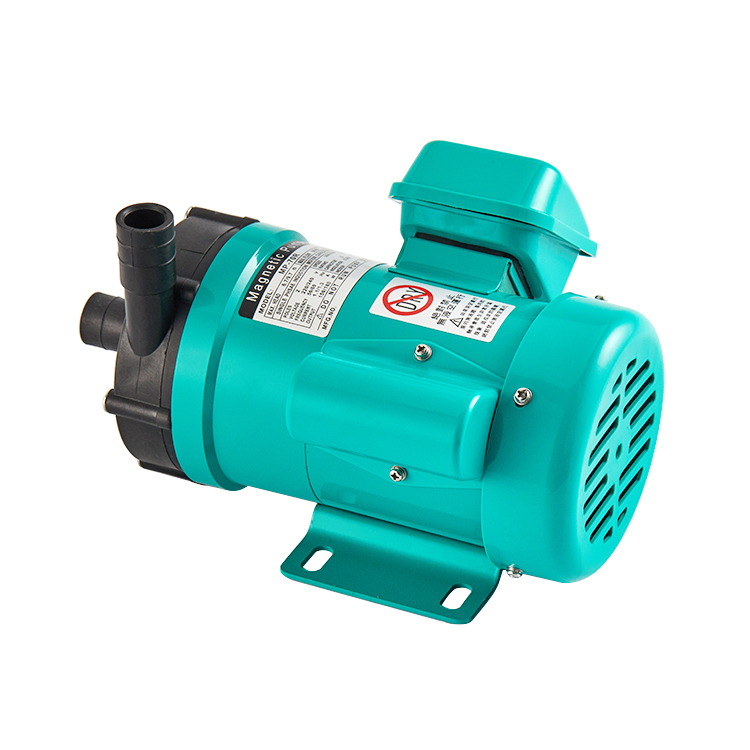
A corrosion resistant magnetic pump represents a revolutionary advancement in fluid transfer technology, designed specifically for applications involving aggressive chemical environments and demanding industrial operations. This specialized pump combines magnetic drive technology with corrosion-resistant materials to eliminate seal leakage while protecting equipment from degradation.
The corrosion resistant magnetic pump functions by using magnetic coupling to transfer rotational force without physical contact between the motor and pump shaft. This innovative design completely eliminates traditional mechanical seals, which are common failure points in standard pumps. The pump housing and wetted components are manufactured from superior materials such as stainless steel, polypropylene, or specialized alloys that withstand exposure to corrosive chemicals, acids, bases, and other aggressive substances.
Key technological features of the corrosion resistant magnetic pump include its hermetically sealed design, which prevents chemical leakage into the environment or workplace. The magnetic impeller operates within a completely enclosed cavity, ensuring zero emissions during operation. Advanced bearing systems utilize the pumped fluid for lubrication, enhancing reliability in chemical transfer applications.
Applications for the corrosion resistant magnetic pump span across multiple industries. Chemical manufacturing facilities rely on these pumps for transferring caustic solutions, sulfuric acid, and other hazardous chemicals. Pharmaceutical production uses them for precise fluid handling without contamination. Water treatment plants employ corrosion resistant magnetic pump systems for handling aggressive treatment chemicals. Semiconductor manufacturing, battery production, and electroplating operations all benefit from this technology's superior protection against corrosive environments.

 EN