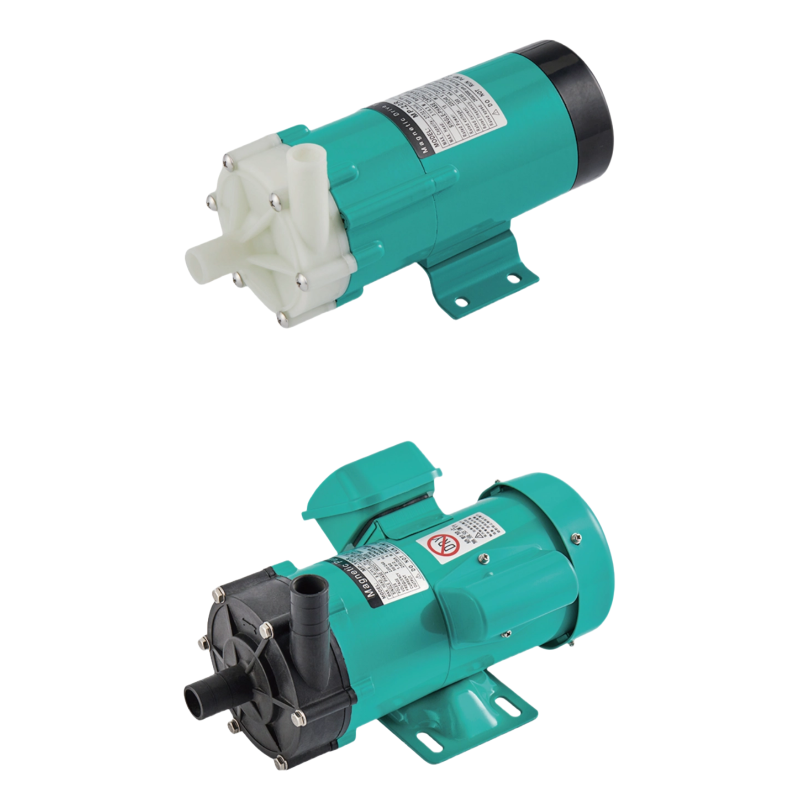
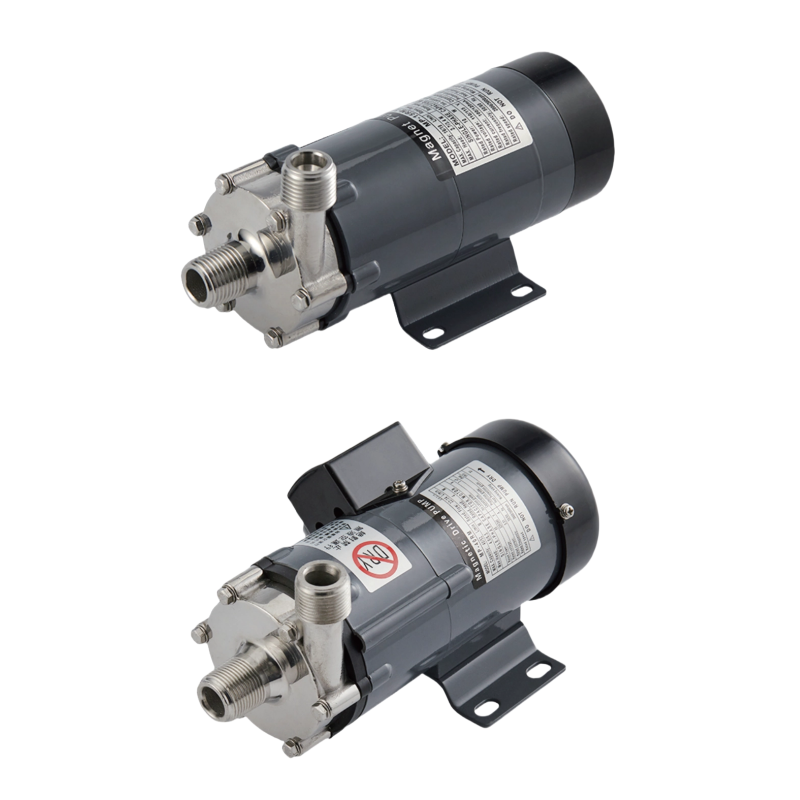
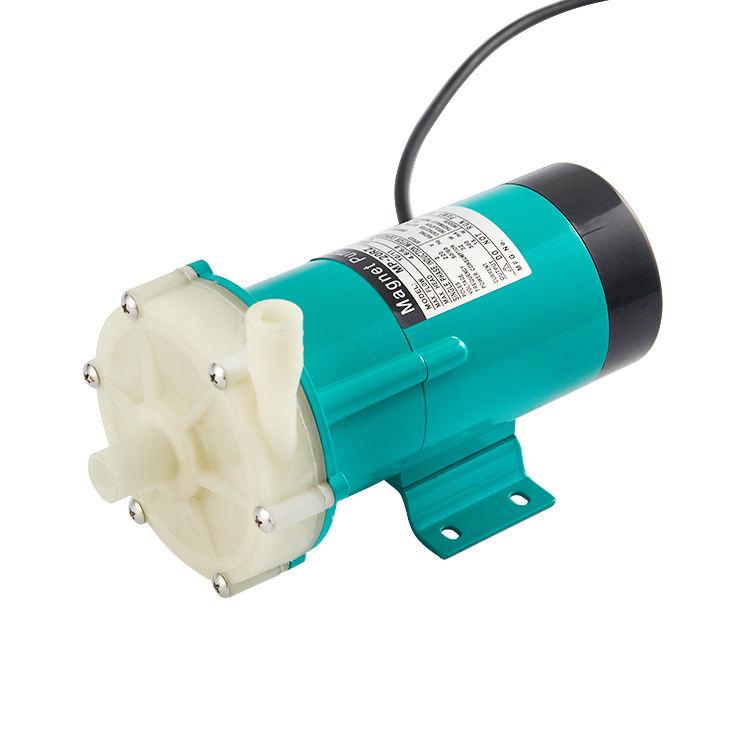
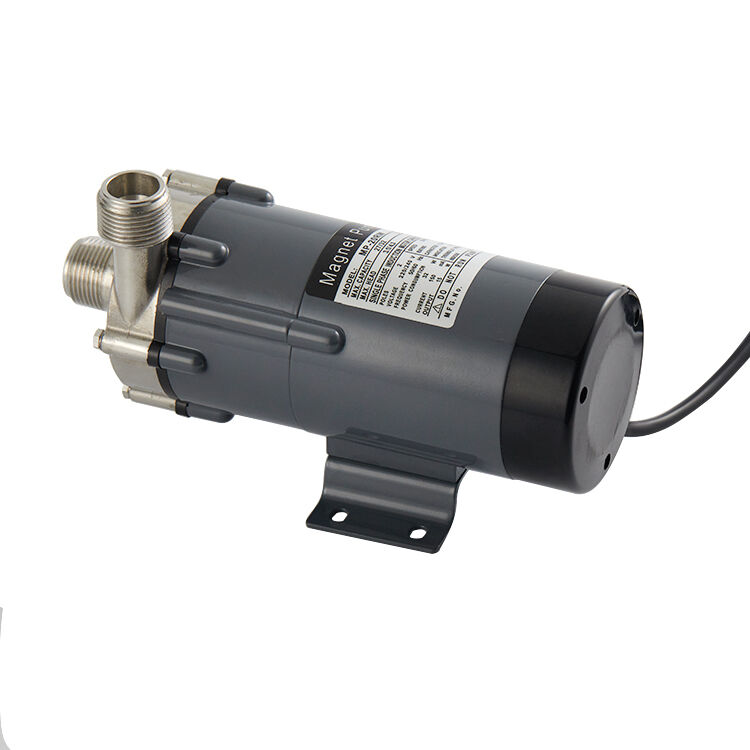
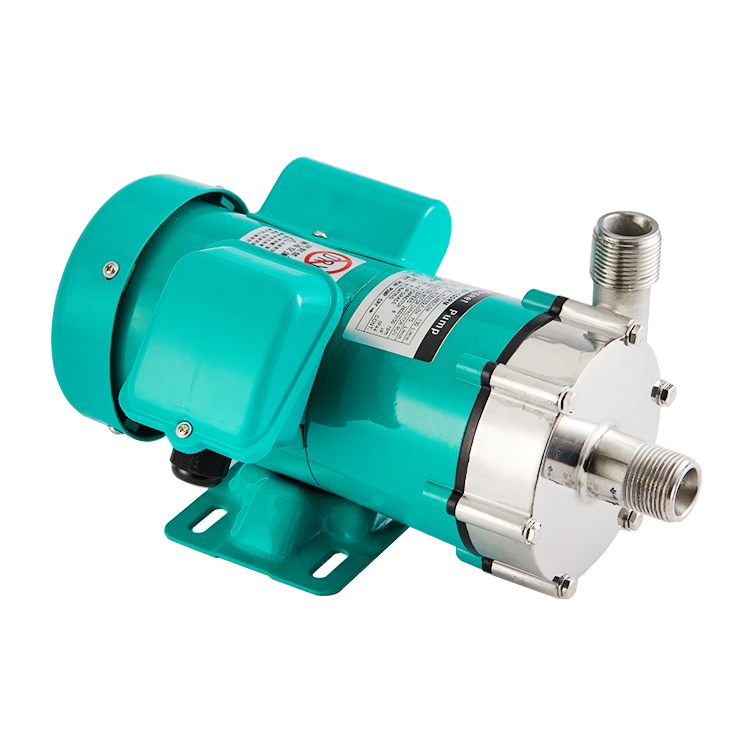
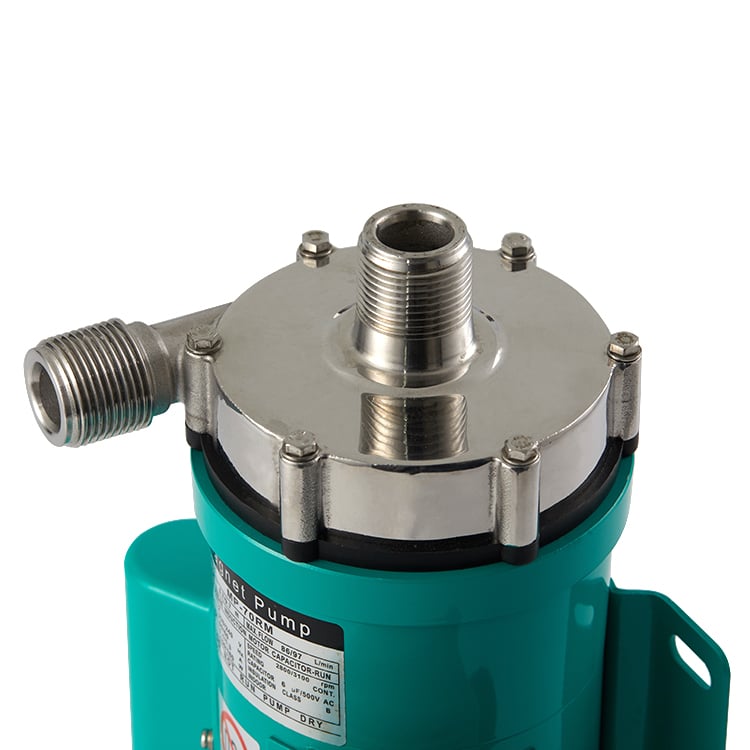
food grade wort pump
A food grade wort pump is a specialized brewing equipment designed to transfer wort safely and efficiently throughout the beer production process. This essential component moves hot wort from the kettle to the fermenter, cooling vessel, or other brewing equipment while maintaining product integrity and hygiene standards. The food grade wort pump operates using reliable centrifugal or peristaltic pumping mechanisms that ensure consistent flow rates without oxidation or contamination.
The primary function of a food grade wort pump is to facilitate smooth wort circulation during various brewing stages. Whether you need to recirculate during mashing, transfer after boiling, or move cooled wort into fermentation vessels, this pump handles all scenarios effectively. The pump's construction uses food-safe materials that meet strict industry regulations, ensuring your beer remains pure and uncontaminated throughout the transfer process.
Technologically, modern food grade wort pump systems feature temperature-resistant seals, stainless steel components, and variable speed controls. These features allow brewers to adjust flow rates according to specific requirements, from gentle transfers to vigorous circulation. The food grade wort pump also incorporates bypass valves and relief systems that protect your equipment from excessive pressure buildup.
Applications for a food grade wort pump span commercial breweries, craft beer production, and home brewing operations. Whether processing five gallons or five hundred, this versatile equipment handles diverse brewing volumes and configurations. The food grade wort pump proves invaluable in scaling production, reducing labor requirements, and improving consistency across brewing batches.

 EN