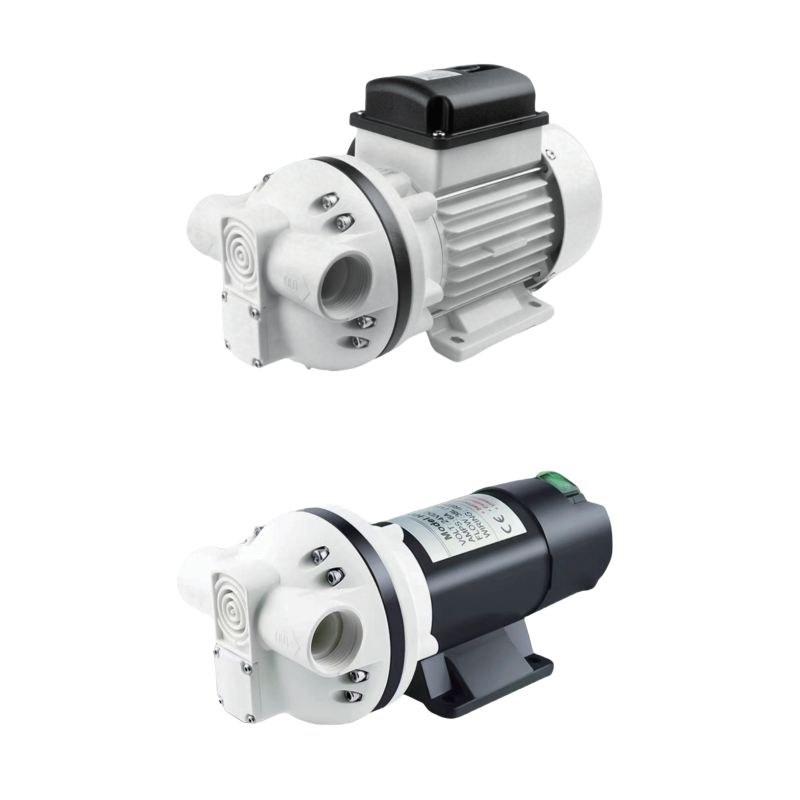
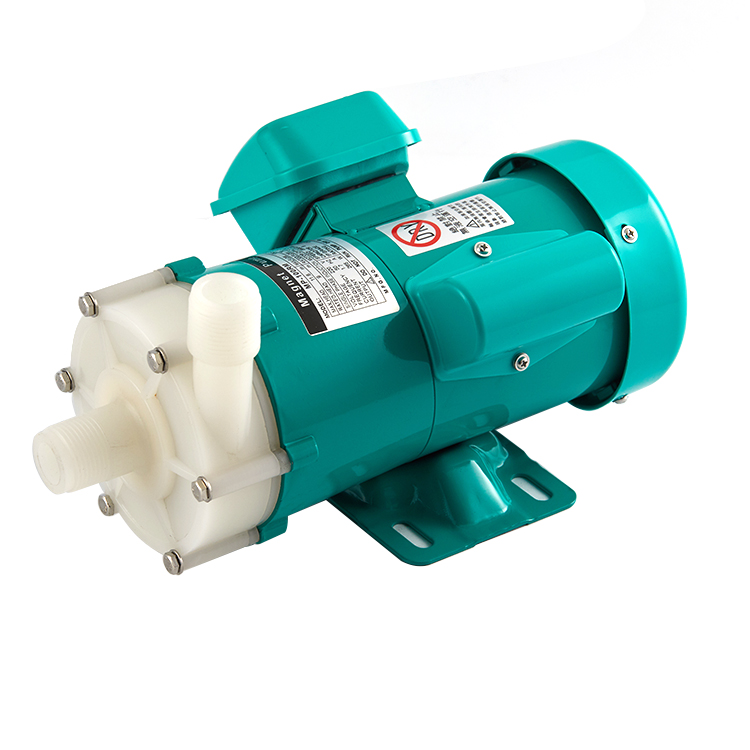
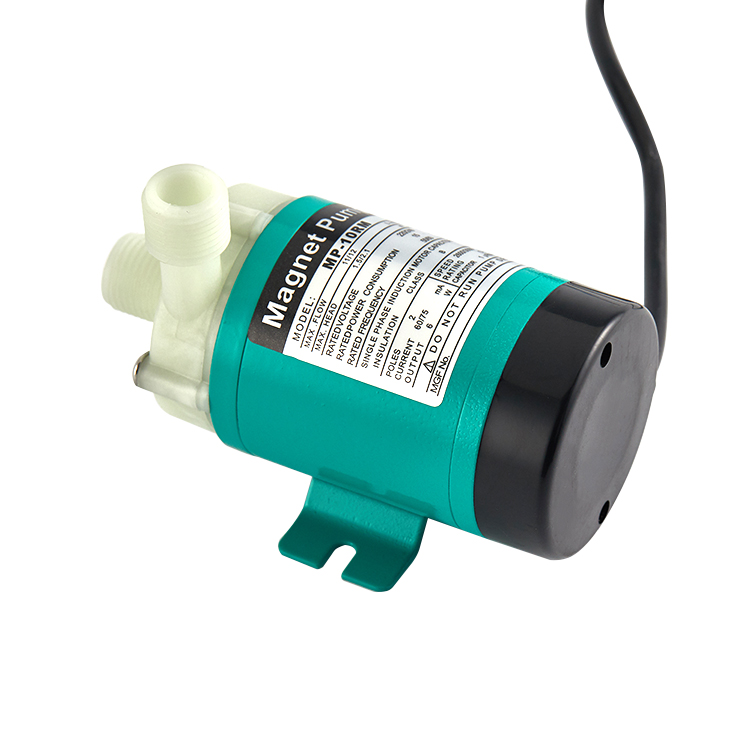
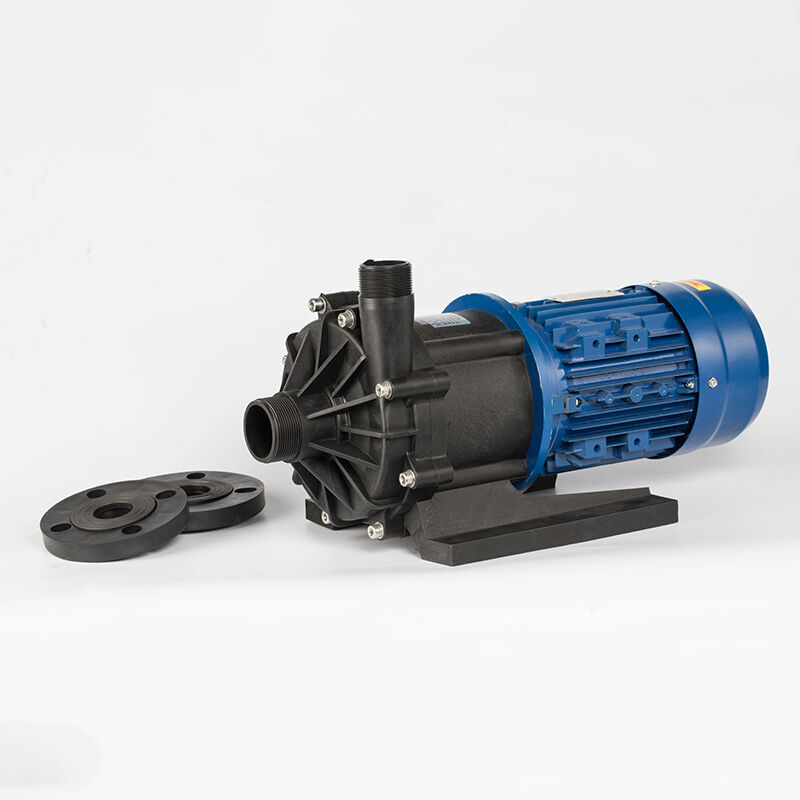
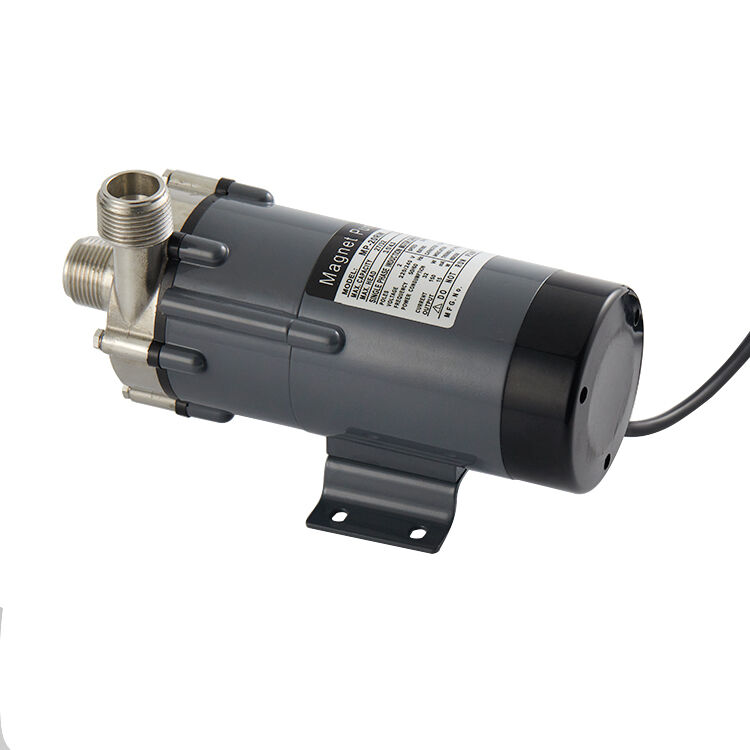
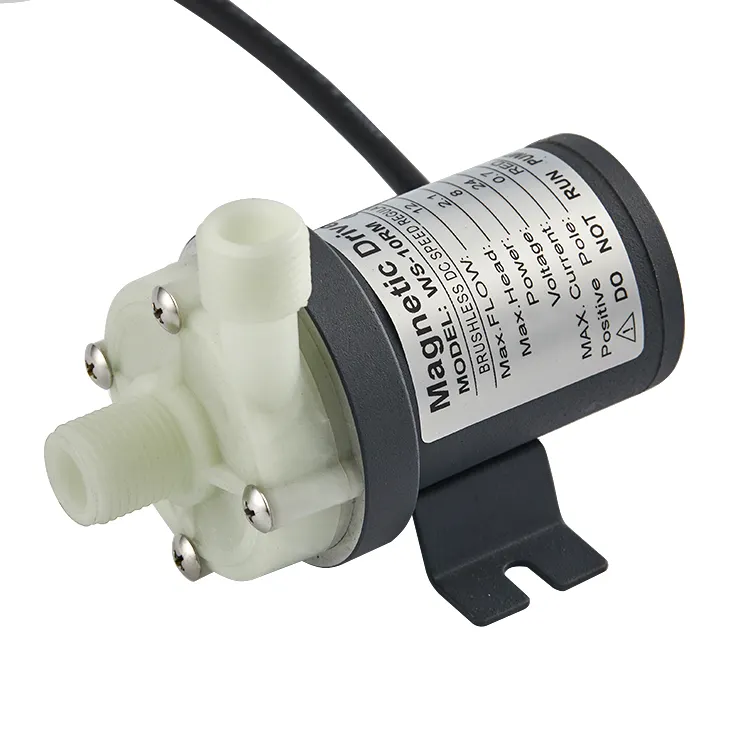
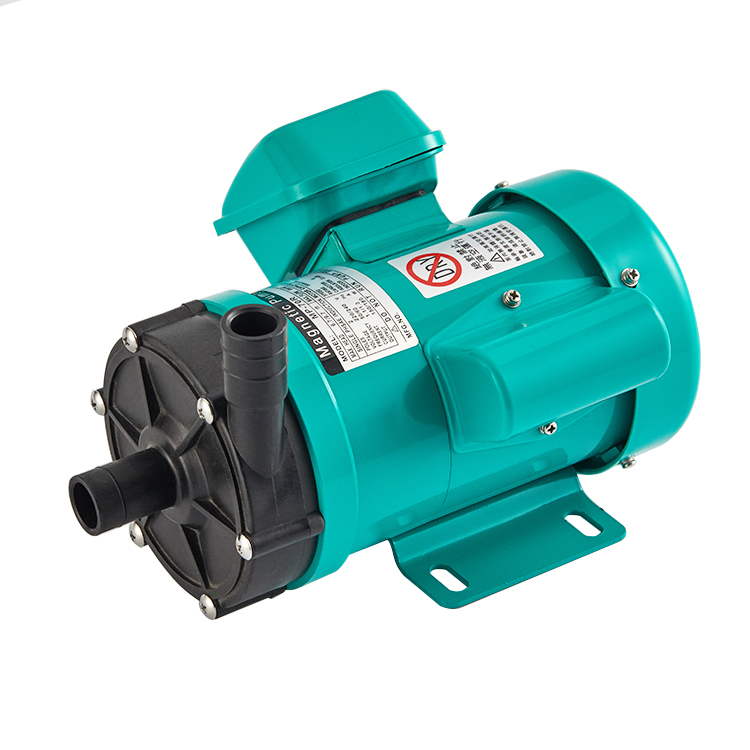
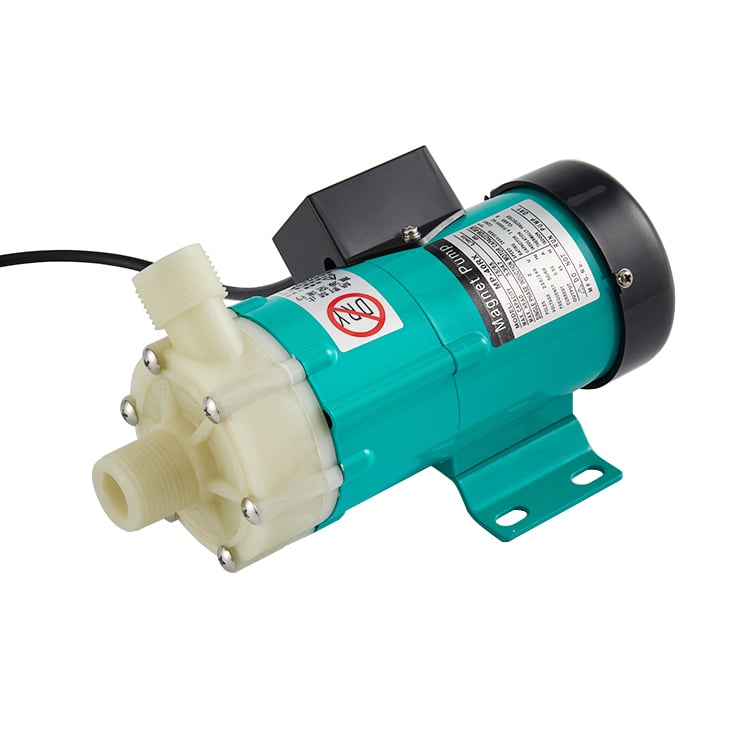
magnetic drive industrial pump
A magnetic drive industrial pump represents a sophisticated pumping solution designed to handle challenging fluid transfer applications across various industrial sectors. This innovative magnetic drive industrial pump utilizes magnetic coupling technology to eliminate traditional mechanical seals, creating a completely sealed system that prevents leakage and contamination.
The magnetic drive industrial pump operates by transferring rotational force through a magnetic field rather than direct shaft contact. Inside the pump housing, an outer magnet rotates with the motor shaft, while an inner magnet connects to the impeller. This magnetic connection allows power transmission without physical contact between moving components.
Key technological features of the magnetic drive industrial pump include its hermetically sealed design, which prevents any fluid escape during operation. The magnetic drive industrial pump excels in handling corrosive chemicals, hazardous materials, and volatile liquids where safety is paramount. Its robust construction ensures reliable performance in demanding environments.
Applications for the magnetic drive industrial pump span chemical processing, pharmaceutical manufacturing, wastewater treatment, and food production facilities. Industries requiring strict environmental compliance particularly benefit from this technology. The magnetic drive industrial pump performs efficiently in laboratories, refineries, and semiconductor manufacturing plants where contamination-free operations are essential.
The design eliminates maintenance associated with traditional mechanical seals, offering significant operational advantages. By choosing a magnetic drive industrial pump, facilities invest in sustainable, reliable fluid transfer technology that meets modern industrial standards and regulatory requirements.

 EN