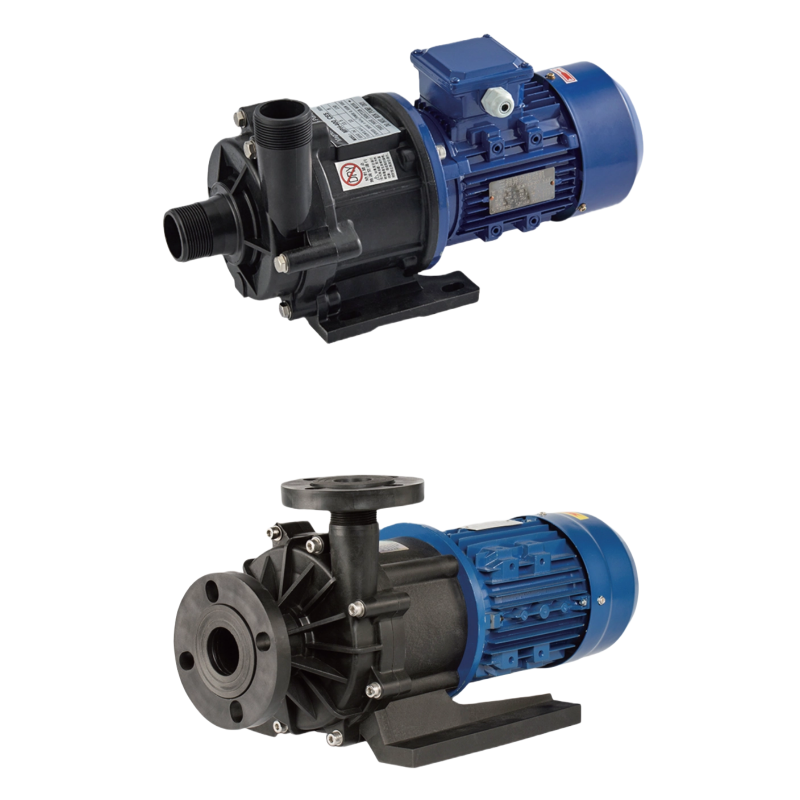
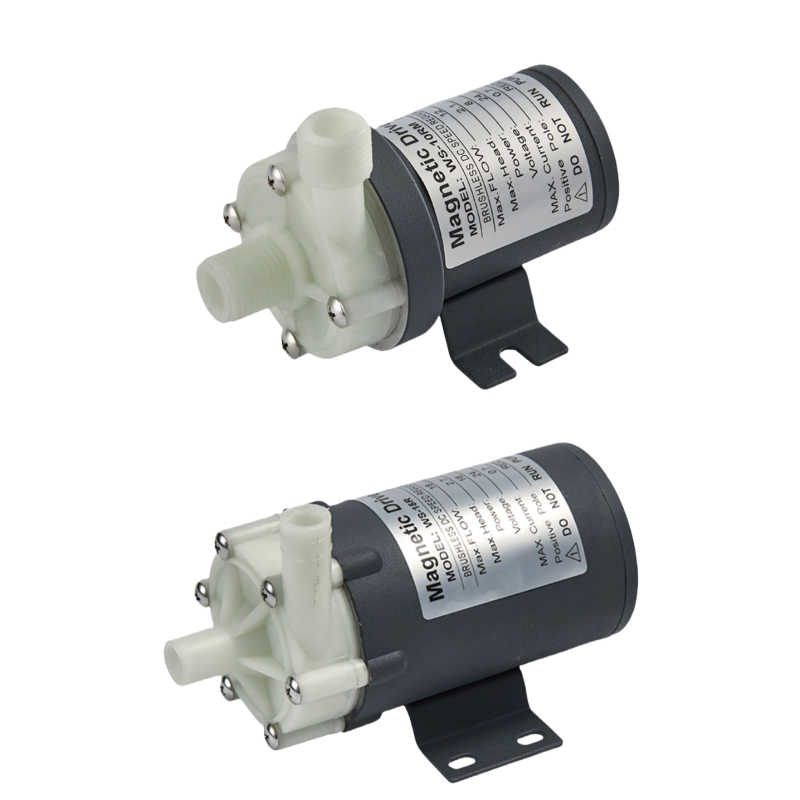
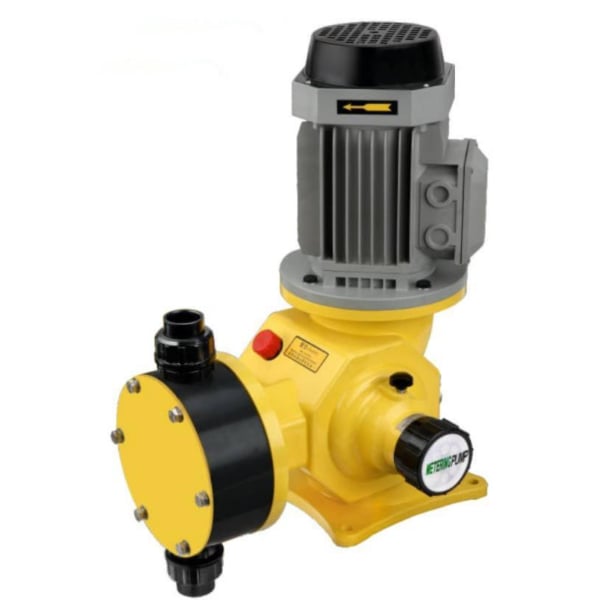
beer pump factory
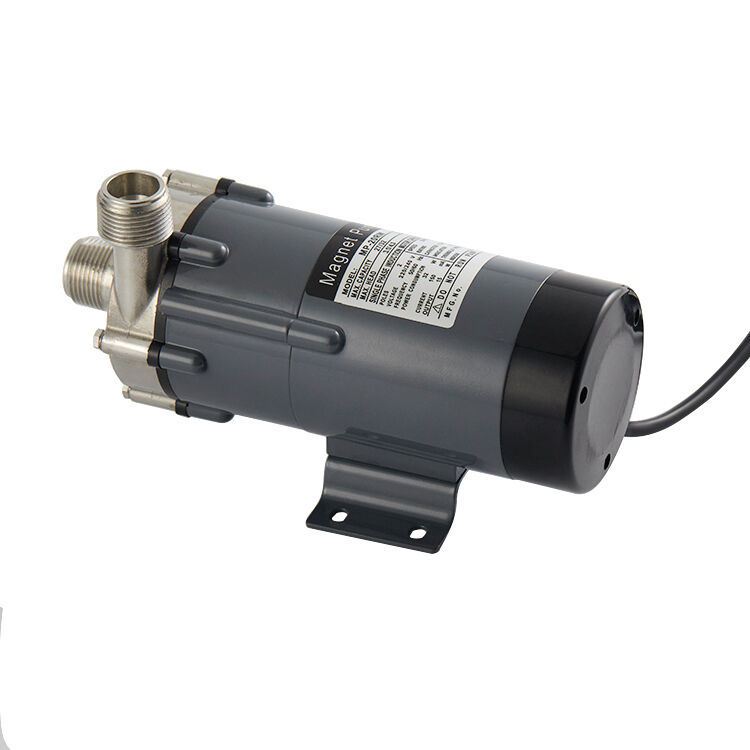
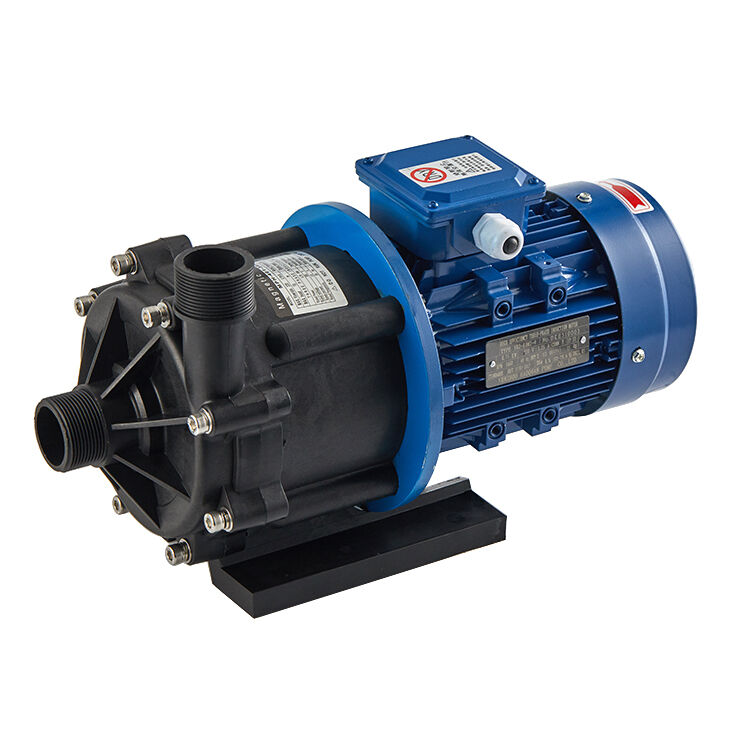
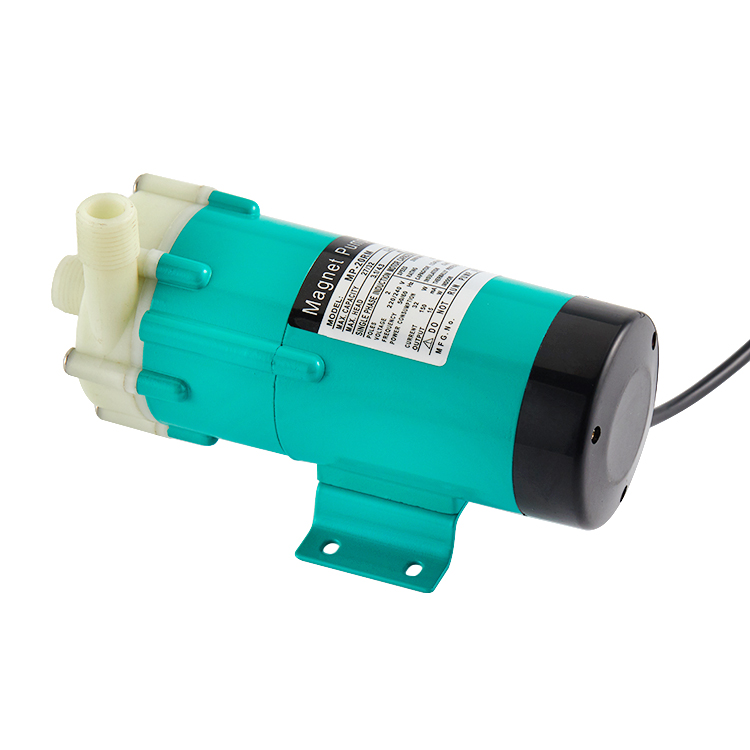
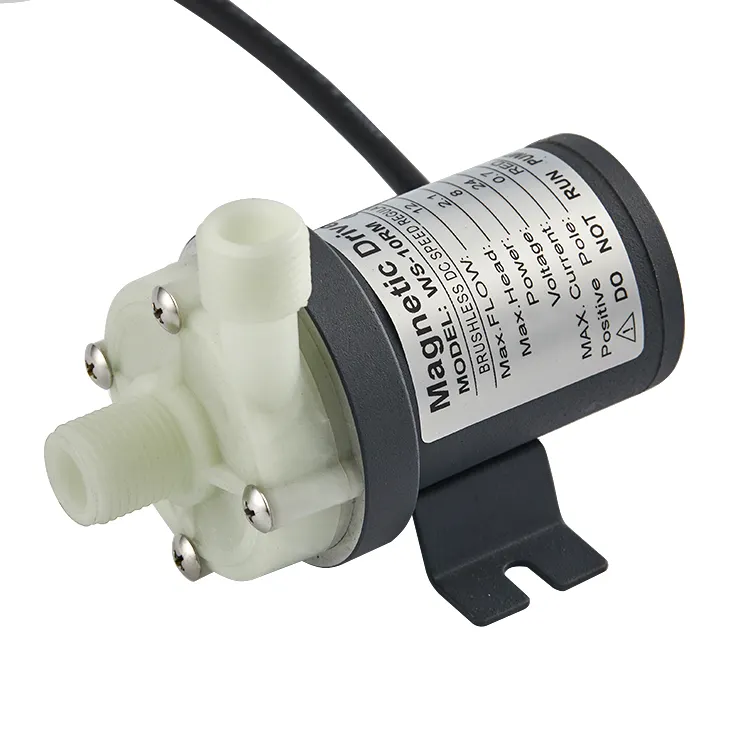
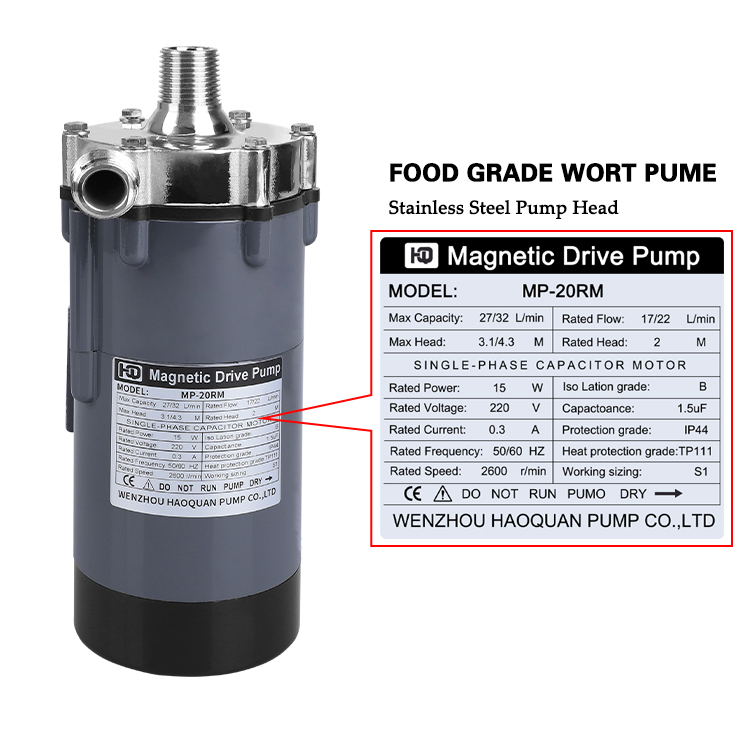
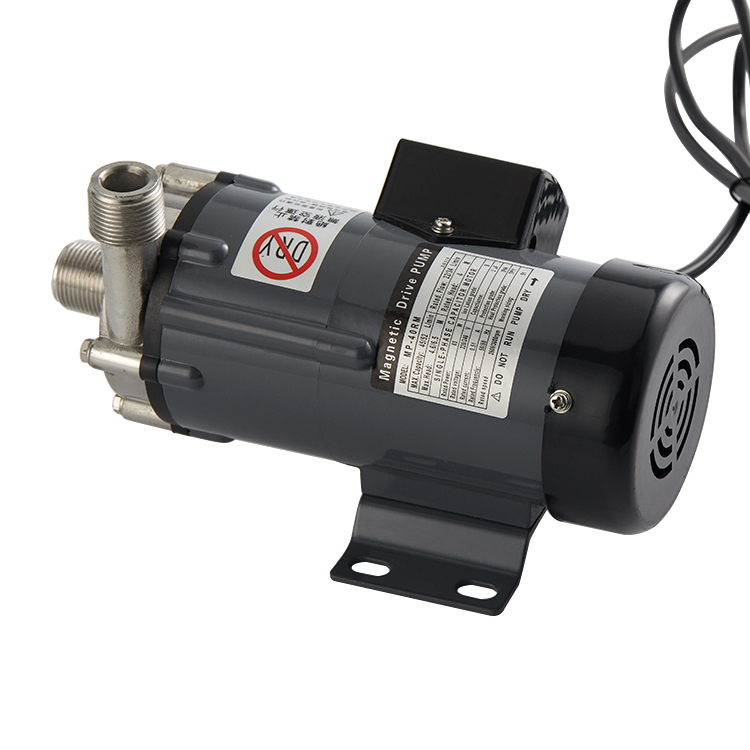
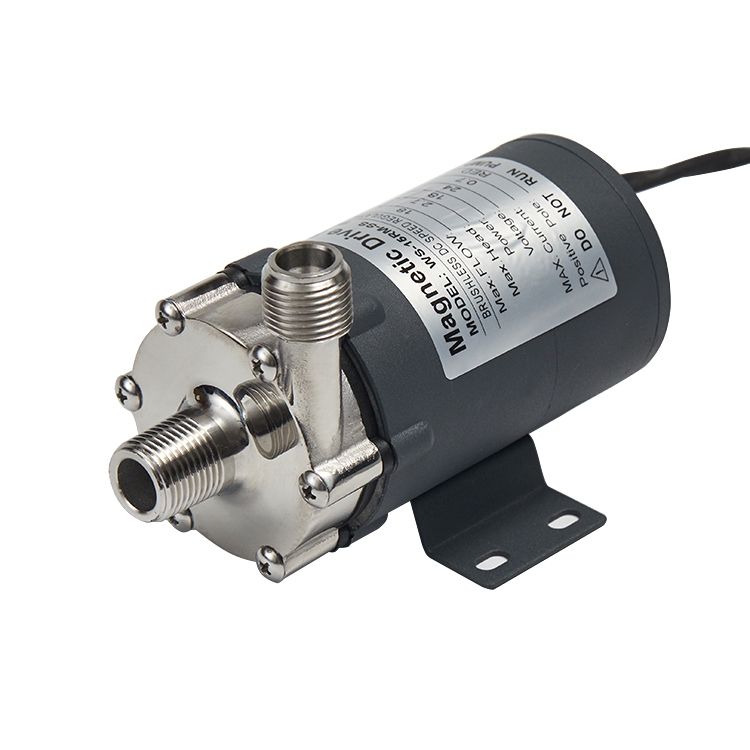
A beer pump factory represents a specialized manufacturing facility dedicated to producing high-quality pumping systems designed specifically for the beverage industry. The beer pump factory manufactures essential equipment that transfers beer efficiently throughout production, storage, and distribution stages. These facilities combine precision engineering with advanced automation technology to create pumps that meet stringent industry standards.
The primary functions of a beer pump factory include designing, manufacturing, and testing various pump models suitable for different beer production scales. Whether serving small craft breweries or large commercial operations, the beer pump factory produces equipment capable of handling the unique properties of beer, including its carbonation levels and viscosity requirements.
Technologically, modern beer pump factory operations feature state-of-the-art manufacturing systems that ensure consistency and reliability. These systems incorporate stainless steel components, sanitary design principles, and corrosion-resistant materials essential for beverage handling. Advanced quality control mechanisms throughout the beer pump factory production process guarantee that each unit meets international food-safety certifications.
Applications for equipment from a beer pump factory extend across the entire brewing industry. From fermentation tank transfers to kegging operations and distribution logistics, the beer pump factory supplies crucial equipment. The versatility of these pumps accommodates both carbonated and non-carbonated beverages, making them invaluable for modern breweries seeking reliable operational efficiency and product quality consistency.

 EN