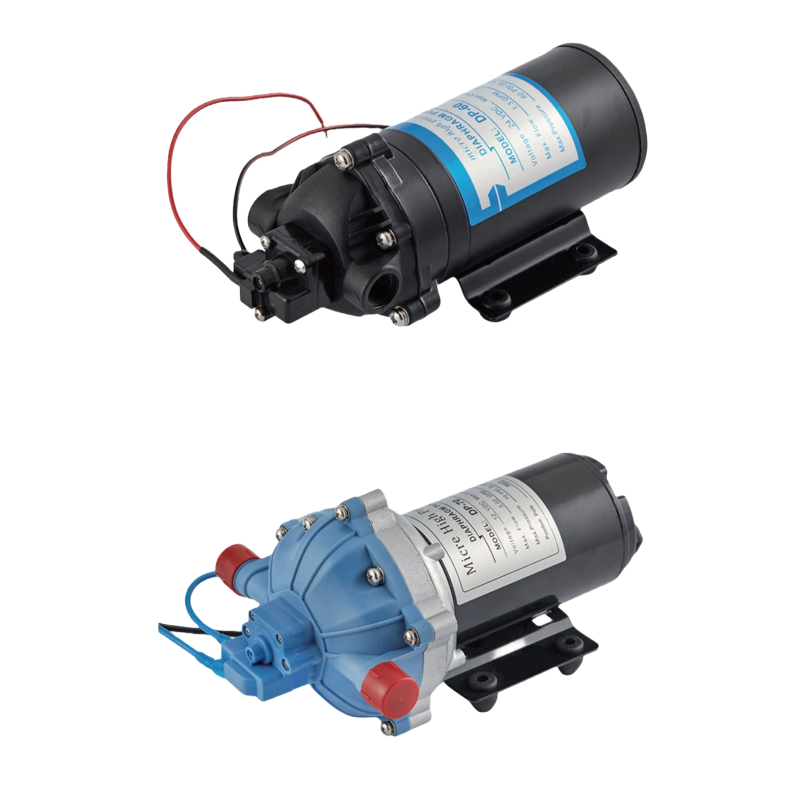
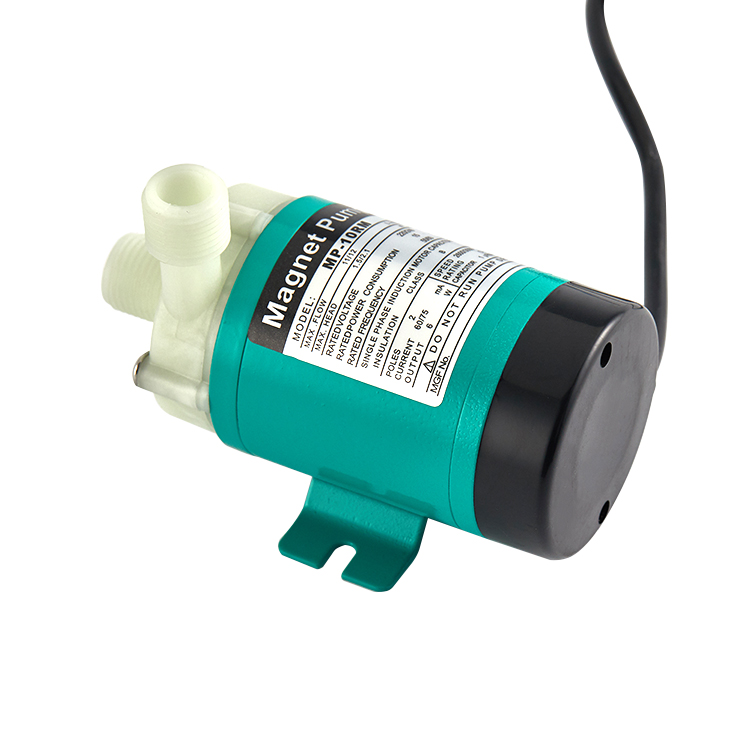
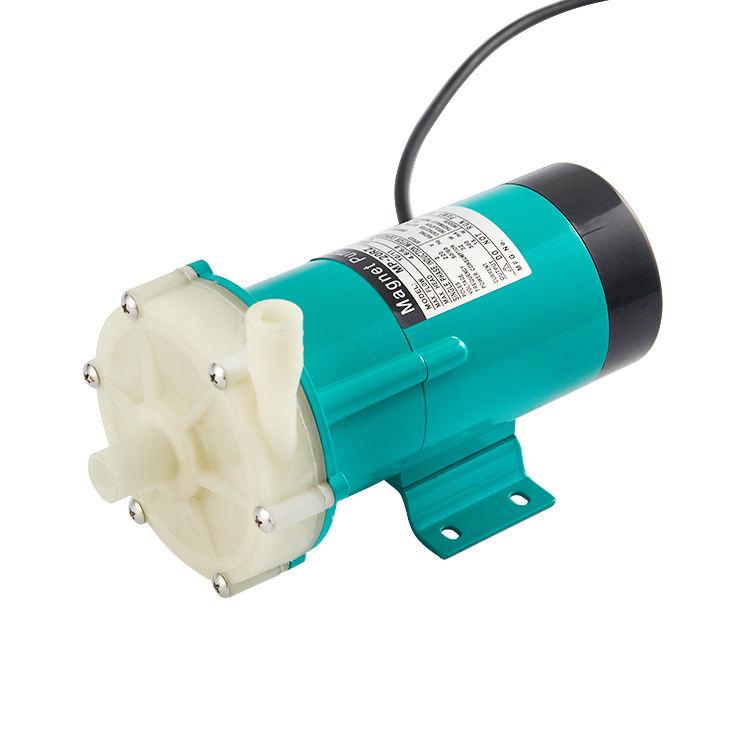
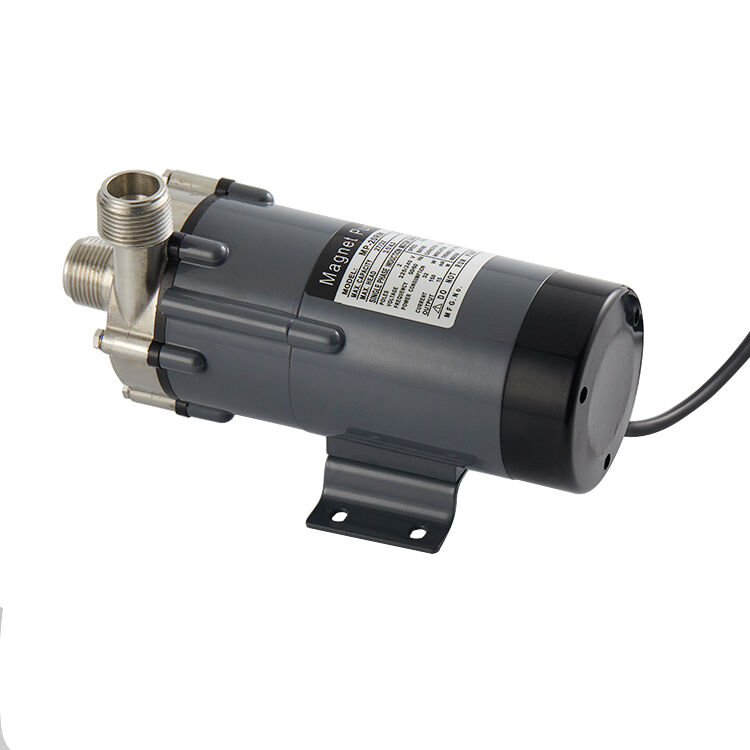
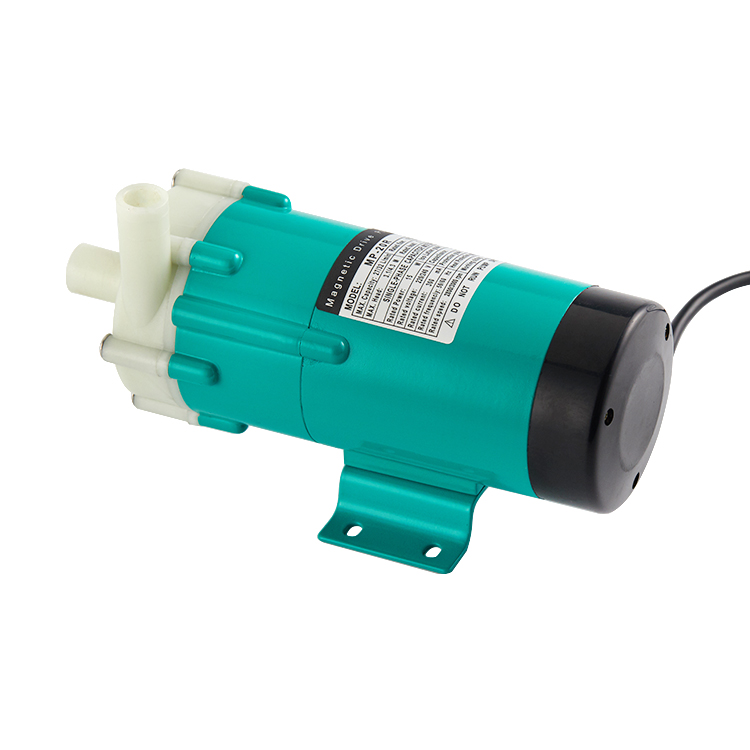
cooling pump factory
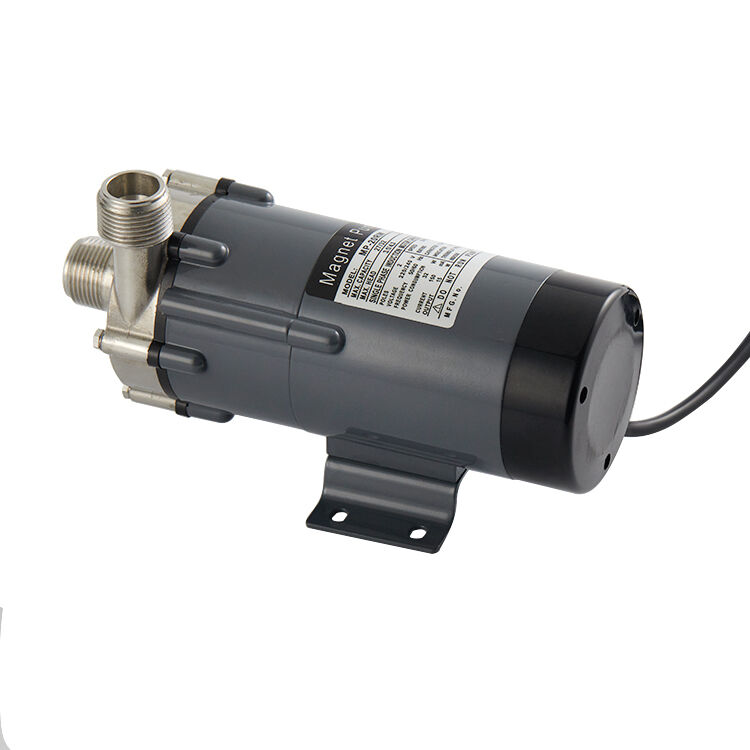
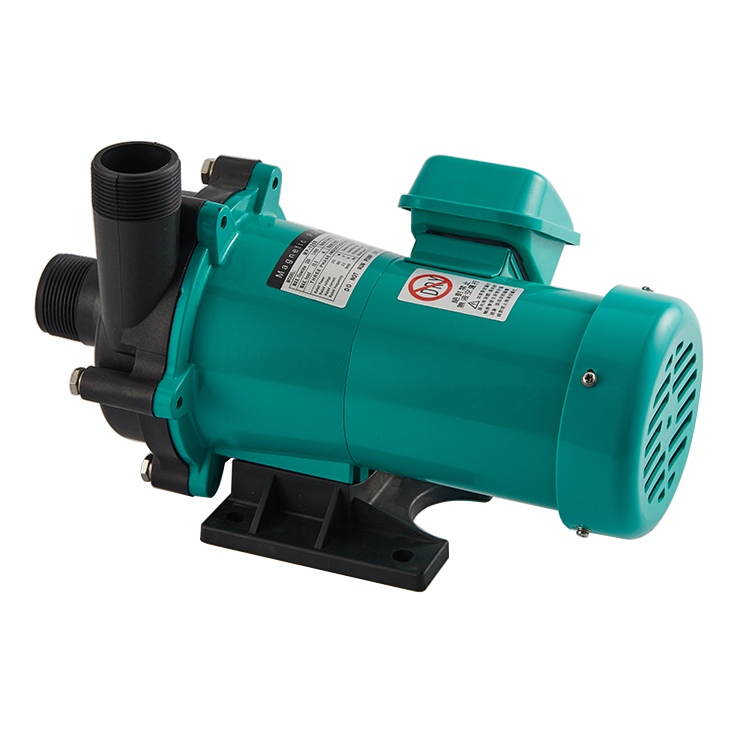
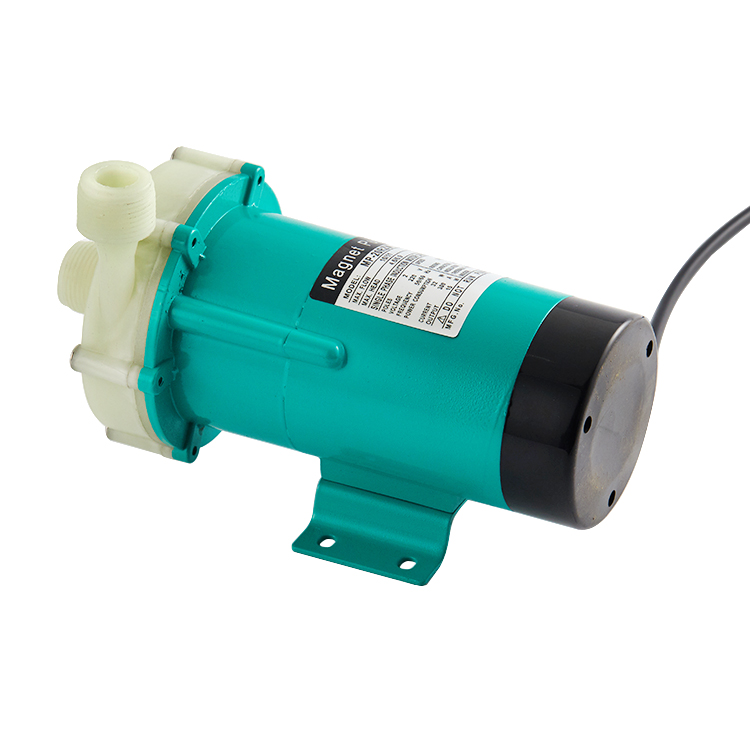
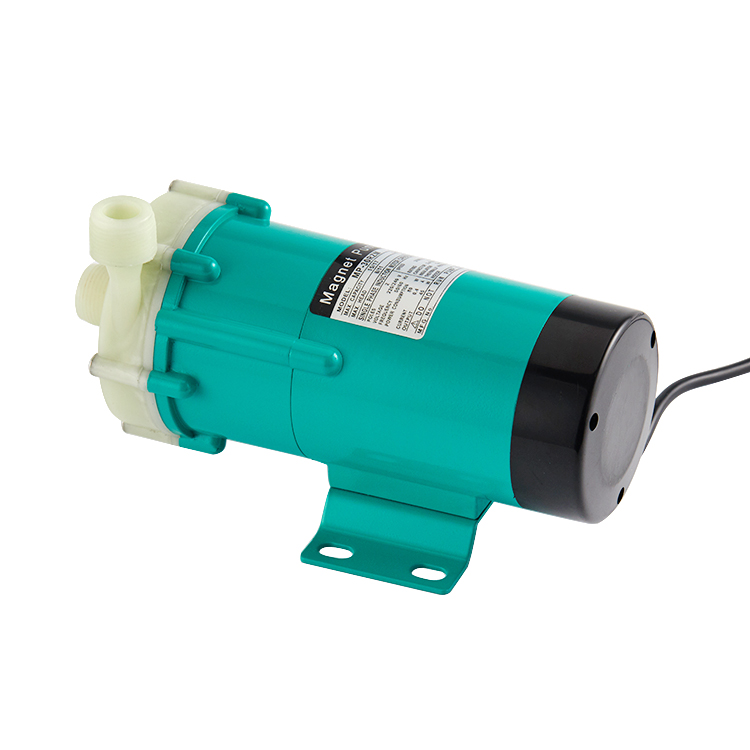
A cooling pump factory represents a specialized manufacturing facility dedicated to producing high-quality cooling pumps designed for diverse industrial and commercial applications. These facilities integrate advanced production technologies with rigorous quality control measures to deliver reliable cooling solutions. The cooling pump factory manufactures pumps that circulate coolant through systems to regulate temperature, prevent overheating, and maintain optimal operational conditions across various equipment and machinery.
The primary function of a cooling pump factory is to design, engineer, and produce pumps that efficiently transfer heat away from critical components. Whether for automotive engines, industrial machinery, HVAC systems, or data centers, the cooling pump factory creates solutions tailored to specific performance requirements. Modern cooling pump factories employ cutting-edge manufacturing techniques including precision machining, automated assembly, and comprehensive testing protocols.
Technological features of a professional cooling pump factory include variable speed capabilities, energy-efficient motor designs, corrosion-resistant materials, and smart monitoring systems. These pumps operate quietly, deliver consistent performance, and require minimal maintenance. The cooling pump factory utilizes CAD design software, CNC machinery, and robotics to ensure precision manufacturing. Quality assurance processes involve pressure testing, flow rate verification, and durability assessments before products reach customers.
Applications span numerous industries including automotive manufacturing, chemical processing, renewable energy systems, telecommunications infrastructure, and medical equipment. A cooling pump factory serves original equipment manufacturers, system integrators, and maintenance professionals who demand dependable cooling solutions. The facility's commitment to innovation ensures products meet evolving industry standards and customer expectations for performance and reliability.

 EN