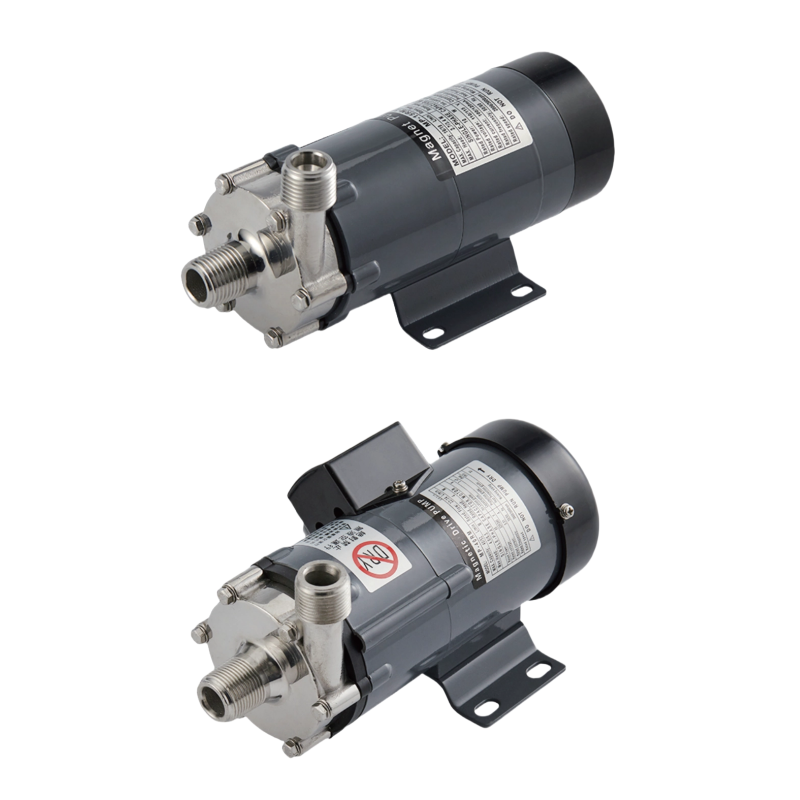
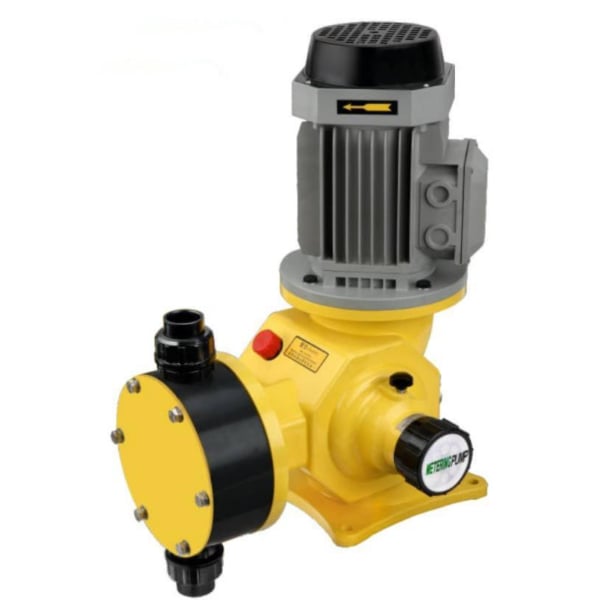
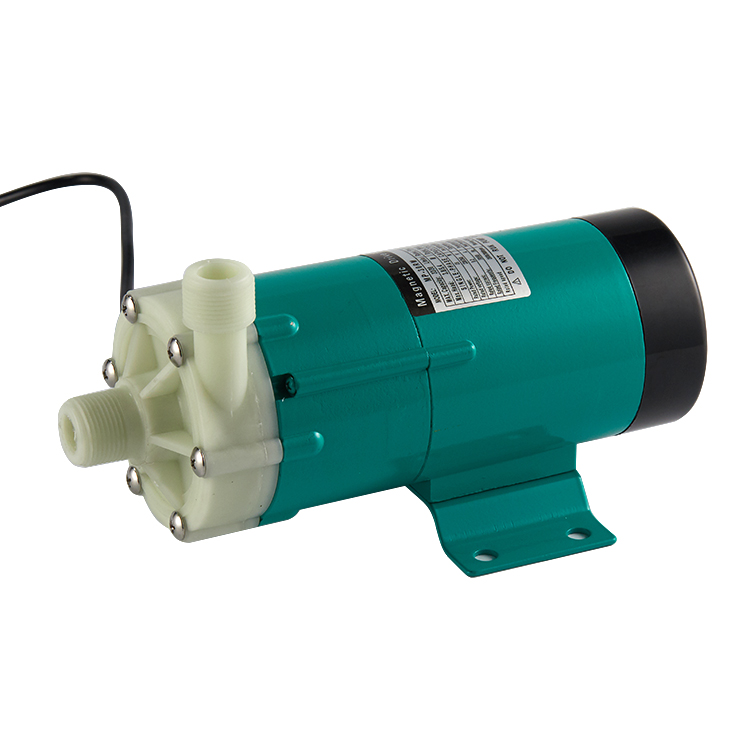
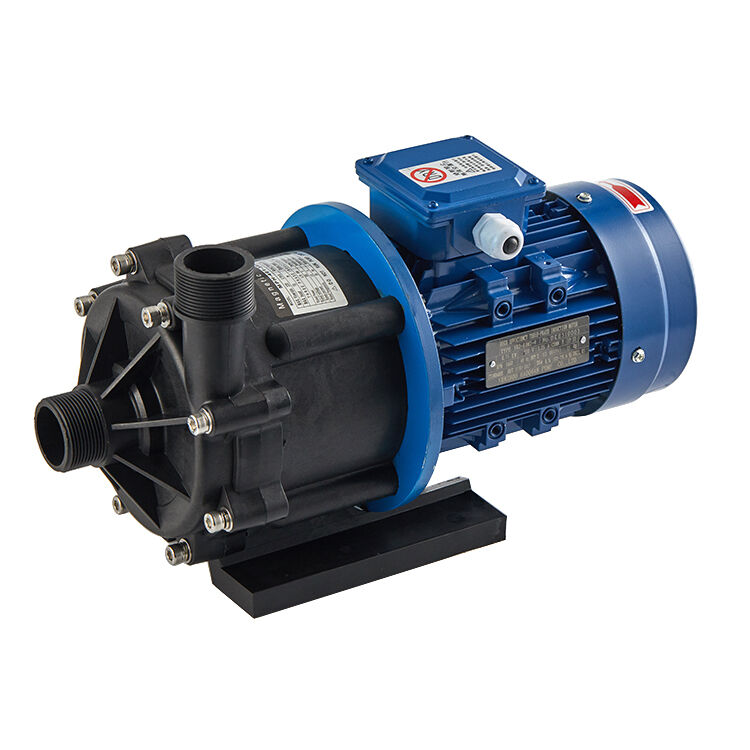
High Temperature Corrosive Pump Solutions

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

high temperature corrosive pump

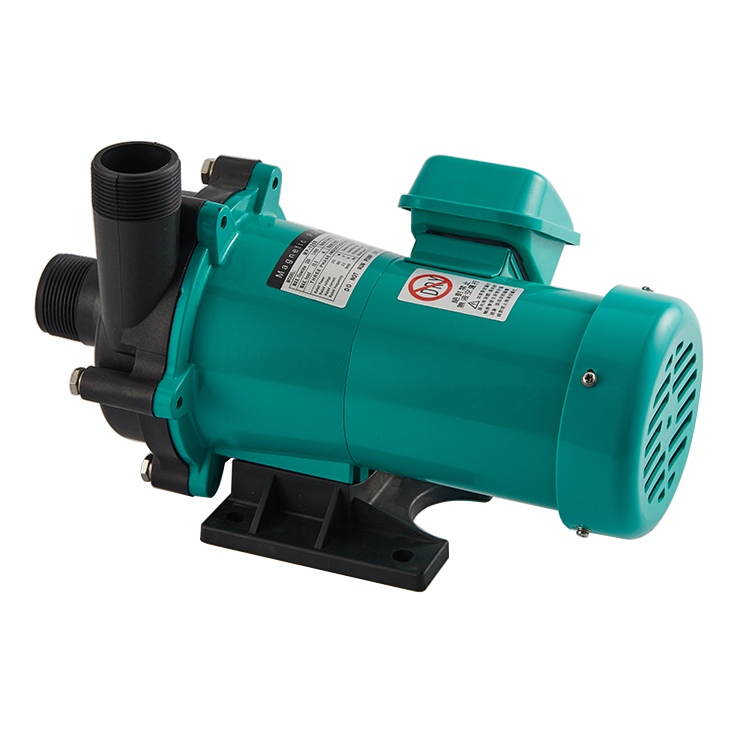
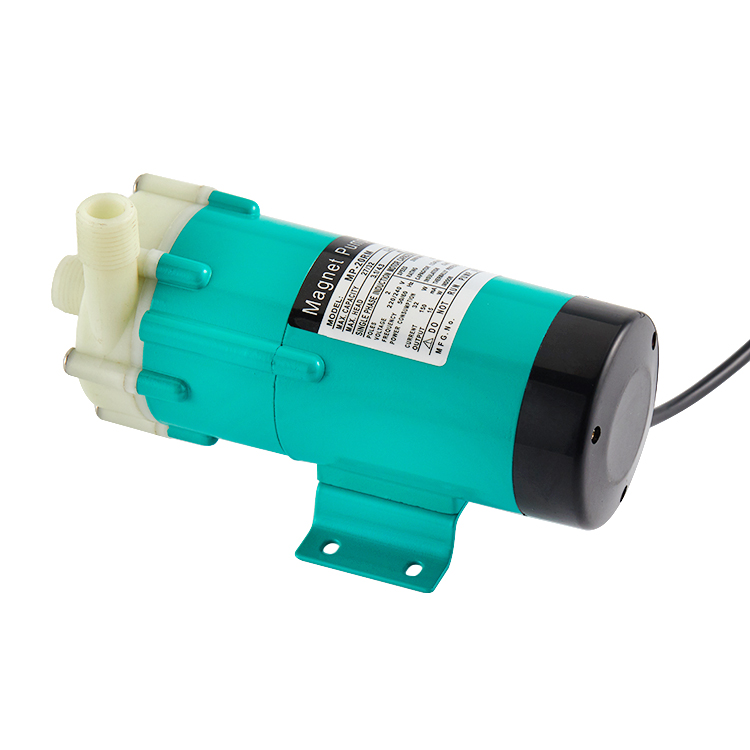
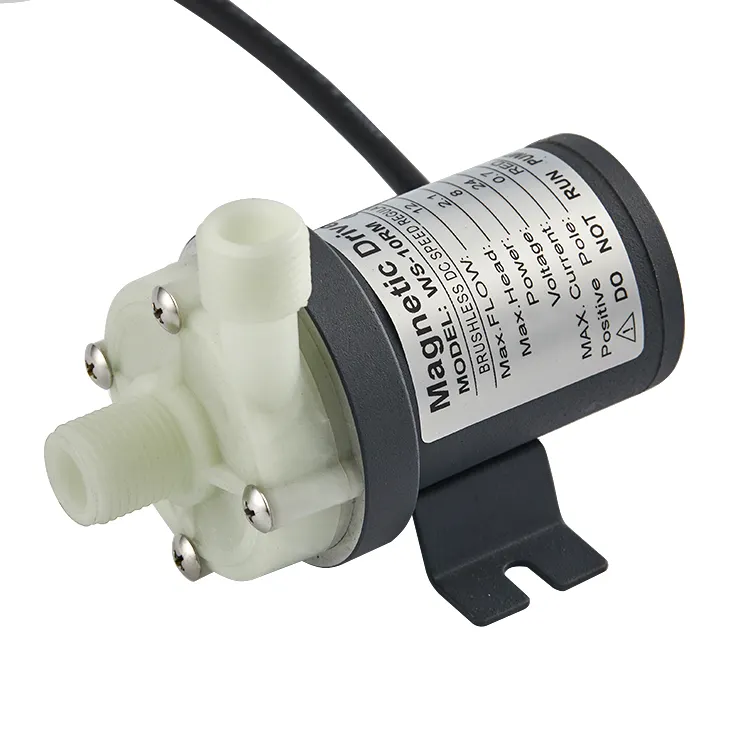
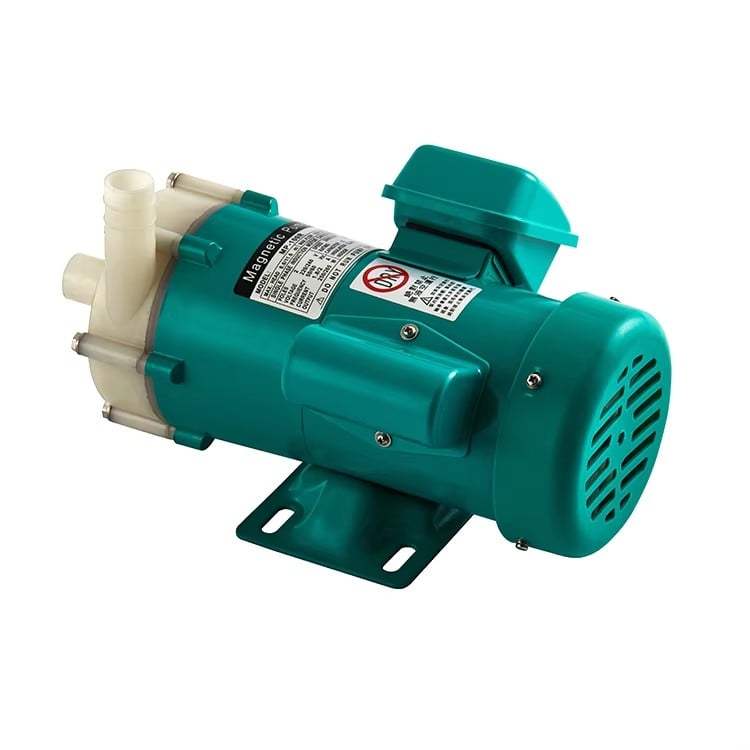
A high temperature corrosive pump represents a specialized industrial solution engineered to handle demanding fluid transfer applications in extreme environments. This high temperature corrosive pump is specifically designed to manage aggressive chemical compounds, molten substances, and corrosive materials at elevated temperatures that would damage conventional pumping equipment. The primary functions of a high temperature corrosive pump include reliably transferring corrosive liquids, handling thermal stresses, and maintaining operational integrity in harsh chemical settings. These pumps excel at moving caustic solutions, acidic fluids, and other reactive substances safely and efficiently across industrial processes. Key technological features distinguish a high temperature corrosive pump from standard alternatives. Advanced materials including specialized alloys, ceramics, and composite linings protect internal components from chemical degradation. Precision engineering minimizes turbulence and heat generation, while robust sealing systems prevent leakage of dangerous substances. Enhanced thermal management systems maintain optimal operating temperatures even when processing extremely hot fluids. Applications for the high temperature corrosive pump span multiple industries. Chemical manufacturing facilities depend on these pumps for processing aggressive compounds. Petrochemical operations utilize them for crude oil refinement and synthetic fuel production. Pharmaceutical companies employ high temperature corrosive pump systems for handling complex chemical intermediates. Power generation facilities use them in cooling systems and waste management. Mining operations rely on them for processing ore leachates and corrosive slurries. Each application demands absolute reliability and superior performance standards that only specialized high temperature corrosive pump solutions can provide.

New Products

The high temperature corrosive pump delivers exceptional value to industrial operations through multiple practical benefits that directly impact productivity and cost management. First, this equipment ensures superior reliability in aggressive environments where standard pumps fail rapidly. By using the high temperature corrosive pump, facilities eliminate frequent equipment replacements, reducing downtime and maintenance expenses significantly.

Operational efficiency represents another critical advantage of selecting a high temperature corrosive pump for your facility. Advanced design features minimize energy consumption while maximizing fluid transfer rates, directly lowering operational costs and improving profitability. The high temperature corrosive pump maintains consistent performance across extended operating periods, delivering predictable results that enhance production planning. Safety improvements constitute a substantial benefit of utilizing a high temperature corrosive pump technology. Robust containment systems prevent hazardous material leaks that endanger personnel and damage environments. Enhanced sealing mechanisms eliminate dangerous spillage, protecting your workforce and maintaining regulatory compliance. The high temperature corrosive pump design incorporates multiple safety layers ensuring workplace protection.

For industries processing caustic chemicals or handling extreme thermal conditions, the high temperature corrosive pump proves indispensable. This equipment accommodates temperature ranges exceeding standard alternatives by considerable margins. Specialized construction materials withstand aggressive chemical attacks that quickly corrode ordinary equipment. Investment in a quality high temperature corrosive pump translates to extended equipment lifespan and reduced total cost of ownership. Decision-useful product context demonstrates that choosing an appropriate high temperature corrosive pump determines operational success. Facilities upgrading from inadequate equipment to professional-grade solutions immediately recognize improved process control and enhanced product quality. The high temperature corrosive pump investment protects future operations while supporting current production demands.

Latest News

Shipping and Logistics Guide: Importing Large Volume Industrial Pumps from Wenzhou

09

Jun

Shipping and Logistics Guide: Importing Large Volume Industrial Pumps from Wenzhou

Introduction: Navigating the Logistics of Wenzhou’s Pump Industry Wenzhou, located in the Zhejiang province of China, is globally recognized as the "Capital of Pumps and Valves." For international B2B buyers, sourcing industrial pumps from Wenz...
View More
Industrial Pump Buying Guide: Centrifugal vs. Positive Displacement, Seal Types, and Energy Efficiency Explained

21

Jul

Industrial Pump Buying Guide: Centrifugal vs. Positive Displacement, Seal Types, and Energy Efficiency Explained

Buying the wrong industrial pump rarely shows up as an immediate failure. Instead, it appears months later as rising energy bills, frequent seal replacements, or gradual efficiency loss that erodes plant profitability. This guide brea...
View More
Magnetic Pump Buying Guide: Neodymium vs. Samarium-Cobalt Magnets, Dry Run Protection, and Flow Rate Explained

21

Jul

Magnetic Pump Buying Guide: Neodymium vs. Samarium-Cobalt Magnets, Dry Run Protection, and Flow Rate Explained

Magnet selection rarely gets the attention it deserves during a magnetic pump purchase, yet it directly affects how the pump performs under heat, chemical exposure, and demagnetization risk over its service life. Combined with dry run protecti...
View More
8 Benefits of Magnetic Pumps in Pharmaceutical and Semiconductor Manufacturing: Leak-Free, Contamination-Free Operation

21

Jul

8 Benefits of Magnetic Pumps in Pharmaceutical and Semiconductor Manufacturing: Leak-Free, Contamination-Free Operation

Pharmaceutical and semiconductor manufacturing share a demanding requirement that few other industries face simultaneously: absolute containment and absolute purity. A single leak or contamination event can compromise an entire batch, trigger regulat...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

high temperature corrosive pump

Advanced Material Construction for Maximum Durability

Advanced Material Construction for Maximum Durability

The high temperature corrosive pump incorporates revolutionary material science that sets industry standards for longevity and performance resilience. Specialized alloys and composite linings create protective barriers against the most aggressive chemical compounds, effectively neutralizing corrosion at molecular levels. These materials endure prolonged exposure to extreme temperatures without degradation, ensuring that your high temperature corrosive pump maintains structural integrity throughout its operational lifespan. This exceptional durability translates to measurable cost savings through extended maintenance intervals and dramatically reduced equipment replacement frequency. When processing caustic solutions or reactive chemicals daily, the advanced material composition becomes invaluable protection. Your high temperature corrosive pump investment proves economical because premium materials prevent catastrophic failures that interrupt production schedules and compromise safety protocols.
Enhanced Thermal Management and Cooling Systems

Enhanced Thermal Management and Cooling Systems

Modern high temperature corrosive pump technology incorporates sophisticated thermal regulation systems that stabilize internal temperatures even when processing extremely hot fluids. Intelligent cooling mechanisms continuously dissipate excess heat, preventing thermal damage to mechanical components and sealing systems. This high temperature corrosive pump feature ensures consistent performance regardless of external temperature conditions, maintaining reliability in challenging industrial environments. The thermal management capability extends equipment lifespan significantly while reducing catastrophic failure risks that threaten production continuity. Operators benefit from predictable performance because the high temperature corrosive pump maintains optimal operating conditions automatically. Enhanced cooling systems also protect sensitive pump components, ensuring that demanding applications no longer compromise equipment longevity or operational reliability.
Superior Sealing Technology for Complete Contamination Prevention

Superior Sealing Technology for Complete Contamination Prevention

The high temperature corrosive pump features revolutionary sealing mechanisms that virtually eliminate dangerous substance leakage, providing comprehensive environmental and workplace protection. Multi-stage sealing systems incorporate self-compensating designs that maintain effectiveness even as components experience thermal expansion and material wear. This high temperature corrosive pump sealing technology prevents hazardous spills that damage ecosystems and endanger personnel safety. Advanced seal materials resist chemical degradation that destroys conventional sealing solutions, maintaining integrity across extended operating periods. Your high temperature corrosive pump investment includes reliability assurance that regulatory inspectors and safety auditors recognize as superior compliance. The enhanced sealing capability transforms facility operations by eliminating contamination concerns, allowing seamless production while meeting stringent environmental protection standards.
High Temperature Corrosive Pump Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000