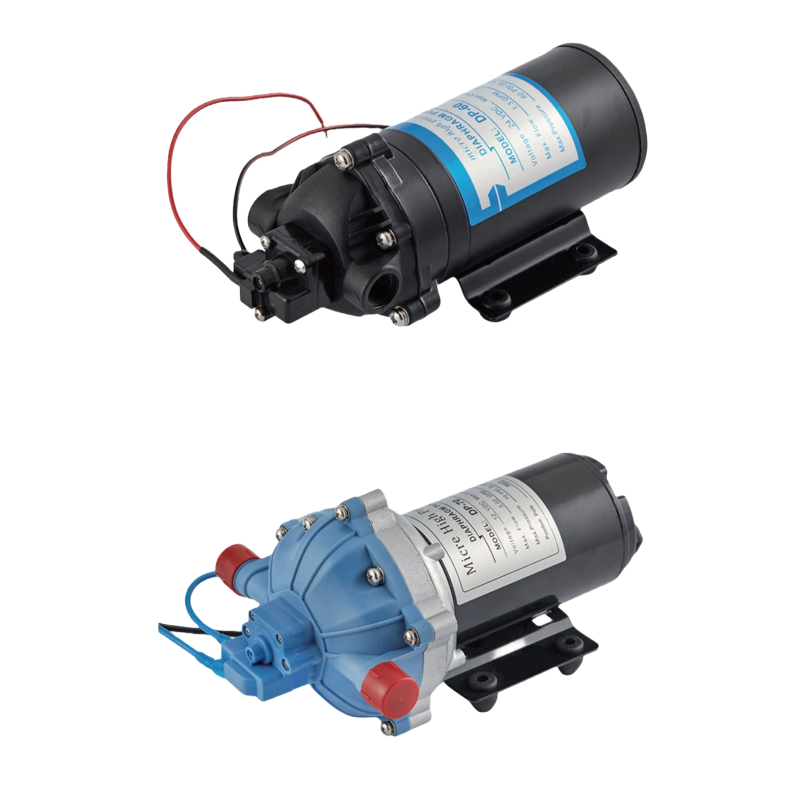
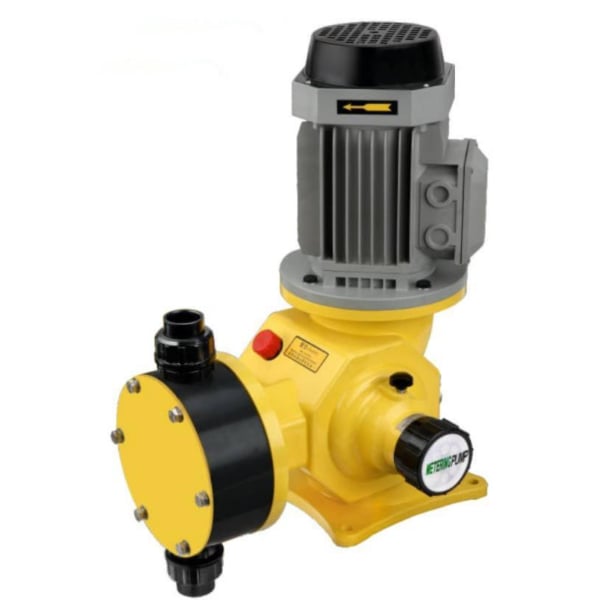
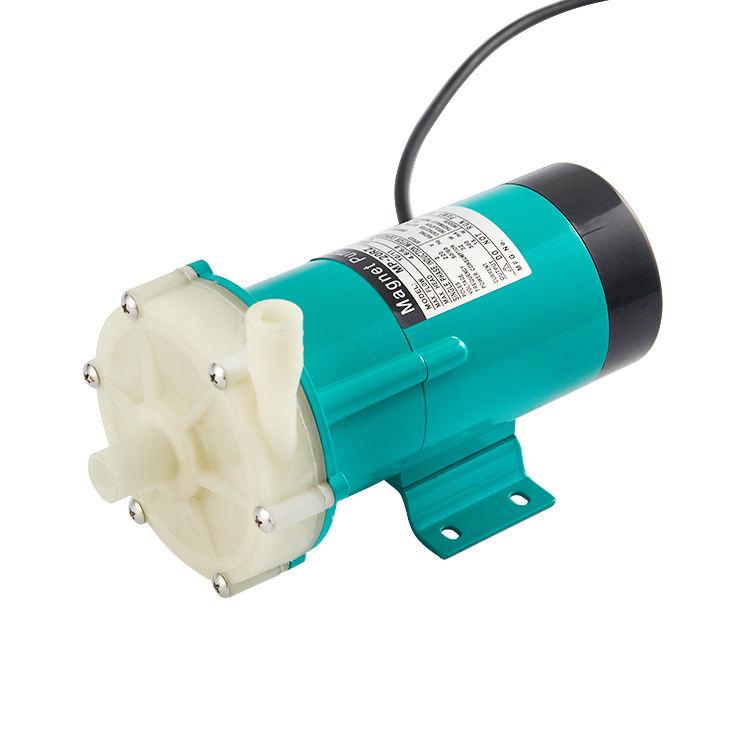
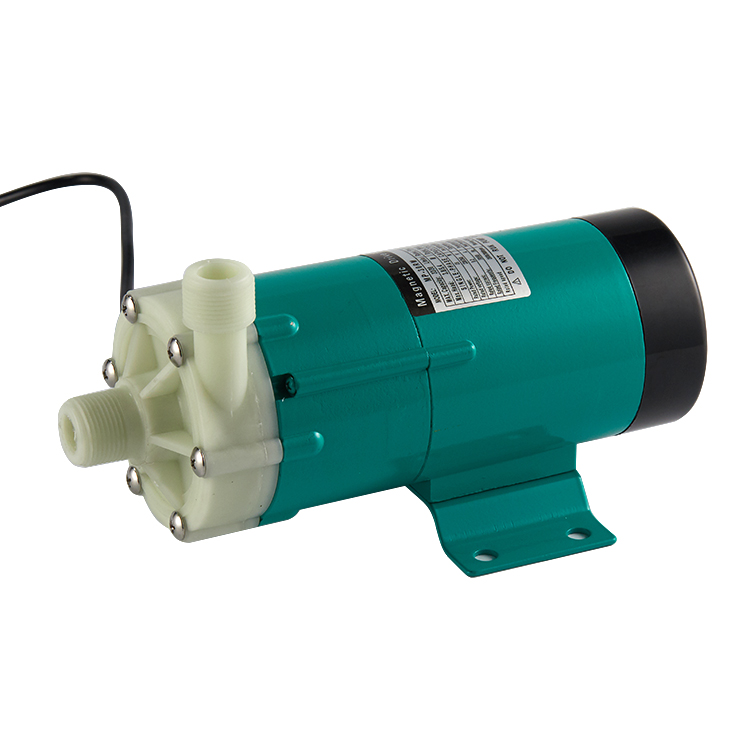
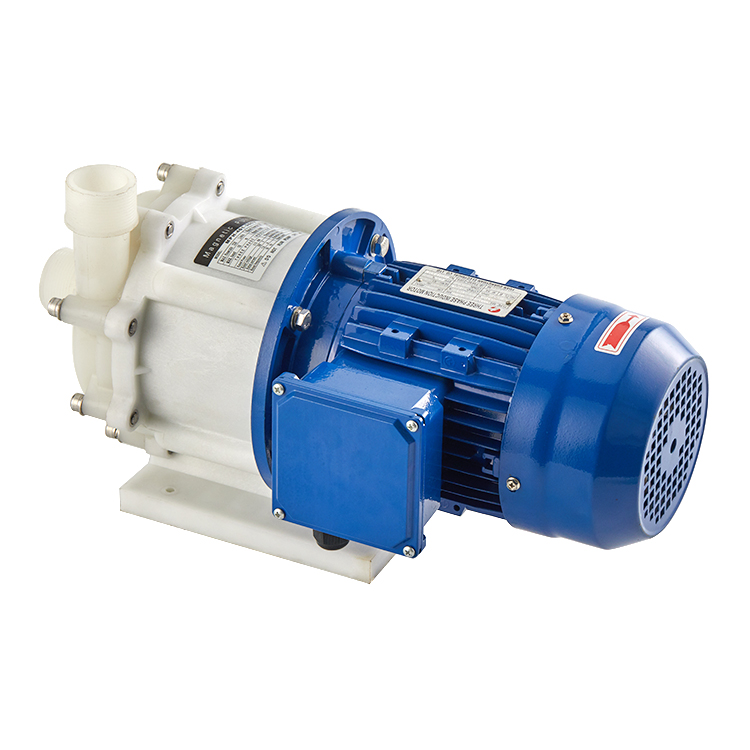
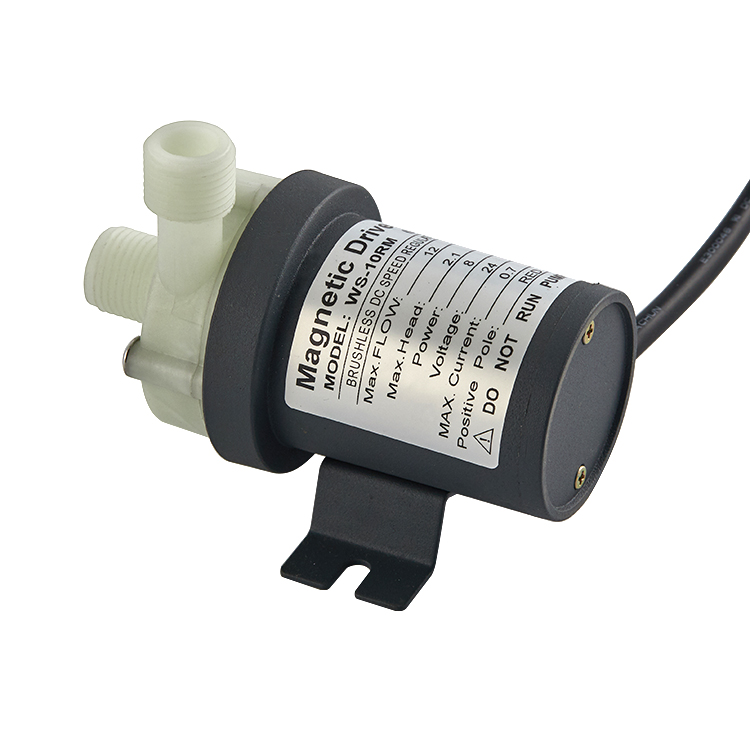
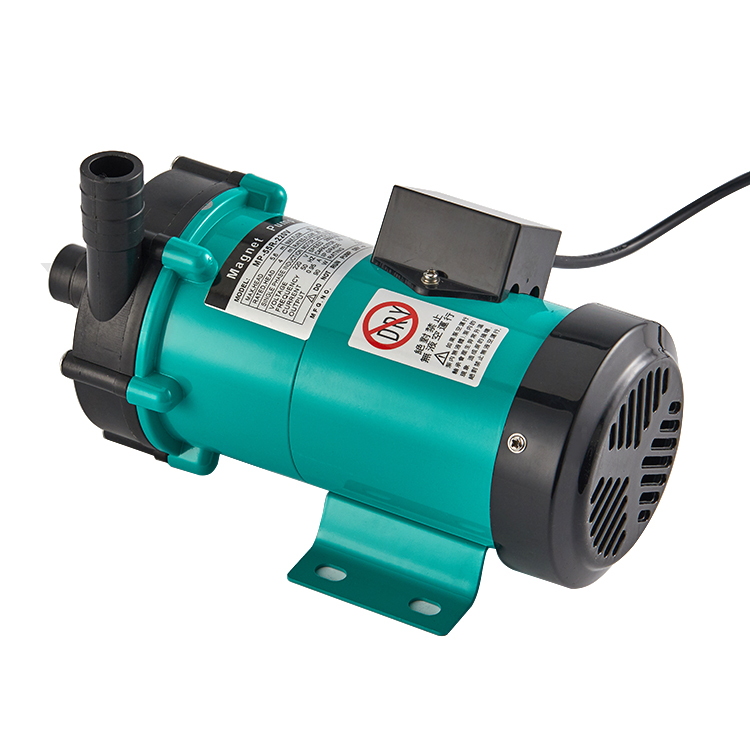
hydrofluoric acid pump
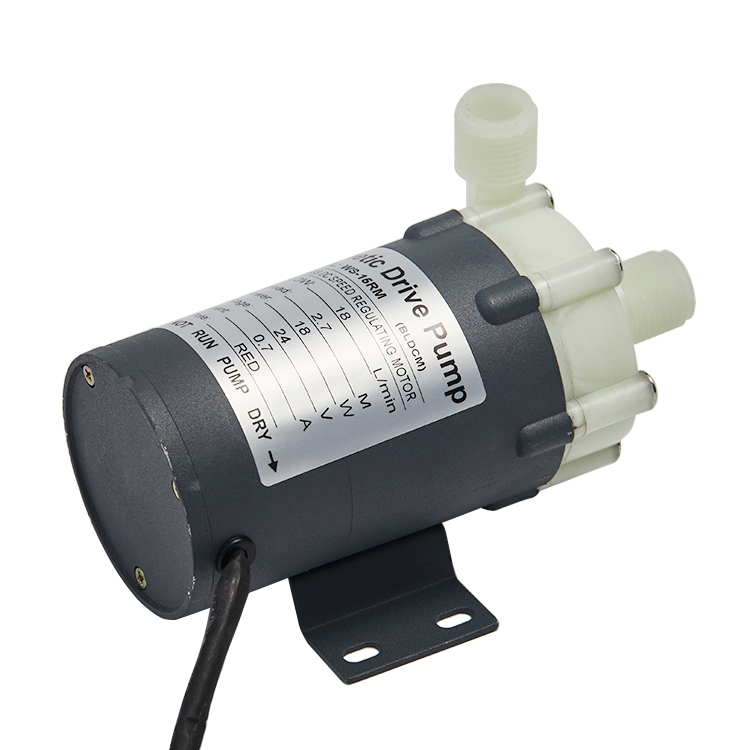
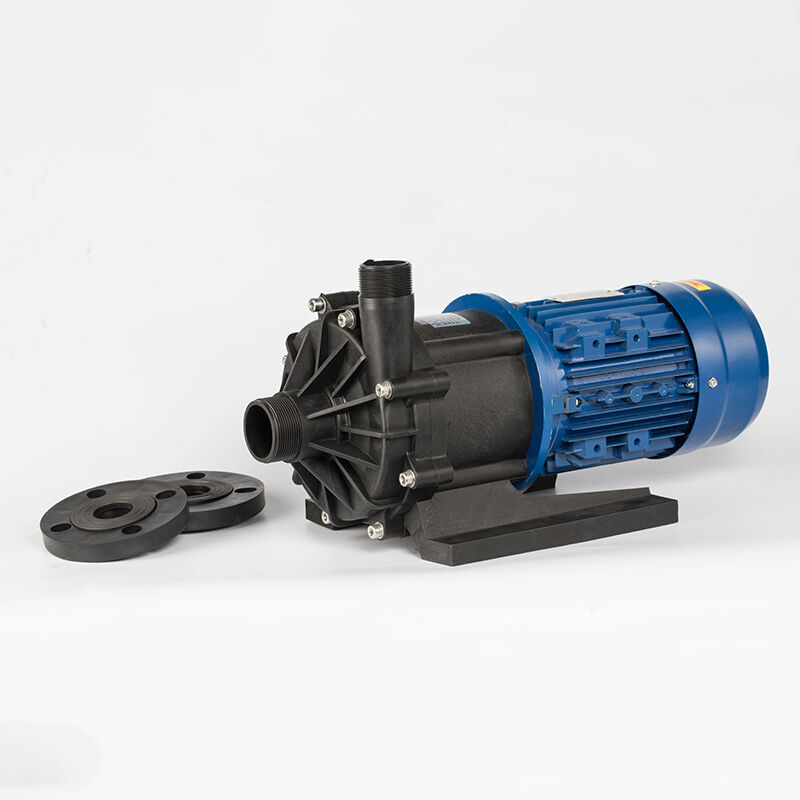
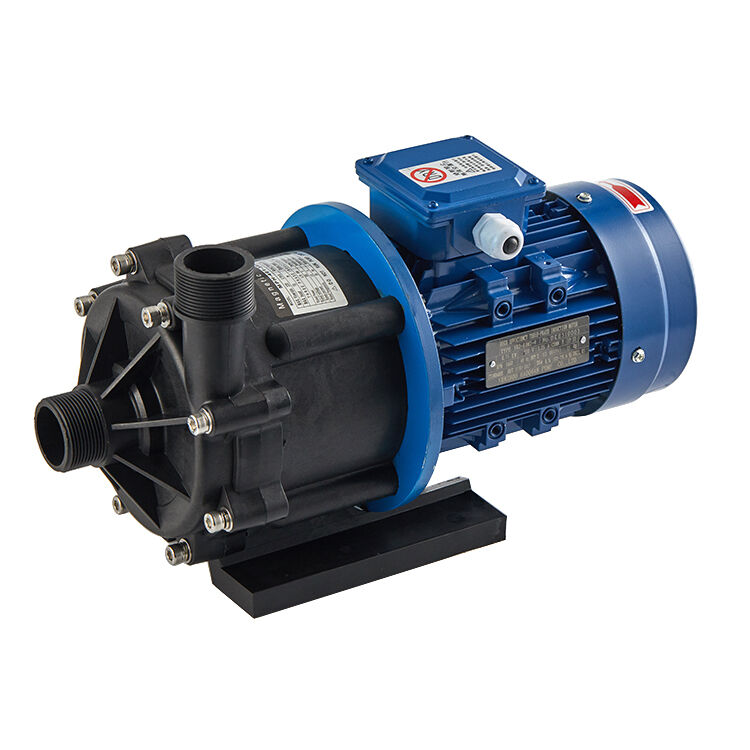
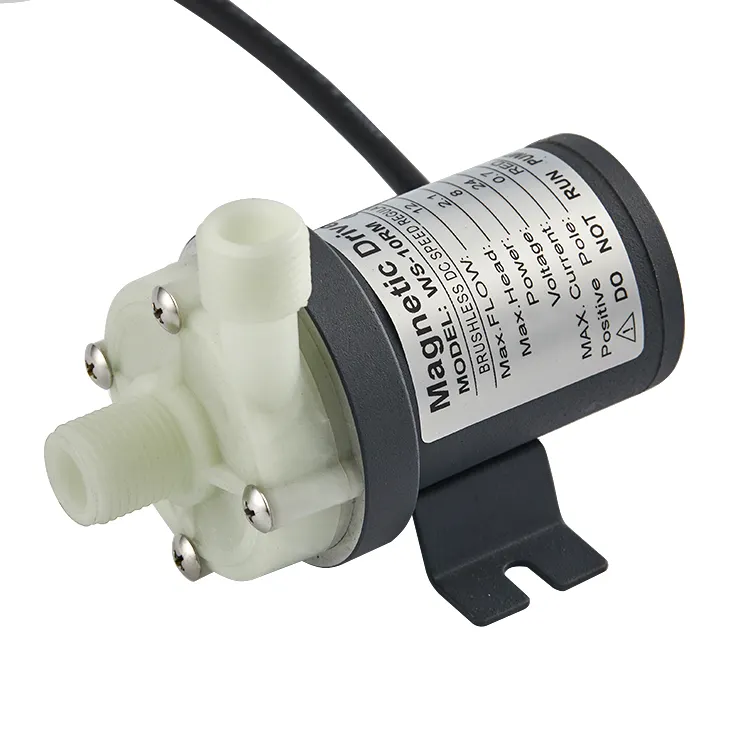
A hydrofluoric acid pump is a specialized chemical transfer device engineered to safely handle and circulate hydrofluoric acid in industrial applications. This hydrofluoric acid pump represents a critical investment for facilities managing corrosive chemical processes. The hydrofluoric acid pump operates by using chemically resistant materials that withstand the extreme corrosive properties of hydrofluoric acid without degradation or failure.
The primary function of a hydrofluoric acid pump involves transferring hydrofluoric acid from storage containers to processing equipment with precision and reliability. Modern hydrofluoric acid pump designs incorporate advanced sealing mechanisms and specialized impeller configurations that prevent leakage and ensure consistent flow rates. These pumps feature magnetic drive technology or seal-less designs that eliminate common failure points associated with traditional centrifugal pumps.
Key technological features include fluoropolymer coatings, titanium components, and specialized bearing assemblies rated for extreme chemical environments. The hydrofluoric acid pump utilizes materials like PTFE, PFA, and polyetheretherketone to resist acid penetration and maintain structural integrity during extended operations.
Applications for a hydrofluoric acid pump span multiple industries including uranium enrichment, pharmaceutical manufacturing, petroleum refining, and metal surface treatment. These pumps handle demanding chemical processing requirements where safety and efficiency directly impact operational costs and regulatory compliance. Industries depend on the hydrofluoric acid pump to maintain consistent production schedules while protecting personnel and facilities from hazardous chemical exposure.

 EN