acid pump manufacturer
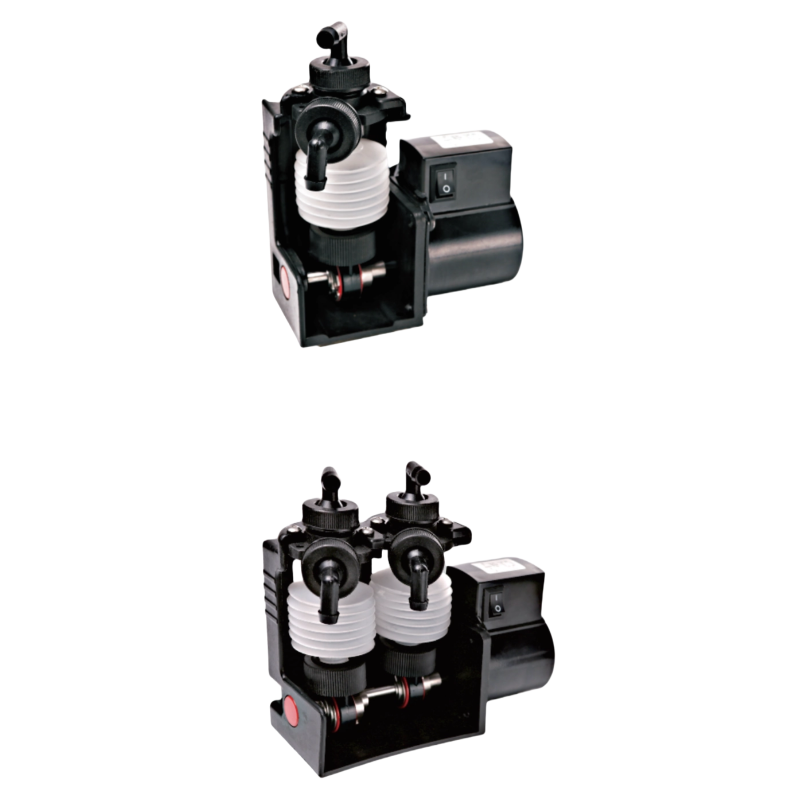
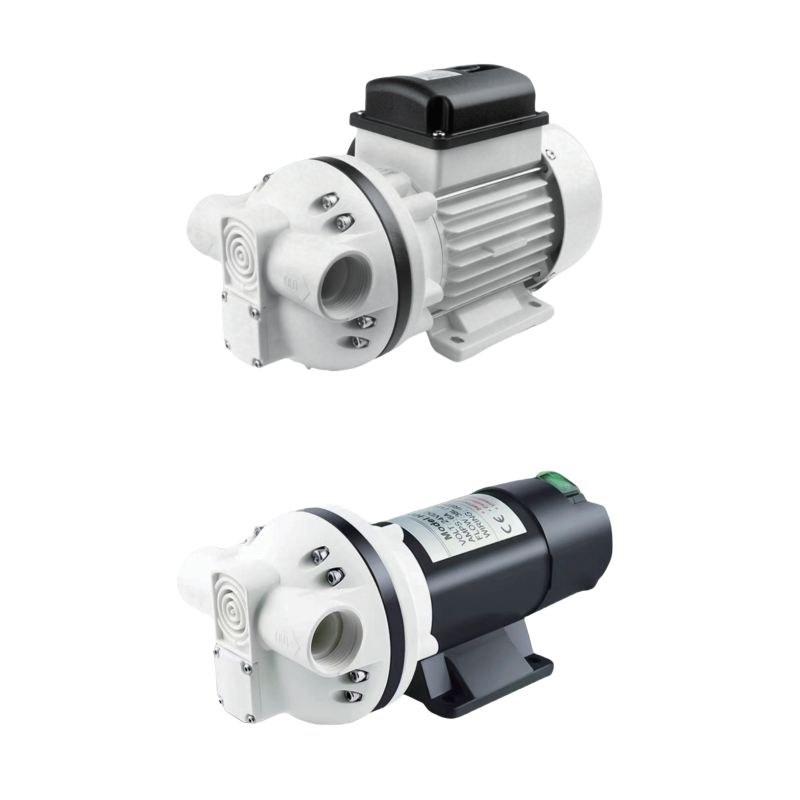
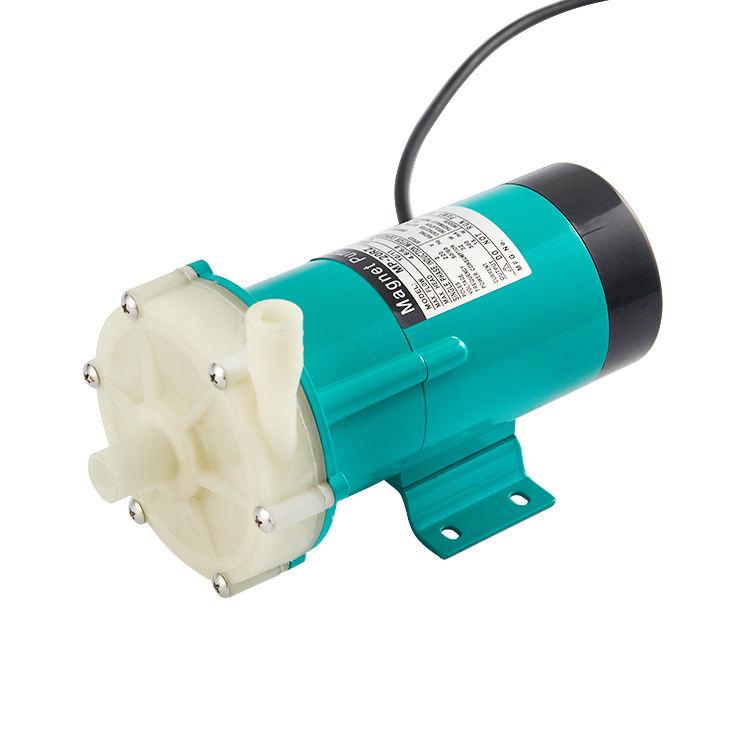
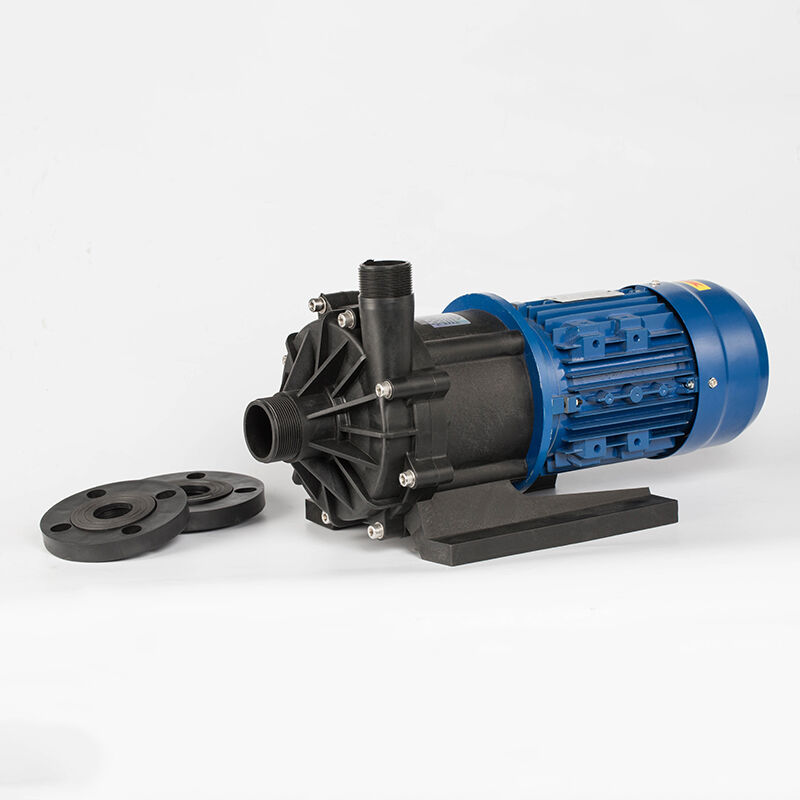
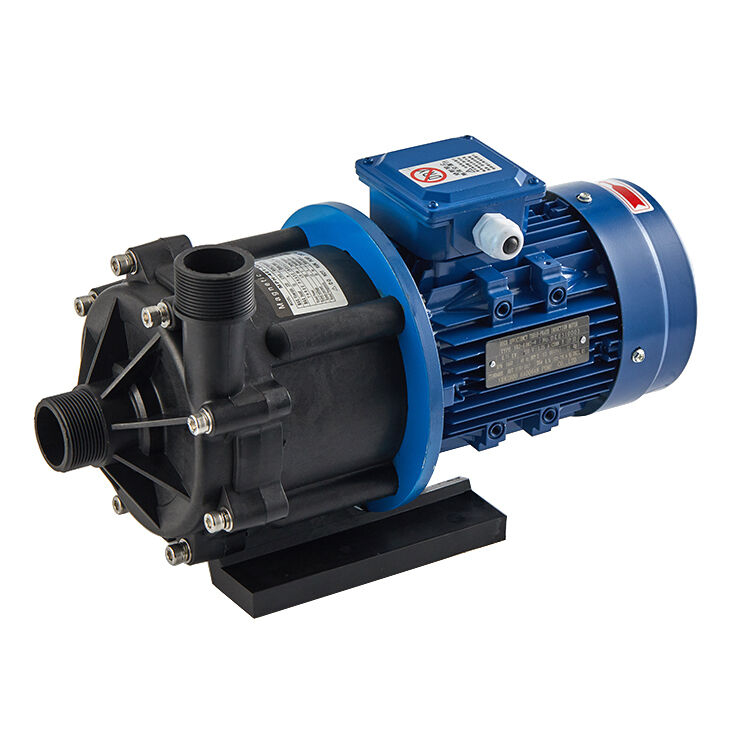
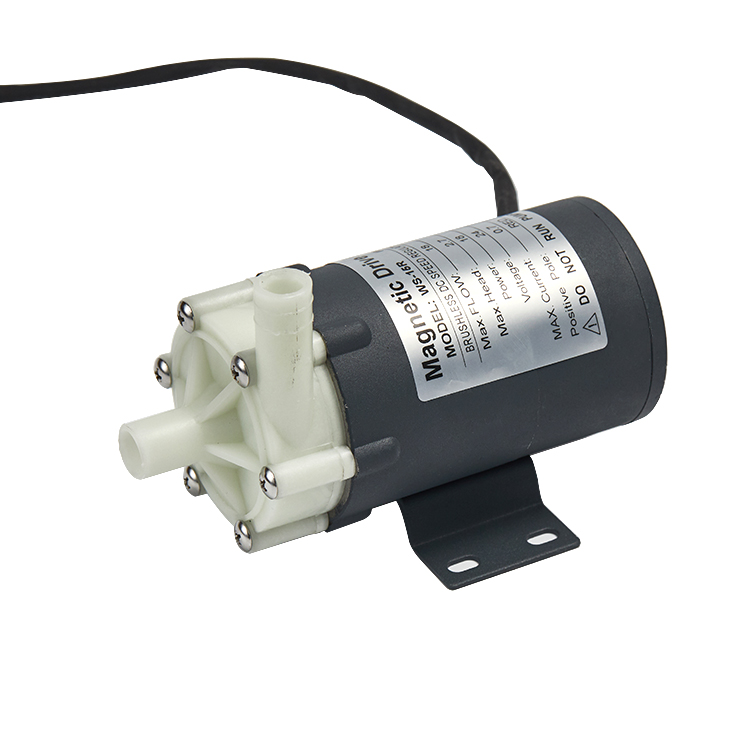
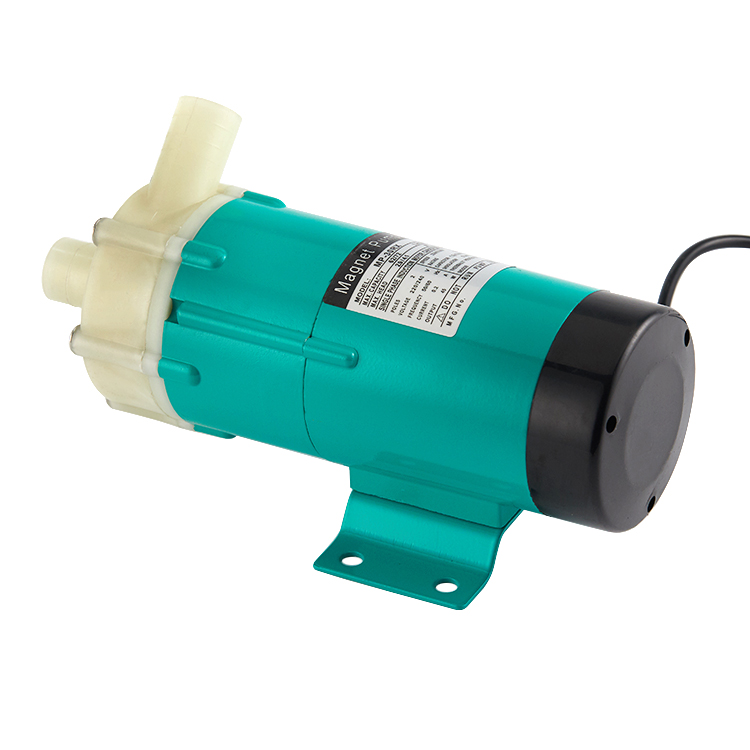
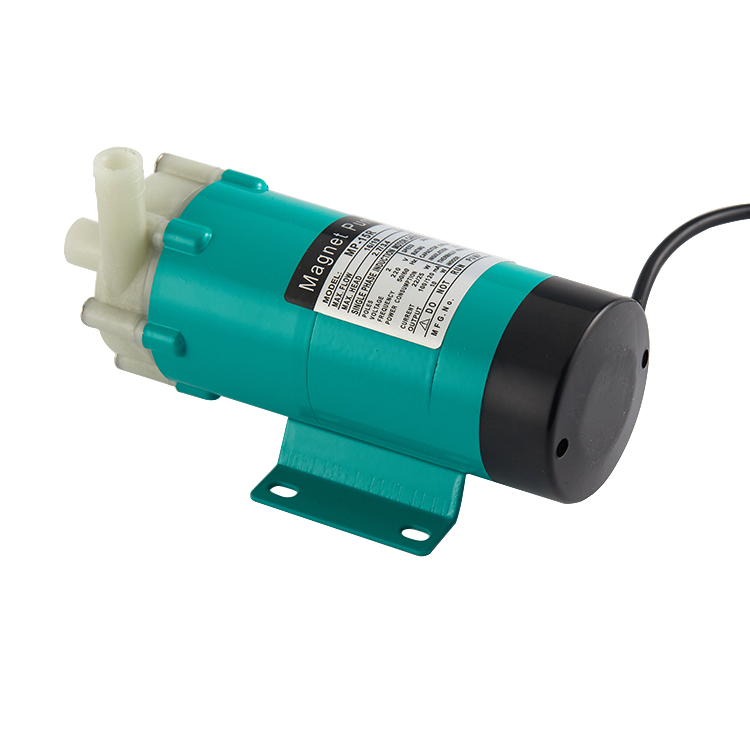
An acid pump manufacturer specializes in designing and producing sophisticated pumping systems engineered to handle corrosive chemical solutions safely and efficiently. These industrial devices represent a critical component in numerous chemical processing operations, where standard pumps would fail due to material degradation.
The primary function of an acid pump manufacturer's products involves transferring acidic fluids from one location to another while maintaining system integrity and preventing leakage. Acid pump manufacturer systems utilize specialized materials such as polypropylene, fluoropolymers, and stainless steel alloys to resist chemical corrosion and extend operational longevity.
Technologically, modern acid pump designs incorporate advanced sealing mechanisms, precision-engineered impellers, and variable speed drives for optimal performance. An acid pump manufacturer develops solutions featuring enhanced suction capabilities, reduced maintenance requirements, and improved energy efficiency compared to conventional alternatives.
Applications for acid pump systems span across diverse industries including chemical manufacturing, pharmaceutical production, metal processing, water treatment facilities, and petroleum refining. The acid pump manufacturer category addresses specific challenges in battery acid handling, sulfuric acid transfer, hydrochloric acid pumping, and nitric acid circulation.
These pumps operate under demanding conditions, requiring robust construction and reliable performance. An acid pump manufacturer delivers equipment capable of handling temperatures ranging from ambient to elevated levels while maintaining chemical compatibility. Industrial clients depend on acid pump manufacturer expertise to ensure continuous operations and workplace safety standards compliance.

 EN