muriatic acid pump
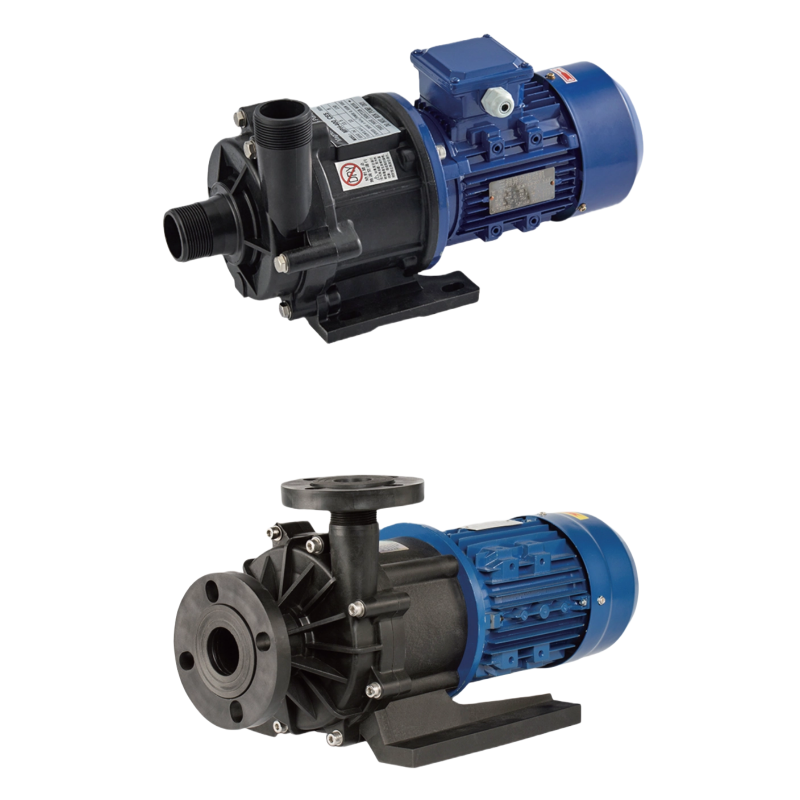
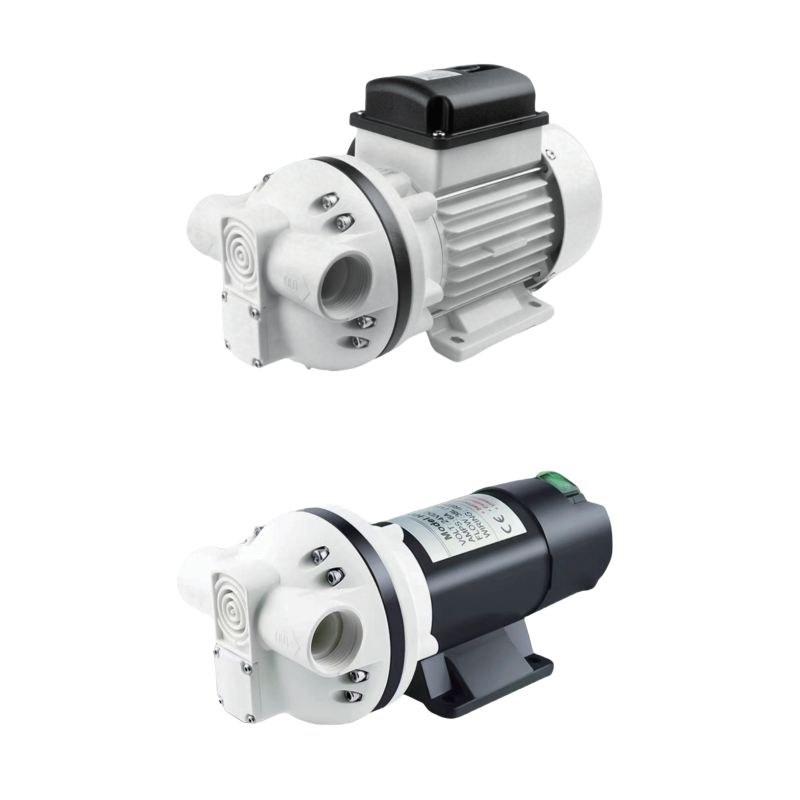
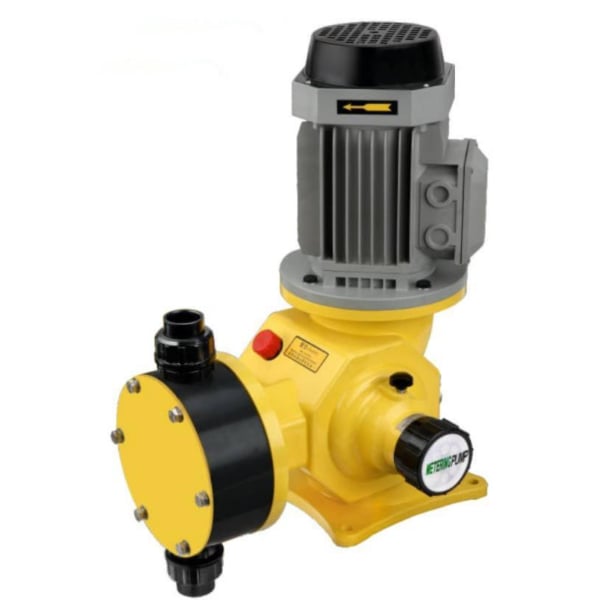
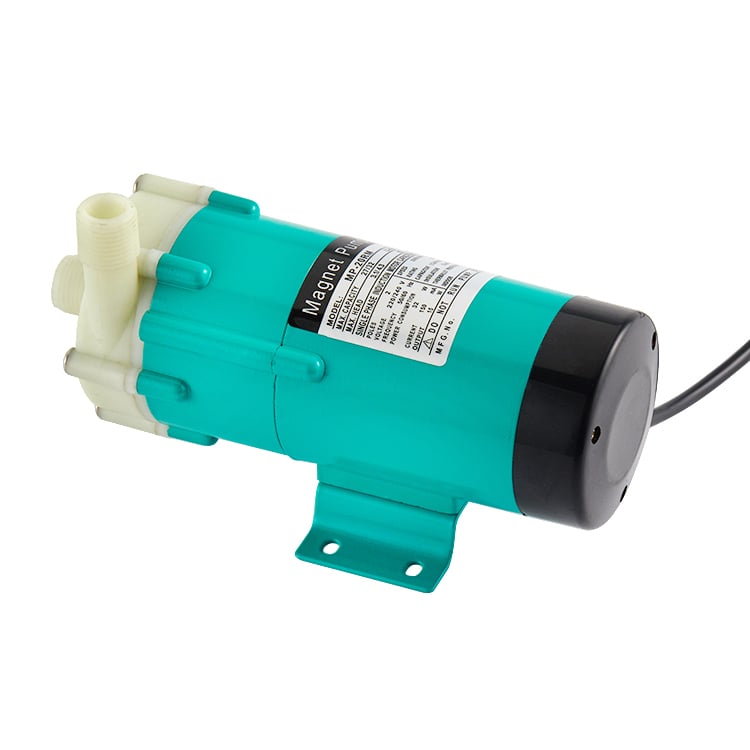
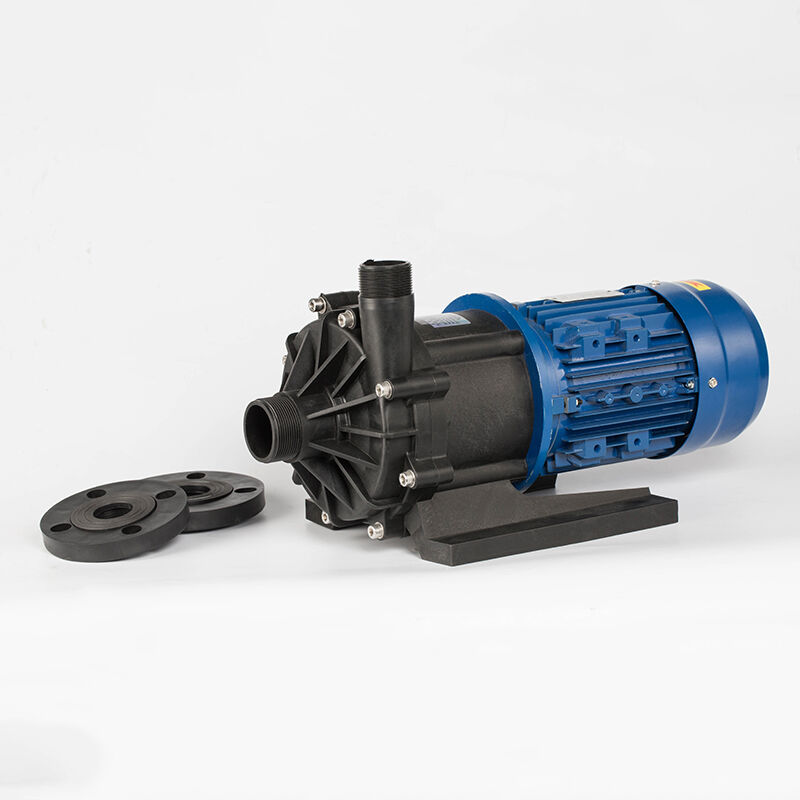
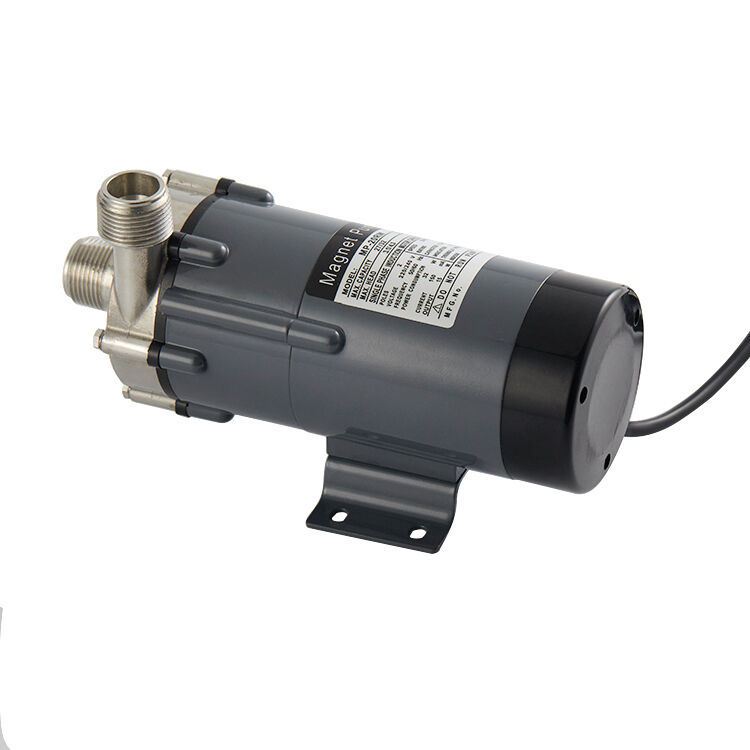
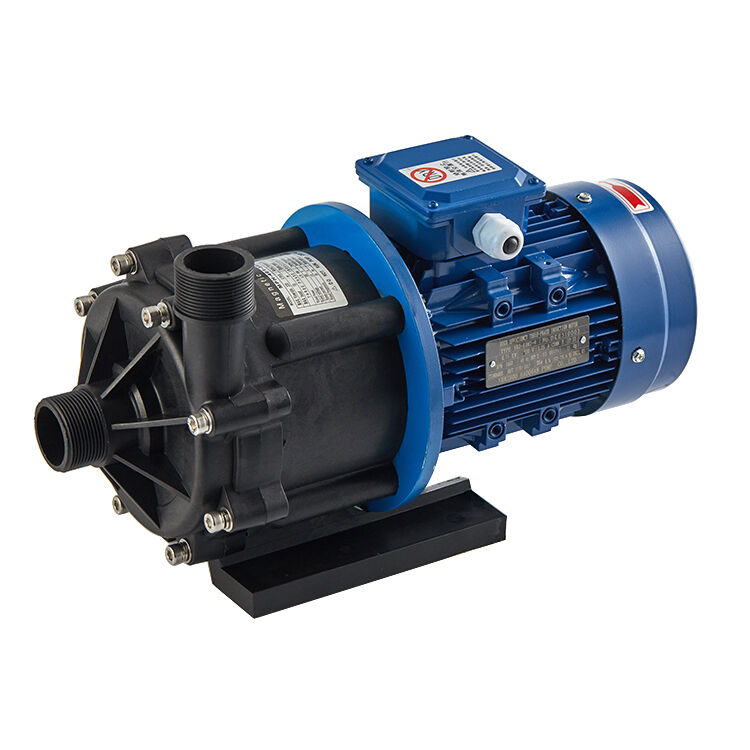
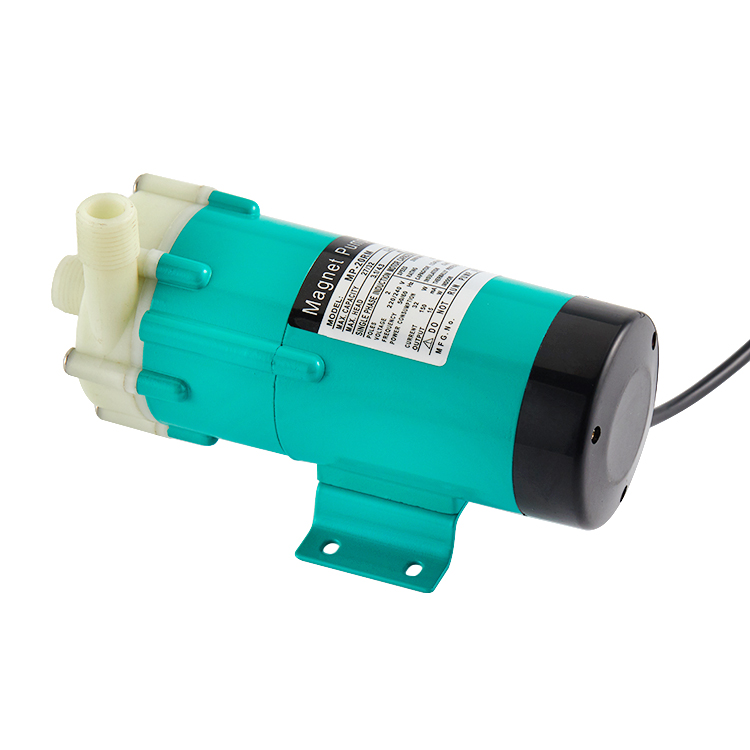
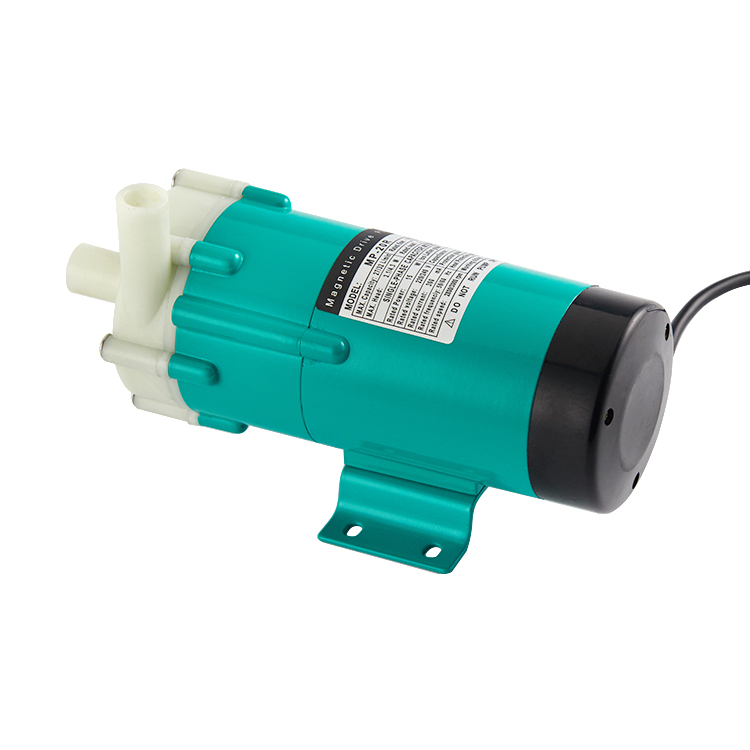
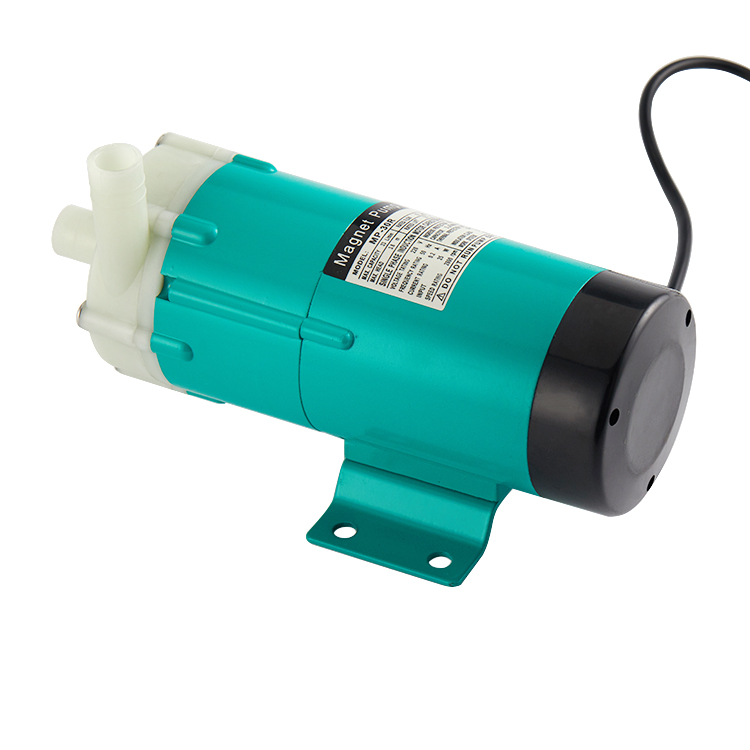
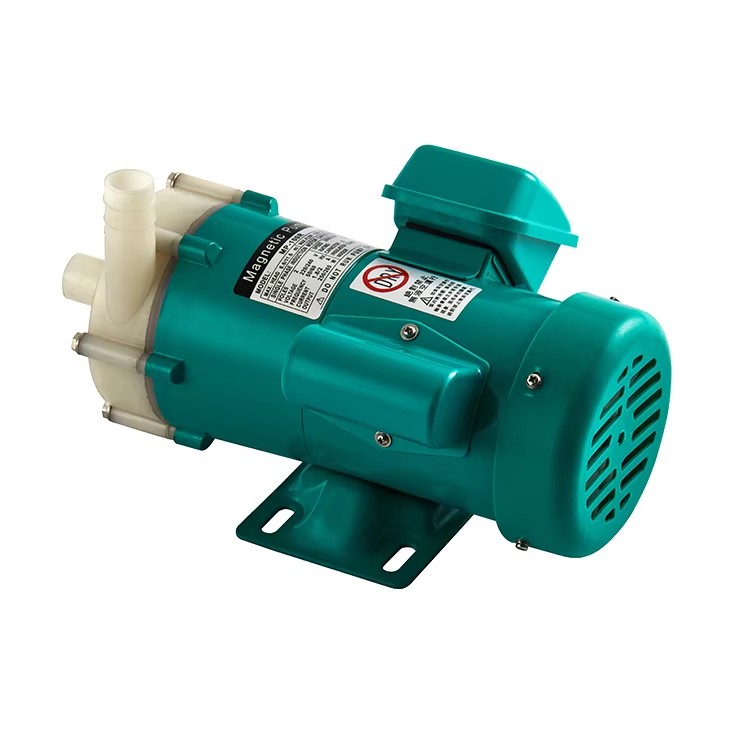
A muriatic acid pump is a specialized chemical handling device designed to safely transfer and dispense hydrochloric acid solutions across industrial and commercial applications. This muriatic acid pump operates with precision engineering to manage corrosive liquids while maintaining operational safety and efficiency. The muriatic acid pump features heavy-duty construction with corrosion-resistant materials that withstand the harsh chemical environment of muriatic acid. These pumps incorporate advanced sealing mechanisms and specialized valves that prevent leakage and ensure reliable performance during extended operations. The muriatic acid pump technology includes variable flow rates and pressure adjustments, allowing operators to customize delivery according to specific application requirements. Key technological features of a muriatic acid pump include acid-resistant wetted parts, reinforced housing, and ergonomic control interfaces. Applications for the muriatic acid pump span multiple industries, including pool maintenance, metal processing, construction cleaning, and industrial chemical production. The muriatic acid pump serves critical roles in descaling operations, pH adjustment, and chemical synthesis processes. By utilizing a muriatic acid pump, facilities can achieve consistent chemical distribution while minimizing worker exposure to hazardous substances. The design of modern muriatic acid pumps prioritizes both performance and safety compliance with industry standards. Whether for routine maintenance or large-scale industrial operations, the muriatic acid pump represents an essential investment in reliable chemical handling infrastructure.

 EN