Stainless Steel Food Grade Pump Head

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

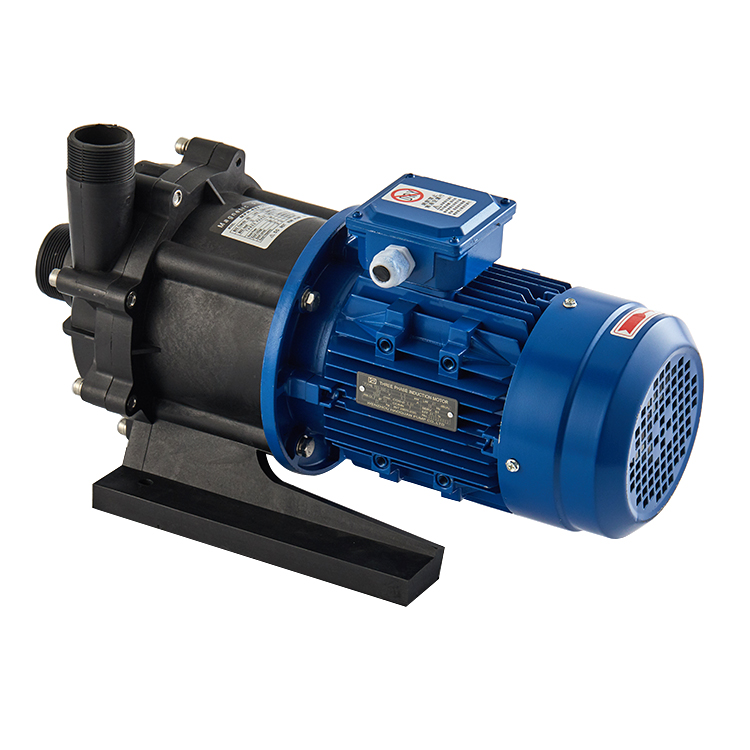
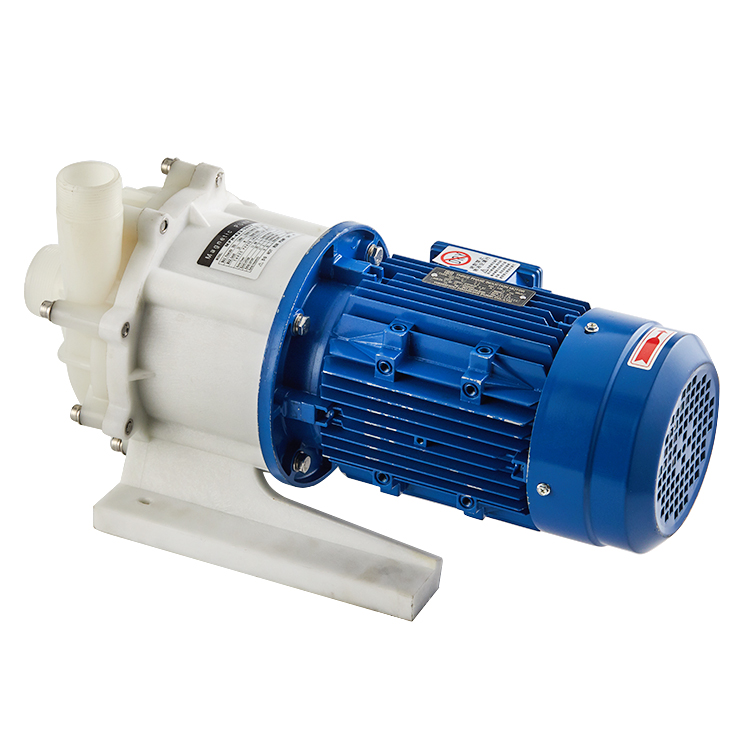
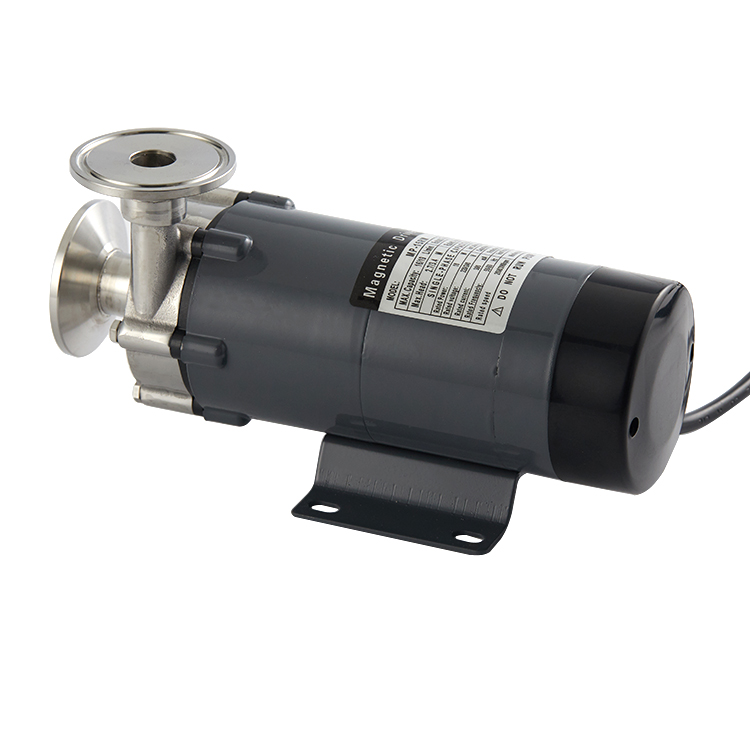
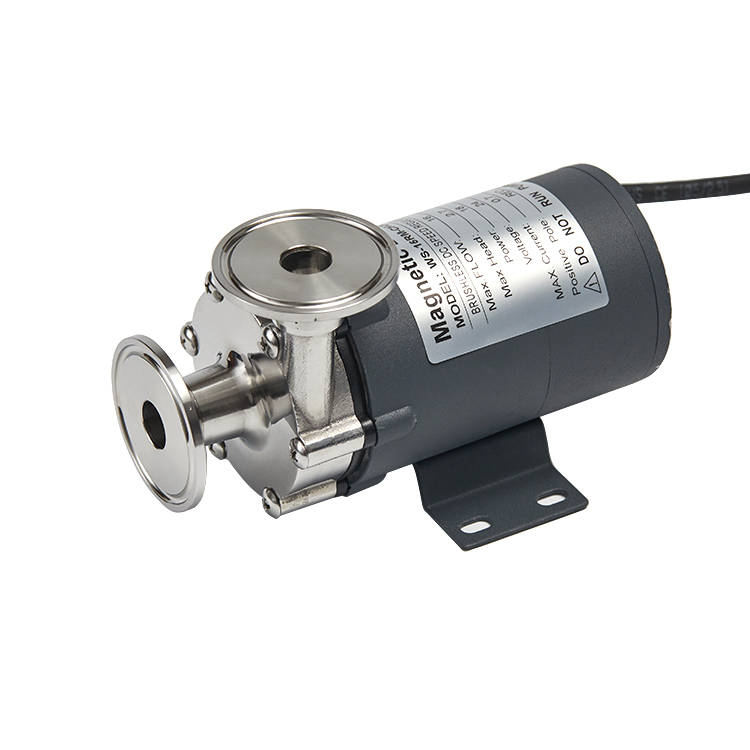
food grade pump with stainless steel head

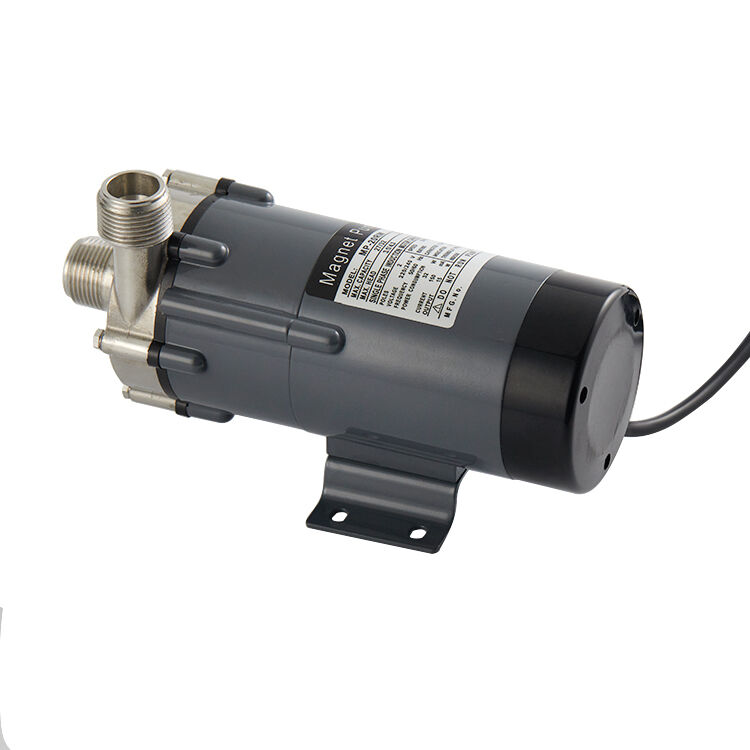
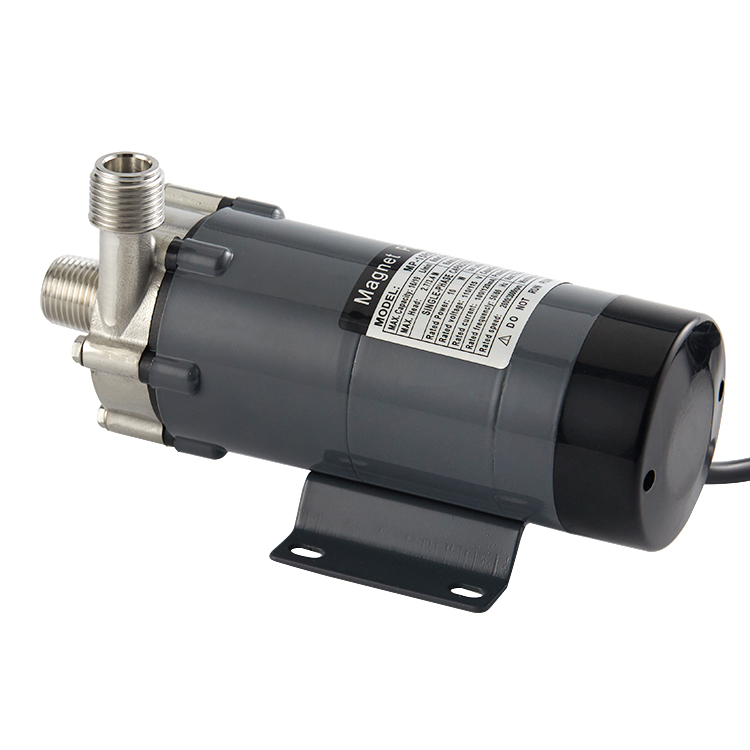
A food grade pump with stainless steel head represents a specialized solution for industries requiring hygienic fluid transfer without contamination risks. This equipment combines advanced engineering with food-safe materials to ensure compliance with stringent health and safety standards. The food grade pump with stainless steel head delivers reliable performance across beverage production, dairy processing, sauce manufacturing, and pharmaceutical applications where product purity remains paramount. The stainless steel head component serves as the critical interface between the pump mechanism and transferred liquids. This construction eliminates corrosion risks and prevents metal particulates from contaminating sensitive products. The food grade pump with stainless steel head maintains its structural integrity across extended operational periods while withstanding frequent sanitation procedures essential in food processing environments. Technologically, these pumps incorporate precision-engineered impellers and carefully designed flow paths that minimize turbulence and product degradation. The food grade pump with stainless steel head operates efficiently across varying viscosity levels, from thin juices to thick pastes, making it adaptable to diverse production requirements. Seal configurations meet food industry certifications, ensuring zero product leakage that could compromise sterility. The robust construction supports continuous operation while maintaining consistent flow rates and pressure outputs, delivering dependable performance for demanding food manufacturing operations requiring uncompromised quality standards.

Popular Products

Choosing a food grade pump with stainless steel head delivers significant operational and business benefits for food processing facilities. The primary advantage lies in contamination prevention: stainless steel construction eliminates rust and corrosion, ensuring your products remain pure and safe throughout transfer operations. Unlike conventional pumps, the food grade pump with stainless steel head requires no protective coatings that might degrade or chip away, creating a genuinely clean transfer solution.

Operational efficiency represents another compelling benefit. The food grade pump with stainless steel head maintains consistent performance across extended production runs without performance degradation. Facility managers appreciate reduced downtime since stainless steel components resist wear from frequent cleaning and sanitization procedures that food plants conduct daily. This translates directly to higher productivity and lower maintenance costs compared to alternative pumping solutions. Decision-making becomes easier when considering regulatory compliance. The food grade pump with stainless steel head automatically satisfies FDA regulations and international food safety standards, eliminating compliance uncertainty. Your facility gains immediate certification readiness without purchasing additional equipment or modifications.

For application suitability, this pump excels across diverse food scenarios: thick sauces, yogurt, chocolate, vegetable oils, and dairy products all benefit from its gentle handling characteristics. The food grade pump with stainless steel head prevents product separation and maintains texture integrity that customers expect. Temperature flexibility allows cold product transfer and heated liquid management without component failure. Investment in a food grade pump with stainless steel head reduces long-term ownership costs through extended service life, minimal component replacement, and energy-efficient operation, making it the smart choice for profit-conscious food manufacturers.

Practical Tips

2026 BLDC Pump Guide: Top Models and Features

09

Jun

2026 BLDC Pump Guide: Top Models and Features

The bldc pump has emerged as one of the most technically advanced fluid-handling solutions available to engineers and procurement professionals entering 2026. Driven by brushless direct current motor technology, these pumps deliver a compelling combi...
View More
A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

09

Jun

A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

Introduction For international B2B buyers, selecting a pump supplier in China is a critical decision that impacts long-term operational costs and product reliability. While high-quality marketing materials and competitive pricing are common, they do ...
View More
Shipping and Logistics Guide: Importing Large Volume Industrial Pumps from Wenzhou

09

Jun

Shipping and Logistics Guide: Importing Large Volume Industrial Pumps from Wenzhou

Introduction: Navigating the Logistics of Wenzhou’s Pump Industry Wenzhou, located in the Zhejiang province of China, is globally recognized as the "Capital of Pumps and Valves." For international B2B buyers, sourcing industrial pumps from Wenz...
View More
Environmental Regulations and Pump Compliance: Navigating CE, RoHS, and Beyond

09

Jun

Environmental Regulations and Pump Compliance: Navigating CE, RoHS, and Beyond

Introduction: The Complexity of Global Compliance In the modern B2B marketplace, manufacturing excellence is only half the battle. The other half is compliance. For industrial pump users and distributors, navigating the maze of international regulati...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade pump with stainless steel head

Superior Contamination Control with Stainless Steel Construction

Superior Contamination Control with Stainless Steel Construction

The food grade pump with stainless steel head eliminates contamination risks that plague conventional pumping systems. Stainless steel naturally resists corrosion, preventing rust particles from entering your product stream and compromising quality or customer safety. This material choice ensures your food products remain pure throughout every transfer cycle, maintaining the integrity that consumers and regulatory bodies demand. Unlike painted or coated alternatives, the food grade pump with stainless steel head requires no protective layers that eventually wear away, exposing underlying materials to moisture and degradation. The smooth stainless steel surfaces resist bacterial attachment and biofilm formation, supporting your sanitation protocols. Food manufacturers gain complete confidence that their products meet the highest purity standards throughout production. The food grade pump with stainless steel head provides peace of mind knowing contamination sources have been engineered out of the system entirely.
Compliance and Certification Readiness

Compliance and Certification Readiness

Installing a food grade pump with stainless steel head immediately addresses regulatory requirements without additional modifications or upgrades. These pumps meet FDA food contact surface requirements, NSF certification standards, and international food safety regulations across multiple markets. Your facility gains automatic compliance readiness, eliminating expensive retrofitting or system replacements. The food grade pump with stainless steel head documentation and certification reduce administrative burden when regulators conduct facility inspections. Stainless steel components align with HACCP principles and preventive food safety measures that modern plants must implement. Unlike equipment requiring special approvals or provisional compliance, the food grade pump with stainless steel head represents a proven solution recognized across the industry. Investment in this equipment protects your facility's reputation and operational license, ensuring you remain compliant regardless of evolving food safety regulations. This compliance certainty allows management to focus resources on production optimization rather than regulatory uncertainty.
Enhanced Durability and Reduced Maintenance Costs

Enhanced Durability and Reduced Maintenance Costs

The food grade pump with stainless steel head delivers exceptional durability that extends equipment lifespan significantly beyond conventional alternatives. Stainless steel resists damage from intensive daily sanitation procedures, chemical cleaning agents, and temperature fluctuations that typically degrade standard materials. Your maintenance budget decreases substantially because the food grade pump with stainless steel head requires fewer component replacements and repairs. Extended service intervals reduce production interruptions and associated downtime costs. The corrosion resistance means stainless steel components outlast painted or rubber-coated alternatives by years, improving return on investment. Facility managers appreciate predictable operating costs since the food grade pump with stainless steel head maintains consistent performance across its operational life. Replacement schedules become more economical because major components rarely fail prematurely. The food grade pump with stainless steel head represents a long-term value investment that compounds savings over multiple production seasons.
Stainless Steel Food Grade Pump Head

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000