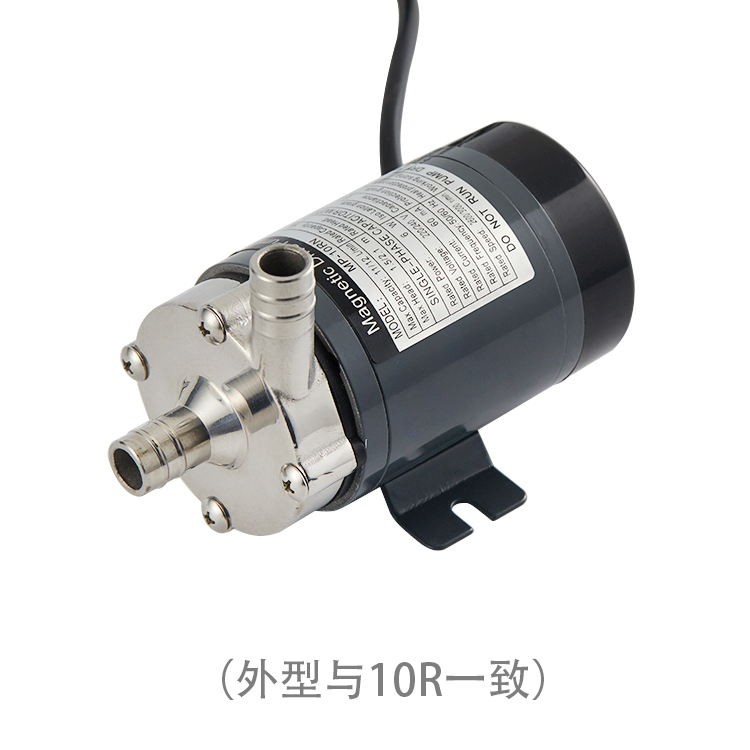
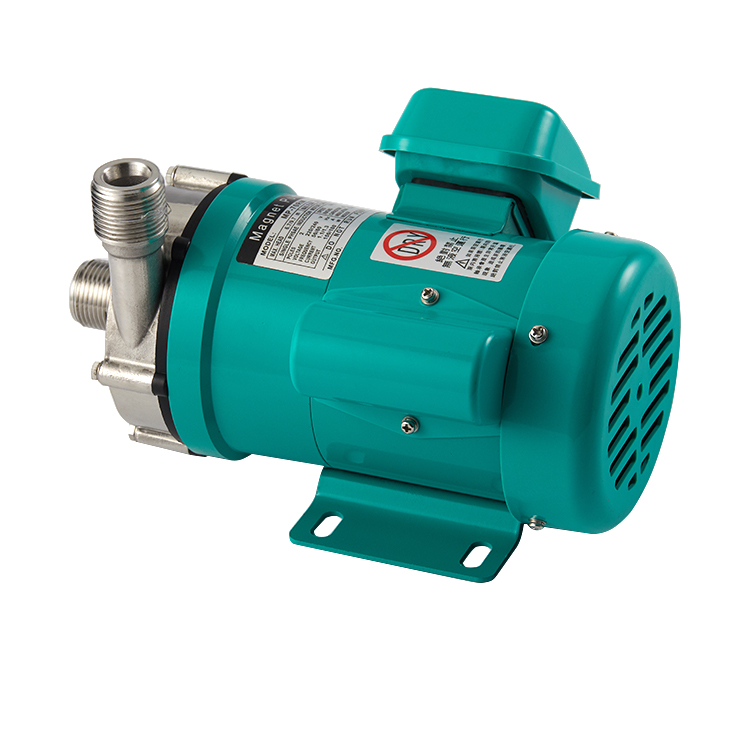
Food Grade Pump Manufacturer Solutions

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade pump manufacturer

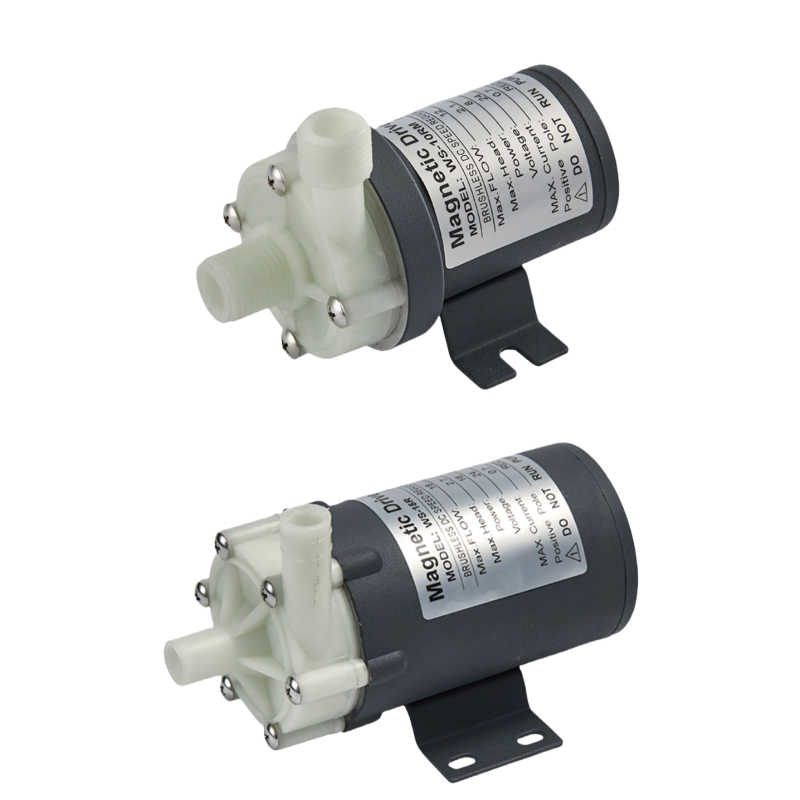
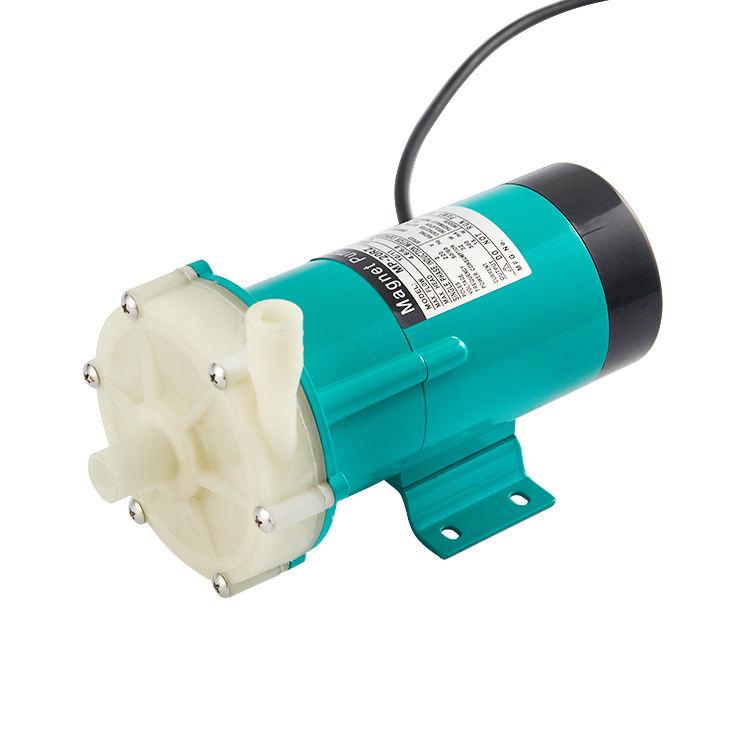
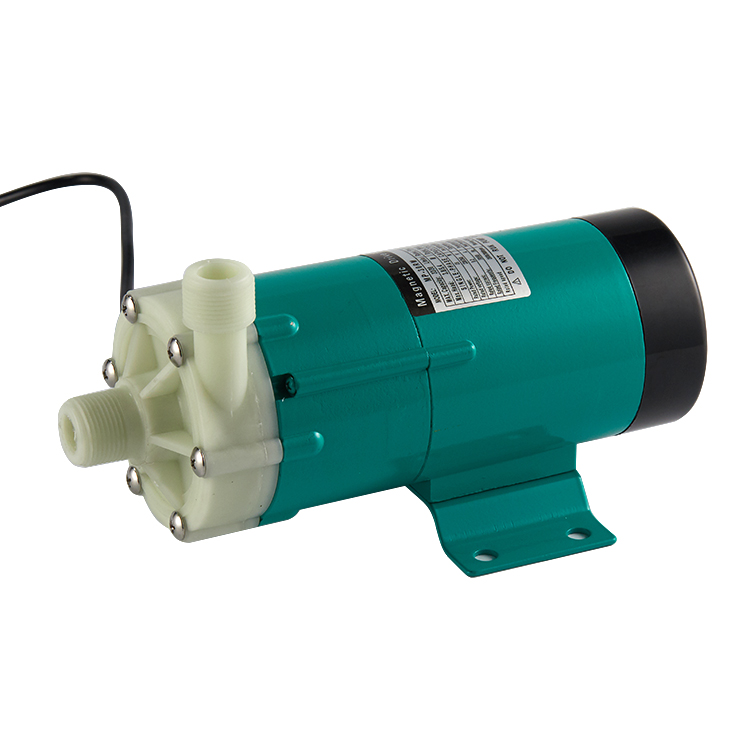
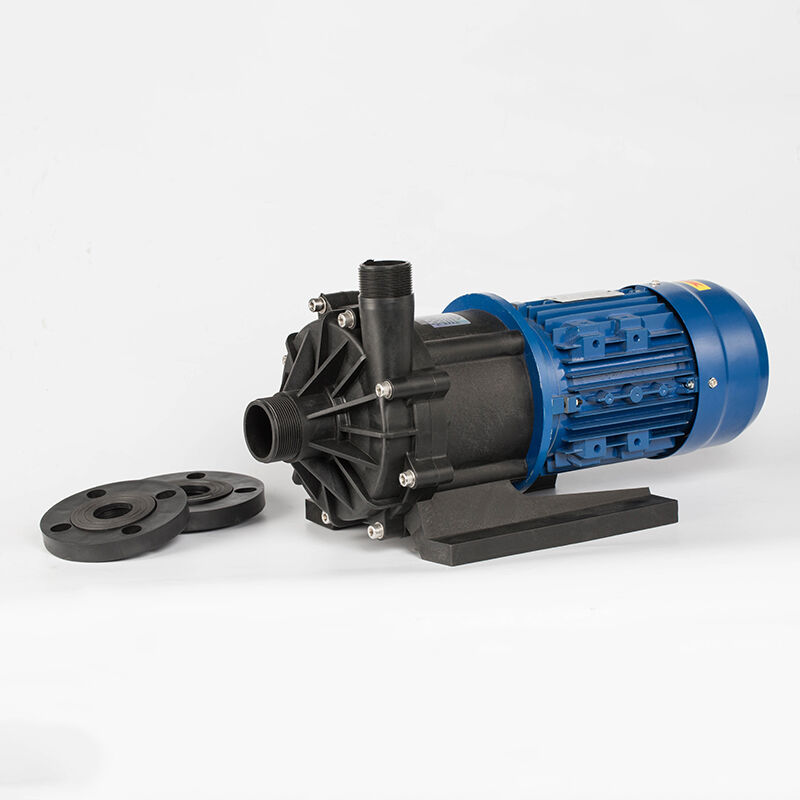
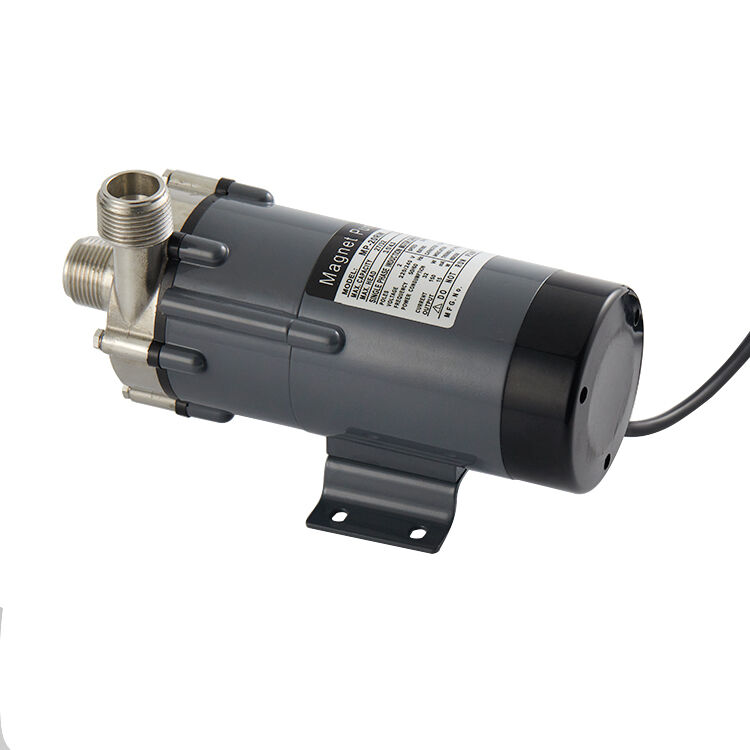
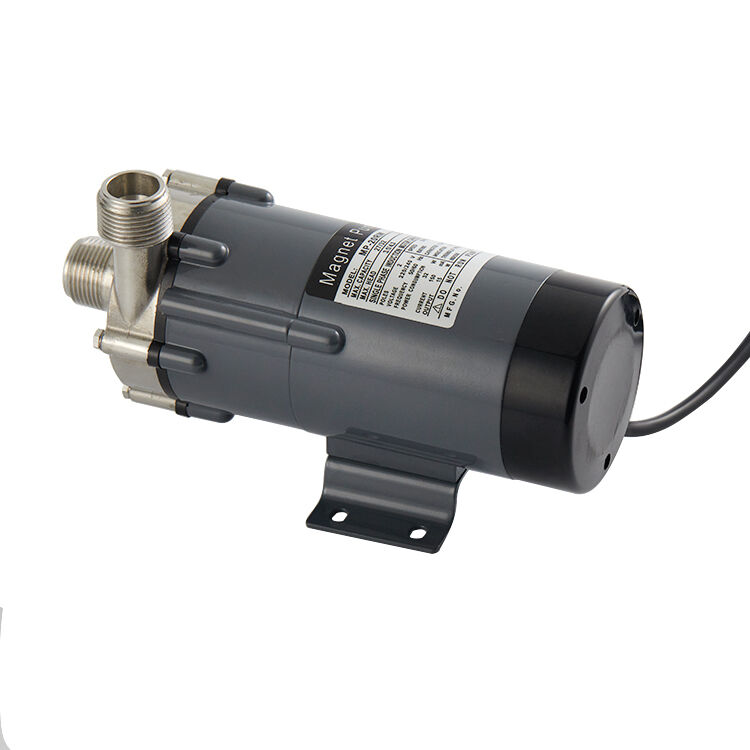
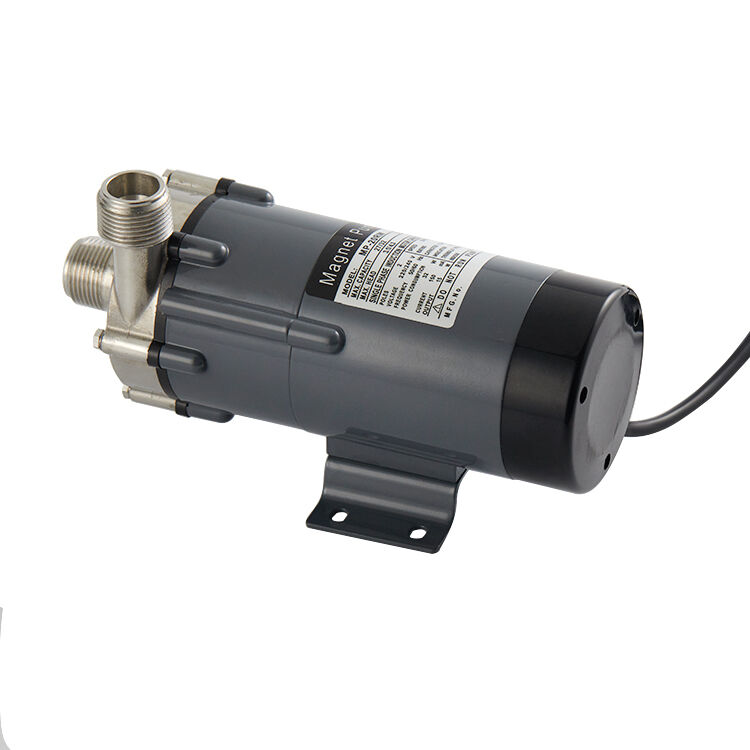
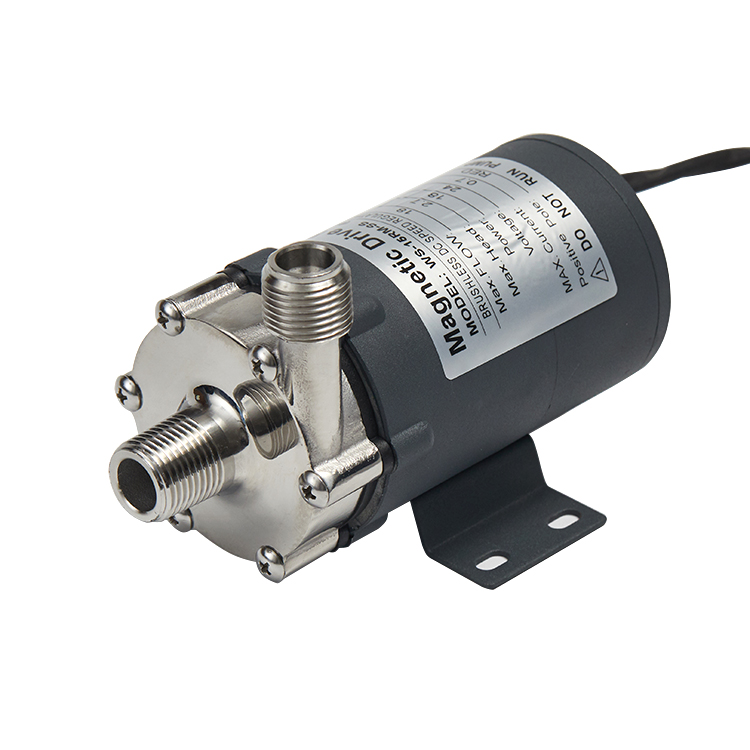
A food grade pump manufacturer specializes in designing and producing pumps that meet strict food safety and sanitation standards required across the food and beverage industry. These pumps are engineered to handle sensitive food products while maintaining product integrity and preventing contamination. The food grade pump manufacturer creates solutions that comply with FDA regulations, USDA standards, and international food safety certifications. Functionally, food grade pumps transfer, mix, and dosage food products ranging from liquids to viscous substances without compromising quality. The food grade pump manufacturer incorporates advanced technologies such as self-priming capabilities, gentle product handling, and minimal product residue design. These pumps feature sanitary construction with tool-free disassembly for quick cleaning and maintenance, eliminating product buildup in hard-to-reach areas. Technological features include hygienic designs with smooth surfaces, stainless steel components, and polished interiors that prevent bacterial growth. The food grade pump manufacturer integrates variable speed controls, precise flow rate monitoring, and compatibility with CIP (Clean-In-Place) systems for automated sanitation. Applications span diverse sectors including dairy processing, beverage production, sauce manufacturing, pharmaceutical operations, and cosmetic production. The food grade pump manufacturer serves producers requiring reliable equipment that ensures product safety, extends shelf life, and maintains nutritional value. Whether processing milk, juice, honey, or specialized food additives, these pumps deliver consistent performance while adhering to the most rigorous food safety requirements in the industry.

New Products

Choosing a food grade pump manufacturer offers substantial practical benefits that directly impact production efficiency and product quality. These pumps eliminate contamination risks through sanitary design principles, ensuring your food products remain safe for consumer consumption. The food grade pump manufacturer provides equipment with surfaces that meet rigorous hygiene standards, reducing bacterial contamination and supporting compliance with regulatory agencies.

Operationally, these pumps minimize maintenance downtime through self-priming features and quick-disconnect components. You can disassemble and clean equipment in minutes without specialized tools, allowing rapid changeovers between different products. The food grade pump manufacturer designs systems that reduce waste by efficiently handling expensive food ingredients with minimal product loss during transfer. Cost-effectiveness emerges from reliable performance that reduces unexpected breakdowns and replacement expenses. These pumps operate at lower energy consumption levels compared to industrial alternatives, directly lowering operational costs while maintaining consistent production rates. The food grade pump manufacturer ensures your equipment delivers years of dependable service with minimal repair needs.

Product quality improvement represents another key advantage. Gentle pumping action preserves delicate food characteristics including flavor profiles, texture, and nutritional content. The food grade pump manufacturer creates solutions preventing foam generation and product separation during processing. Application suitability matters significantly. Whether processing cold products, hot liquids, or temperature-sensitive ingredients, the food grade pump manufacturer offers specialized configurations meeting your specific production requirements. Decision-useful context includes compatibility with automated systems, integration capabilities with existing production lines, and scalability for growing operations, making these pumps essential investments for food producers prioritizing quality and safety.

Tips And Tricks

Smart Dosing Systems: Integrating Precision Pumps into Automated Production Lines

09

Jun

Smart Dosing Systems: Integrating Precision Pumps into Automated Production Lines

Introduction: The Evolution of Fluid Handling in Industry 4.0 The Fourth Industrial Revolution, or Industry 4.0, is fundamentally reshaping how factories operate. At the heart of this transformation is the shift from manual, isolated processes to int...
View More
Inside Haoquan’s Quality Inspection System: Ensuring Zero-Defect Pump Manufacturing

09

Jun

Inside Haoquan’s Quality Inspection System: Ensuring Zero-Defect Pump Manufacturing

Introduction In the high-stakes world of industrial fluid management, the reliability of a pump is not just a performance metric—it is a cornerstone of operational safety and economic efficiency. For industries ranging from chemical processing ...
View More
A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

09

Jun

A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

Introduction For international B2B buyers, selecting a pump supplier in China is a critical decision that impacts long-term operational costs and product reliability. While high-quality marketing materials and competitive pricing are common, they do ...
View More
The Value of R&D Innovation in Reducing Total Cost of Ownership (TCO) for Pumps

09

Jun

The Value of R&D Innovation in Reducing Total Cost of Ownership (TCO) for Pumps

Introduction In the B2B procurement process, the initial purchase price of an industrial pump is often just the tip of the iceberg. Smart facility managers and procurement directors know that the true cost of a pump is revealed over its entire lifesp...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade pump manufacturer

Sanitary Design and Food Safety Compliance

Sanitary Design and Food Safety Compliance

The food grade pump manufacturer prioritizes hygiene through comprehensive sanitary design principles meeting FDA, USDA, and international certifications. Each component features smooth, polished surfaces eliminating micro-crevices where bacteria accumulate. Stainless steel construction throughout prevents rust and corrosion while supporting rigorous cleaning protocols. The food grade pump manufacturer ensures all wetted parts meet pharmaceutical-grade standards, protecting your products from contamination sources. Quick-disconnect fittings enable tool-free disassembly for thorough cleaning, while CIP system compatibility automates sanitation procedures. This design philosophy guarantees your food products maintain maximum safety throughout processing operations. Choosing a food grade pump manufacturer with proven sanitary credentials protects consumer health and maintains brand reputation in competitive markets.
Versatile Handling of Diverse Food Products

Versatile Handling of Diverse Food Products

The food grade pump manufacturer creates equipment handling various food products from thin liquids to thick viscous substances without product degradation. Whether processing milk, yogurt, honey, sauces, or juices, these pumps maintain precise flow control preventing foam generation and product separation. Variable speed capabilities allow operators to adjust pumping rates matching specific product characteristics and processing requirements. The food grade pump manufacturer ensures gentle product treatment preserving flavor profiles and nutritional content throughout transfer operations. Equipment compatibility extends to temperature-sensitive ingredients requiring controlled handling conditions. This versatility eliminates the need for multiple specialized pumps, reducing capital equipment investments while increasing operational flexibility. Production teams benefit from streamlined processes using a single food grade pump manufacturer solution handling diverse product lines effectively.
Reduced Operational Costs and Maintenance Efficiency

Reduced Operational Costs and Maintenance Efficiency

The food grade pump manufacturer delivers long-term cost savings through energy-efficient operation and minimized maintenance requirements. Self-priming capabilities eliminate pre-startup procedures, reducing labor time and improving production scheduling. Durable stainless steel construction withstands rigorous sanitation cycles, extending equipment lifespan beyond conventional alternatives. The food grade pump manufacturer designs systems requiring minimal spare parts inventory, lowering ongoing supply chain expenses. Reduced downtime from quick cleanings and tool-free assembly maximizes production hours while decreasing labor costs. Energy consumption levels remain substantially lower than industrial-grade alternatives, reflecting positively on utility budgets. Selecting a food grade pump manufacturer known for reliability minimizes emergency repairs and replacement expenses. These cumulative advantages create compelling financial justification, making food grade pump manufacturer solutions smart investments supporting profitability across food processing operations.
Food Grade Pump Manufacturer Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000