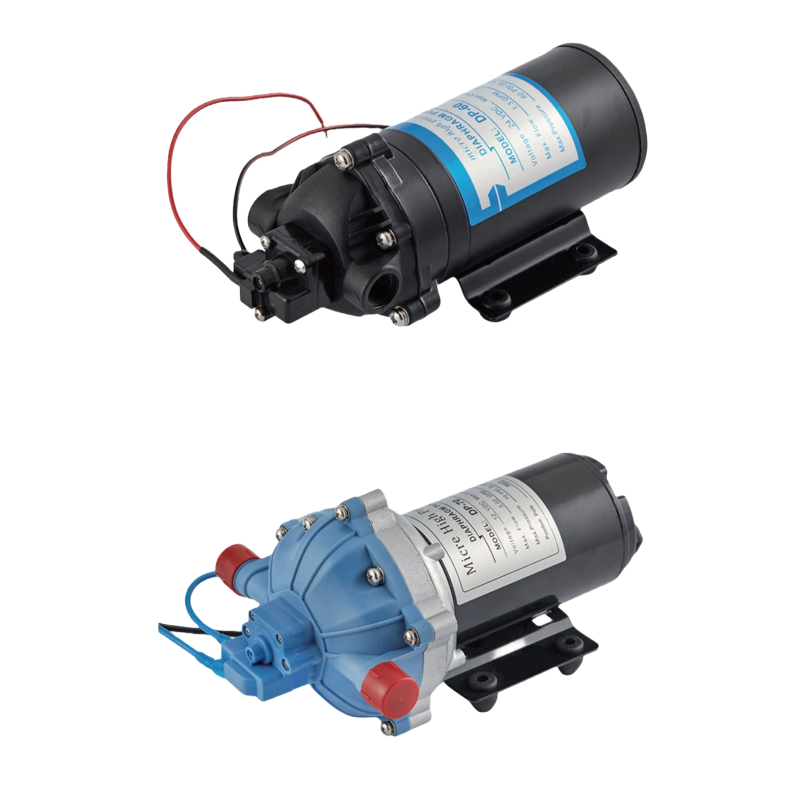
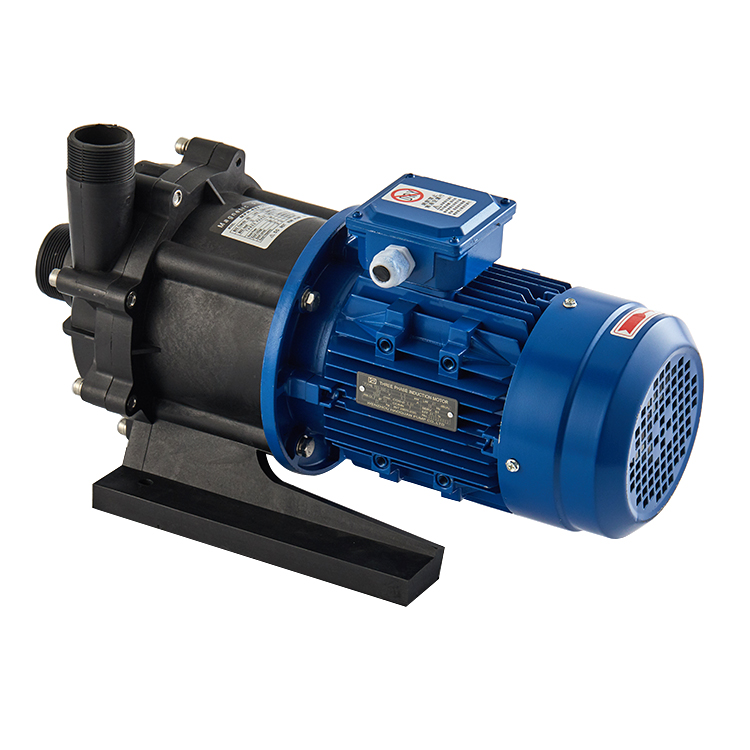
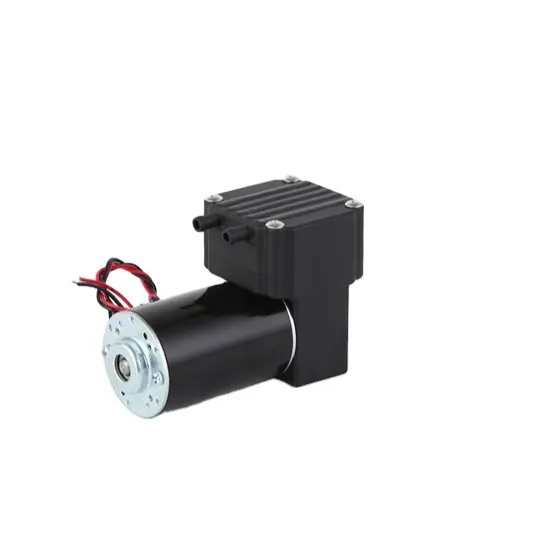
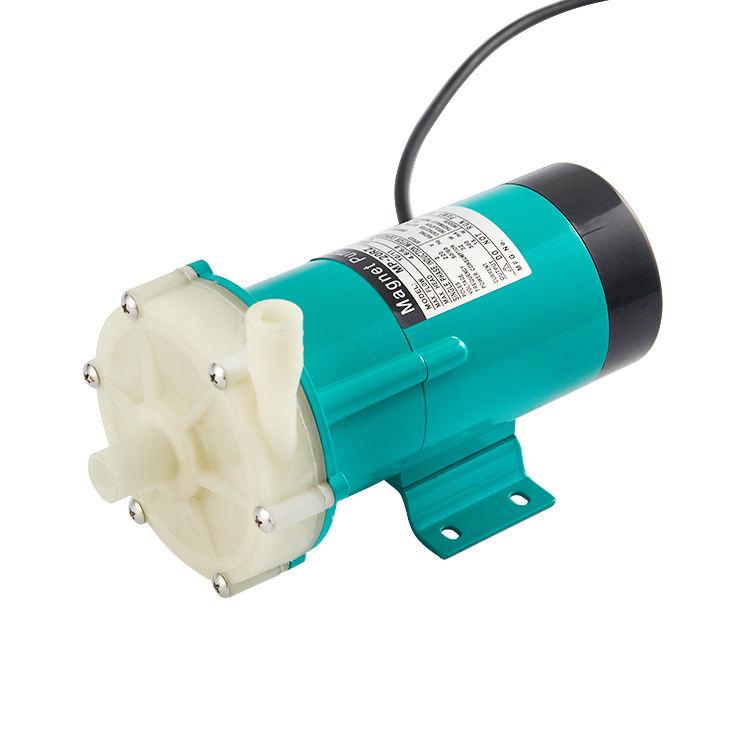
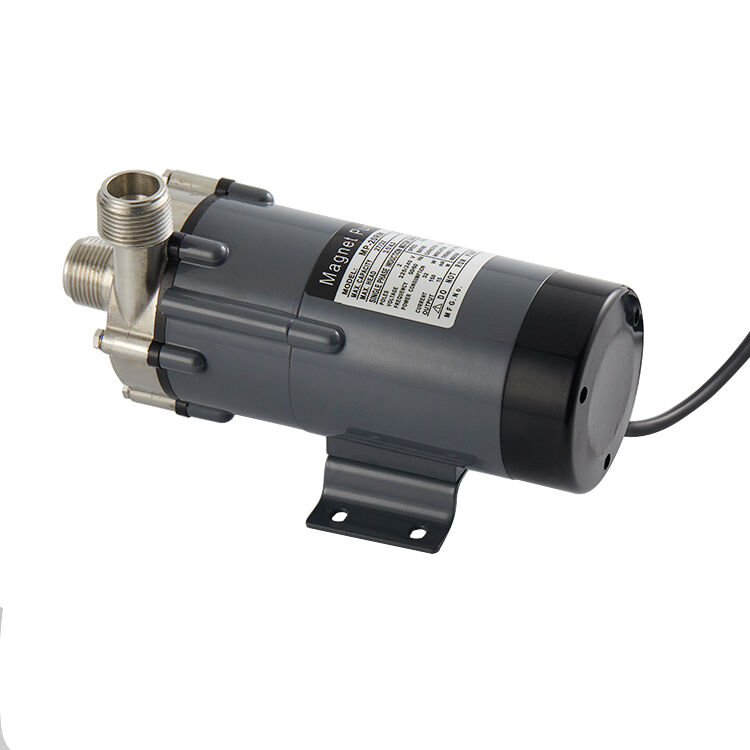
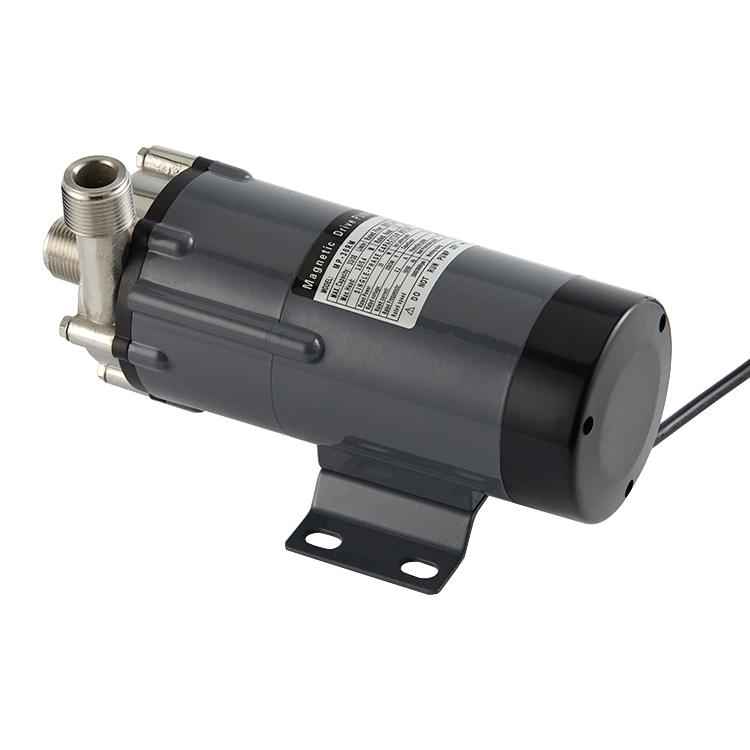
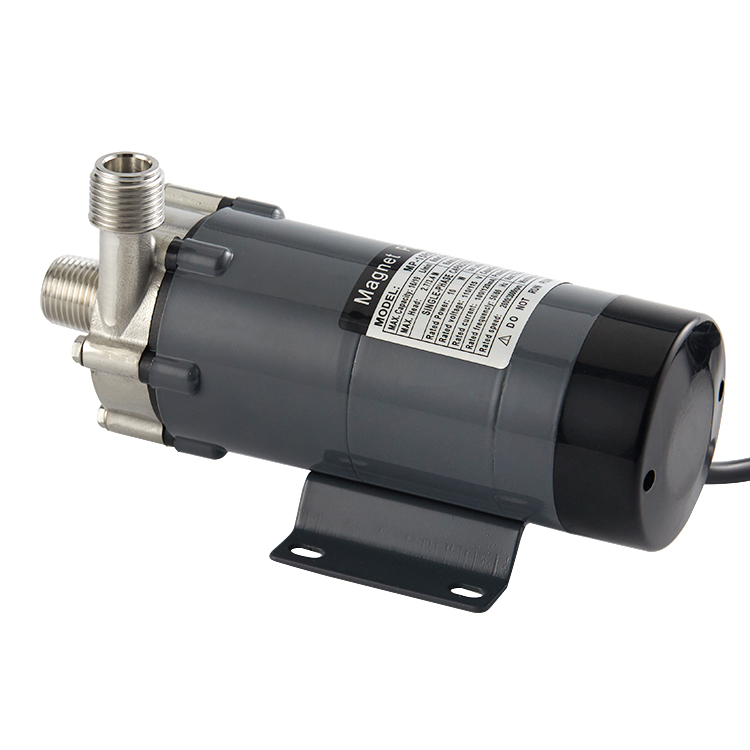
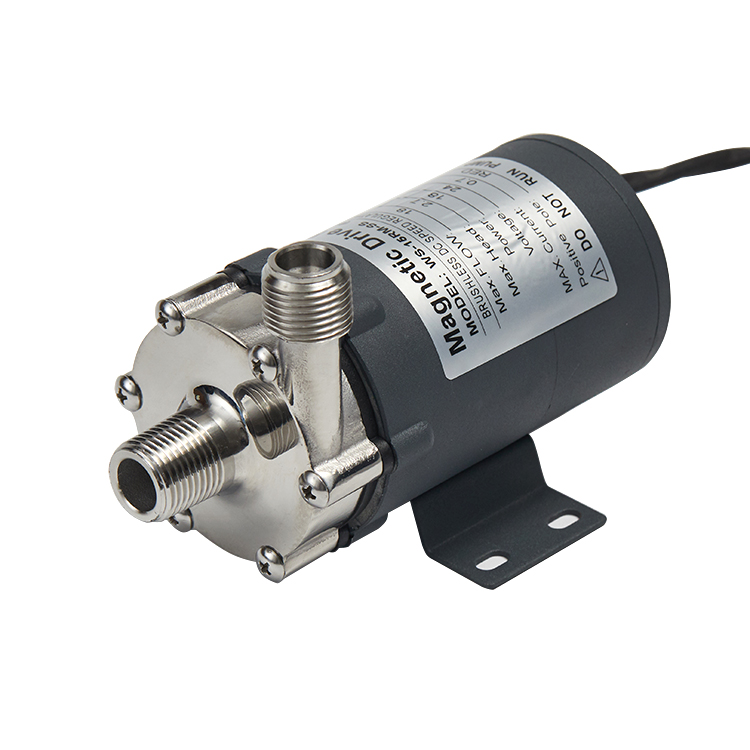
small food grade transfer pump
A small food grade transfer pump is an essential piece of equipment designed to move liquid products safely and efficiently within food processing and beverage production facilities. This compact pump system transfers various food products including oils, sauces, juices, dairy products, and other liquid ingredients while maintaining strict hygiene standards. The small food grade transfer pump operates using gentle pumping mechanisms that protect product integrity and prevent contamination throughout the transfer process.
The technological features of a small food grade transfer pump include stainless steel construction, sanitary design standards, and compatibility with food-safe materials. These pumps meet FDA and USDA regulations, ensuring compliance with industry standards. The small food grade transfer pump typically incorporates sealed bearings and smooth internal surfaces to facilitate easy cleaning and prevent bacterial growth.
Applications for a small food grade transfer pump span across multiple industries. Food manufacturers use these pumps for transferring ingredients between processing stages, while beverage companies rely on them for consistent product movement. The small food grade transfer pump proves invaluable in dairy operations, commercial kitchens, and ingredient distribution centers. Its versatility makes it suitable for both small-scale artisanal producers and larger manufacturing environments. The compact design allows installation in space-limited facilities without compromising performance or safety standards.

 EN