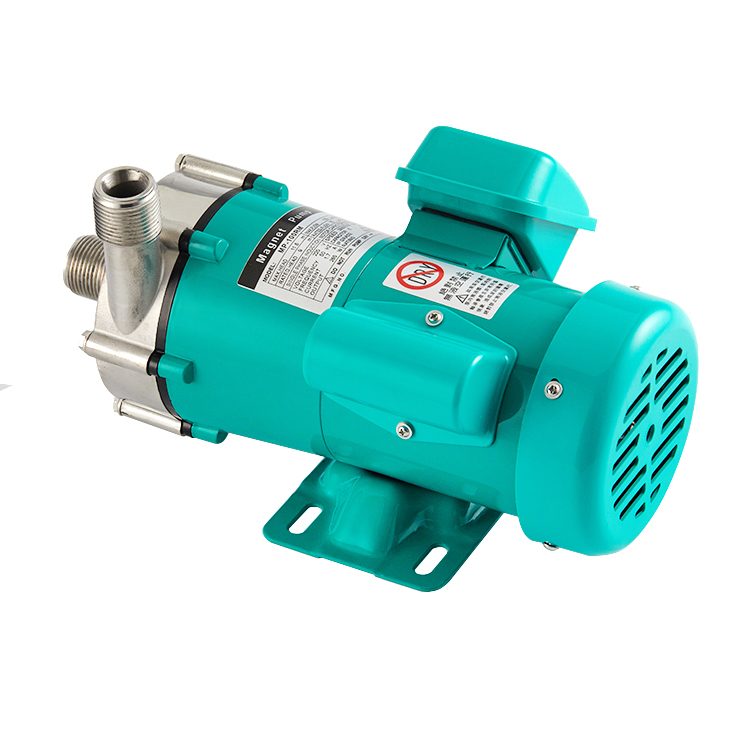
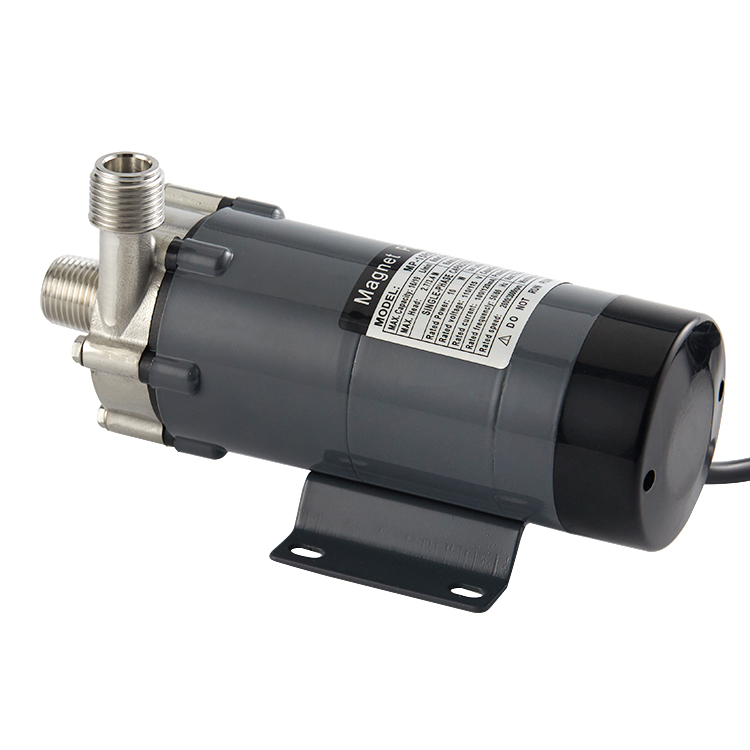
food grade pump exporter
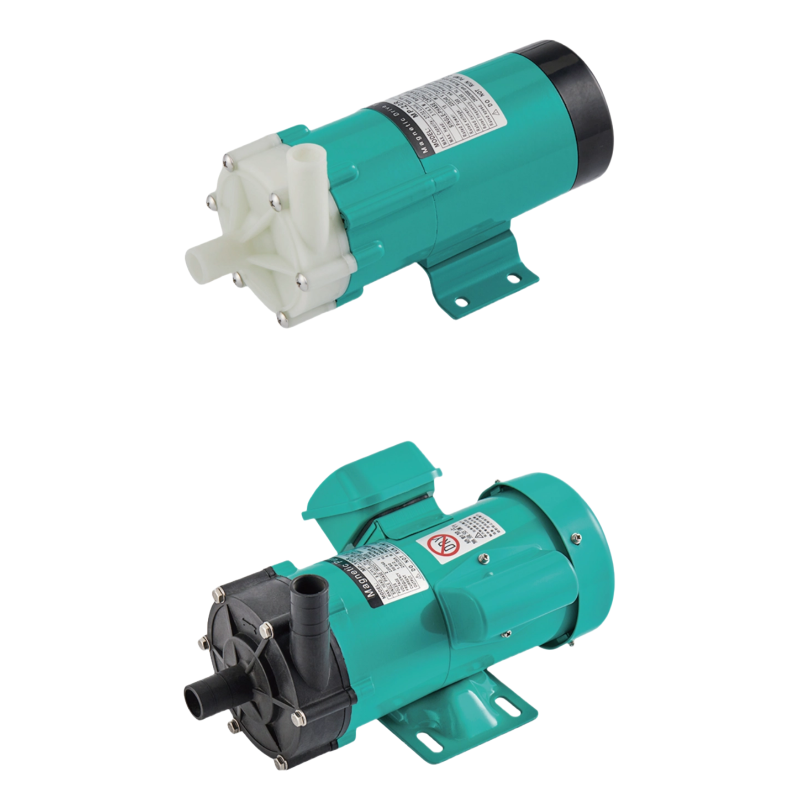
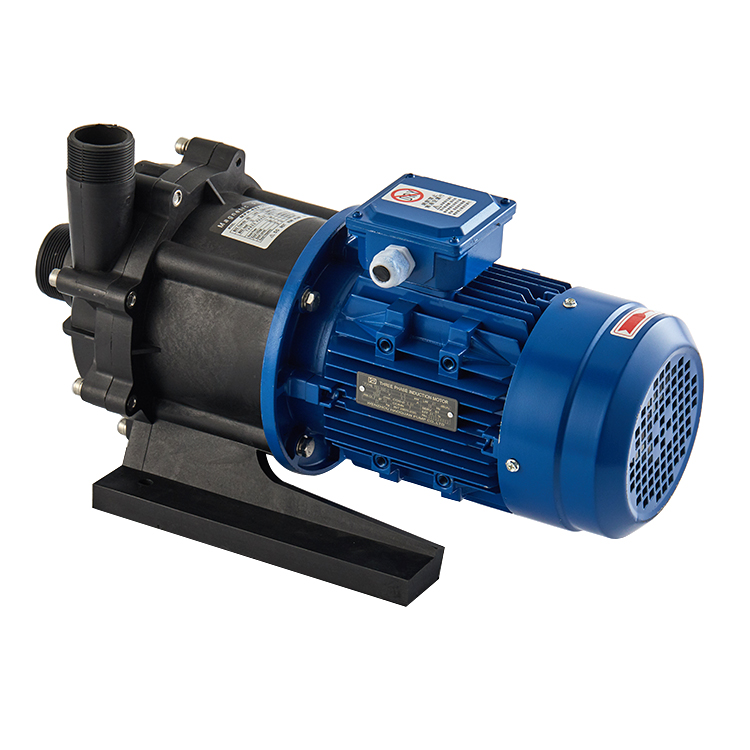
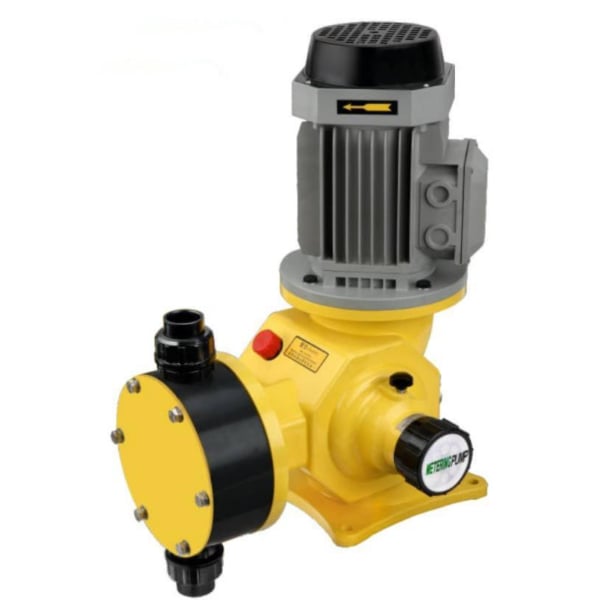
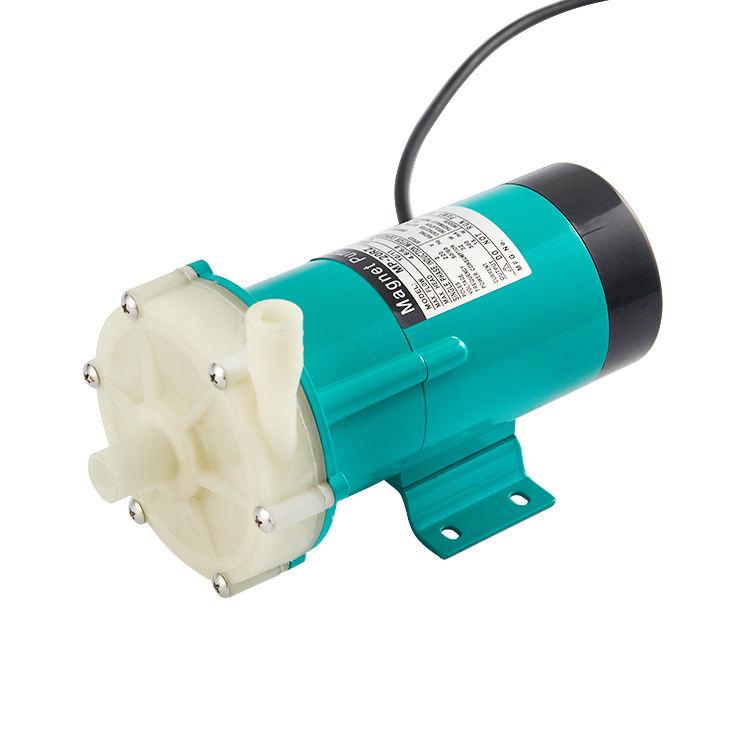
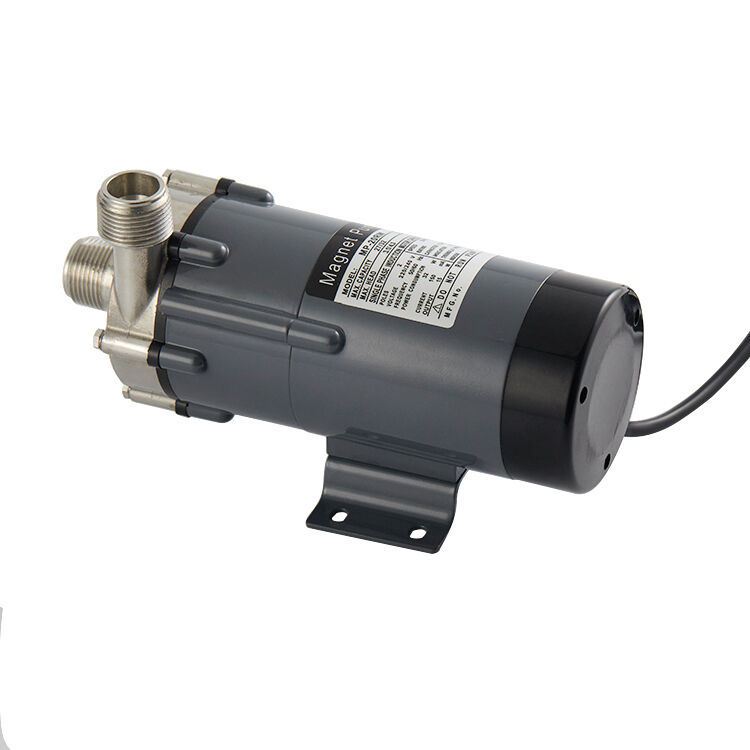
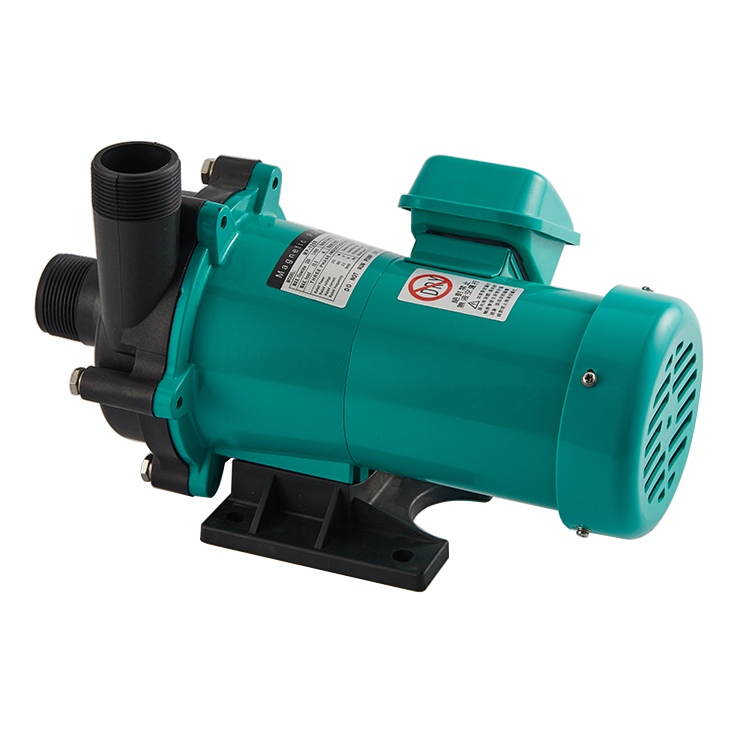
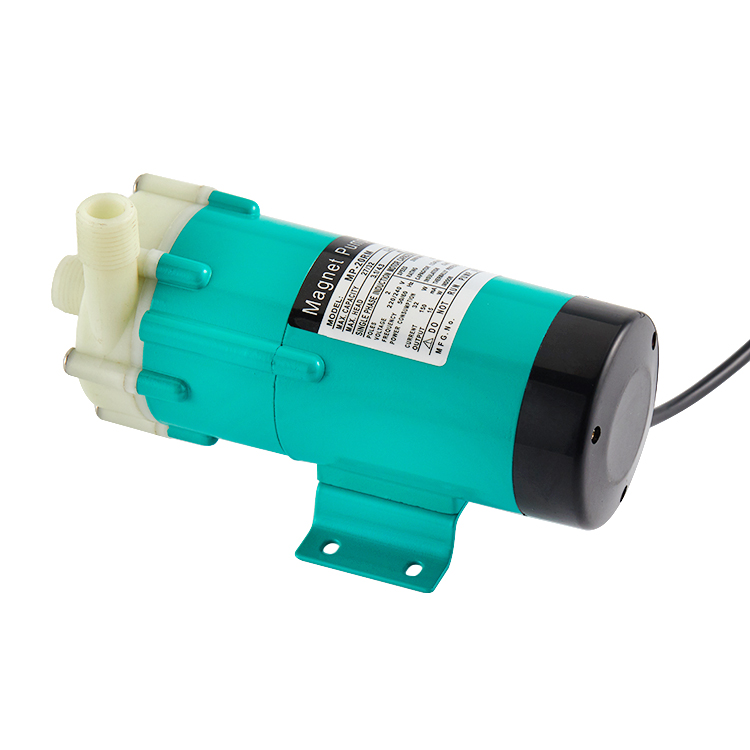
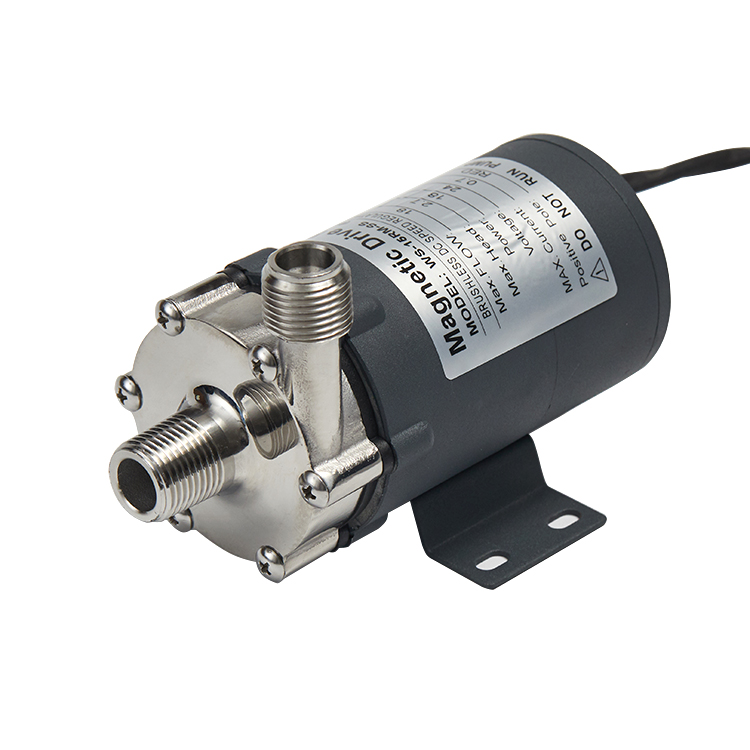
A food grade pump exporter specializes in providing high-quality pumping solutions designed specifically for the food and beverage industry. As a food grade pump exporter, the company delivers equipment that meets stringent international food safety standards and regulations. These pumps are engineered to handle various liquid products, including juices, dairy, oils, sauces, and beverages, while maintaining product integrity and purity throughout the transfer process.
The main functions of a food grade pump exporter include manufacturing pumps that efficiently transport food products without contamination or degradation. The technological features incorporate advanced materials such as stainless steel and food-safe elastomers that prevent chemical reactions with products. A food grade pump exporter utilizes precision engineering to ensure minimal product loss and consistent flow rates across different viscosity levels.
Key applications for pumps from a food grade pump exporter span numerous industries. These include dairy processing facilities, beverage production plants, sauce and condiment manufacturing, pharmaceutical companies, and cosmetic producers. The versatile design allows a food grade pump exporter to serve both large-scale industrial operations and smaller specialized producers. Modern food grade pump exporter models feature variable speed drives, self-priming capabilities, and easy-to-clean designs that reduce downtime and maintenance costs. These pumps ensure compliance with FDA, EHEDG, and 3-A Sanitary Standards, making them essential equipment for companies prioritizing quality assurance.

 EN