12v Food Grade Pump: Reliable Transfer

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

12v food grade pump

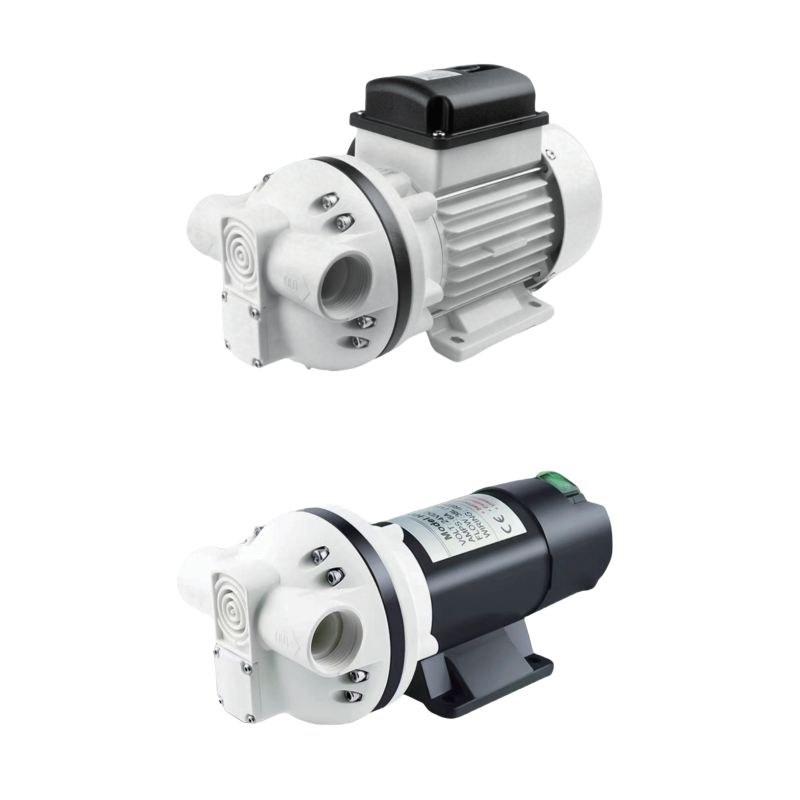
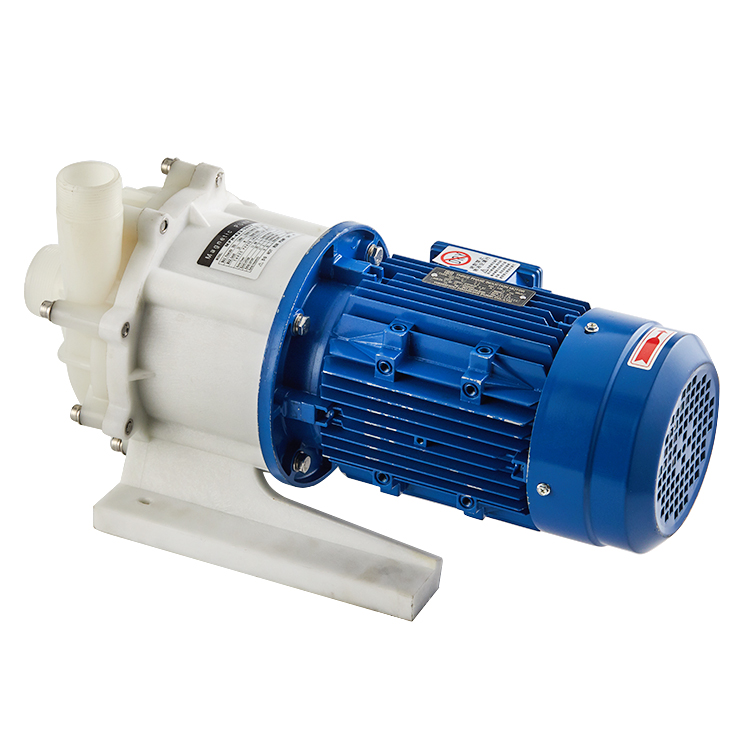
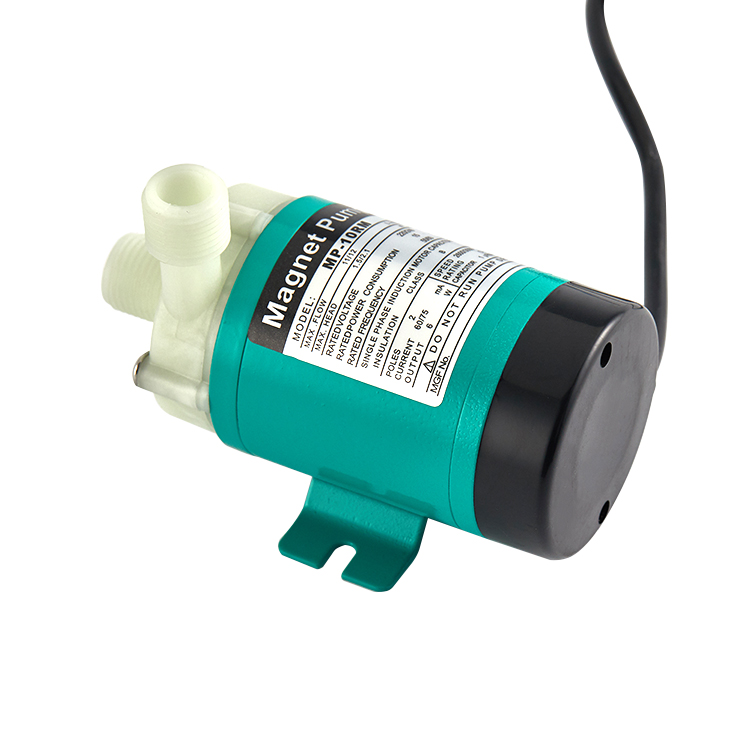
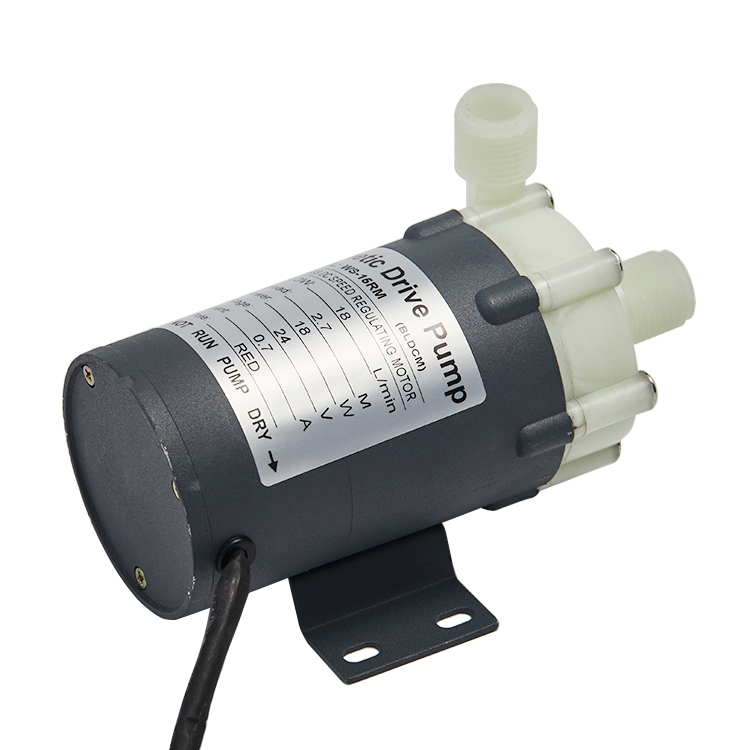
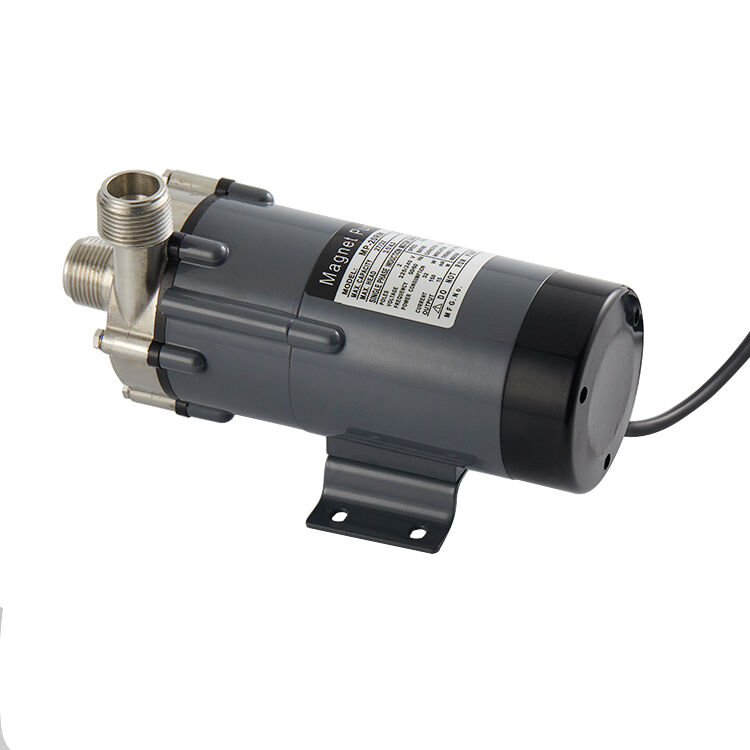
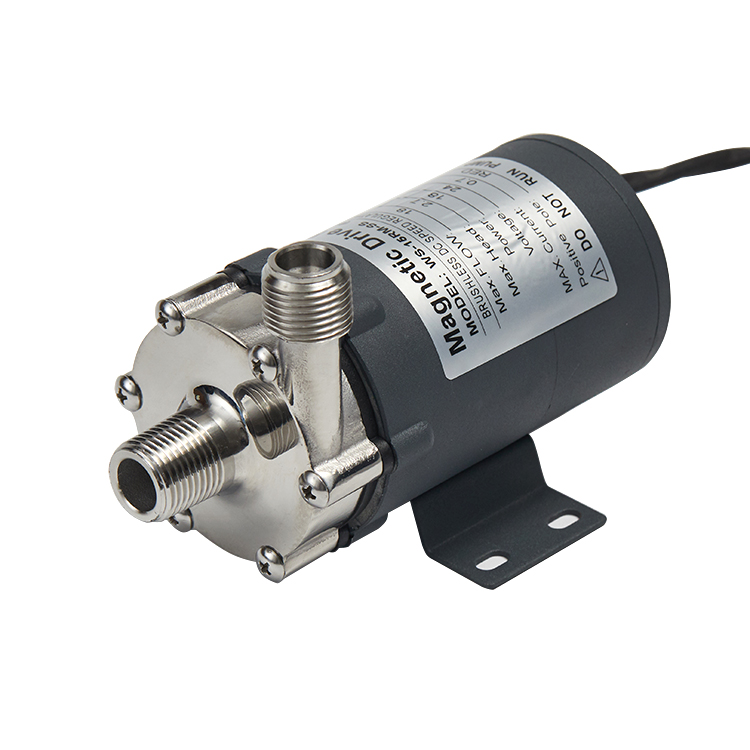
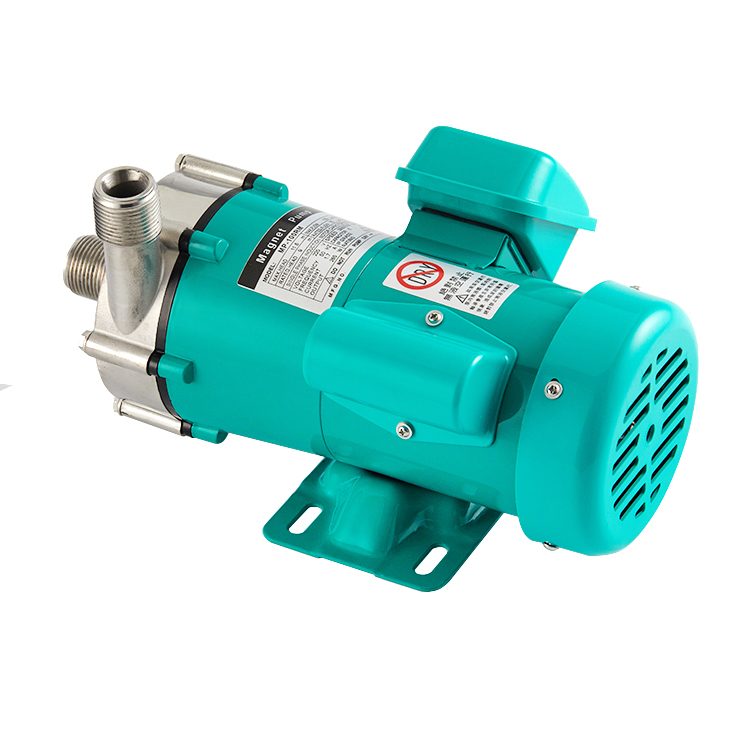
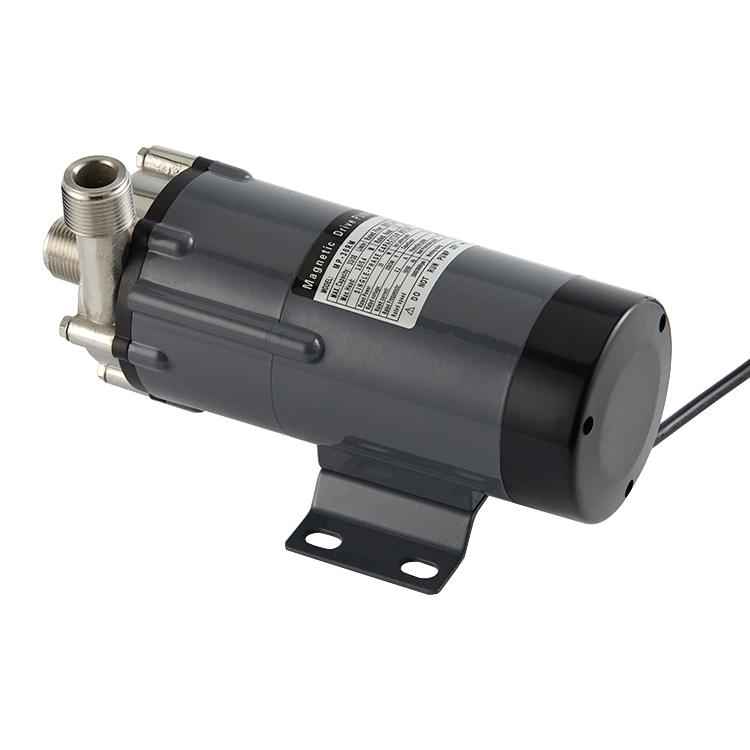
A 12v food grade pump represents a specialized fluid transfer solution designed specifically for the food and beverage industry. This compact, efficient device operates on a 12-volt power supply, making it ideal for portable applications, mobile food service units, and small-scale production environments. The 12v food grade pump features construction materials that comply with strict food safety standards, ensuring that all components contacting liquids are non-toxic and safe for consumable products. The primary function of a 12v food grade pump involves transferring beverages, sauces, oils, and other food-compatible liquids from one container to another with precision and reliability. Technologically, this pump incorporates brushless motor technology, which reduces maintenance requirements and extends operational lifespan. The 12v food grade pump operates with minimal noise levels, making it suitable for customer-facing environments such as cafes, restaurants, and catering services. Key technological features include adjustable flow rates, self-priming capabilities, and thermal protection systems. These components work together to provide consistent performance across varying viscosity liquids. The 12v food grade pump delivers reliable performance in numerous applications including beverage dispensing, sauce transfer, ingredient mixing, and ingredient circulation. Installation remains straightforward, requiring only basic electrical connections and appropriate hose attachments. The compact design allows integration into existing food service equipment or standalone operation. Whether serving small businesses or supplementing larger operations, the 12v food grade pump offers dependable fluid management in food preparation environments.

New Product Releases

A 12v food grade pump delivers exceptional practical benefits that directly address the needs of food service professionals and beverage distributors. The most significant advantage involves complete food safety compliance, as the 12v food grade pump features FDA-approved materials and sanitary construction that prevents contamination. This ensures your products maintain their integrity and quality throughout the transfer process.

Operationally, the 12v food grade pump provides energy efficiency that reduces electricity costs compared to traditional AC-powered alternatives. The brushless motor operates quietly, allowing seamless integration into customer-facing spaces without creating disruptive noise. Setup time becomes minimal thanks to universal hose connections and straightforward installation procedures, enabling business owners to deploy the pump quickly without specialized expertise. For specific applications, the 12v food grade pump excels in mobile catering operations where portability matters significantly. The compact footprint accommodates tight spaces in food trucks, carts, and temporary serving stations. The pump handles diverse liquid types, from thin beverages to thicker sauces, offering versatility that justifies the investment across multiple use cases.

Decision-useful context includes the 12v food grade pump's ability to operate from battery banks or vehicle electrical systems, providing unmatched flexibility for remote locations. Maintenance costs remain low because the brushless motor design eliminates carbon brush replacement. The thermal protection system prevents overheating during extended use, safeguarding equipment longevity. Long-term reliability means reduced downtime and consistent service delivery. These operational benefits combine to make the 12v food grade pump an economical choice for businesses prioritizing both safety and efficiency in their food handling processes.

Practical Tips

2026 BLDC Pump Guide: Top Models and Features

09

Jun

2026 BLDC Pump Guide: Top Models and Features

The bldc pump has emerged as one of the most technically advanced fluid-handling solutions available to engineers and procurement professionals entering 2026. Driven by brushless direct current motor technology, these pumps deliver a compelling combi...
View More
Industrial Pumping Solutions for the Textile Industry: Dyeing and Finishing Equipment

09

Jun

Industrial Pumping Solutions for the Textile Industry: Dyeing and Finishing Equipment

Introduction: The Demanding Fluid Dynamics of Textile Manufacturing The textile industry is one of the most resource-intensive and chemically complex manufacturing sectors globally. From the initial scouring and bleaching of raw fibers to the intrica...
View More
Smart Dosing Systems: Integrating Precision Pumps into Automated Production Lines

09

Jun

Smart Dosing Systems: Integrating Precision Pumps into Automated Production Lines

Introduction: The Evolution of Fluid Handling in Industry 4.0 The Fourth Industrial Revolution, or Industry 4.0, is fundamentally reshaping how factories operate. At the heart of this transformation is the shift from manual, isolated processes to int...
View More
Vertical Integration in Pump Manufacturing: How it Benefits International B2B Buyers

09

Jun

Vertical Integration in Pump Manufacturing: How it Benefits International B2B Buyers

Introduction In the increasingly complex global supply chain, international B2B buyers often face challenges such as unpredictable lead times, fluctuating quality standards, and hidden costs passed down from multiple tiers of suppliers. For companies...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

12v food grade pump

Food-Safe Construction for Superior Product Protection

Food-Safe Construction for Superior Product Protection

The 12v food grade pump incorporates materials specifically approved for direct food contact, meeting FDA and NSF standards that govern food service equipment. Every component touching your beverages, sauces, or ingredients comes from non-reactive materials that prevent flavor contamination or chemical leaching. The 12v food grade pump utilizes stainless steel interior surfaces and food-grade rubber seals that withstand repeated washing and sanitization cycles required in commercial kitchens. This construction standard extends the pump's working life while ensuring your products arrive at customers in perfect condition. The sealed motor design protects internal mechanisms from moisture and liquid spray, critical protection in wet food service environments. Choosing a 12v food grade pump means investing in equipment that prioritizes consumer safety above all else.
Efficient 12V Operation for Portable Power Solutions

Efficient 12V Operation for Portable Power Solutions

Operating on a standard 12-volt electrical supply makes the 12v food grade pump uniquely adaptable to various power sources that traditional AC pumps cannot access. Connect directly to vehicle electrical systems in food trucks, refrigerated vans, or catering trailers. Battery backup capability allows the 12v food grade pump to continue functioning during power interruptions, essential for maintaining service continuity at events or outdoor locations. The efficient brushless motor consumes minimal electricity, extending battery life when operating on portable power banks. Lower power consumption translates directly to reduced operational costs compared to conventional pumping solutions. The 12v food grade pump's energy efficiency makes it environmentally responsible while supporting bottom-line profitability. Remote deployment becomes practical and economical when you eliminate dependency on conventional electrical infrastructure, positioning this equipment as the preferred choice for mobile food service operations.
Reliable Performance with Minimal Maintenance Requirements

Reliable Performance with Minimal Maintenance Requirements

The 12v food grade pump features brushless motor technology that eliminates carbon brush wear, a primary source of maintenance issues in conventional pumps. Reduced moving parts mean fewer components susceptible to failure, translating directly to extended equipment lifespan and lower lifetime ownership costs. The self-priming capability of the 12v food grade pump allows quick startup without manual priming procedures, saving valuable time during busy service periods. Thermal protection systems automatically monitor motor temperature, shutting down operation if dangerous heat accumulates, protecting your investment and ensuring safe operation. Simple cleaning procedures keep the 12v food grade pump hygienic without requiring disassembly or specialized tools. Sealed construction prevents debris infiltration, eliminating frequent repairs associated with contaminated motors. This reliability-focused design means business owners spend less time troubleshooting equipment and more time serving customers, making the 12v food grade pump a dependable workhorse for continuous commercial applications.
12v Food Grade Pump: Reliable Transfer

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000