Food Grade Pump Supplier Solutions

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade pump supplier

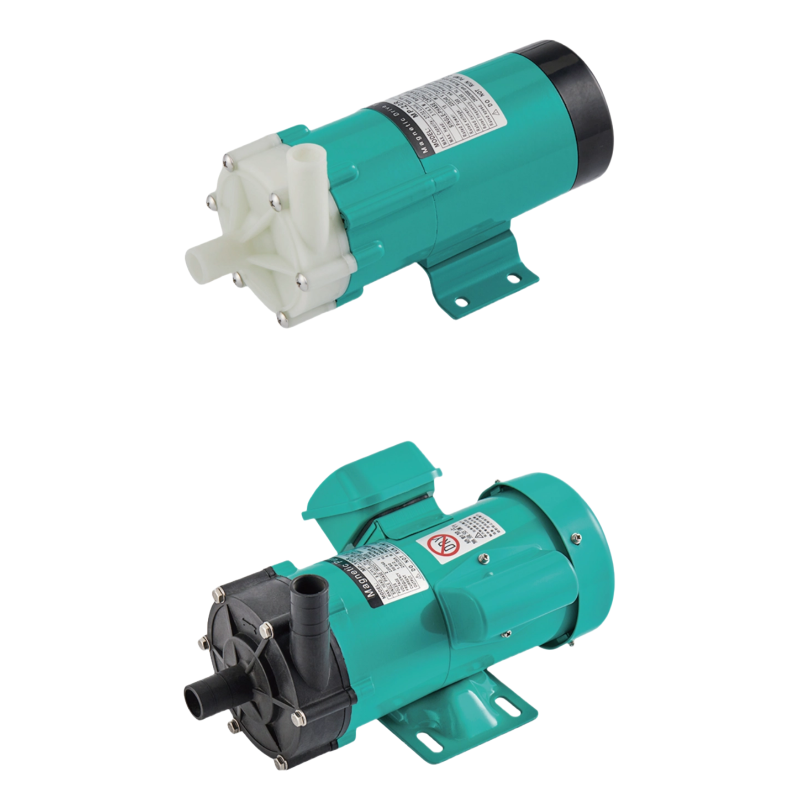
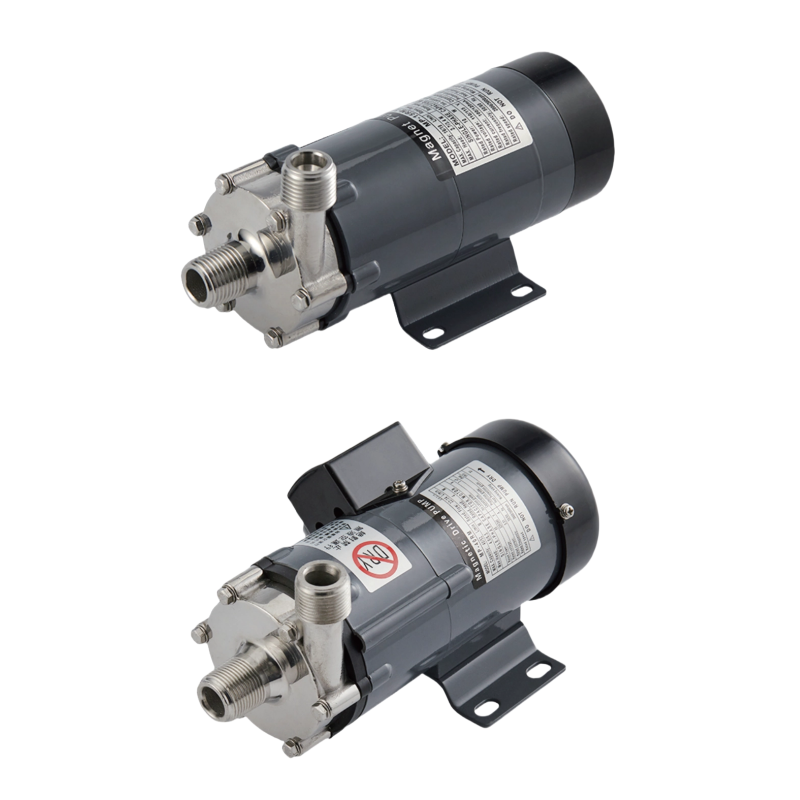
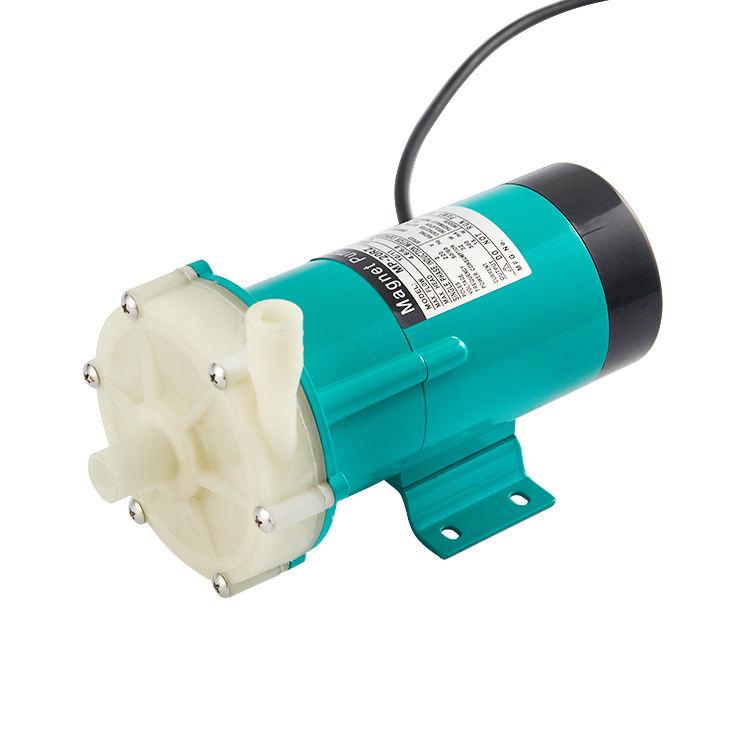
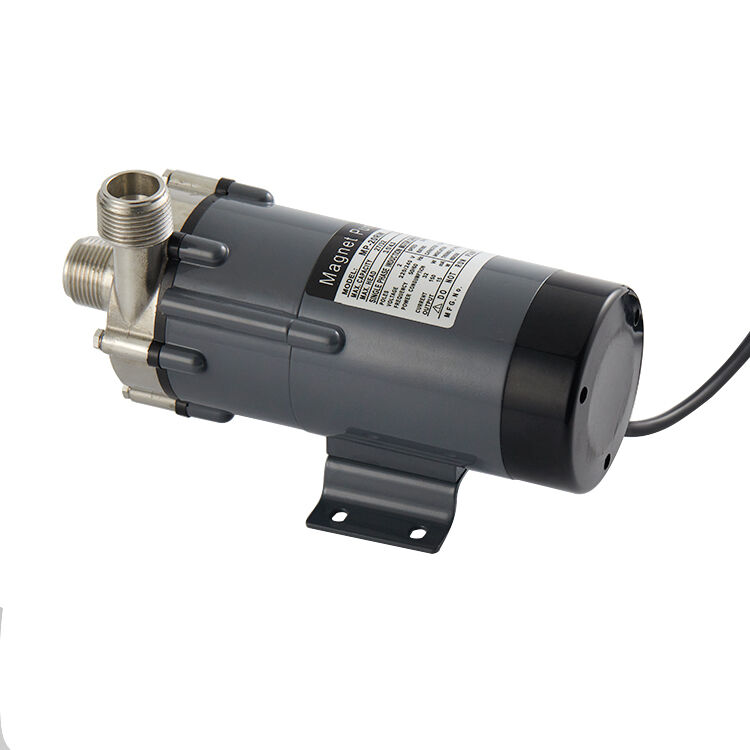
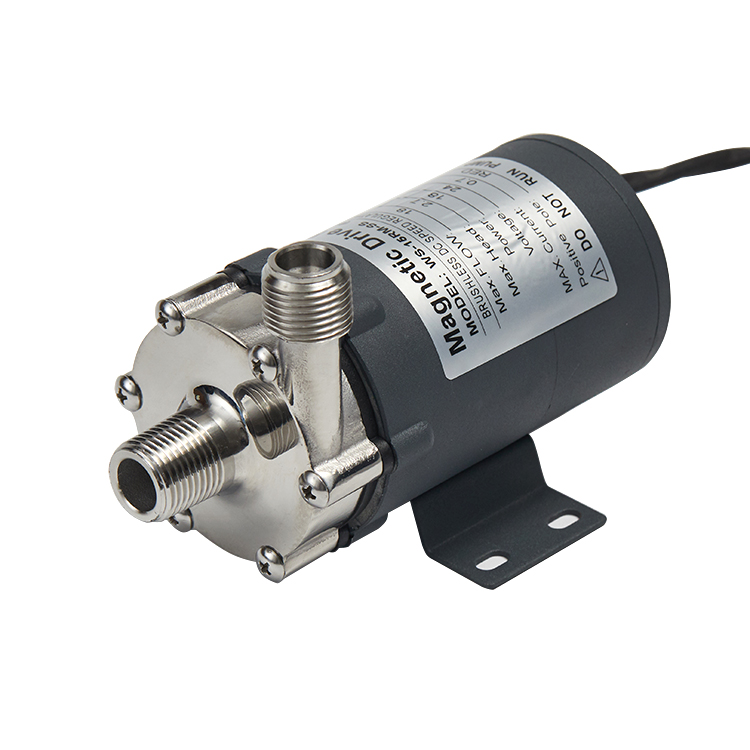
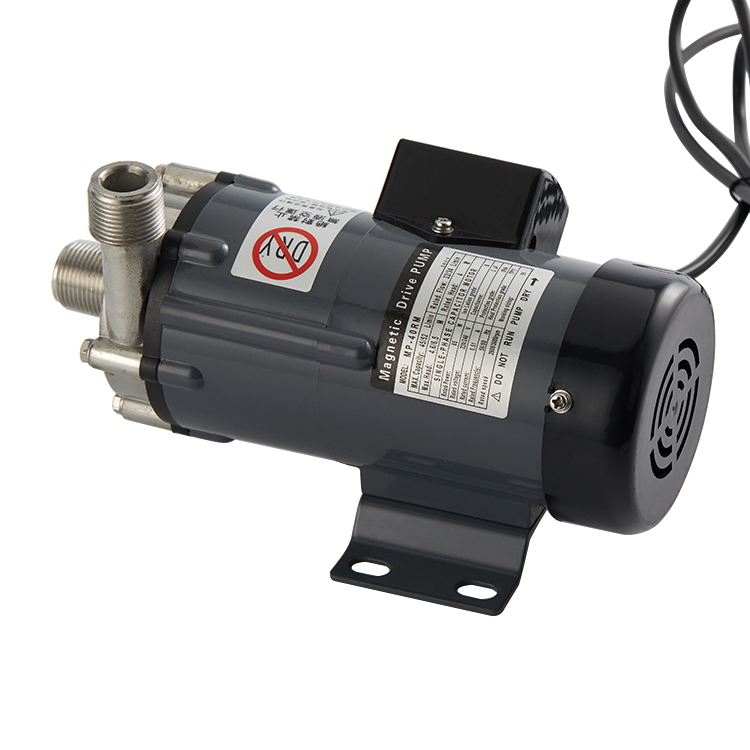
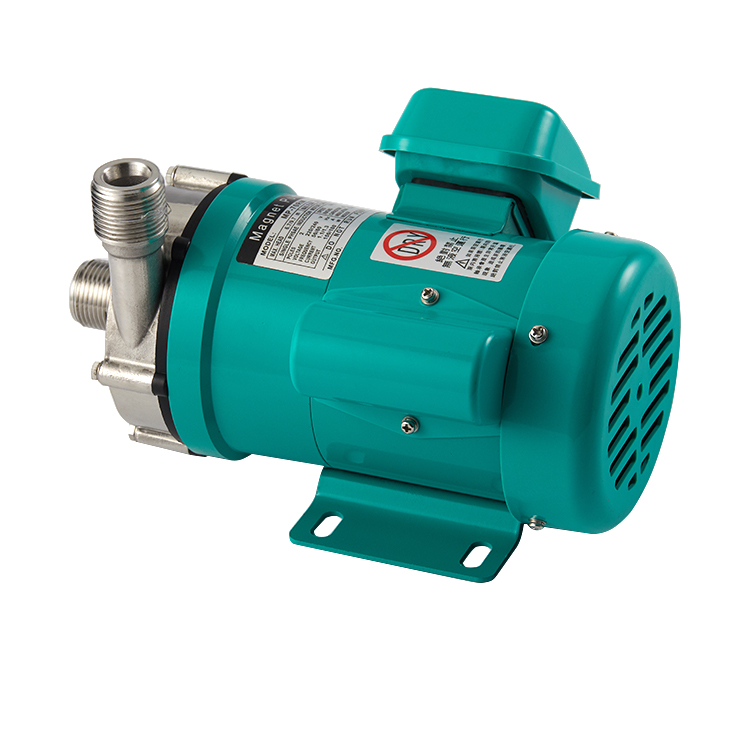
A food grade pump supplier specializes in providing high-quality pumping solutions designed specifically for the food and beverage industry. These pumps meet stringent regulatory standards and safety requirements essential for handling consumable products. A reliable food grade pump supplier offers equipment that maintains product integrity while preventing contamination throughout processing operations. Food grade pumps function by transferring liquids, viscous substances, and semi-solid materials through production lines without compromising quality or safety. The primary functions include precise metering, gentle handling of delicate ingredients, and consistent flow rates across various processing stages. A professional food grade pump supplier ensures their equipment handles diverse applications from dairy products to pharmaceutical ingredients. Technological features distinguish premium offerings from basic alternatives. Advanced food grade pump suppliers incorporate materials like stainless steel and FDA-approved components that resist corrosion and withstand frequent sanitization cycles. These pumps feature hygienic design elements, minimizing dead zones where bacteria could accumulate. Variable speed controls and automated pressure monitoring systems enhance operational precision. Applications span multiple industries where product purity matters critically. Food grade pump suppliers support yogurt production, sauce manufacturing, juice processing, and cosmetic formulation. Pharmaceutical companies and nutraceutical manufacturers also depend on food grade pump suppliers for ingredient handling. The versatility of modern pumping technology allows solutions for various viscosity levels and temperature ranges, making food grade pump suppliers invaluable partners in maintaining production excellence and regulatory compliance.

New Products

Choosing the right food grade pump supplier delivers significant operational and commercial benefits for your business. These advantages extend beyond basic functionality to encompass reliability, efficiency, and peace of mind. First, food grade pump suppliers provide equipment engineered for absolute safety and compliance. Working with an established food grade pump supplier means your operations meet FDA regulations, USDA standards, and international food safety certifications without additional modifications or workarounds. This eliminates costly compliance issues and potential production shutdowns. Second, quality food grade pump suppliers reduce contamination risks substantially. Their equipment features smooth surfaces and minimal crevices where harmful microorganisms could flourish. This direct benefit protects your brand reputation and prevents expensive product recalls that damage customer trust.

Third, partnering with a food grade pump supplier improves operational efficiency. Precision pumping reduces product waste during transfer, lowering your per-unit production costs. Consistent flow rates minimize processing time variations, allowing faster turnaround on orders. Fourth, reliable food grade pump suppliers offer excellent maintenance support and spare parts availability. Quick access to replacement components means minimal downtime when maintenance becomes necessary. This responsiveness directly impacts your production schedule and revenue.

Finally, expert food grade pump suppliers provide technical consultation for your specific application. They help select appropriate equipment configurations, reducing the risk of purchasing oversized or undersized units. This consultative approach ensures optimal performance from day one, maximizing your return on investment. These combined advantages make working with experienced food grade pump suppliers a strategic business decision that strengthens operations while protecting product quality and regulatory standing.

Practical Tips

Inside Haoquan’s Quality Inspection System: Ensuring Zero-Defect Pump Manufacturing

09

Jun

Inside Haoquan’s Quality Inspection System: Ensuring Zero-Defect Pump Manufacturing

Introduction In the high-stakes world of industrial fluid management, the reliability of a pump is not just a performance metric—it is a cornerstone of operational safety and economic efficiency. For industries ranging from chemical processing ...
View More
From Prototype to Mass Production: Haoquan’s OEM/ODM Project Management Process

09

Jun

From Prototype to Mass Production: Haoquan’s OEM/ODM Project Management Process

Introduction In the competitive industrial landscape, "off-the-shelf" pumps often fail to meet the unique requirements of specialized applications. Whether it's a micro-vacuum pump for a diagnostic medical device or a high-pressure diaphragm pump for...
View More
How Smart Sensors and IoT are Transforming Industrial Pump Maintenance Strategies

09

Jun

How Smart Sensors and IoT are Transforming Industrial Pump Maintenance Strategies

Introduction: The Intelligence Surge in Pumping Systems For decades, industrial pump maintenance was characterized by two primary methods: "run-to-fail" (reactive) or "calendar-based" (preventative). Both methods are inherently inefficient. Reactive ...
View More
Magnetic Pump vs. Mechanically Sealed Pump: Which One Eliminates Leaks and Reduces Maintenance Costs?

21

Jul

Magnetic Pump vs. Mechanically Sealed Pump: Which One Eliminates Leaks and Reduces Maintenance Costs?

Seal failure remains one of the most common reasons an industrial pump ends up offline unexpectedly. For plant engineers handling hazardous, corrosive, or high-value fluids, the choice between a magnetic drive pump and a mechanically sealed pump dire...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

food grade pump supplier

Hygienic Design Standards for Maximum Safety

Hygienic Design Standards for Maximum Safety

Premium food grade pump suppliers prioritize hygienic engineering principles in every product design. Their equipment features smooth, crevice-free surfaces that eliminate harboring sites for pathogens and bacteria. Food grade pump suppliers construct pumps using stainless steel and FDA-approved elastomers that withstand repeated cleaning cycles without degradation. The importance of hygienic design cannot be overstated in food processing environments. A quality food grade pump supplier understands that even microscopic contamination can compromise entire production batches. Their commitment to design excellence means your operations maintain the highest sanitation standards consistently. This value extends beyond immediate safety. By investing in equipment from a food grade pump supplier emphasizing hygienic design, you protect your brand reputation and customer loyalty. Retailers and consumers increasingly demand products manufactured under the strictest safety protocols. Choosing a food grade pump supplier that delivers hygienic excellence positions your business as quality-focused and trustworthy in competitive markets.
Precision Control and Consistent Performance

Precision Control and Consistent Performance

Advanced food grade pump suppliers deliver equipment with sophisticated control systems enabling precise metering and flow rate management. These systems maintain consistent product transfer regardless of viscosity variations or pressure fluctuations. A dedicated food grade pump supplier invests in technology ensuring reliable performance across extended production runs. Precision matters significantly when manufacturing products requiring exact ingredient ratios. Food grade pump suppliers offering variable speed drives and pressure sensors provide real-time monitoring capabilities. Operators can adjust parameters instantly, preventing product defects before they occur. The value of this precision extends to cost savings and quality assurance. Accurate metering reduces ingredient waste substantially, directly improving profit margins. Consistent performance minimizes batch-to-batch variations, ensuring uniform product quality that satisfies consumer expectations. When selecting a food grade pump supplier, prioritize those demonstrating commitment to precision technology and automated controls that protect your production integrity and profitability.
Expert Support and Long-Term Partnership

Expert Support and Long-Term Partnership

Distinguishing food grade pump suppliers includes their commitment to customer success beyond the initial sale. Leading food grade pump suppliers employ technical specialists who understand complex production environments and assist with equipment optimization. They provide training, troubleshooting, and strategic guidance for maximizing equipment performance. The value of partnership with a food grade pump supplier extends throughout the equipment lifecycle. Responsive technical support minimizes unexpected downtime that disrupts production schedules and revenue streams. Expert food grade pump suppliers maintain readily available spare parts inventory, ensuring quick replacement availability when needed. Proactive communication from a food grade pump supplier helps identify maintenance needs before failures occur. Regular inspections and performance analysis prevent costly emergency repairs. This partnership approach distinguishes professional food grade pump suppliers from transactional vendors. By choosing food grade pump suppliers emphasizing long-term relationships and customer support, you gain a trusted resource invested in your operational success and growth trajectory.
Food Grade Pump Supplier Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000