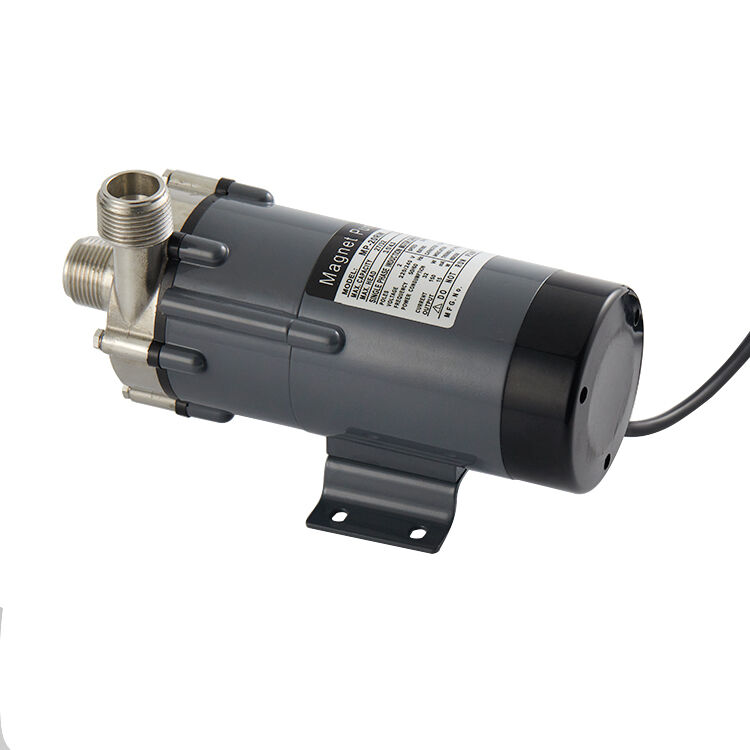
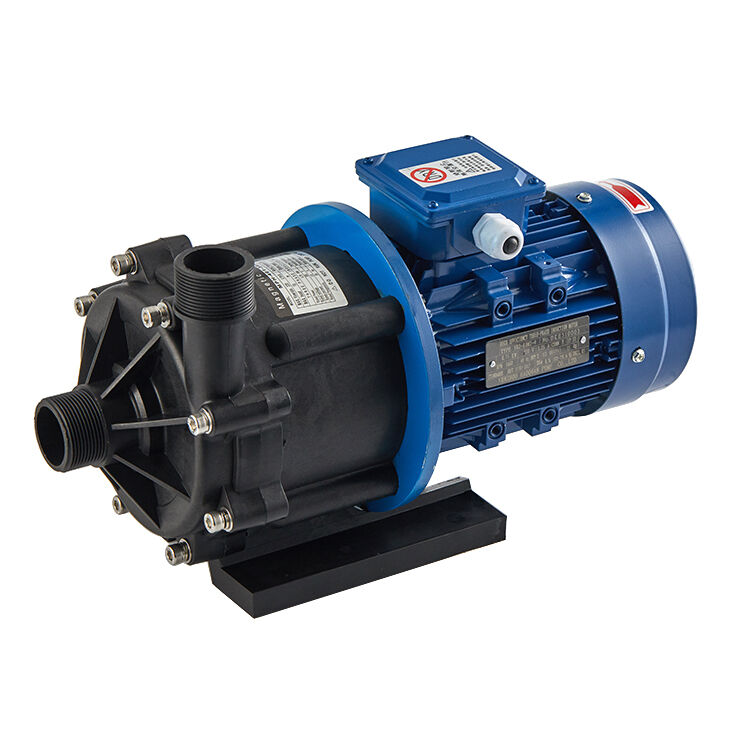
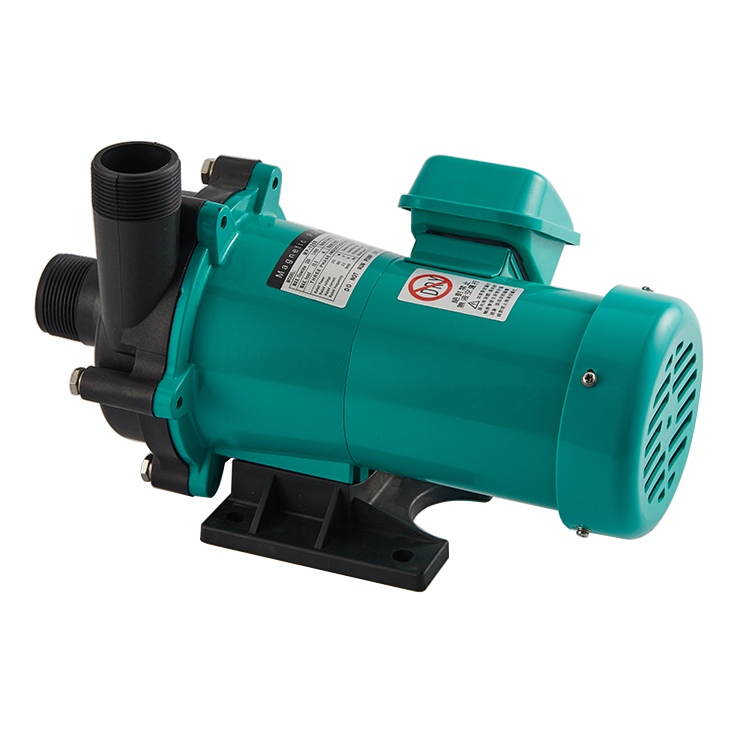
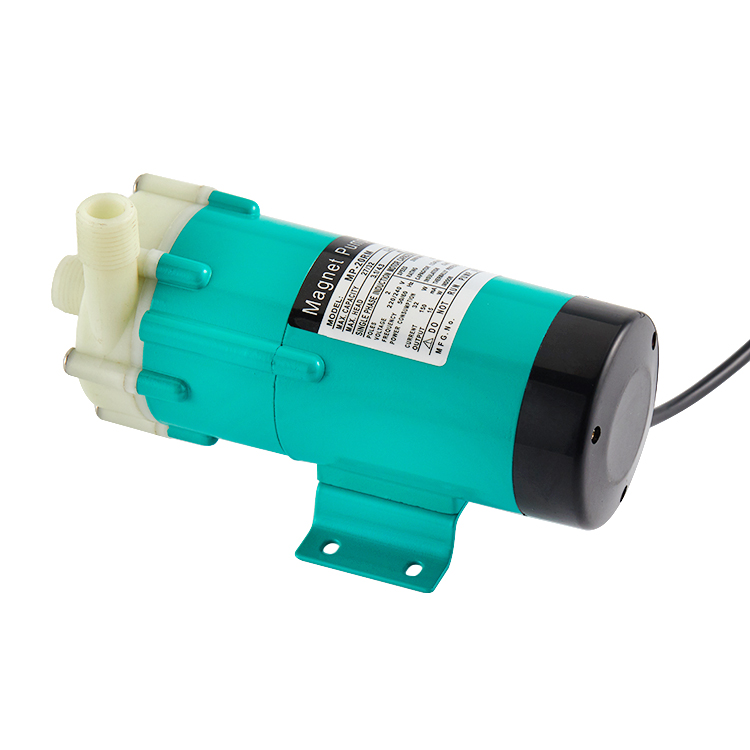
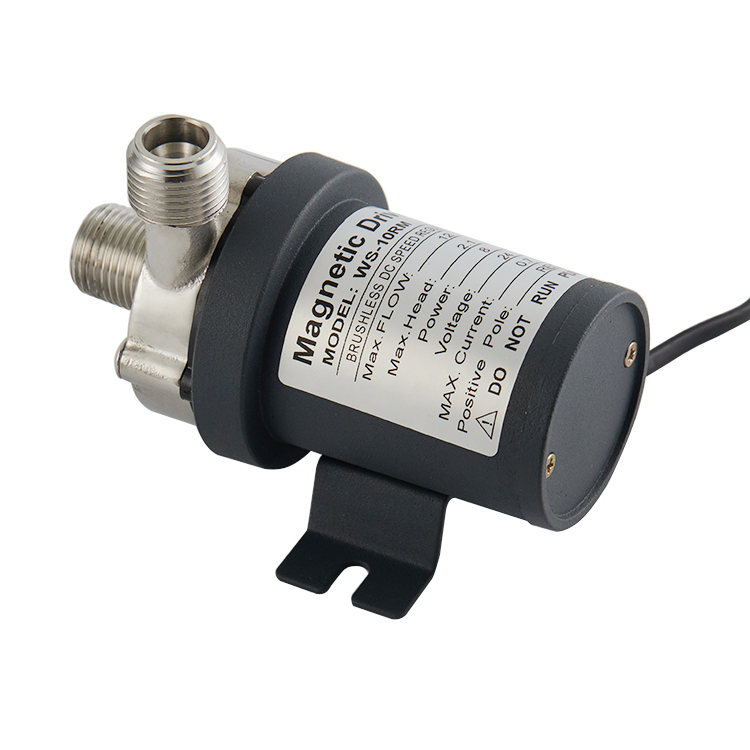
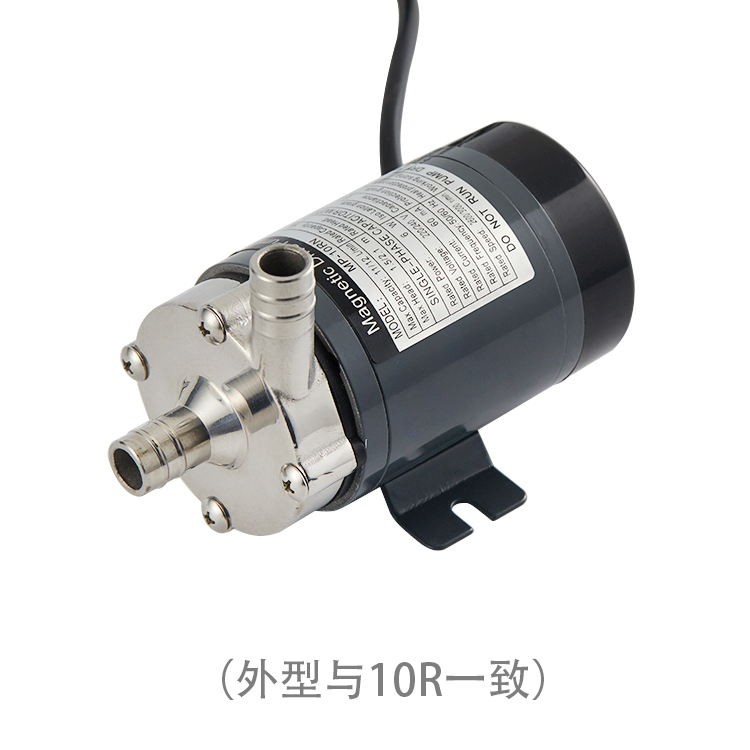
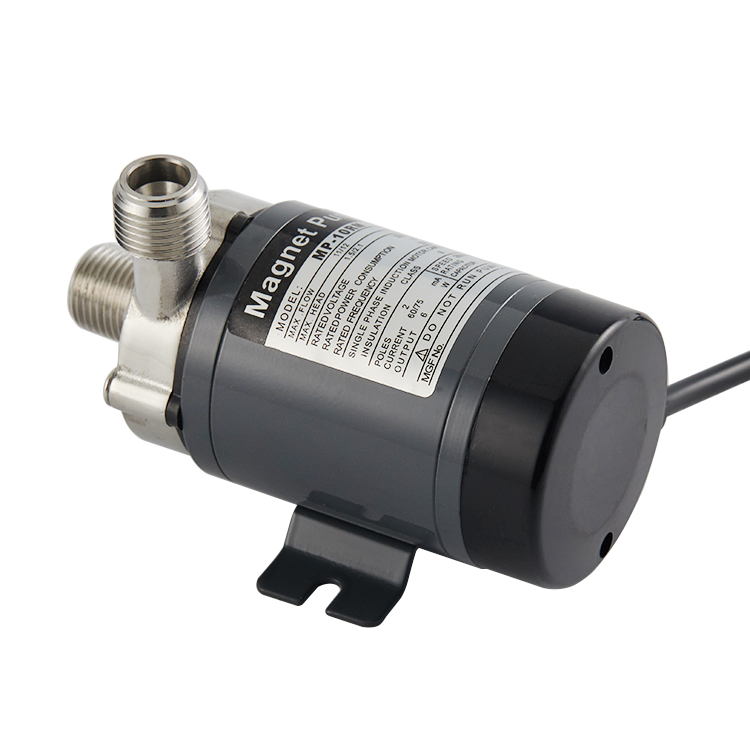
food grade pump with variable speed
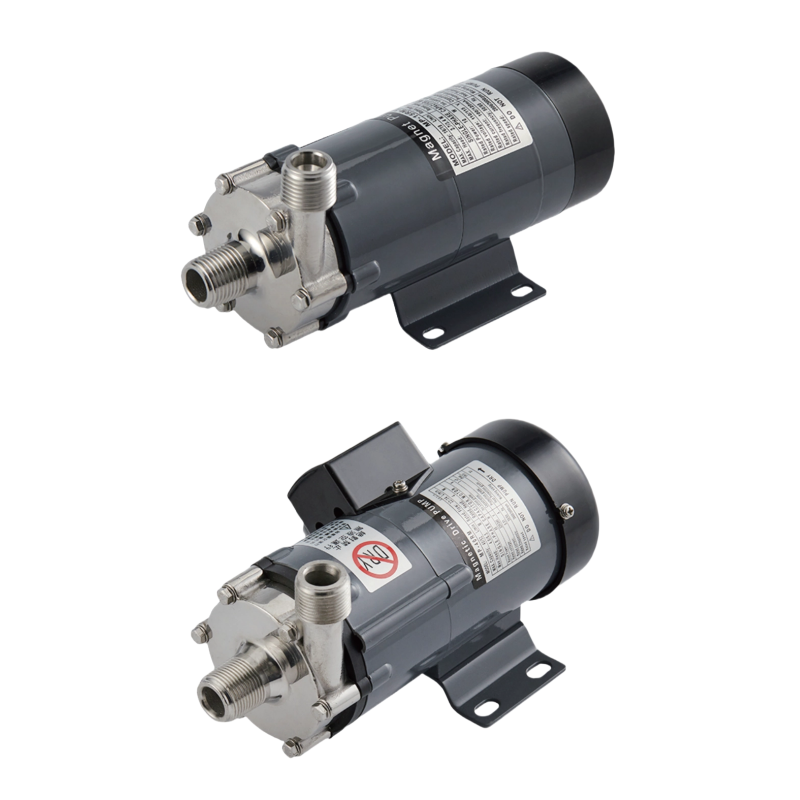
A food grade pump with variable speed represents a modern solution for industries requiring precise fluid transfer and consistent performance. This specialized equipment combines advanced engineering with food-safe materials to meet stringent regulatory standards. The food grade pump with variable speed operates by adjusting motor velocity to control flow rates and pressure levels dynamically, making it ideal for applications where precise dosing matters significantly.
The primary function of a food grade pump with variable speed is to transfer liquids, viscous products, and sensitive ingredients without contamination or degradation. Whether handling dairy products, beverages, sauces, or pharmaceutical preparations, this equipment maintains product integrity throughout the transfer process. The variable speed feature enables operators to optimize performance based on specific application requirements, reducing waste and enhancing efficiency.
Technologically, the food grade pump with variable speed integrates stainless steel components, sanitary connections, and non-toxic materials throughout its construction. The variable speed mechanism allows seamless adjustment from low to high capacity operations, accommodating diverse production scenarios. Advanced control systems enable precise monitoring and automation, ensuring consistent delivery rates and minimizing human intervention. These pumps feature sealed designs that prevent external contamination while facilitating thorough cleaning and sterilization protocols essential in food processing environments.

 EN