Portable Food Grade Pump

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

portable food grade pump

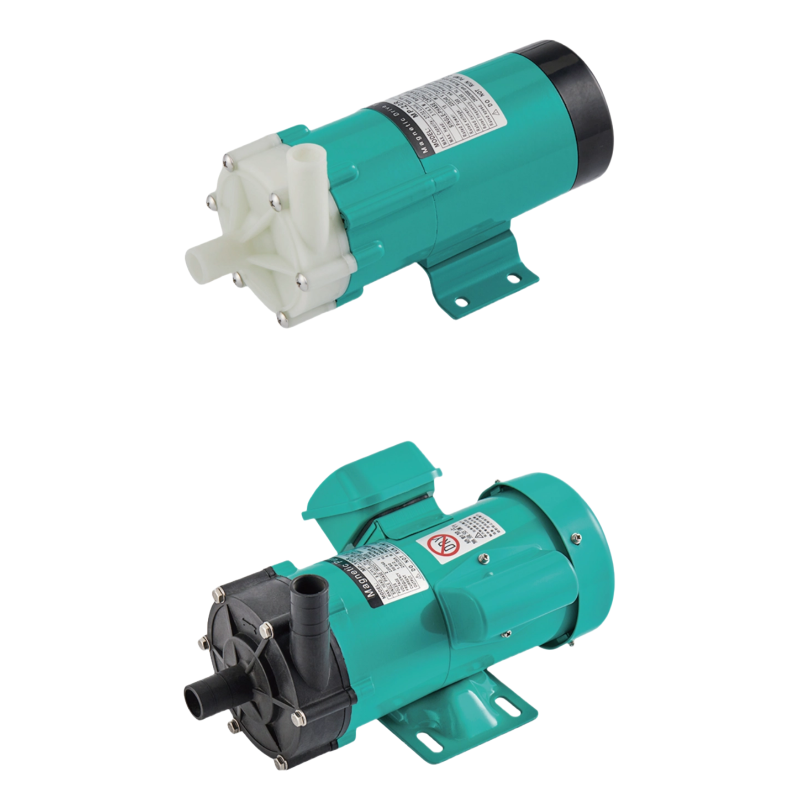
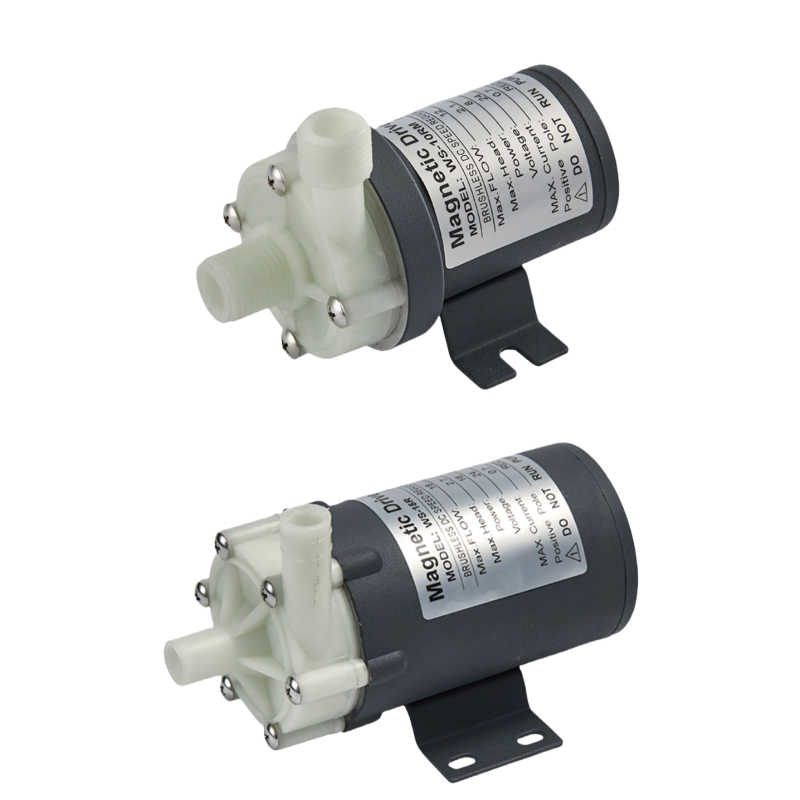
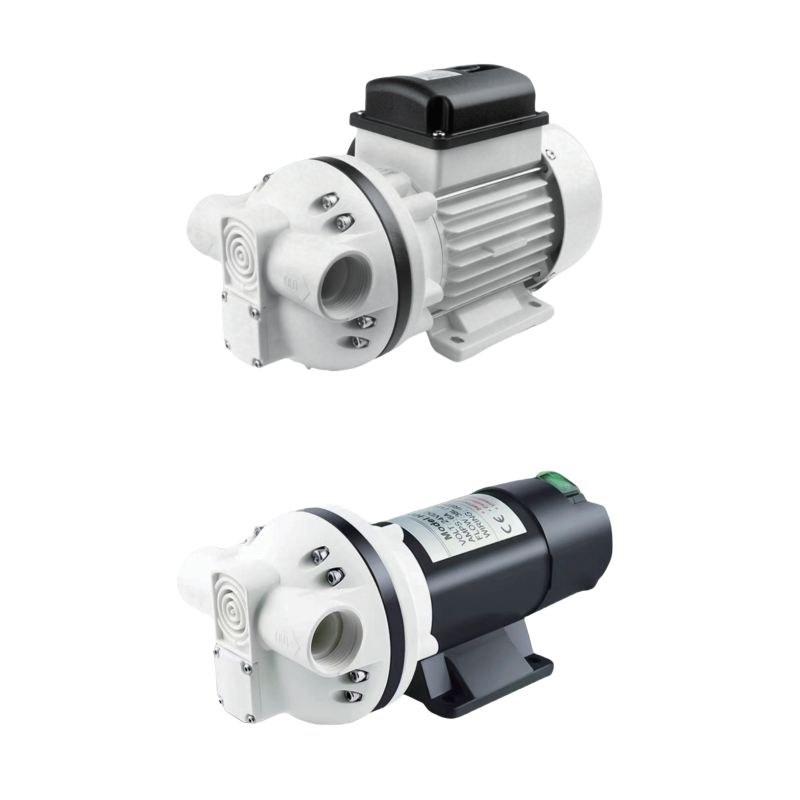
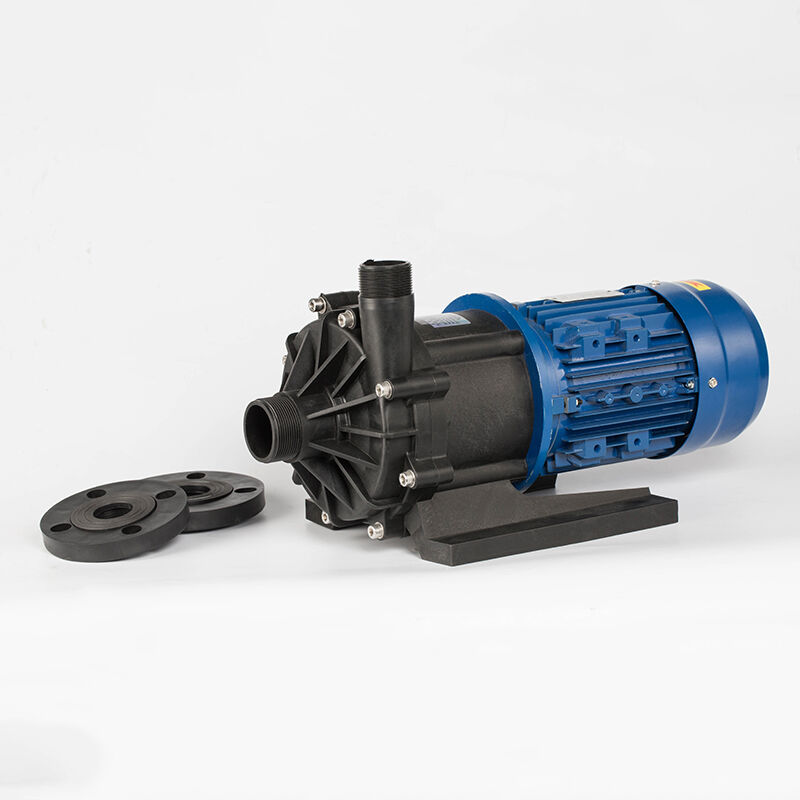
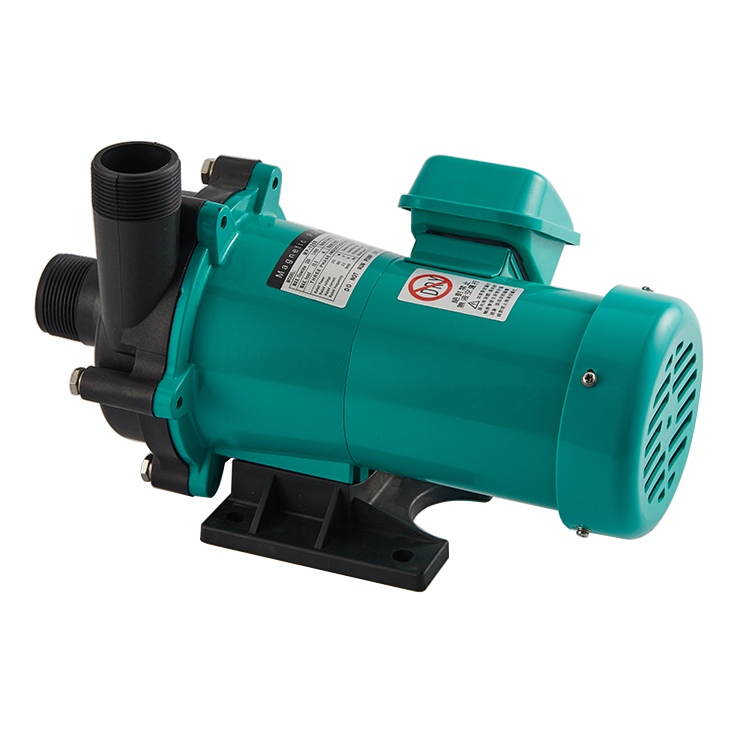
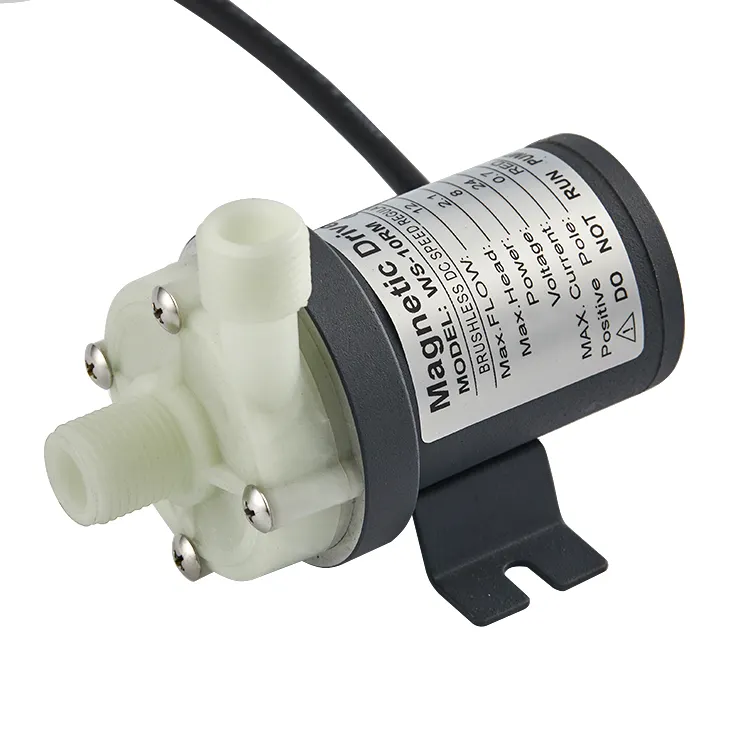
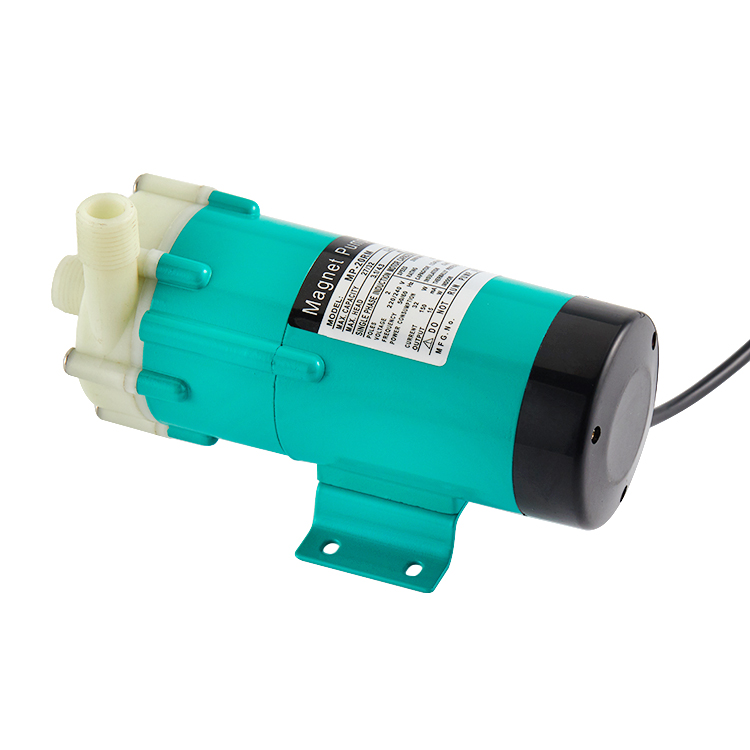
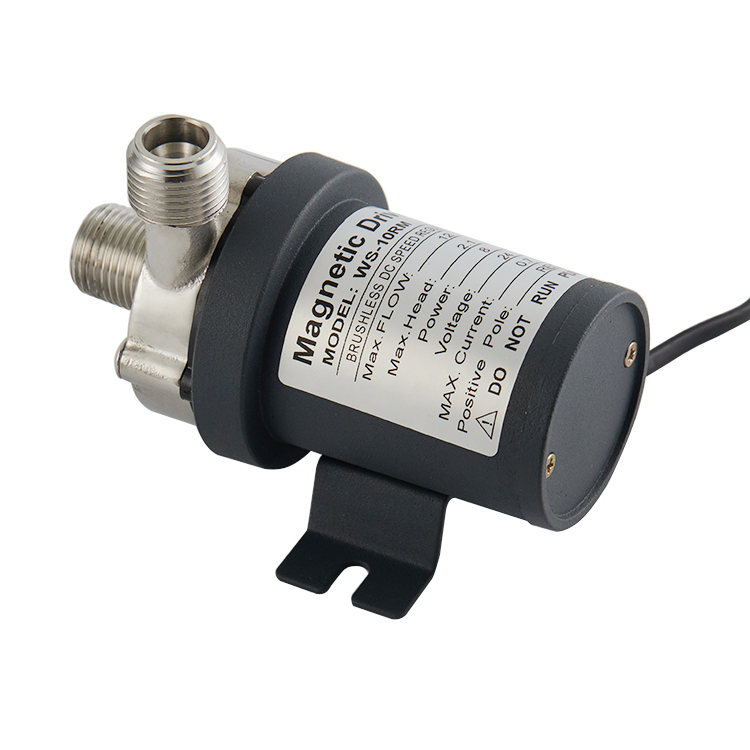
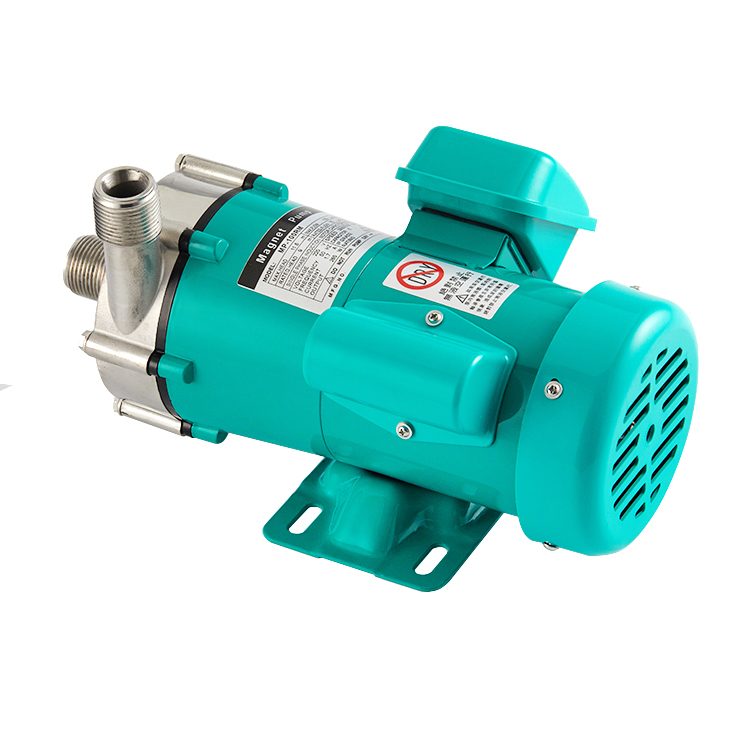
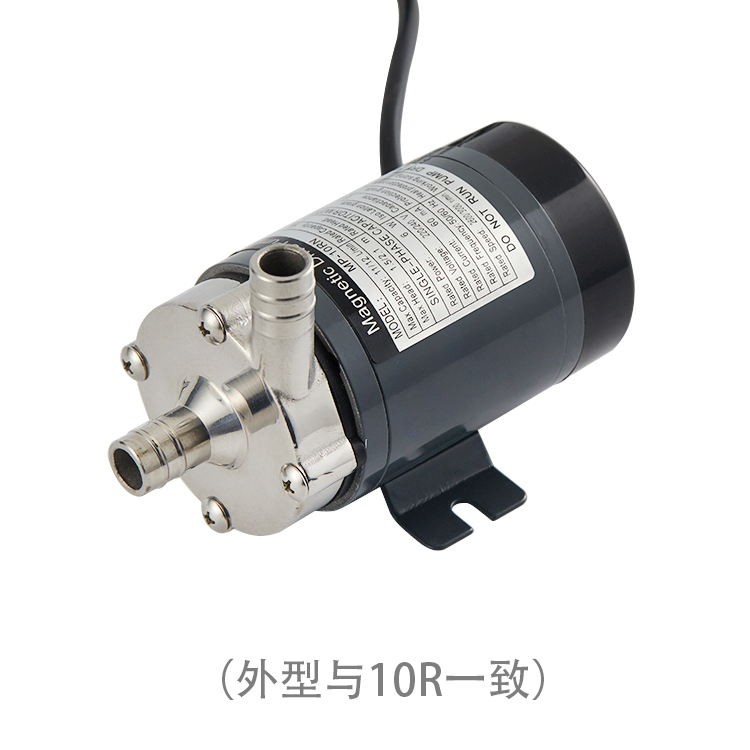
A portable food grade pump represents an essential tool for businesses and individuals working with food products, beverages, and culinary ingredients. This innovative equipment delivers reliable fluid transfer solutions specifically designed to meet stringent food safety standards. The portable food grade pump functions by utilizing efficient pumping mechanisms that transport liquids without contamination, making it ideal for commercial kitchens, restaurants, catering services, and food processing facilities. The portable food grade pump incorporates advanced technological features that distinguish it from standard pumping equipment. Its construction utilizes food-safe materials certified for direct contact with consumable products, ensuring compliance with health regulations and industry guidelines. The pump delivers consistent flow rates while maintaining product integrity, preventing oxidation and preserving flavor profiles crucial for culinary applications. Key technological features include adjustable pressure settings, variable speed controls, and seamless operation across various viscosity levels. These capabilities enable users to handle diverse liquids ranging from thin sauces to thick batters with equal efficiency. The portable food grade pump operates through electric-powered systems that provide reliable performance while consuming minimal energy. Applications for the portable food grade pump span numerous industries including beverage production, ingredient distribution, sauce manufacturing, and restaurant operations. Its portability allows seamless movement between different workstations, enhancing operational flexibility. Whether transferring hot chocolate, cooking oils, fruit purees, or specialized culinary ingredients, the portable food grade pump delivers professional-grade performance in controlled, sanitary conditions.

Popular Products

The portable food grade pump delivers exceptional value through its comprehensive advantages designed specifically for food industry professionals. This equipment eliminates manual labor associated with traditional transfer methods, significantly reducing preparation time and minimizing physical strain on staff members. By automating fluid transfer processes, the portable food grade pump enhances workplace efficiency while maintaining consistent quality standards across all operations.

Operational benefits extend beyond simple convenience. The portable food grade pump ensures precise portion control and accurate ingredient distribution, reducing waste and improving cost management for businesses operating on tight margins. Its reliable performance minimizes downtime, allowing kitchens and production facilities to maintain consistent service schedules without interruption. Staff members can redirect their efforts toward value-added tasks rather than physically moving heavy containers. For restaurants and catering services, the portable food grade pump proves invaluable in managing high-volume ingredient transfers during peak service periods. The equipment handles multiple liquid types simultaneously, adapting to changing operational demands throughout the day. Its portability means operators can position the portable food grade pump wherever needed, eliminating bottlenecks in workflow efficiency.

Food safety represents a paramount consideration, and the portable food grade pump addresses this concern comprehensively. Its food-grade certification guarantees that all materials contact surfaces meet regulatory requirements, protecting consumer health and preserving brand reputation. Decision-making becomes straightforward when evaluating equipment designed specifically for food applications. The portable food grade pump investment protects businesses from contamination risks, regulatory violations, and costly recalls. Long-term durability and minimal maintenance requirements make this equipment a smart financial decision for facilities prioritizing both safety and profitability.

Latest News

How to Optimize the Performance of Urea Pumps in Harsh Operating Conditions

09

Jun

How to Optimize the Performance of Urea Pumps in Harsh Operating Conditions

Introduction: The Vulnerability of SCR Systems in Extreme Environments Selective Catalytic Reduction (SCR) systems are a critical component of modern diesel engines, responsible for transforming harmful nitrogen oxides (NOx) into harmless water and n...
View More
Industrial Pump Buying Guide: Centrifugal vs. Positive Displacement, Seal Types, and Energy Efficiency Explained

21

Jul

Industrial Pump Buying Guide: Centrifugal vs. Positive Displacement, Seal Types, and Energy Efficiency Explained

Buying the wrong industrial pump rarely shows up as an immediate failure. Instead, it appears months later as rising energy bills, frequent seal replacements, or gradual efficiency loss that erodes plant profitability. This guide brea...
View More
How to Choose the Right Magnetic Pump for Corrosive Chemicals, High-Purity Fluids, and Explosive Environments

21

Jul

How to Choose the Right Magnetic Pump for Corrosive Chemicals, High-Purity Fluids, and Explosive Environments

Magnetic drive pumps are often selected for one reason: eliminating the shaft seal removes the most common leak path in an industrial pump. But not every magnetic pump is built the same way, and selecting the wrong configuration for corrosive, high-p...
View More
Magnetic Pump Buying Guide: Neodymium vs. Samarium-Cobalt Magnets, Dry Run Protection, and Flow Rate Explained

21

Jul

Magnetic Pump Buying Guide: Neodymium vs. Samarium-Cobalt Magnets, Dry Run Protection, and Flow Rate Explained

Magnet selection rarely gets the attention it deserves during a magnetic pump purchase, yet it directly affects how the pump performs under heat, chemical exposure, and demagnetization risk over its service life. Combined with dry run protecti...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

portable food grade pump

Food-Safe Material Construction

Food-Safe Material Construction

The portable food grade pump utilizes premium materials specifically certified for food contact applications, ensuring absolute safety when handling consumable products. Every component that contacts liquids meets rigorous health standards and regulatory requirements established by food safety authorities worldwide. This commitment to material excellence distinguishes the portable food grade pump from general-purpose pumping equipment. Operators gain confidence knowing that beverages, sauces, oils, and ingredients remain completely uncontaminated throughout the transfer process. The food-grade certification eliminates concerns about chemical leaching or material degradation that could compromise product quality. This fundamental feature proves essential for facilities required to maintain comprehensive documentation of food safety compliance. The portable food grade pump's construction protects both the product integrity and the business reputation, making it an indispensable investment for professional food operations.
Portability and Flexible Deployment

Portability and Flexible Deployment

The portable food grade pump's lightweight design and compact dimensions enable seamless movement throughout commercial kitchens and production facilities. This mobility addresses real operational challenges by allowing staff to position equipment exactly where needed, whether transferring ingredients between storage areas, filling containers at service lines, or supporting special event catering requirements. The portable food grade pump eliminates fixed installation limitations that restrict traditional pumping systems to permanent locations. Operators appreciate the flexibility to adapt their workspace configuration based on daily operational demands and seasonal production variations. Electric cord accessibility becomes the only installation requirement, dramatically reducing setup complexity compared to permanently mounted equipment. The portable food grade pump's adaptability makes it suitable for temporary installations, mobile food services, and facilities with dynamic workflow requirements. This operational flexibility translates directly into competitive advantages for businesses needing responsive, agile equipment solutions that accommodate changing customer demands and production schedules.
Precise Control and Consistent Performance

Precise Control and Consistent Performance

The portable food grade pump delivers exceptional precision through adjustable speed controls and pressure settings that adapt to specific ingredient requirements and operational objectives. Variable flow rate functionality enables operators to transfer delicate ingredients gently while maintaining rapid throughput for standard operations. This control capability ensures the portable food grade pump performs effectively across diverse applications, from sensitive fruit purees requiring careful handling to thick batter mixtures demanding stronger pumping force. Consistent performance prevents product degradation and maintains nutritional integrity for health-conscious food producers. Operators can program specific configurations for frequently used ingredients, streamlining operations and reducing training requirements for new staff members. The portable food grade pump's precision reduces over-pumping incidents that waste expensive ingredients and creates environmental concerns. Reliable, consistent operation minimizes equipment downtime and extends service life through reduced mechanical stress, ultimately delivering superior return on investment for food service businesses prioritizing both quality and operational efficiency.
Portable Food Grade Pump

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000