chinese magnetic pump factory
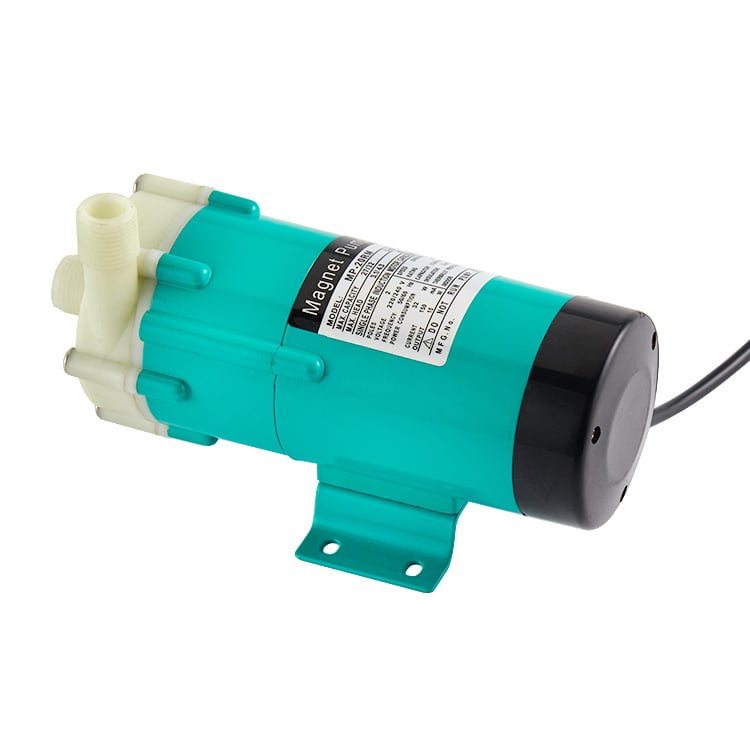
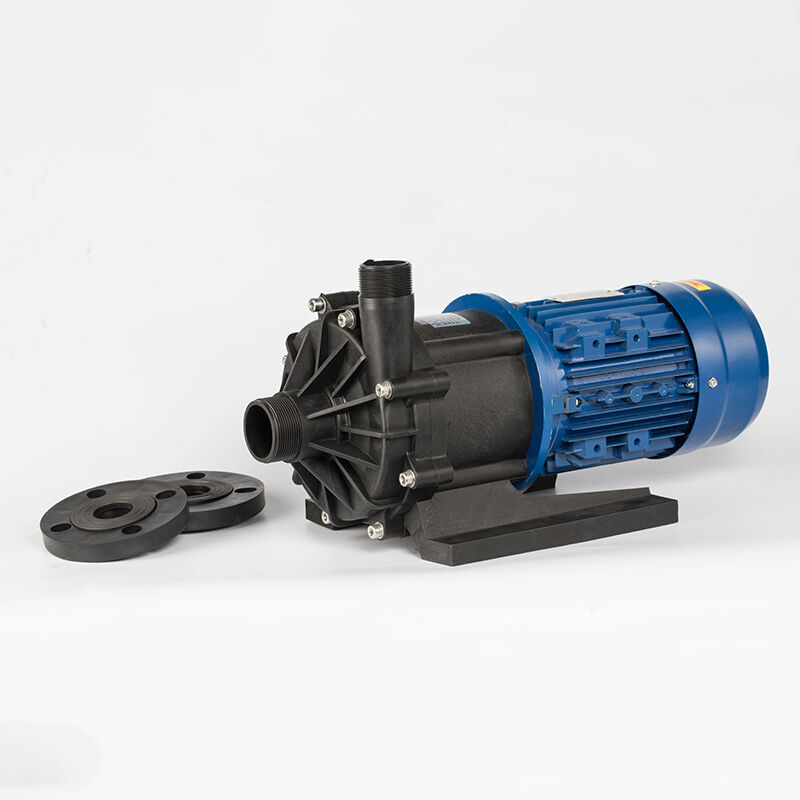
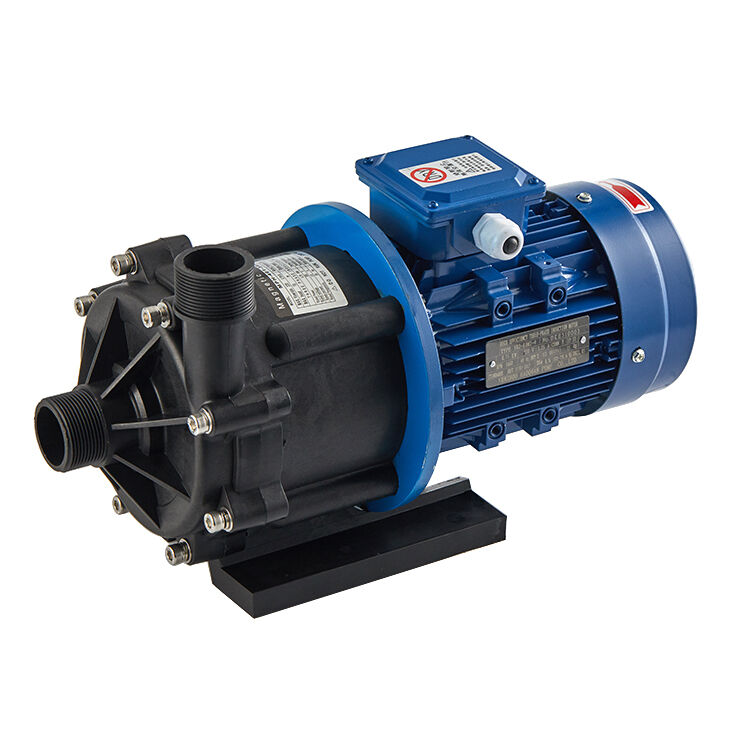
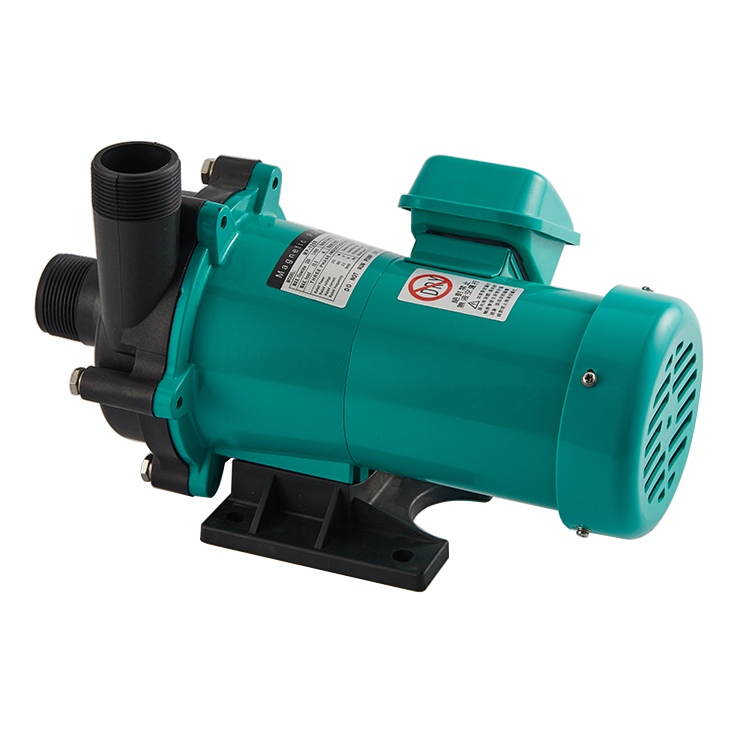
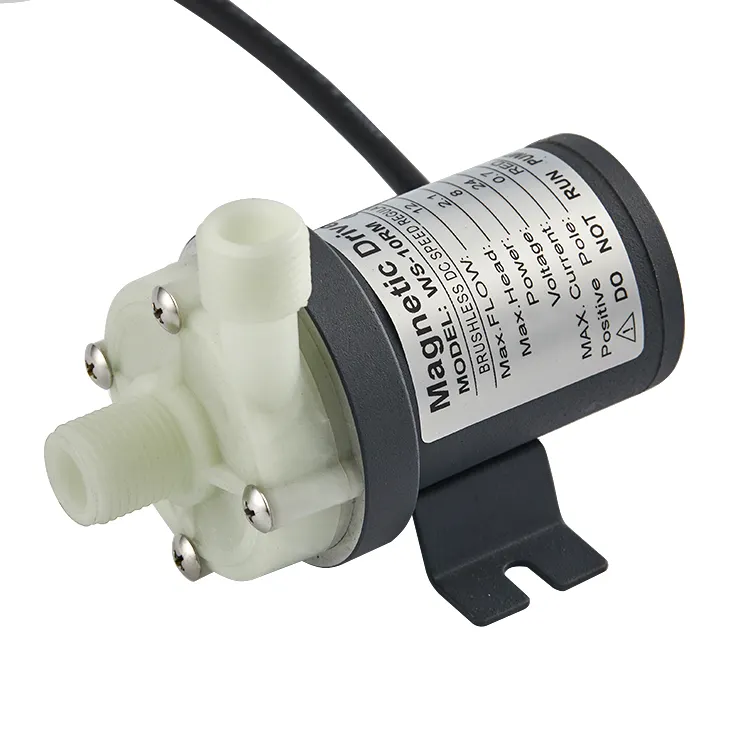
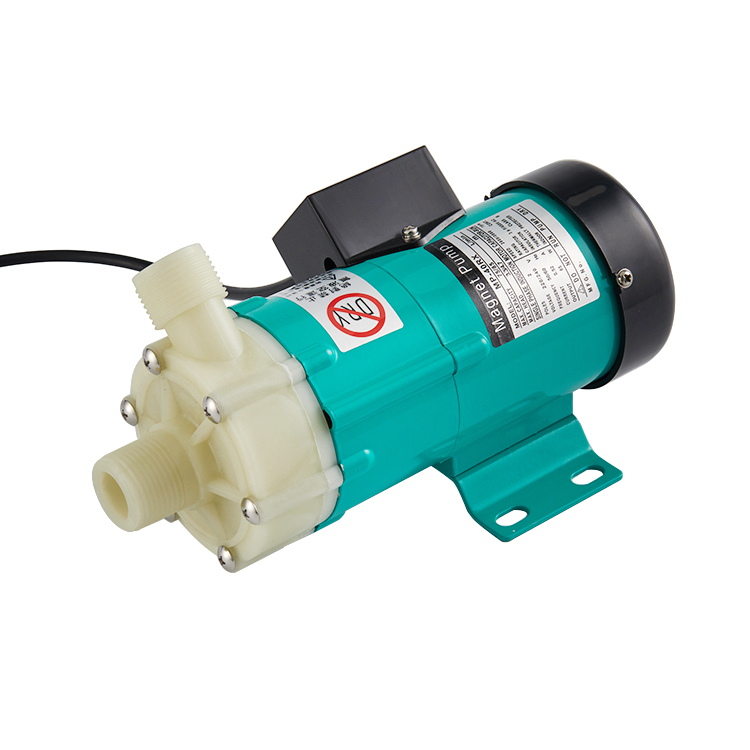
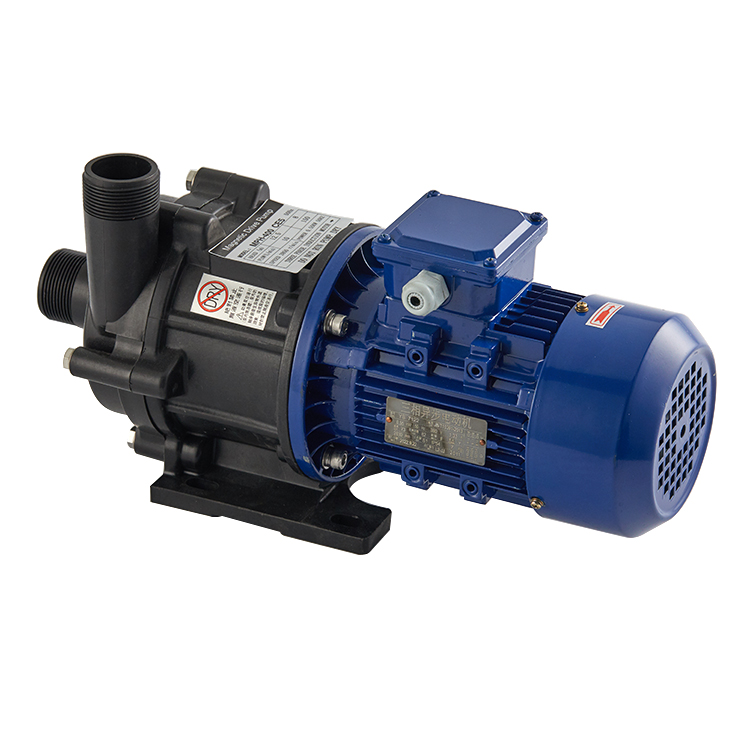
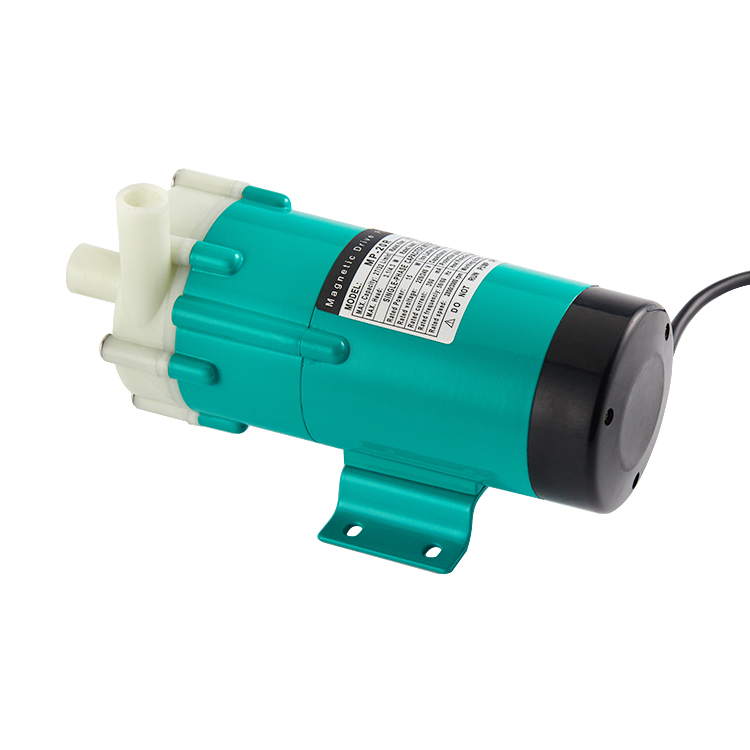
A Chinese magnetic pump factory represents a leading manufacturer specializing in advanced pumping solutions engineered with magnetic drive technology. These facilities produce high-quality magnetic pumps designed to meet diverse industrial demands across multiple sectors. The Chinese magnetic pump factory integrates cutting-edge engineering with cost-effective manufacturing processes to deliver reliable equipment.
Magnetic pumps from a Chinese magnetic pump factory operate without mechanical seals, utilizing magnetic coupling systems that eliminate fluid leakage risks. This innovative technology ensures hermetic sealing while maintaining operational efficiency. The primary function involves transferring corrosive, hazardous, or valuable fluids safely and efficiently. The Chinese magnetic pump factory manufactures pumps suitable for chemical processing, pharmaceutical production, semiconductor manufacturing, and environmental applications.
Technological features include advanced impeller designs, precision-engineered magnetic couplings, and durable materials resistant to aggressive environments. These pumps operate with minimal maintenance requirements, reducing downtime and operational costs. The factory employs sophisticated quality control systems throughout manufacturing processes. Products from the Chinese magnetic pump factory meet international standards including ISO certifications and regulatory compliance requirements.
Applications span industrial chemical transfer, pharmaceutical processing, wastewater treatment, and precision fluid handling. The Chinese magnetic pump factory continues advancing magnetic pump technology through continuous research and development initiatives. These pumps deliver superior performance characteristics, including enhanced reliability, reduced environmental contamination, and improved workplace safety. The manufacturing expertise ensures consistent product quality and long-term customer satisfaction.

 EN