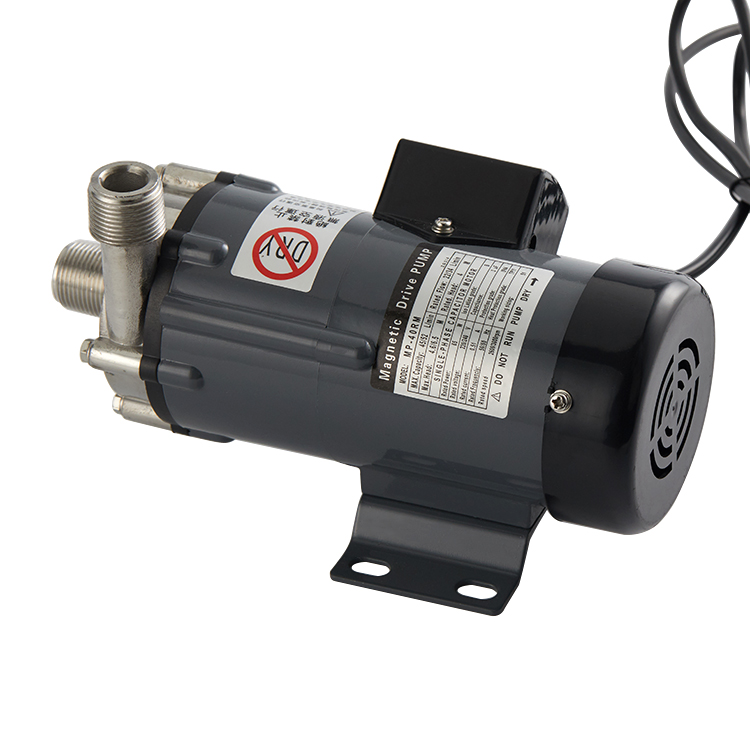
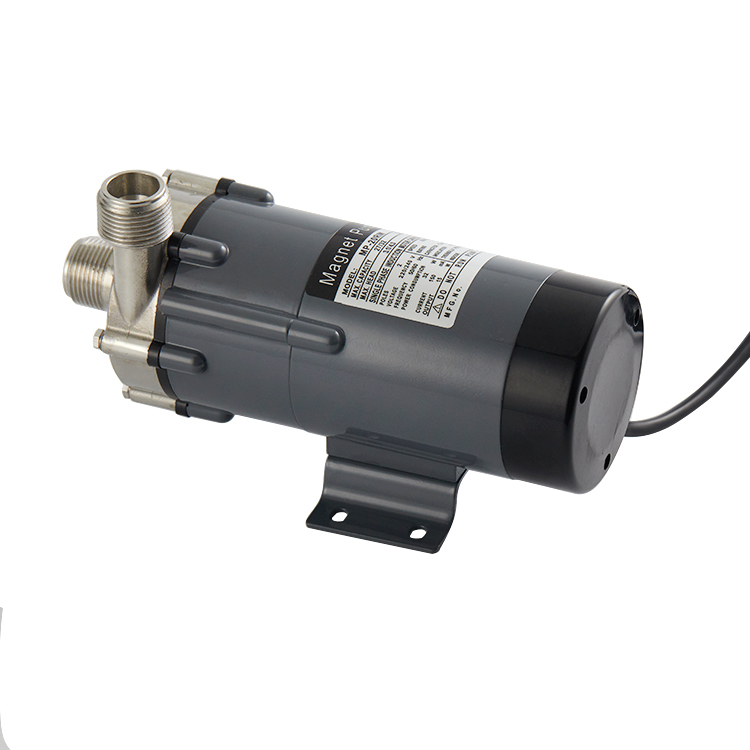
food grade brewing pump
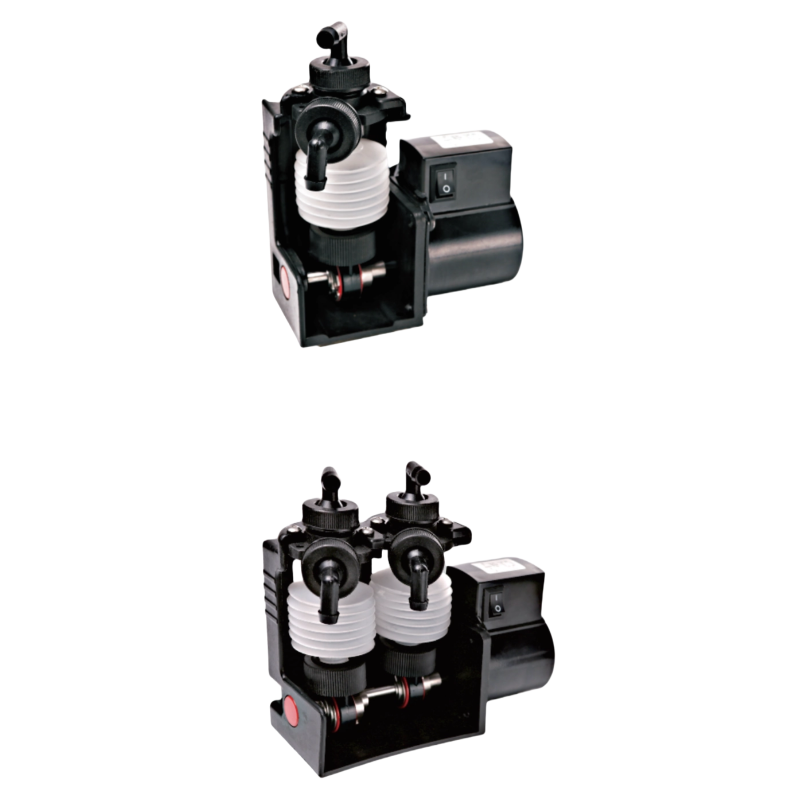
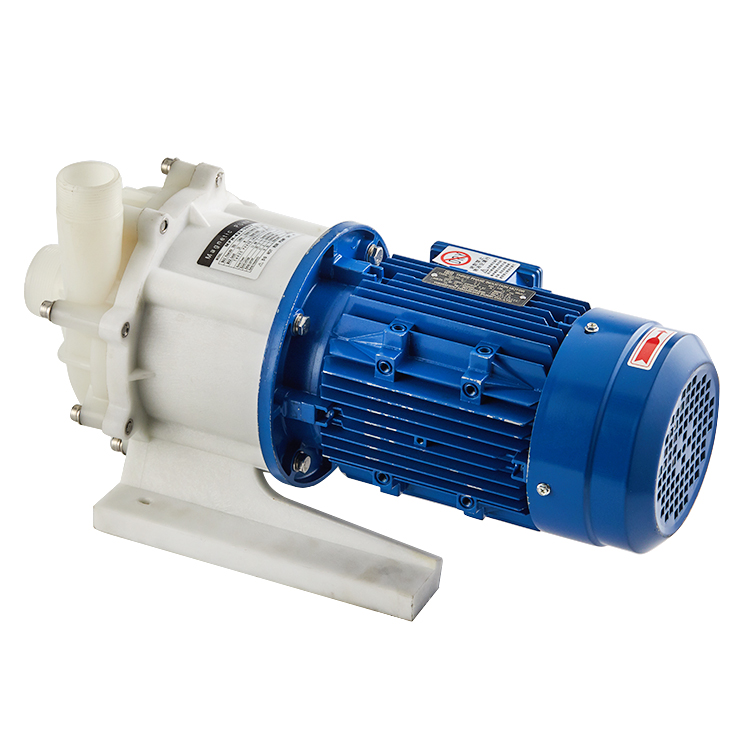
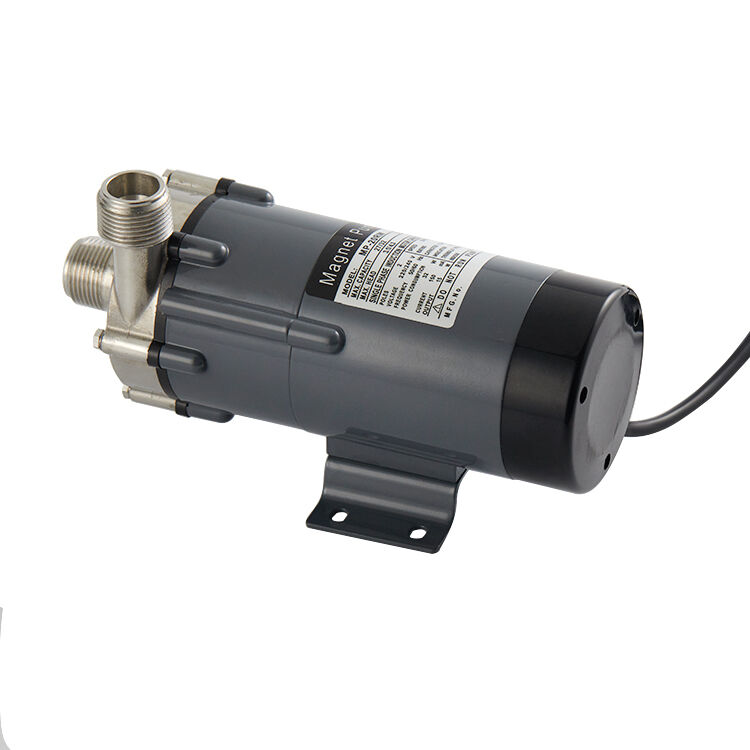
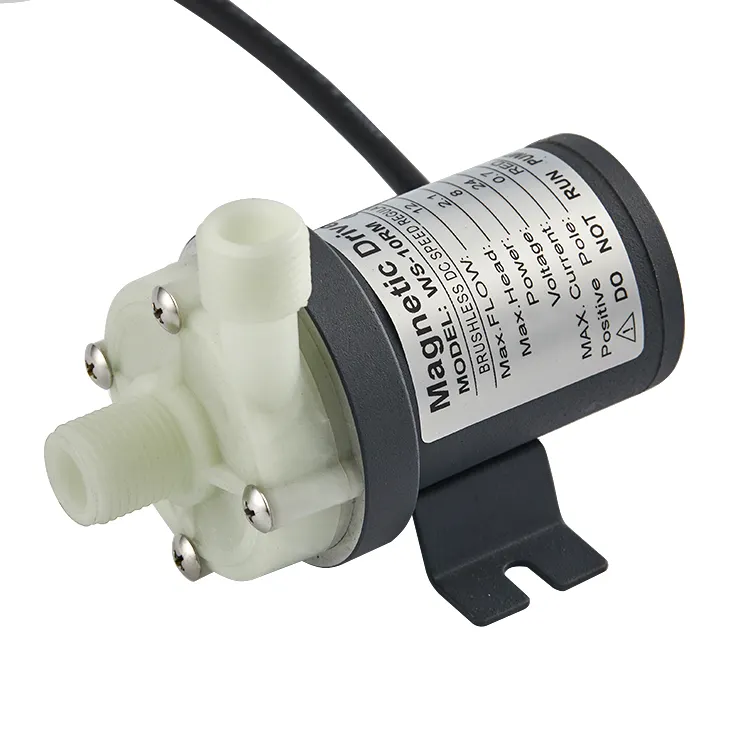
A food grade brewing pump is a specialized piece of equipment designed to transfer liquids safely during brewing operations while maintaining the highest hygiene and safety standards. This essential device functions by moving water, wort, and other brewing solutions through your brewing system with precision and reliability. The food grade brewing pump delivers consistent flow rates, ensuring uniform heat distribution and optimal extraction during the brewing process.
Modern food grade brewing pump technology incorporates stainless steel construction, food-safe materials, and advanced sealing mechanisms that prevent contamination. These pumps feature variable speed controls, allowing brewers to adjust flow rates according to specific recipe requirements and mashing schedules. The design ensures minimal product degradation while maintaining sterile conditions throughout the transfer process.
Applications for a food grade brewing pump extend across craft breweries, commercial brewing facilities, brewpubs, and homebrew operations. Whether you need to recirculate mash, transfer hot wort, or fill fermentation vessels, a food grade brewing pump provides reliable performance. These pumps are equally suitable for cold water transfers and hot liquid applications, making them versatile additions to any brewing setup. Professional breweries depend on food grade brewing pump systems to maintain consistency, improve efficiency, and meet strict food safety regulations. The equipment's durability and food-safe certification make it an investment in both quality and compliance.

 EN