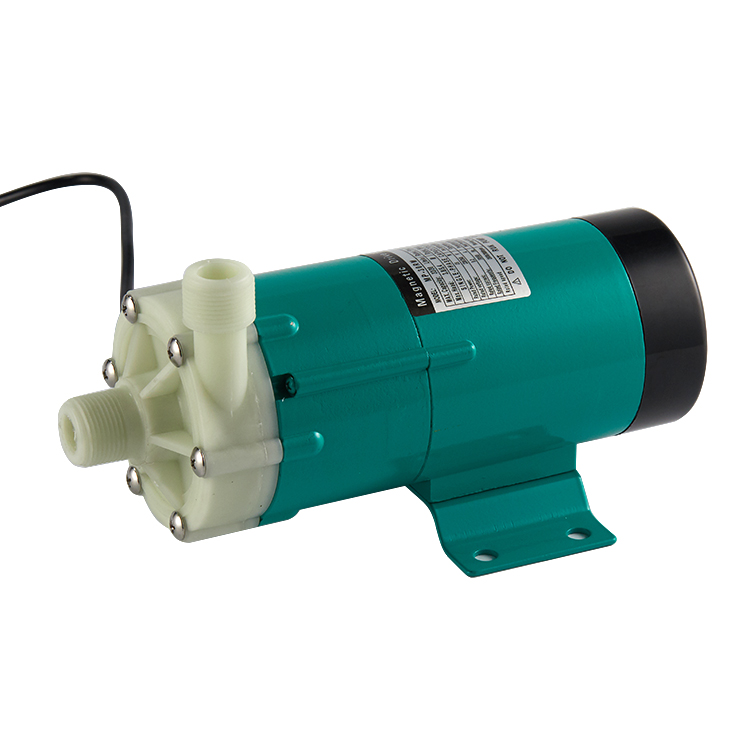
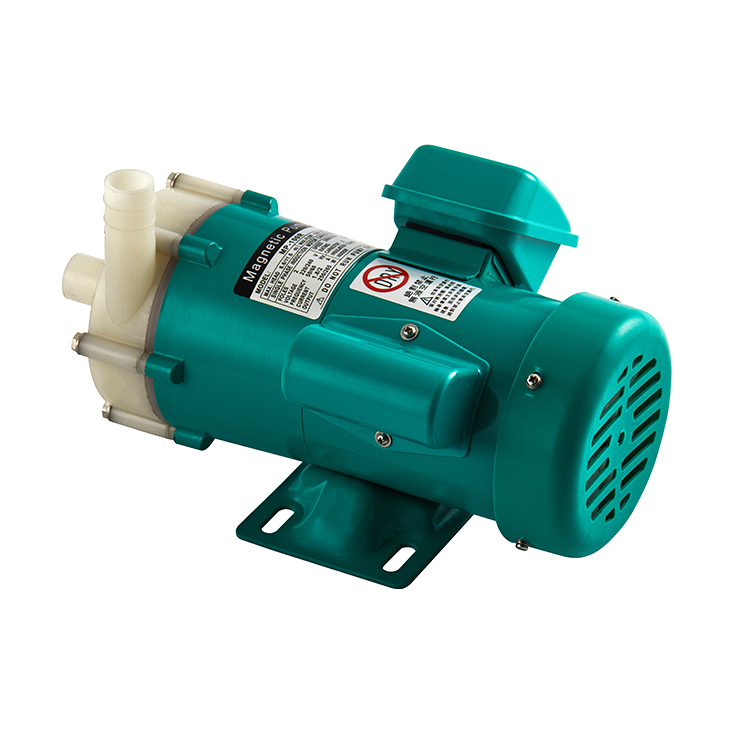
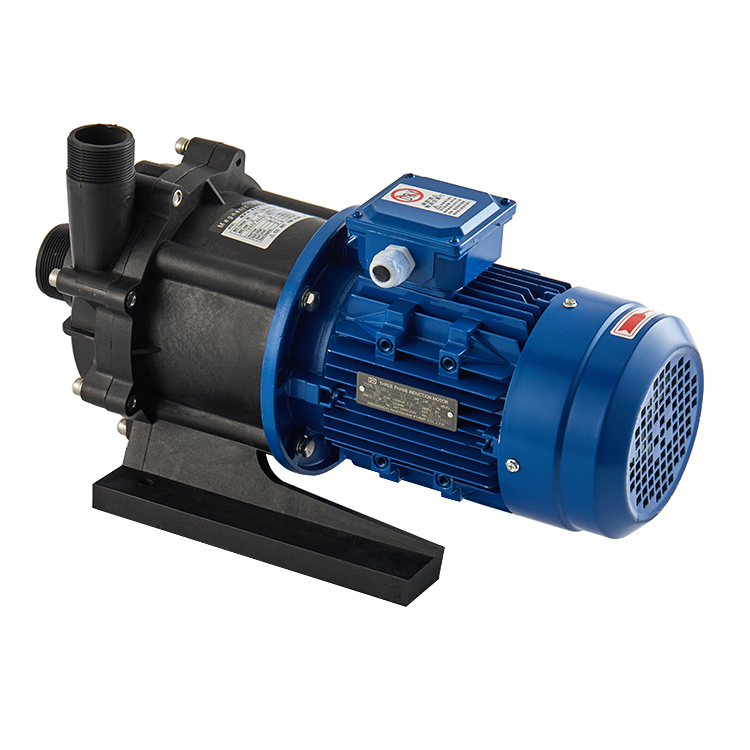
chemical pump for acid transfer
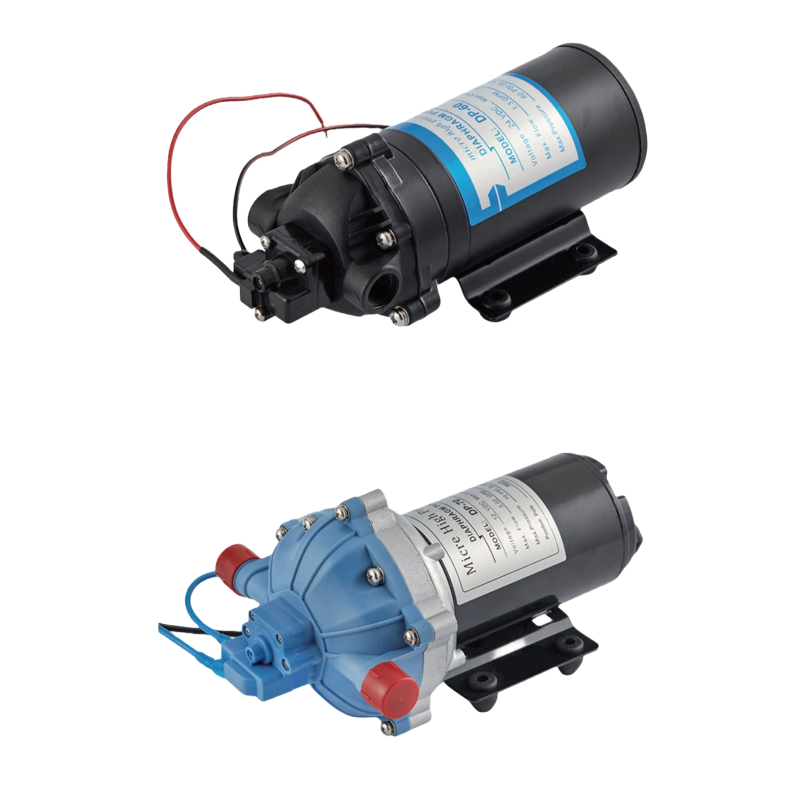
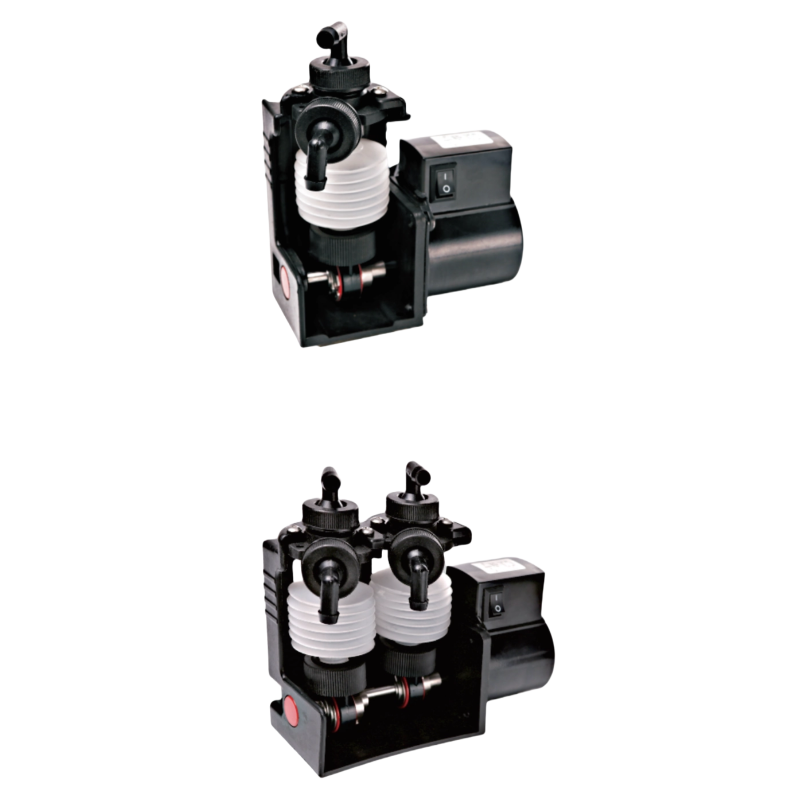
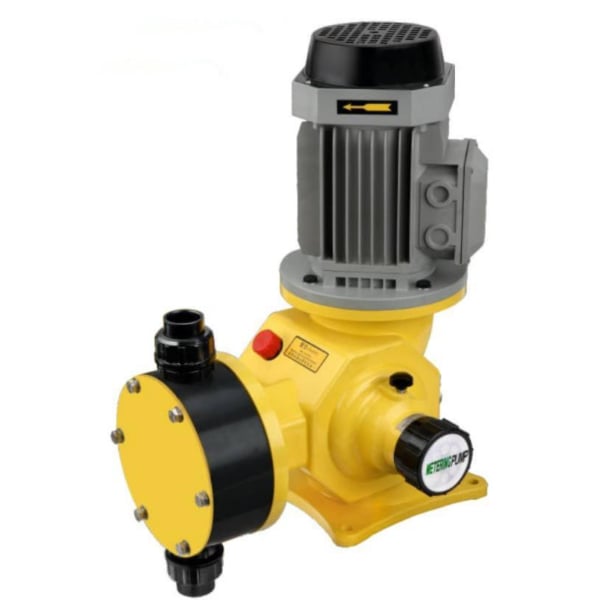
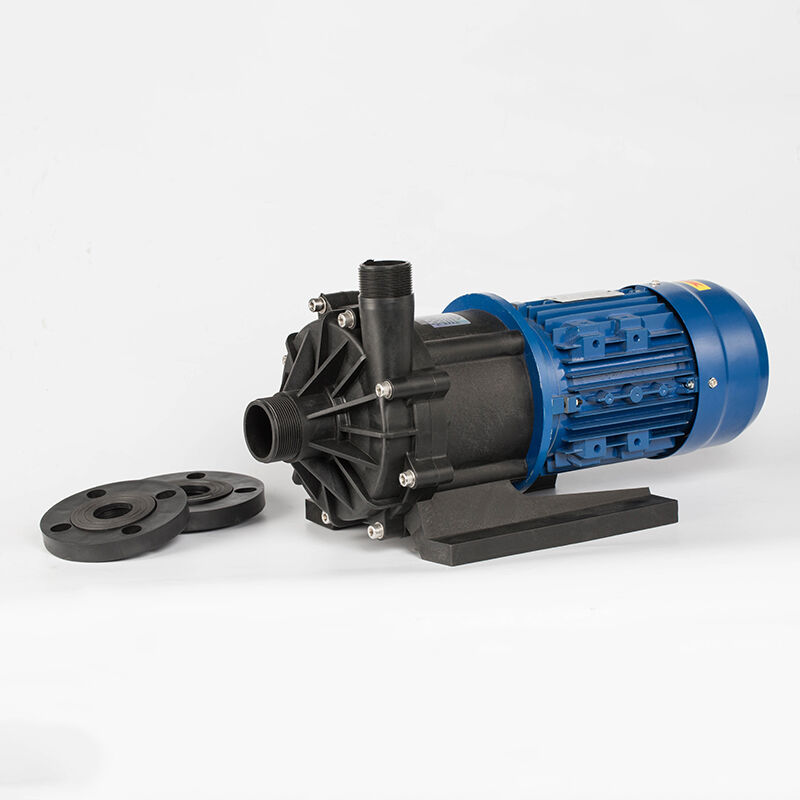
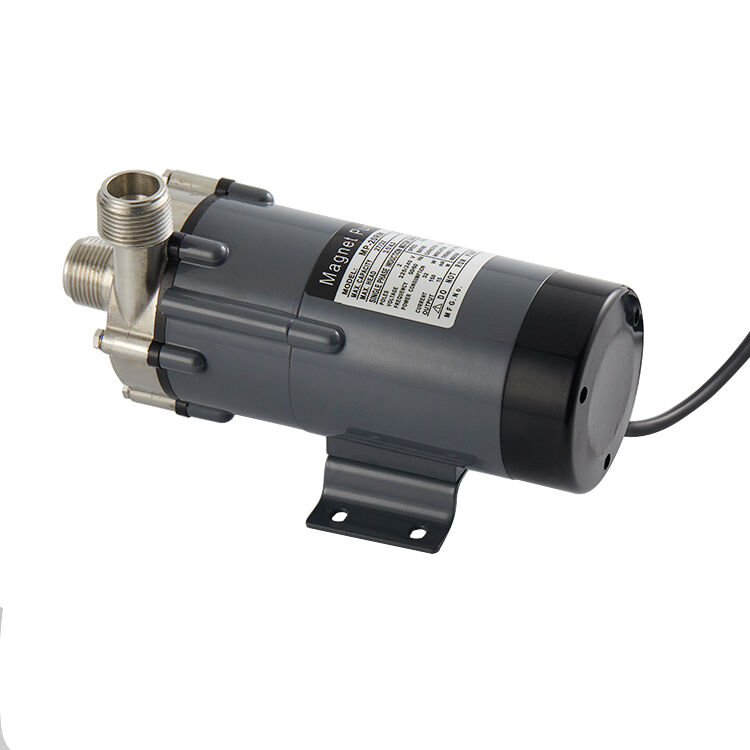
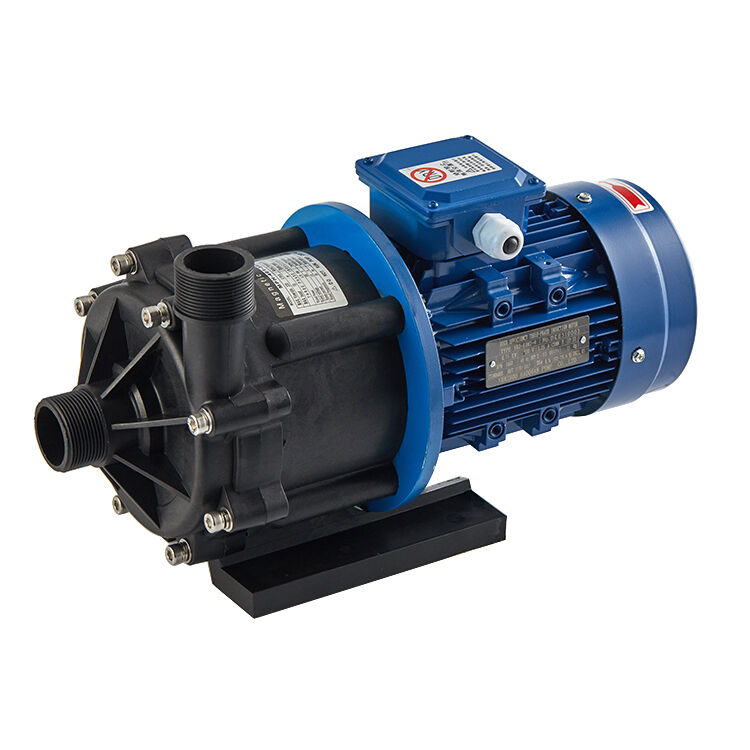
A chemical pump for acid transfer represents a specialized industrial solution designed to safely and efficiently move corrosive liquid substances through processing systems. This equipment plays a critical role in various manufacturing environments where handling aggressive chemicals demands reliable performance and robust construction. The chemical pump for acid transfer utilizes advanced engineering principles to ensure leak-free operations while maintaining consistent flow rates across diverse applications.
The primary function of a chemical pump for acid transfer involves transporting corrosive acids such as sulfuric acid, hydrochloric acid, and phosphoric acid from storage containers to processing stations. These pumps feature specialized materials including Teflon, polypropylene, and fluoropolymer coatings that resist chemical degradation and corrosion. The chemical pump for acid transfer operates with precision mechanical seals and reinforced impellers designed specifically to withstand the aggressive nature of acidic environments.
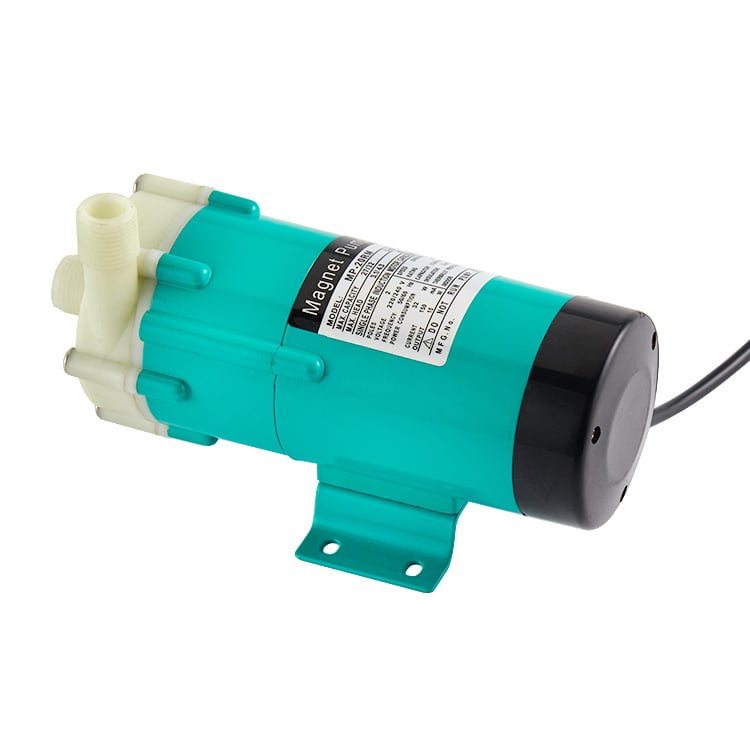
Technologically, modern chemical pump for acid transfer systems incorporate variable speed drives, integrated monitoring systems, and automatic shut-off mechanisms to prevent overflow and spillage. These pumps deliver exceptional durability through magnetic drive technology that eliminates traditional shaft seals, reducing maintenance requirements significantly. Applications span across chemical manufacturing, water treatment facilities, pharmaceutical production, metal processing, and battery production industries where acid transfer remains essential to operational success.

 EN