Chemical Pump for Bleach | Safe Dosing Solutions

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

chemical pump for bleach

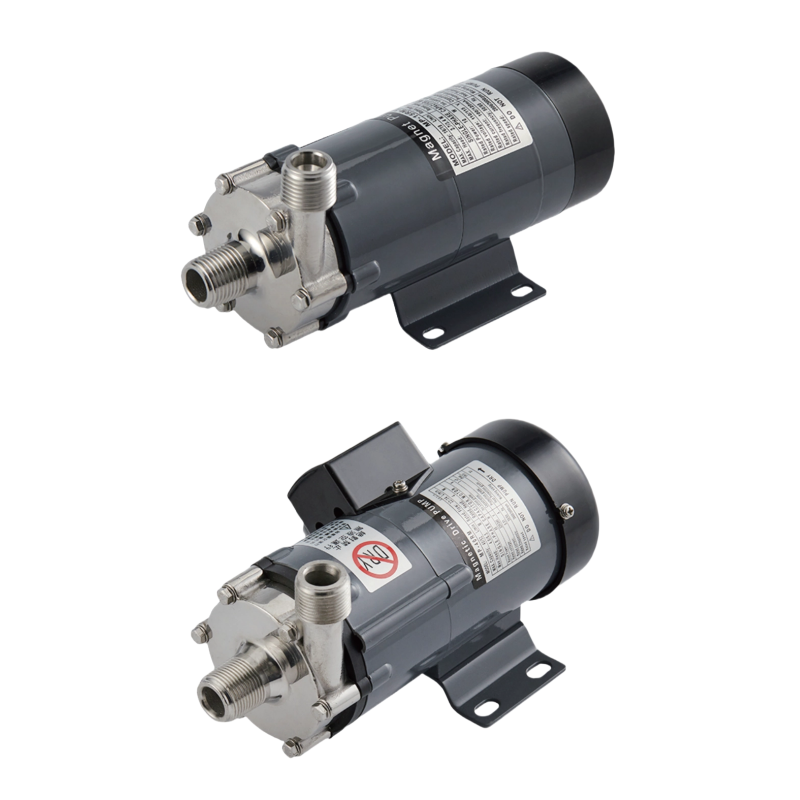
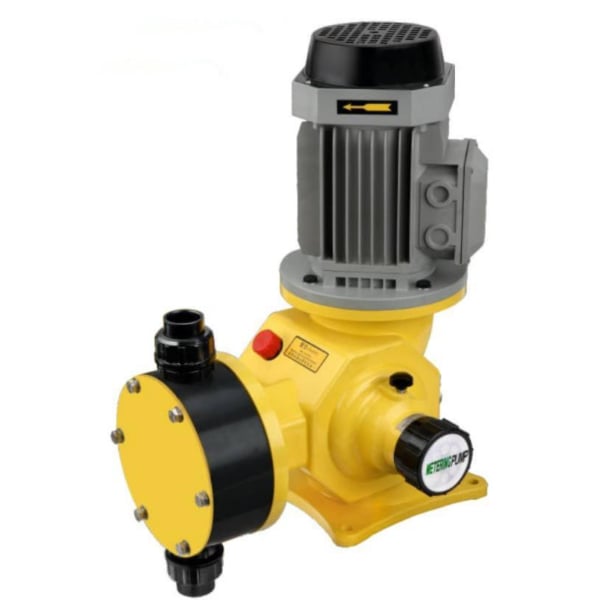
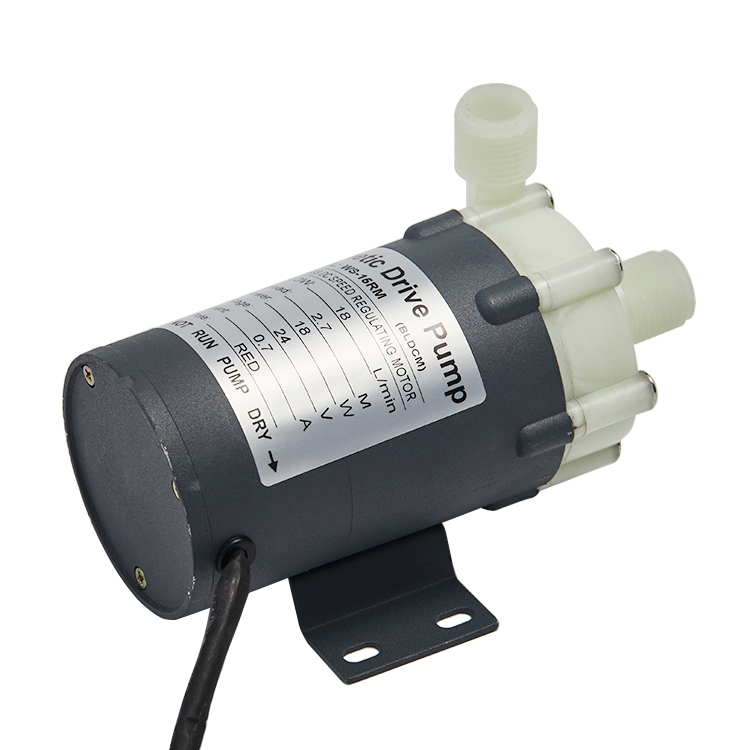
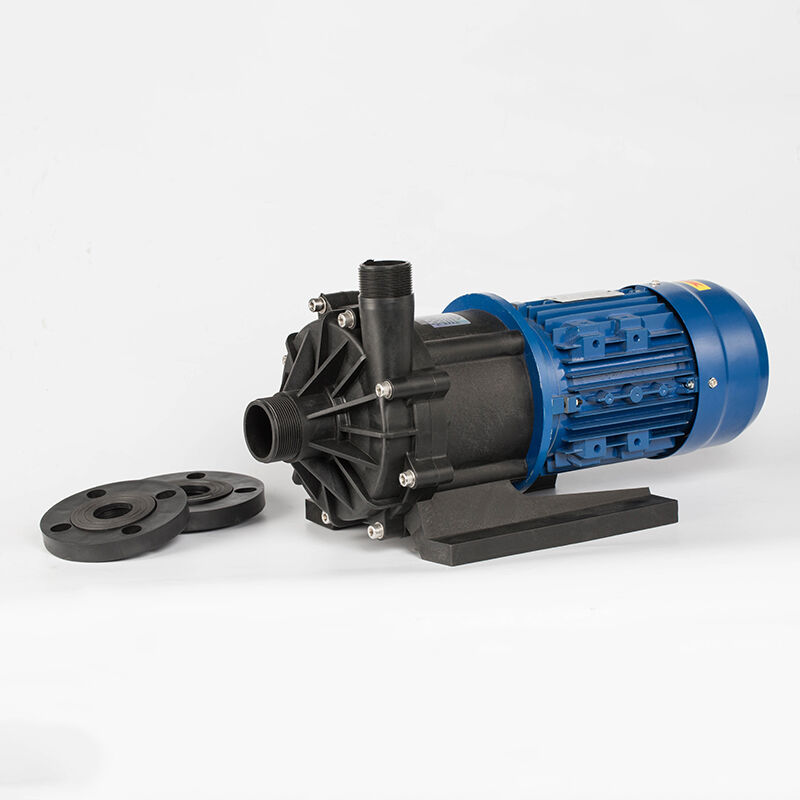
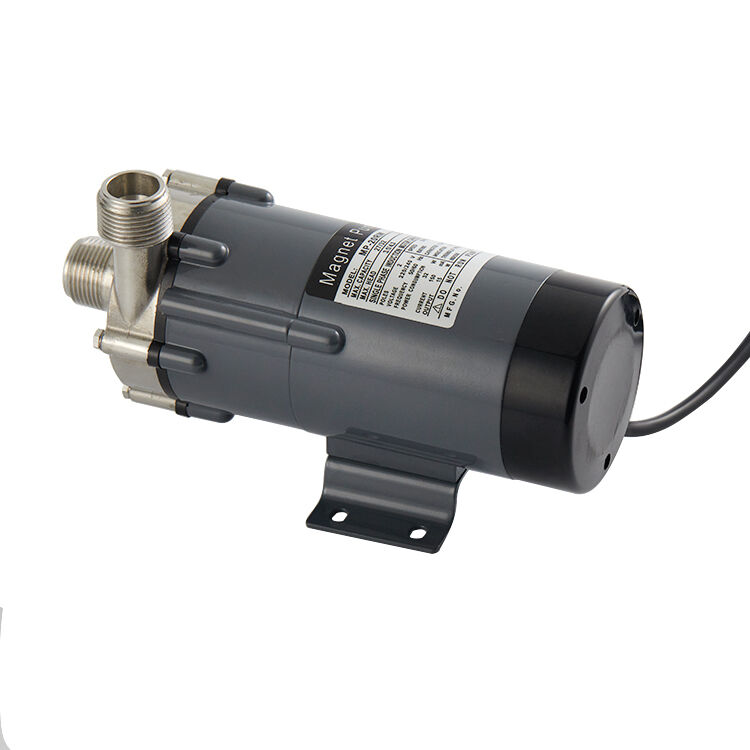
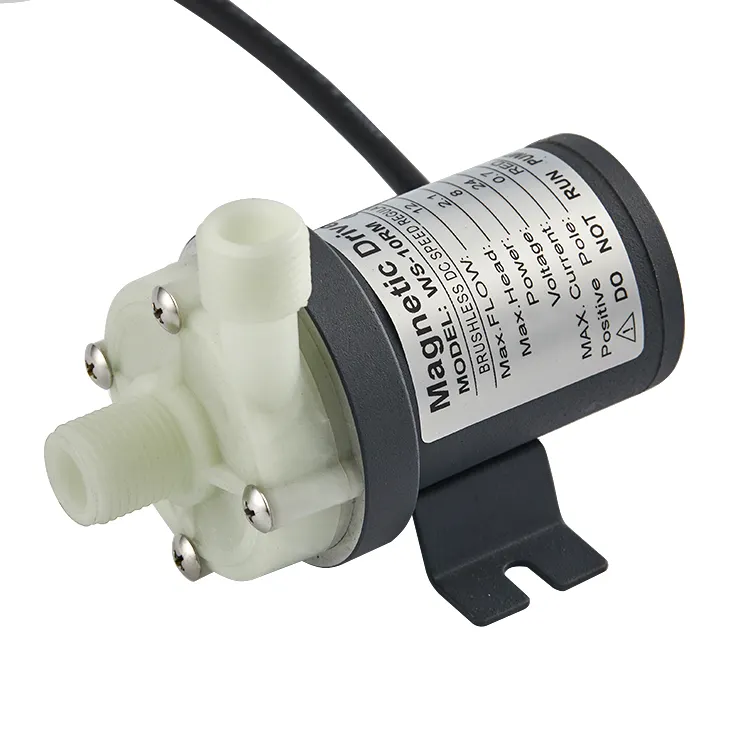
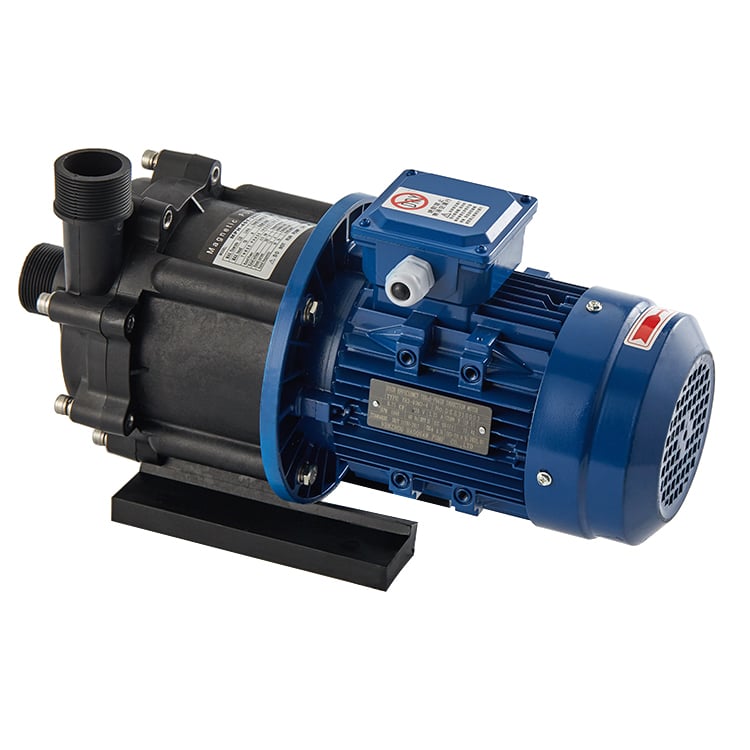
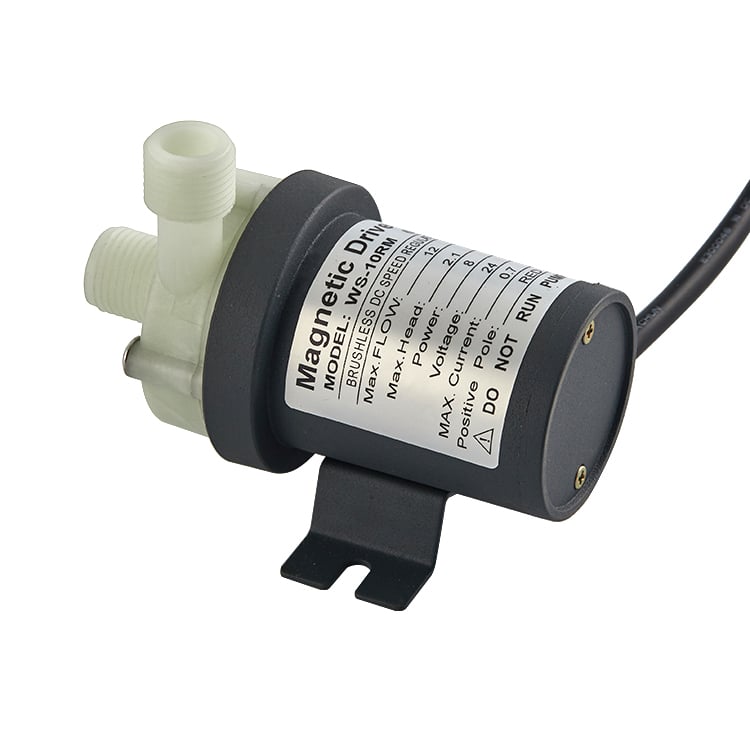
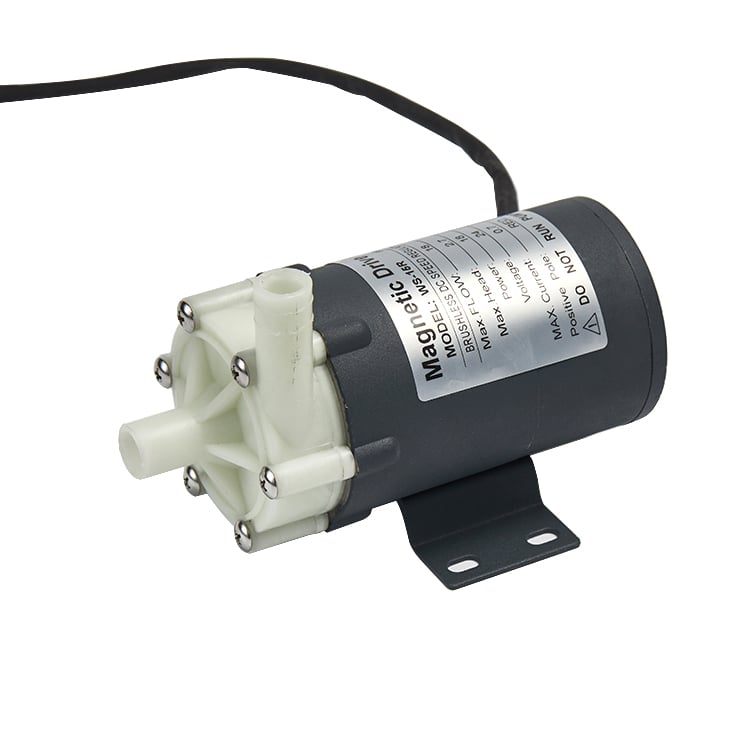
A chemical pump for bleach is a specialized industrial or household device designed to safely dispense, transfer, and distribute bleach solutions with precision and consistency. This chemical pump for bleach serves critical functions across multiple applications, from water treatment facilities to cleaning operations and disinfection processes. The primary function of a chemical pump for bleach involves metering accurate quantities of bleach while maintaining system integrity and preventing corrosive damage to equipment components. Technological features of a modern chemical pump for bleach include corrosion-resistant materials such as polypropylene, PVDF, or specialized elastomers that withstand bleach's aggressive chemical properties. These pumps utilize peristaltic or diaphragm pump technology, which eliminates contact between bleach and metal components, significantly extending equipment lifespan. Variable speed controls enable operators to adjust flow rates according to specific requirements, while integrated safety mechanisms prevent overfilling and backflow situations. Applications for a chemical pump for bleach extend throughout industrial, commercial, and residential sectors. Water treatment plants employ these pumps for disinfection and sterilization processes. Swimming pool maintenance operations depend on precise bleach dosing to maintain safe water chemistry. Food processing facilities utilize chemical pump for bleach systems to sanitize equipment and surfaces. Healthcare facilities and laboratories use these pumps for sterilization protocols. Residential cleaning operations benefit from automated chemical pump for bleach distribution, reducing manual handling risks and ensuring consistent results across multiple cleaning tasks.

New Product Recommendations

Choosing a chemical pump for bleach delivers substantial operational and safety benefits that directly improve your workplace efficiency and protect your team. The primary advantage of a chemical pump for bleach lies in its ability to eliminate dangerous manual handling of corrosive substances. Workers avoid direct contact with bleach, dramatically reducing chemical burn injuries and inhalation hazards that commonly occur during traditional pouring or spraying methods.

Operational efficiency improves remarkably when you implement a chemical pump for bleach system. Automated dispensing ensures consistent dosing every single time, removing human error from your disinfection or cleaning processes. This precision reduces chemical waste significantly, lowering your operational costs while delivering superior results. A chemical pump for bleach operates continuously without fatigue, maintaining steady performance across extended shifts and demanding applications.

The durability of a quality chemical pump for bleach represents exceptional value for your investment. Corrosion-resistant construction withstands bleach's destructive properties indefinitely, preventing premature equipment failure that plagued older pumping solutions. You'll experience fewer maintenance interruptions and extended service intervals, keeping your operations running smoothly without unexpected downtime. Compatibility advantages emerge when selecting a chemical pump for bleach designed for your specific application. These pumps integrate seamlessly into existing water treatment infrastructure, pool systems, or industrial cleaning operations. Flexible installation options accommodate various facility layouts and configurations. Most importantly, regulatory compliance becomes automatic with a certified chemical pump for bleach system, satisfying safety standards and environmental requirements without additional modifications or expensive retrofitting projects.

Tips And Tricks

2026 BLDC Pump Guide: Top Models and Features

09

Jun

2026 BLDC Pump Guide: Top Models and Features

The bldc pump has emerged as one of the most technically advanced fluid-handling solutions available to engineers and procurement professionals entering 2026. Driven by brushless direct current motor technology, these pumps deliver a compelling combi...
View More
Smart Dosing Systems: Integrating Precision Pumps into Automated Production Lines

09

Jun

Smart Dosing Systems: Integrating Precision Pumps into Automated Production Lines

Introduction: The Evolution of Fluid Handling in Industry 4.0 The Fourth Industrial Revolution, or Industry 4.0, is fundamentally reshaping how factories operate. At the heart of this transformation is the shift from manual, isolated processes to int...
View More
A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

09

Jun

A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

Introduction For international B2B buyers, selecting a pump supplier in China is a critical decision that impacts long-term operational costs and product reliability. While high-quality marketing materials and competitive pricing are common, they do ...
View More
8 Benefits of Magnetic Pumps in Pharmaceutical and Semiconductor Manufacturing: Leak-Free, Contamination-Free Operation

21

Jul

8 Benefits of Magnetic Pumps in Pharmaceutical and Semiconductor Manufacturing: Leak-Free, Contamination-Free Operation

Pharmaceutical and semiconductor manufacturing share a demanding requirement that few other industries face simultaneously: absolute containment and absolute purity. A single leak or contamination event can compromise an entire batch, trigger regulat...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

chemical pump for bleach

Superior Corrosion Resistance for Long-Term Reliability

Superior Corrosion Resistance for Long-Term Reliability

A chemical pump for bleach constructed from advanced materials like PVDF and polypropylene withstands bleach's corrosive nature indefinitely without degradation. Unlike standard pumps that deteriorate rapidly when exposed to bleach, a properly engineered chemical pump for bleach maintains structural integrity through years of continuous operation. This exceptional corrosion resistance translates directly into lower replacement costs and minimal maintenance requirements. Facility managers benefit from extended service life that far surpasses conventional pumping equipment. The robust construction of a chemical pump for bleach prevents leaks and seal failures that contaminate surrounding areas and create safety hazards. Investment protection becomes reality when you choose a chemical pump for bleach specifically designed for bleach applications, delivering reliability that justifies premium pricing through years of trouble-free performance.
Precise Metering and Chemical Accuracy

Precise Metering and Chemical Accuracy

Accurate chemical dosing separates professional bleach treatment from inconsistent results, and a chemical pump for bleach delivers precision that manual methods cannot match. Variable flow rate controls enable operators to calibrate a chemical pump for bleach to exact specifications, whether treating large municipal water systems or maintaining residential pool chemistry. This precision ensures optimal disinfection without chemical waste or overdosing problems. A chemical pump for bleach with electronic controls allows programmable settings, enabling automated scheduling across multiple treatment cycles. Consistent dosing improves treatment effectiveness while reducing chemical consumption and associated costs. Healthcare facilities and food processing plants particularly value the reliability of a chemical pump for bleach that guarantees uniform sanitization across all treated surfaces and systems. Smart monitoring systems integrated into modern chemical pump for bleach designs provide real-time data validation, alerting operators to any deviations from programmed parameters.
Enhanced Safety and Worker Protection

Enhanced Safety and Worker Protection

Chemical safety fundamentally improves when operations transition from manual bleach handling to an automated chemical pump for bleach system. Workers eliminate exposure to hazardous fumes and direct contact with concentrated solutions when using a chemical pump for bleach, reducing occupational injuries and health risks substantially. Enclosed distribution systems prevent accidental splashes and spills that create dangerous work environments. A chemical pump for bleach installed in a properly ventilated location contains chemical hazards effectively, protecting nearby personnel and equipment. Emergency shut-off capabilities integrated into quality chemical pump for bleach designs provide immediate response options during unexpected situations. Regulatory agencies recognize the superior safety profile of a chemical pump for bleach system, often reducing workplace inspection frequency and liability insurance premiums. Training requirements decrease significantly since operators interact with a chemical pump for bleach interface rather than raw chemicals, allowing even minimally trained staff to maintain safe operations reliably.
Chemical Pump for Bleach | Safe Dosing Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000