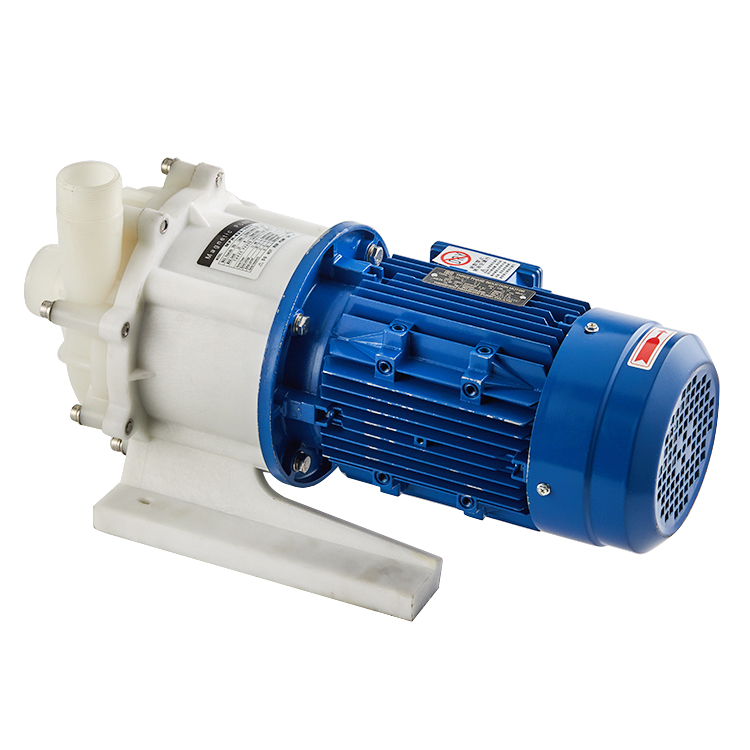
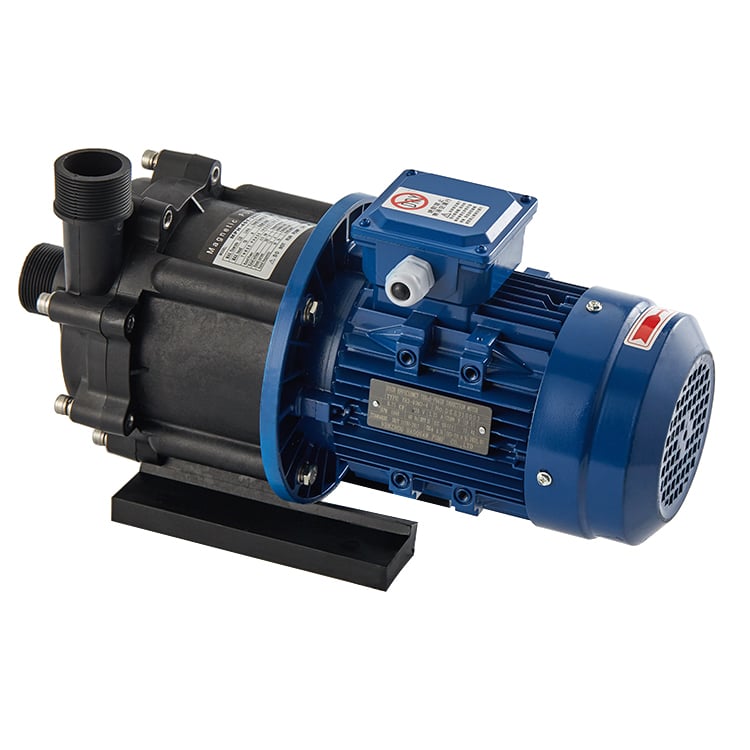
chemical pump supplier
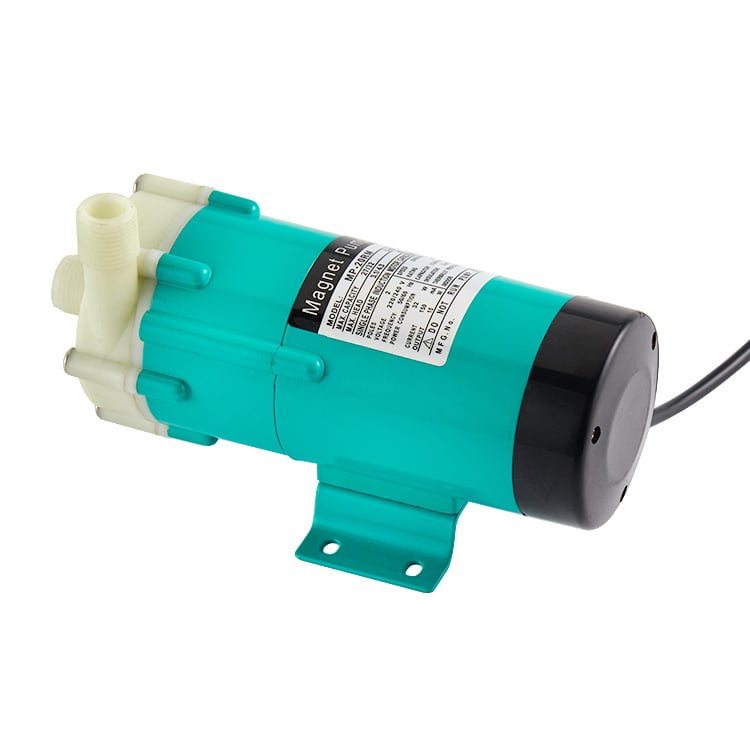
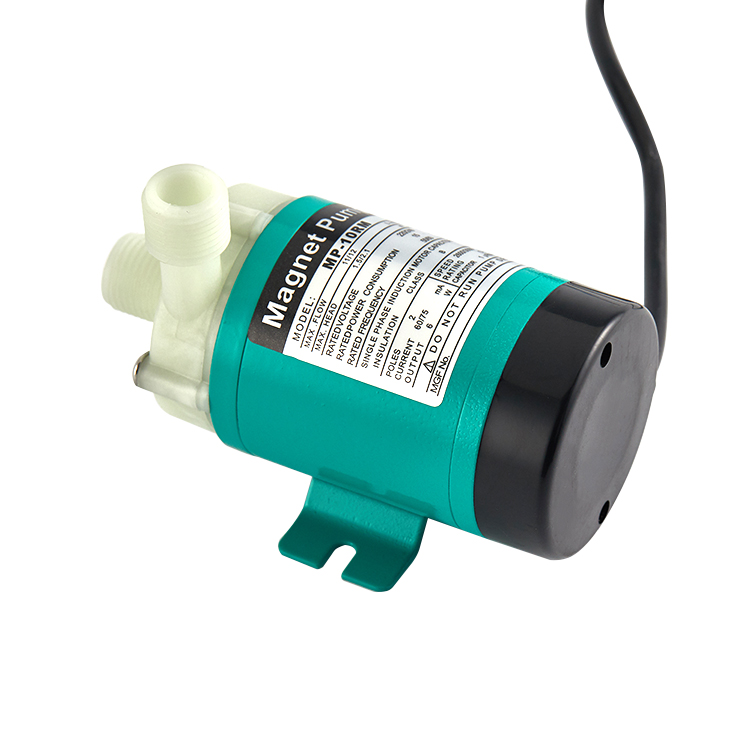
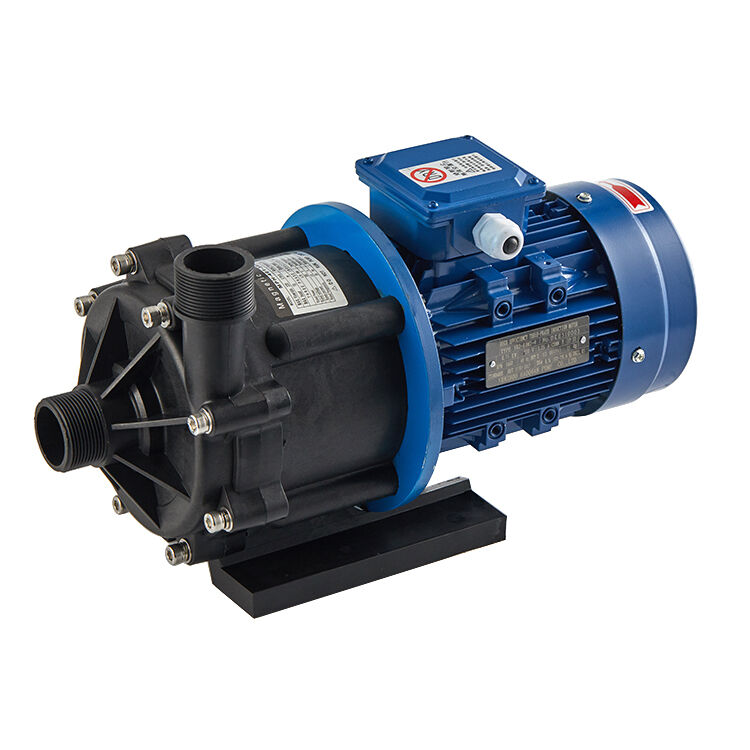
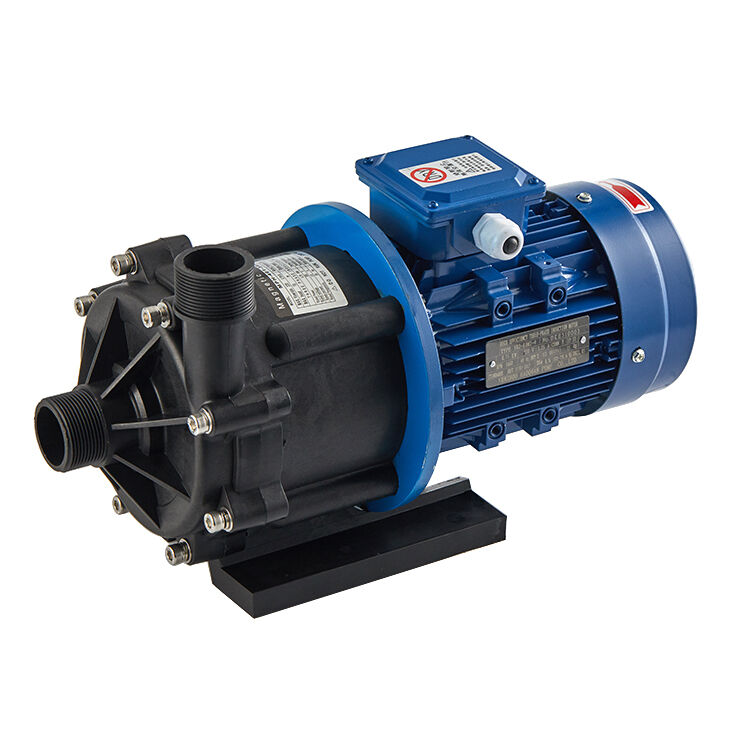
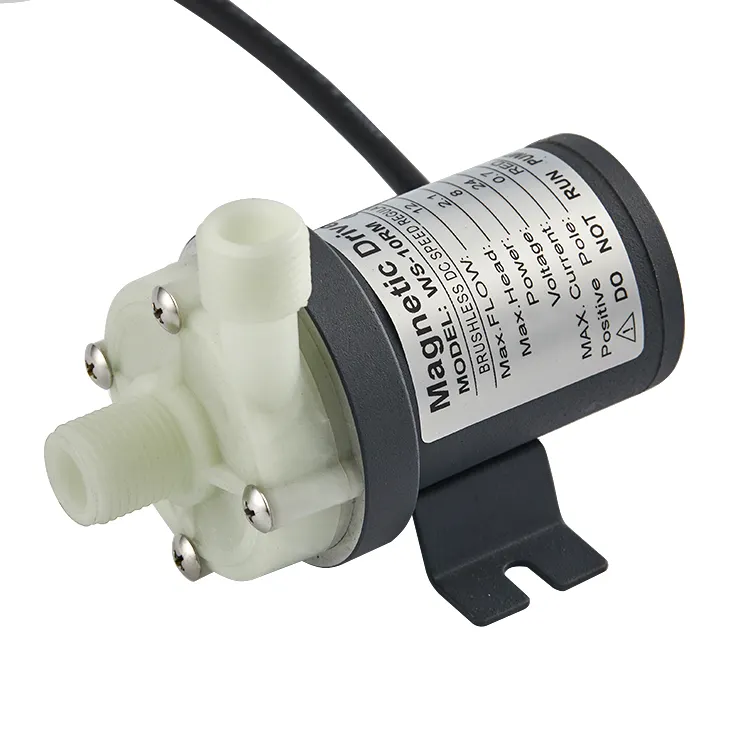
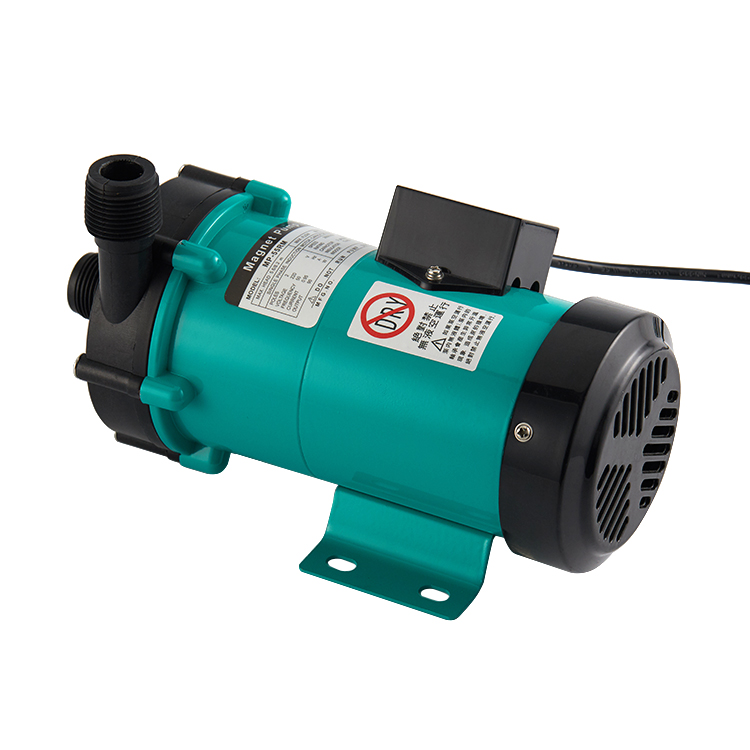
A chemical pump supplier specializes in providing durable and reliable pumping solutions designed to handle corrosive, hazardous, and specialized fluids across multiple industries. As a professional chemical pump supplier, companies deliver comprehensive systems engineered to transfer, circulate, and manage challenging chemical applications safely and efficiently. These pumps represent critical infrastructure for manufacturing operations, waste management facilities, pharmaceutical production, and chemical processing plants worldwide.
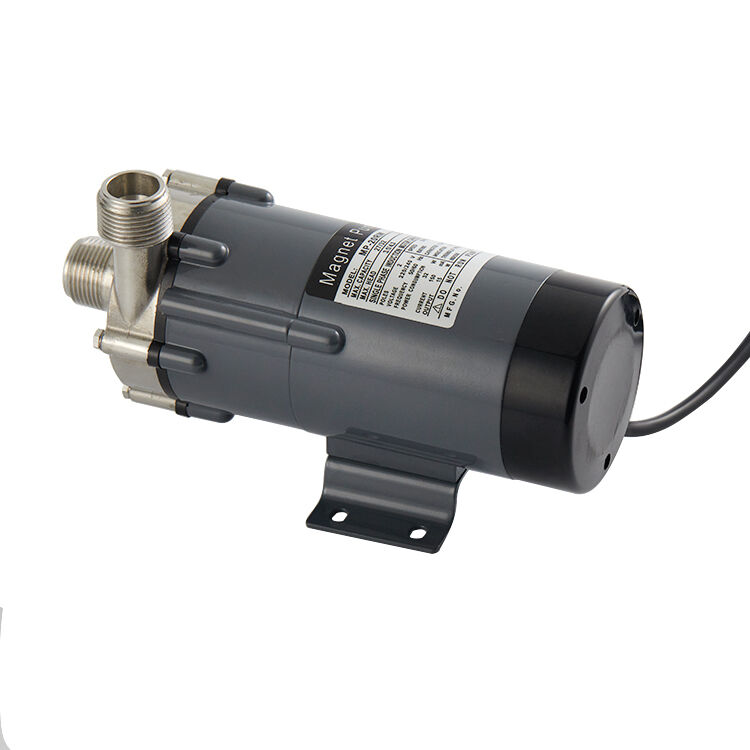
The chemical pump supplier sector offers advanced technologies including centrifugal pumps, positive displacement pumps, and specialized variants built from corrosion-resistant materials such as stainless steel, fluoropolymers, and engineered composites. These technological features enable the chemical pump supplier to address extreme pressure conditions, temperature fluctuations, and aggressive chemical environments that standard pumps cannot withstand.
Key functions include precise fluid transfer, pressure regulation, mixing operations, and containment of dangerous substances. Selecting the right chemical pump supplier ensures operational continuity, regulatory compliance, and worker safety. Modern chemical pump suppliers integrate smart monitoring systems, predictive maintenance capabilities, and IoT connectivity to optimize performance and reduce downtime. Applications span petrochemicals, water treatment, semiconductor manufacturing, food processing, and laboratory operations. The chemical pump supplier industry continues evolving with innovations in energy efficiency and environmental protection, making these solutions indispensable for contemporary industrial demands and future sustainability initiatives.

 EN