chemical pump factory
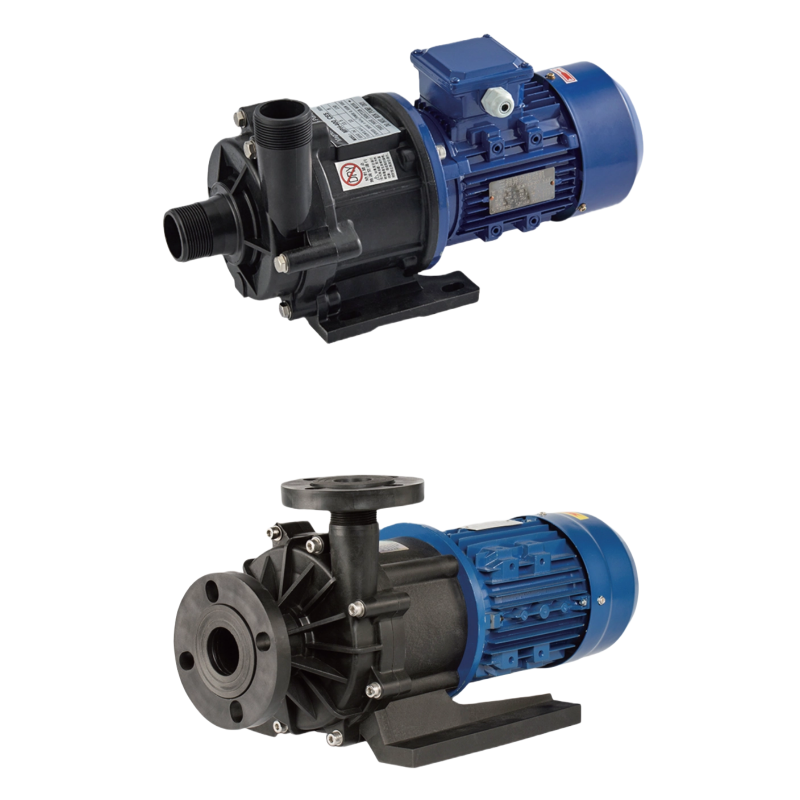
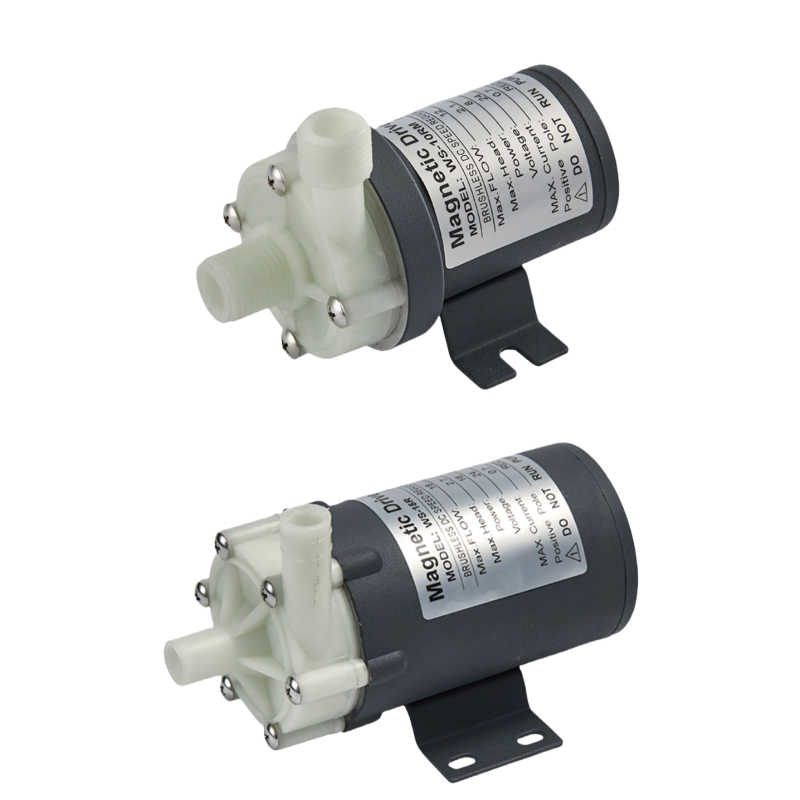
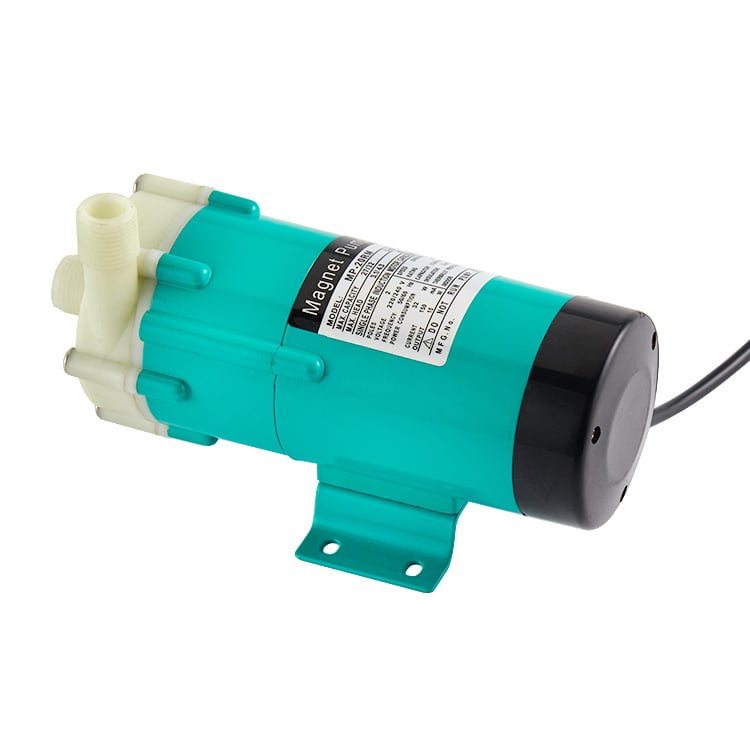
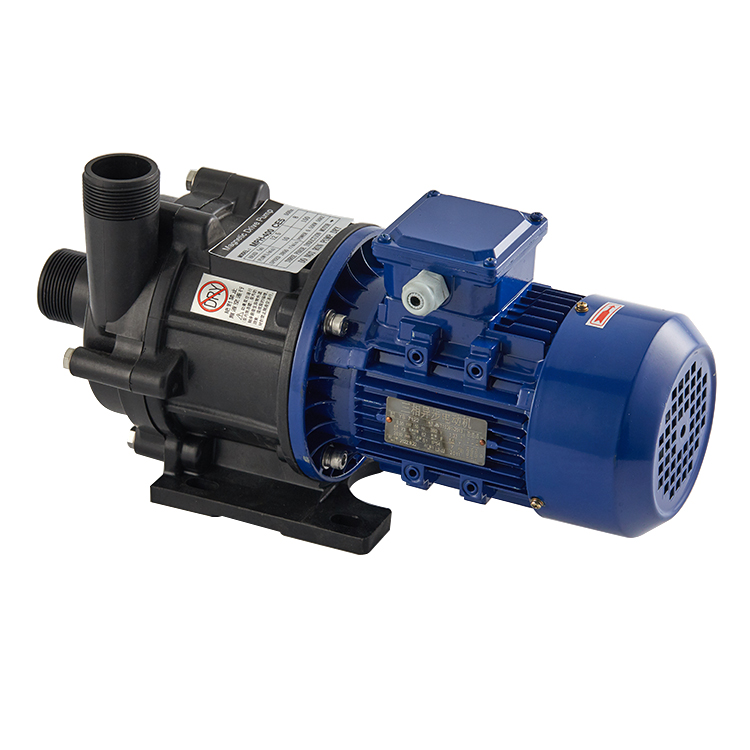
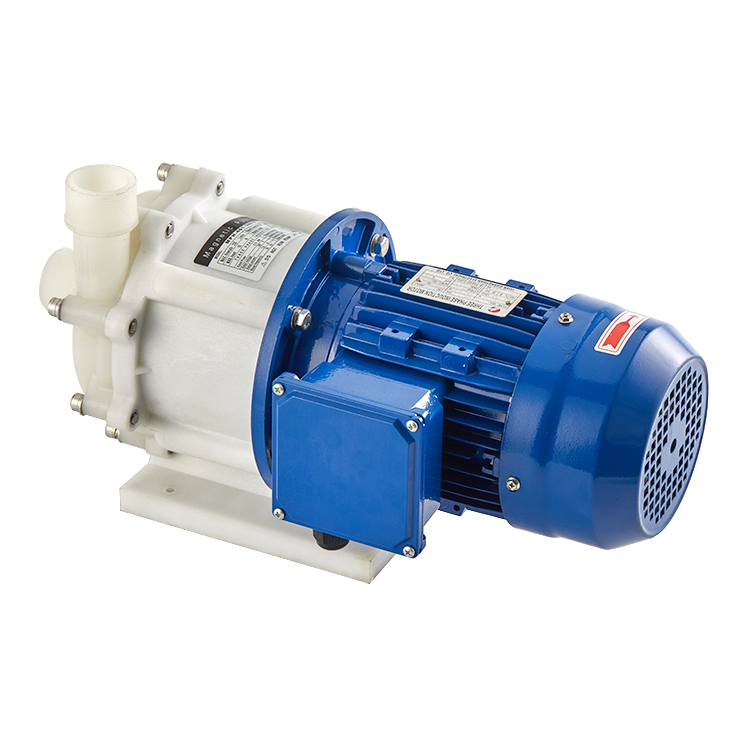
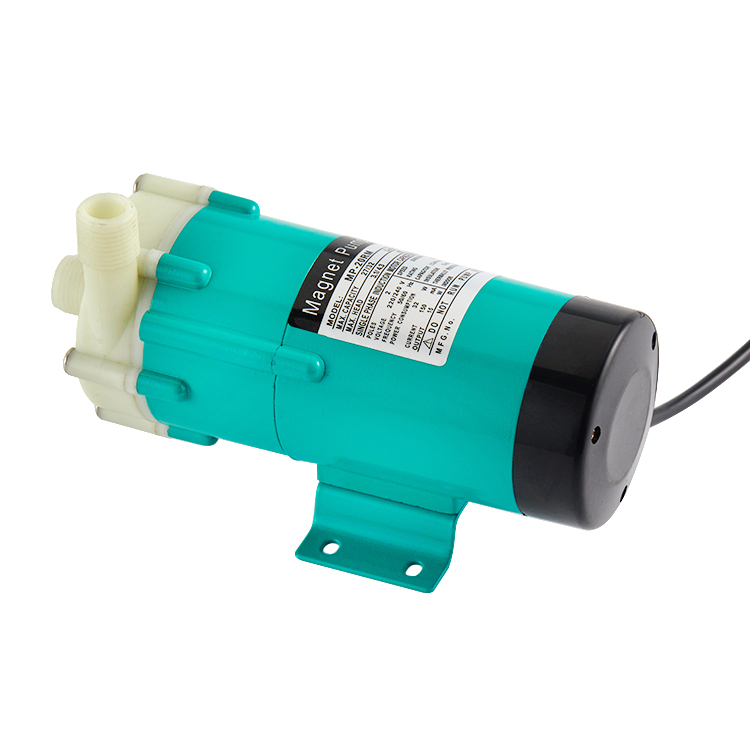
A chemical pump factory represents a specialized manufacturing facility dedicated to producing high-quality pumping solutions for the chemical industry. The chemical pump factory designs and manufactures pumps specifically engineered to handle corrosive, hazardous, and complex fluid applications. These facilities combine advanced engineering expertise with cutting-edge production capabilities to deliver reliable equipment that meets stringent industry standards.
The primary function of a chemical pump factory is to develop pumps capable of transferring aggressive chemicals, solvents, and specialized fluids without degradation or failure. Modern chemical pump factory operations incorporate sophisticated technology, including precision casting methods, advanced material science, and rigorous quality control protocols. These technological features ensure that each pump meets exact performance specifications and maintains structural integrity under demanding conditions.
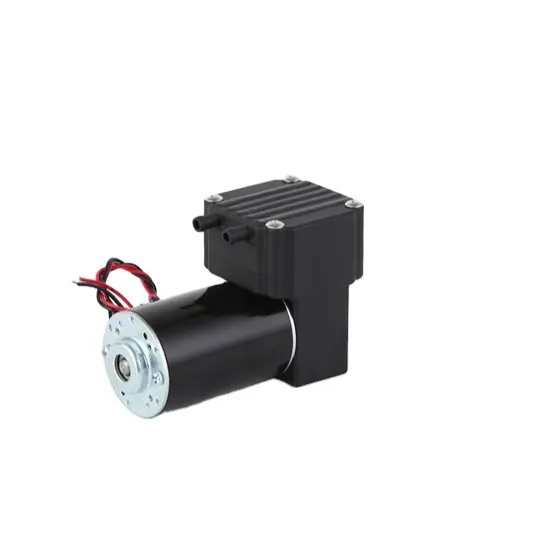
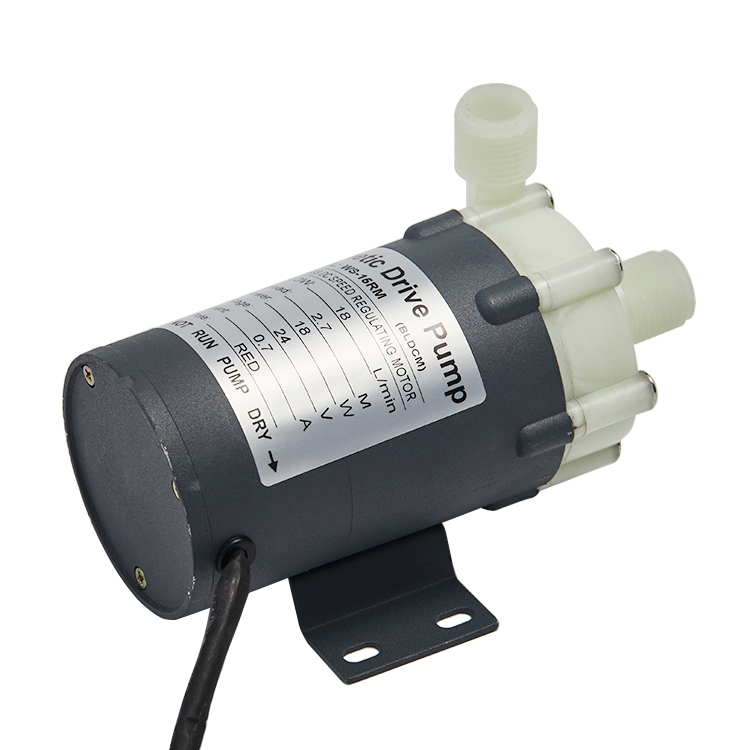
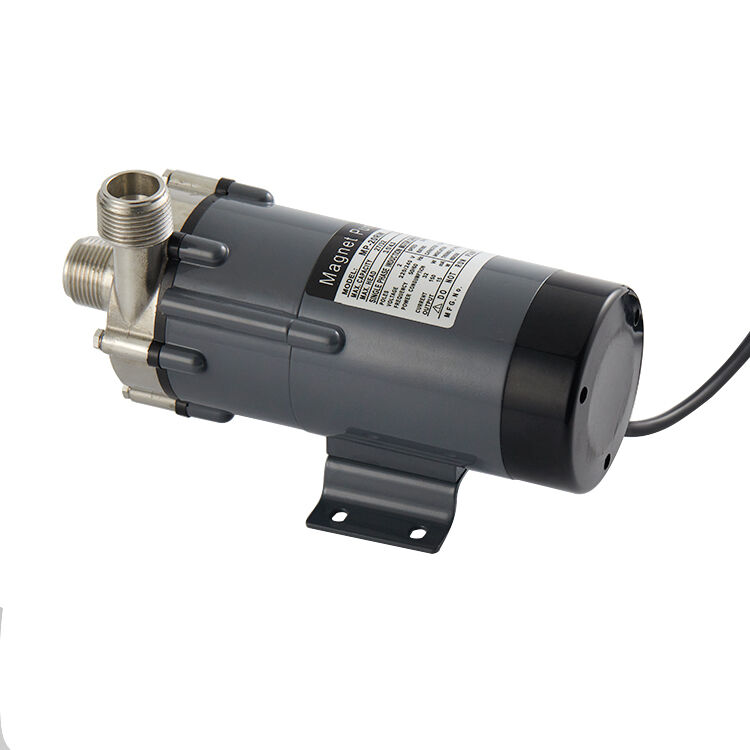
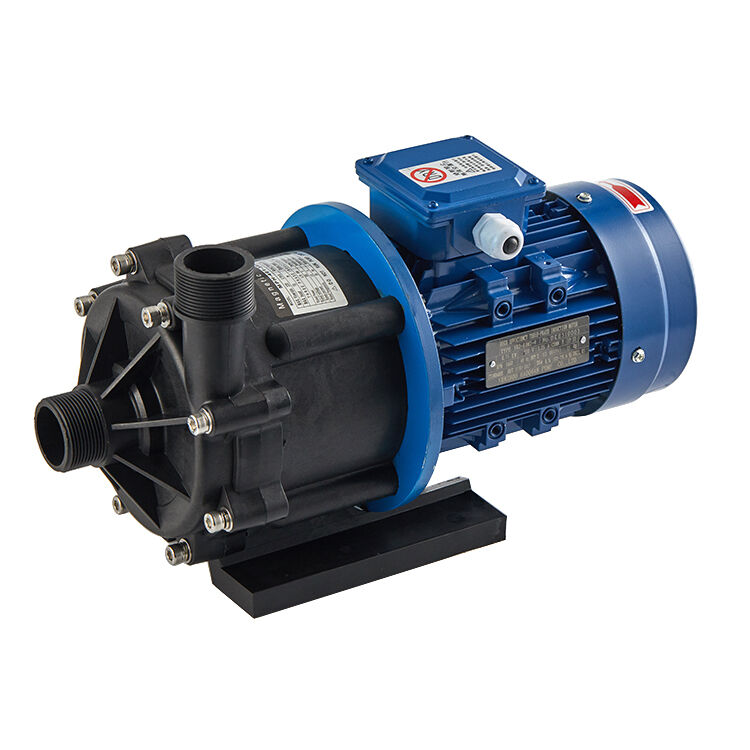
Applications for products from a chemical pump factory extend across numerous industries, including pharmaceutical manufacturing, petrochemical processing, water treatment facilities, and specialty chemical production. The chemical pump factory produces centrifugal pumps, positive displacement pumps, and diaphragm pumps tailored for specific chemical environments. Each type serves distinct operational requirements, from high-volume transfer to precision dosing applications. By specializing in chemical pump manufacturing, these facilities provide industries with dependable equipment that prevents leaks, reduces downtime, and ensures worker safety in hazardous environments.

 EN