Chemical Pump Manufacturer Solutions

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

chemical pump manufacturer

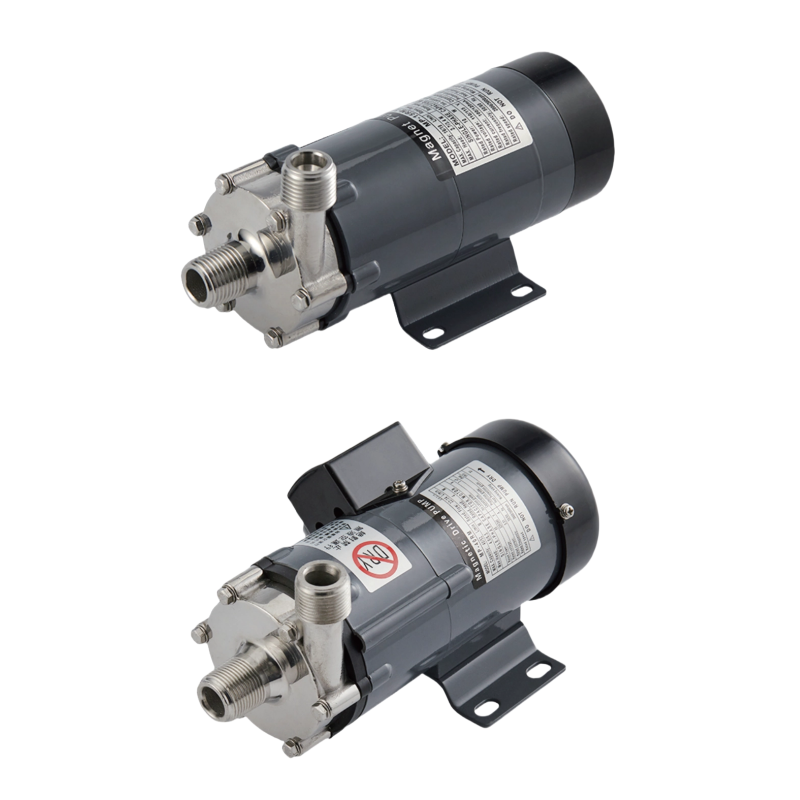
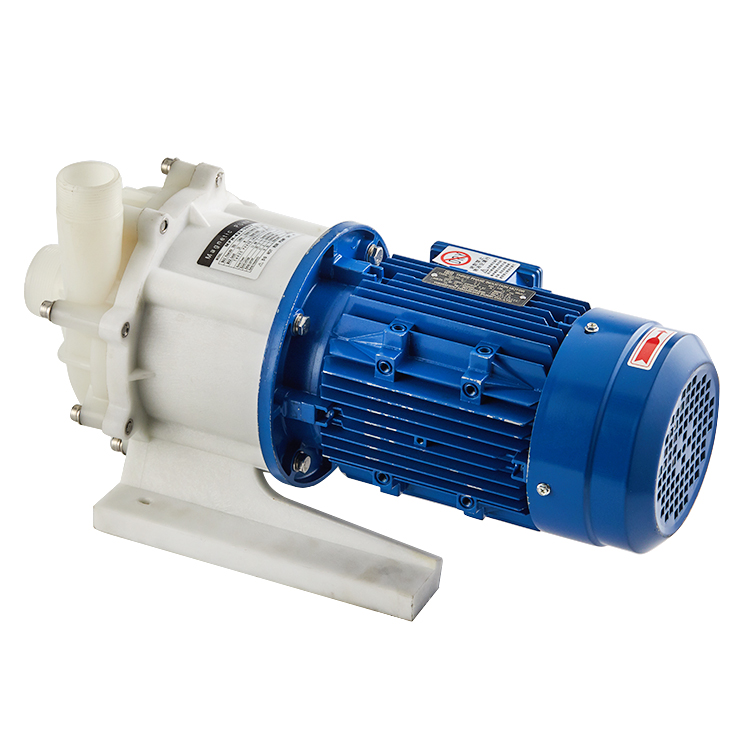
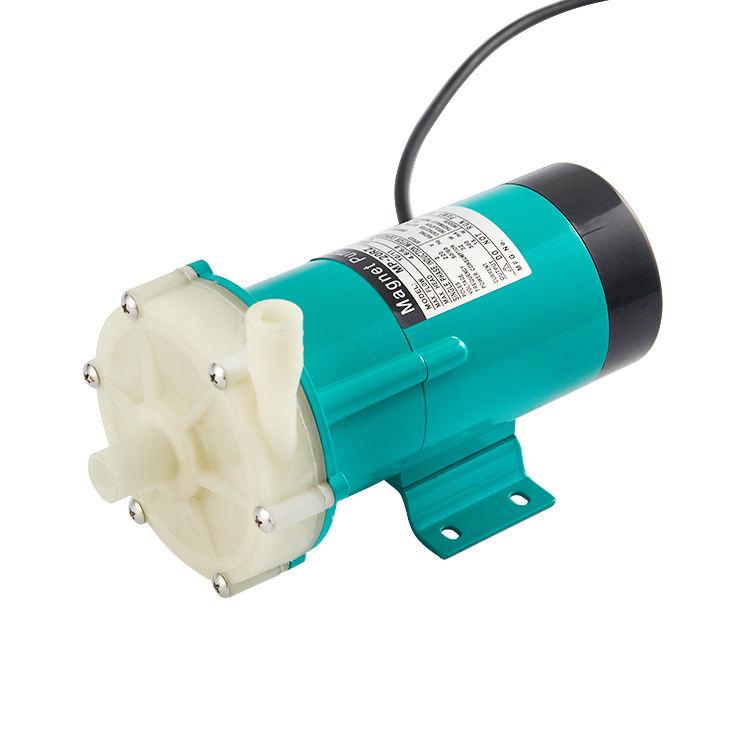
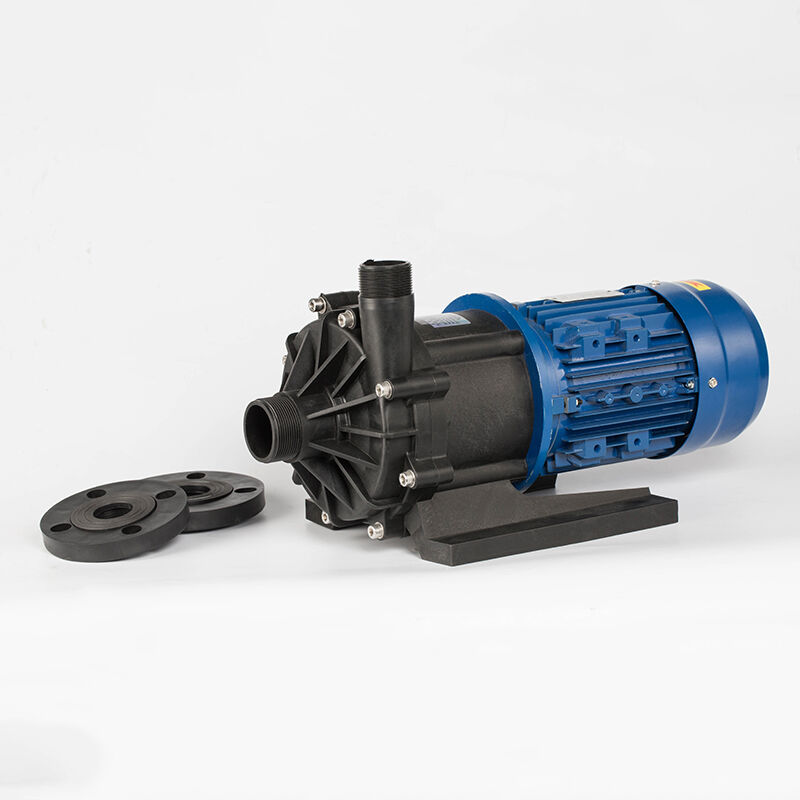
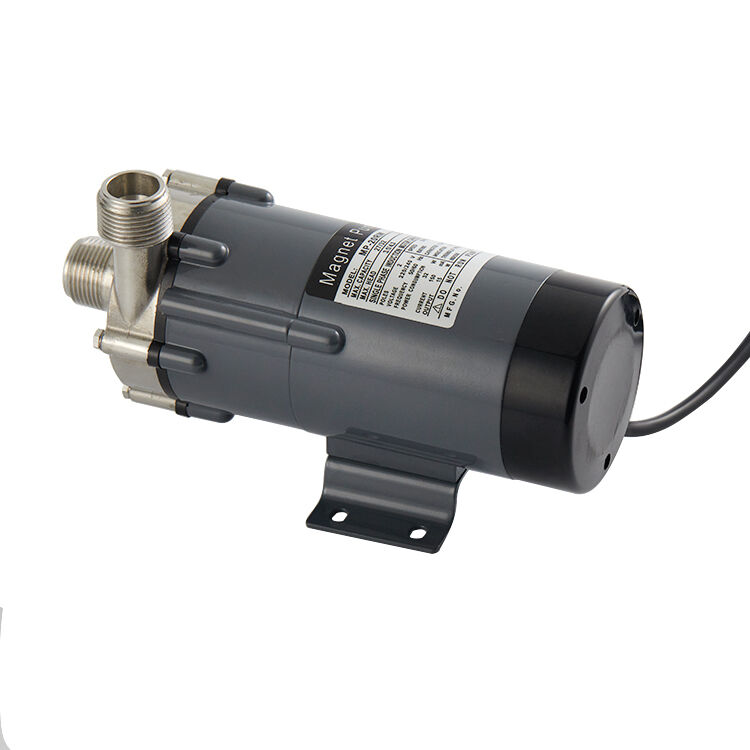
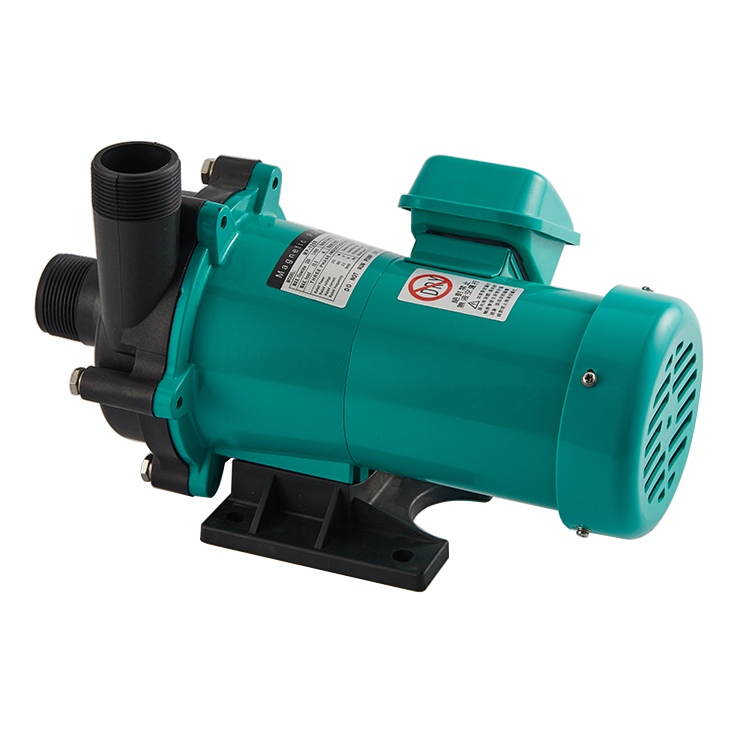
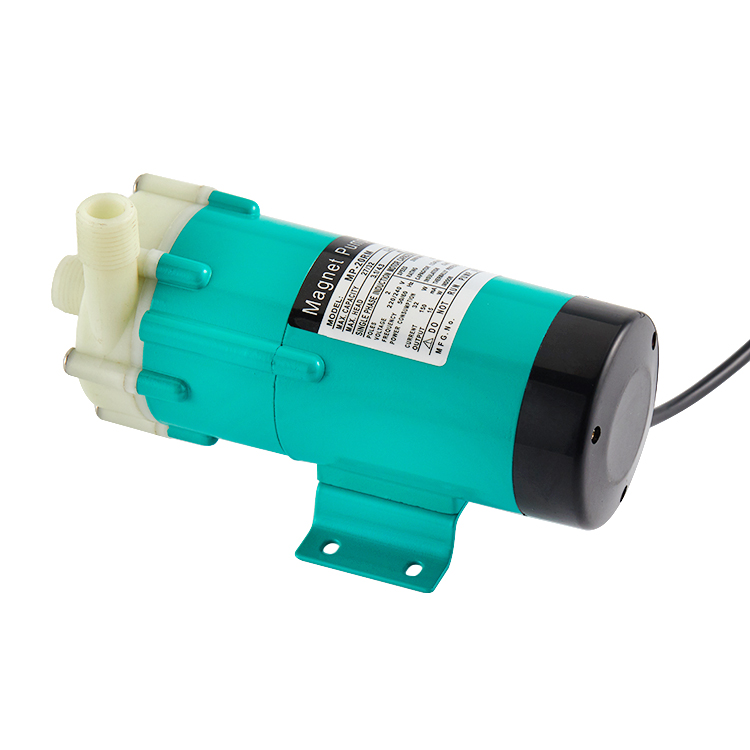
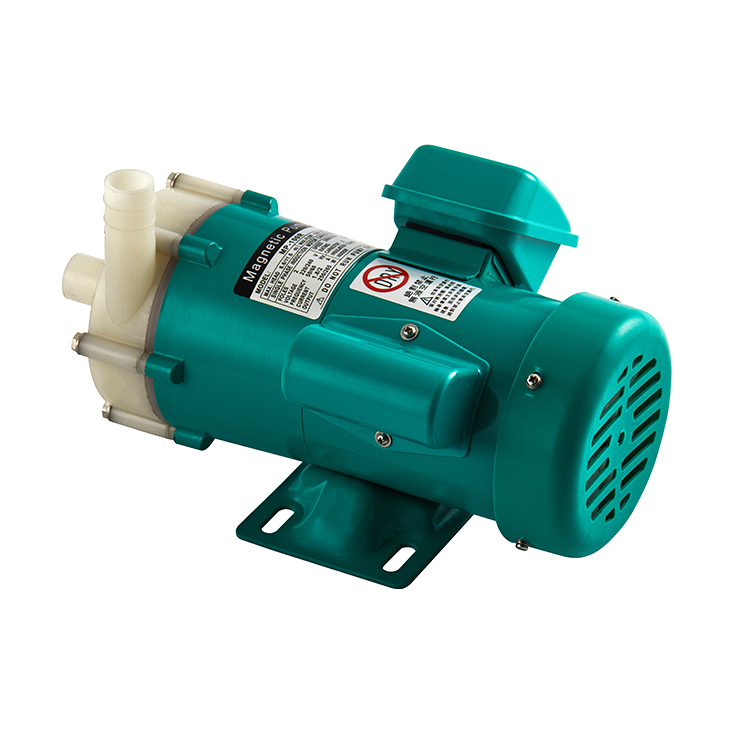
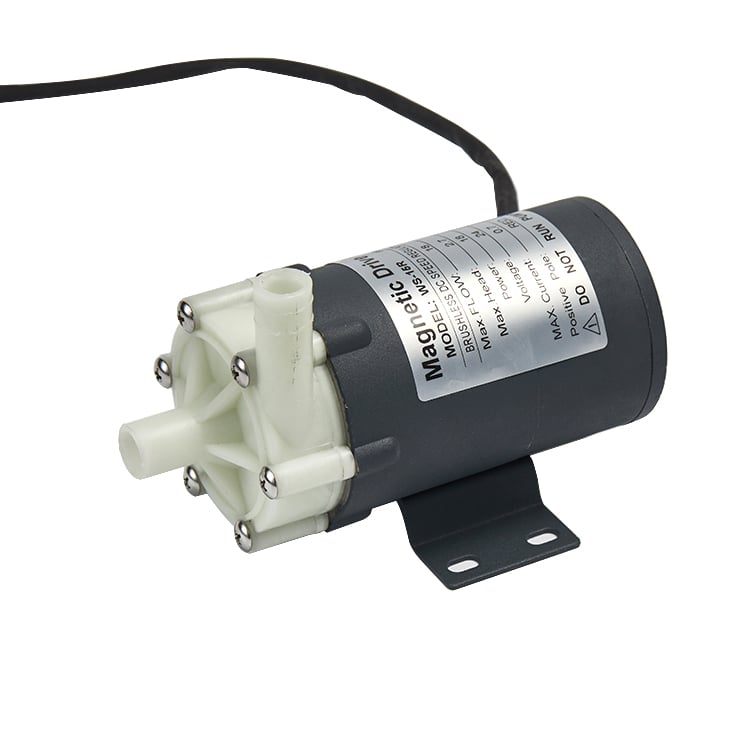
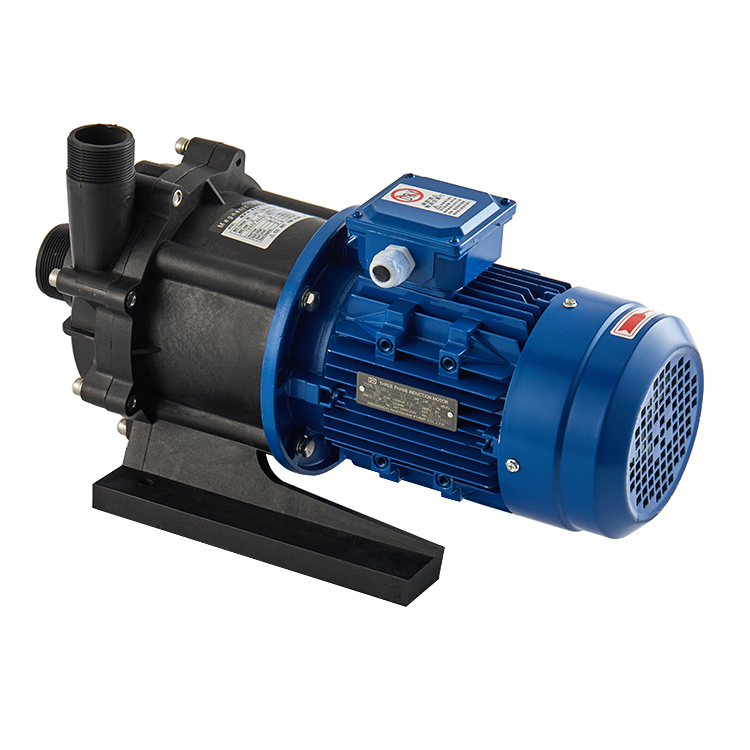
A chemical pump manufacturer specializes in designing and producing advanced pumping solutions for handling corrosive, abrasive, and hazardous chemical substances across various industrial applications. These specialized systems represent the backbone of chemical processing operations, ensuring safe and efficient fluid transfer in demanding environments. The primary function of a chemical pump manufacturer is to develop robust pumping equipment that withstands extreme chemical exposure while maintaining consistent performance. These pumps handle everything from diluted acids and bases to complex industrial solvents, making them indispensable in pharmaceutical, petrochemical, water treatment, and food processing industries. Technologically, modern chemical pump manufacturers integrate advanced materials like specialty alloys, ceramics, and high-performance polymers to create corrosion-resistant solutions. Precision engineering ensures minimal leakage rates and extended equipment lifespan. Many chemical pump manufacturers now incorporate digital monitoring systems and predictive maintenance features that enhance operational efficiency and reduce downtime. Key applications include chemical transfer, metering precise quantities, waste treatment, and circulation processes. A professional chemical pump manufacturer provides customized solutions tailored to specific chemical compatibility requirements and flow rate demands. These pumps operate reliably in harsh conditions where standard equipment would fail, making them critical components in industries handling reactive and hazardous materials worldwide.

Popular Products

Choosing a reliable chemical pump manufacturer offers significant practical benefits that directly impact your operational success and cost efficiency. First, these manufacturers provide superior reliability in hazardous environments where chemical resistance is non-negotiable. Their pumps minimize system downtime and unexpected failures, protecting both equipment investment and worker safety. A dedicated chemical pump manufacturer delivers exceptional durability through specialized material selection and rigorous engineering standards. This means your pumping systems operate longer between maintenance intervals, reducing replacement costs substantially. Their expertise ensures compatibility with your specific chemicals, preventing corrosion damage that compromises performance and safety.

Operational benefits are substantial when selecting an experienced chemical pump manufacturer. These companies offer custom solutions that match your exact flow rates, pressure requirements, and chemical specifications, eliminating compatibility issues. Enhanced energy efficiency in their designs reduces power consumption, lowering utility costs across your facility.

Decision-useful product context matters significantly. A professional chemical pump manufacturer provides comprehensive technical support, including installation guidance and troubleshooting assistance. They offer scalable solutions that grow with your business needs, from small laboratory applications to large industrial operations. Their equipment typically features easier maintenance access and standardized replacement parts, minimizing service expenses. Additionally, working with an established chemical pump manufacturer ensures compliance with industry safety standards and environmental regulations. Their pumps include advanced sealing technologies that prevent hazardous leaks, protecting your workforce and environment. Long-term partnerships with quality manufacturers provide valuable peace of mind and consistent performance you can rely upon.

Practical Tips

How to Optimize the Performance of Urea Pumps in Harsh Operating Conditions

09

Jun

How to Optimize the Performance of Urea Pumps in Harsh Operating Conditions

Introduction: The Vulnerability of SCR Systems in Extreme Environments Selective Catalytic Reduction (SCR) systems are a critical component of modern diesel engines, responsible for transforming harmful nitrogen oxides (NOx) into harmless water and n...
View More
A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

09

Jun

A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

Introduction For international B2B buyers, selecting a pump supplier in China is a critical decision that impacts long-term operational costs and product reliability. While high-quality marketing materials and competitive pricing are common, they do ...
View More
Magnetic Pump vs. Mechanically Sealed Pump: Which One Eliminates Leaks and Reduces Maintenance Costs?

21

Jul

Magnetic Pump vs. Mechanically Sealed Pump: Which One Eliminates Leaks and Reduces Maintenance Costs?

Seal failure remains one of the most common reasons an industrial pump ends up offline unexpectedly. For plant engineers handling hazardous, corrosive, or high-value fluids, the choice between a magnetic drive pump and a mechanically sealed pump dire...
View More
Magnetic Pump Buying Guide: Neodymium vs. Samarium-Cobalt Magnets, Dry Run Protection, and Flow Rate Explained

21

Jul

Magnetic Pump Buying Guide: Neodymium vs. Samarium-Cobalt Magnets, Dry Run Protection, and Flow Rate Explained

Magnet selection rarely gets the attention it deserves during a magnetic pump purchase, yet it directly affects how the pump performs under heat, chemical exposure, and demagnetization risk over its service life. Combined with dry run protecti...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

chemical pump manufacturer

Advanced Corrosion-Resistant Materials

Advanced Corrosion-Resistant Materials

The most successful chemical pump manufacturer uses cutting-edge material science to create pumps that resist virtually any corrosive chemical. These specialists employ specialty alloys, reinforced polymers, and ceramic components engineered specifically for hostile chemical environments. This material innovation prevents degradation and maintains structural integrity even when handling aggressive acids, bases, and organic solvents. A leading chemical pump manufacturer invests heavily in research and development to stay ahead of material technology. Their pumps feature multi-layer construction that provides secondary protection if the primary surface encounters unexpected chemical exposure. This redundant protection system significantly extends equipment lifespan and reduces catastrophic failures. The importance of advanced materials cannot be overstated in chemical processing. When a chemical pump manufacturer selects inappropriate materials, pump failure becomes inevitable and costly. Superior materials mean your operations continue uninterrupted, employee safety remains protected, and your facility maintains full productivity. This commitment to material excellence distinguishes top-tier manufacturers from competitors.
Precision Engineering and Custom Solutions

Precision Engineering and Custom Solutions

Every leading chemical pump manufacturer recognizes that one-size-fits-all approaches fail in chemical processing environments. These manufacturers employ precision engineering to develop custom solutions matching your exact specifications, chemical compatibility requirements, and performance demands. Advanced CAD design and computational modeling ensure optimal pump efficiency for your specific applications. Customization extends beyond basic specifications when working with a professional chemical pump manufacturer. They analyze your complete system requirements, including temperature fluctuations, viscosity variations, and pressure dynamics, creating tailored solutions that maximize performance. This engineering precision reduces energy consumption, improves flow accuracy, and enhances system reliability throughout your operations. The value of precision engineering manifests in superior pump performance and predictable operating characteristics. A conscientious chemical pump manufacturer conducts extensive testing before delivery, verifying that each system meets promised specifications under real-world conditions. This meticulous approach prevents costly installation problems and ensures seamless integration with existing infrastructure, delivering immediate operational benefits.
Comprehensive Technical Support and Compliance

Comprehensive Technical Support and Compliance

Outstanding chemical pump manufacturers provide far more than physical equipment; they deliver comprehensive technical expertise and ongoing support. These specialists ensure your pumps comply with industry safety standards, environmental regulations, and equipment certifications required in your jurisdiction. Their support teams guide installation, troubleshoot operational issues, and provide maintenance recommendations that extend equipment life. A responsible chemical pump manufacturer maintains readily available replacement parts and keeps technicians trained on their complete product line. This commitment to customer success means minimal downtime when maintenance becomes necessary. Their documentation is clear and accessible, empowering your maintenance team to handle routine servicing independently. Compliance support distinguishes premium manufacturers from budget alternatives. A professional chemical pump manufacturer documents all certifications, maintains traceability records, and provides the technical documentation required for regulatory audits. This comprehensive support package protects your facility from legal liability and ensures consistent adherence to environmental and safety protocols, providing invaluable business continuity and risk mitigation benefits.
Chemical Pump Manufacturer Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000