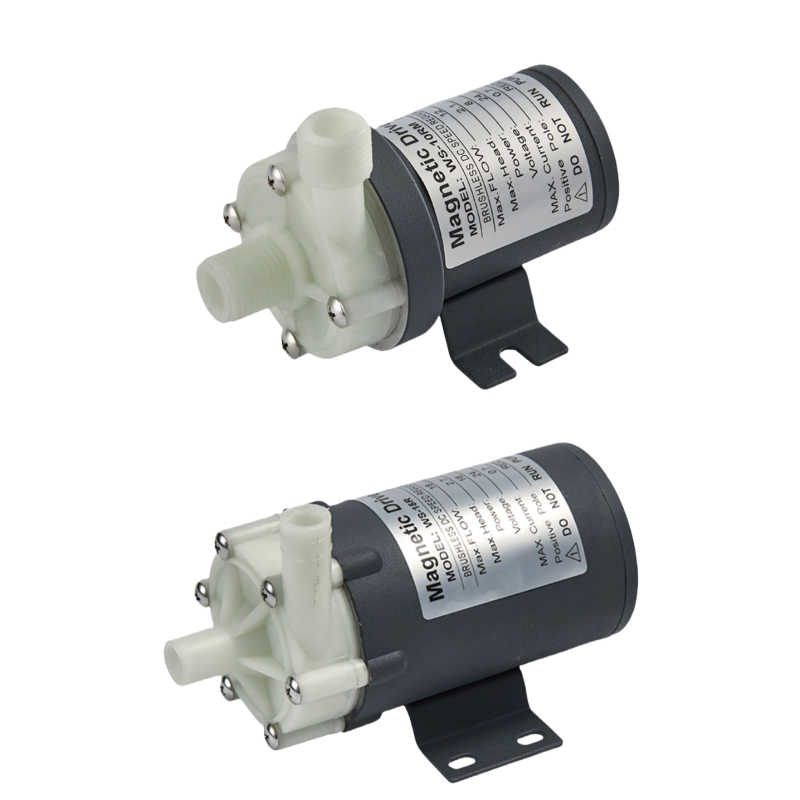
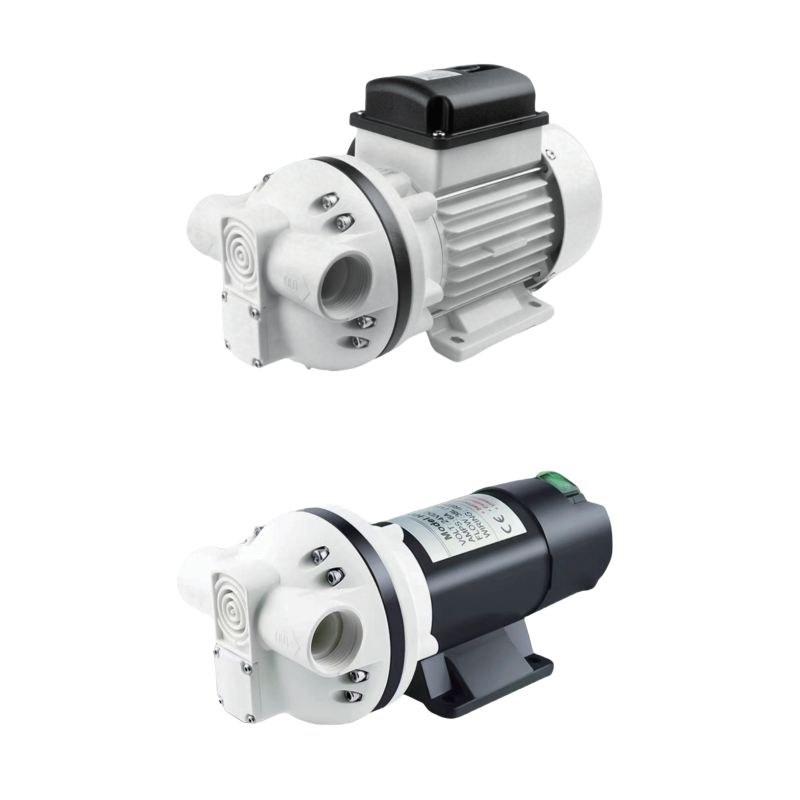
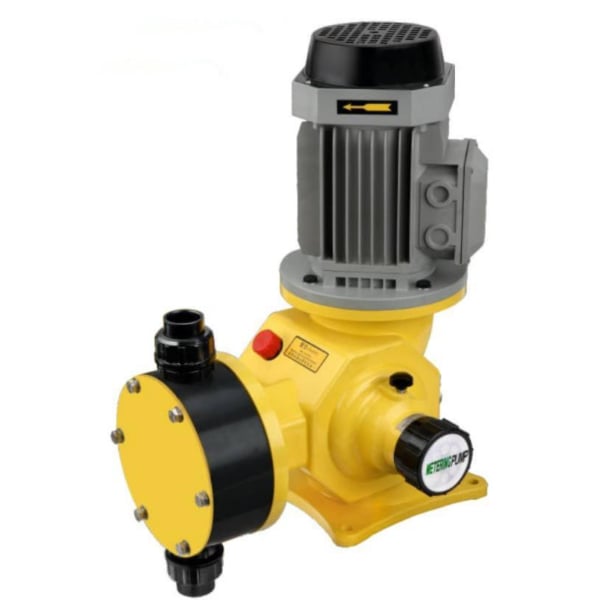
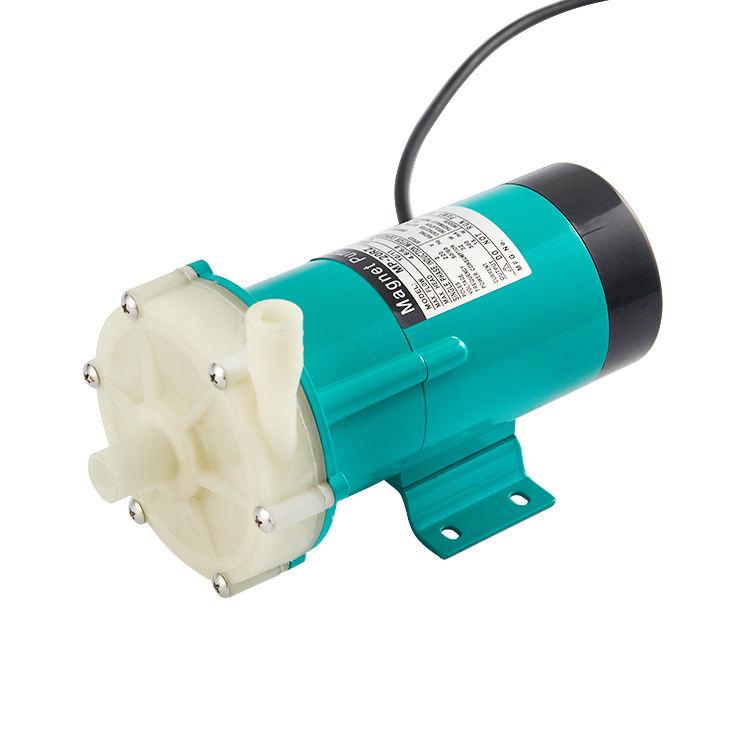
Chemical Pump for Corrosive Liquids

All Categories
Get a Quote

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

chemical pump for corrosive liquids

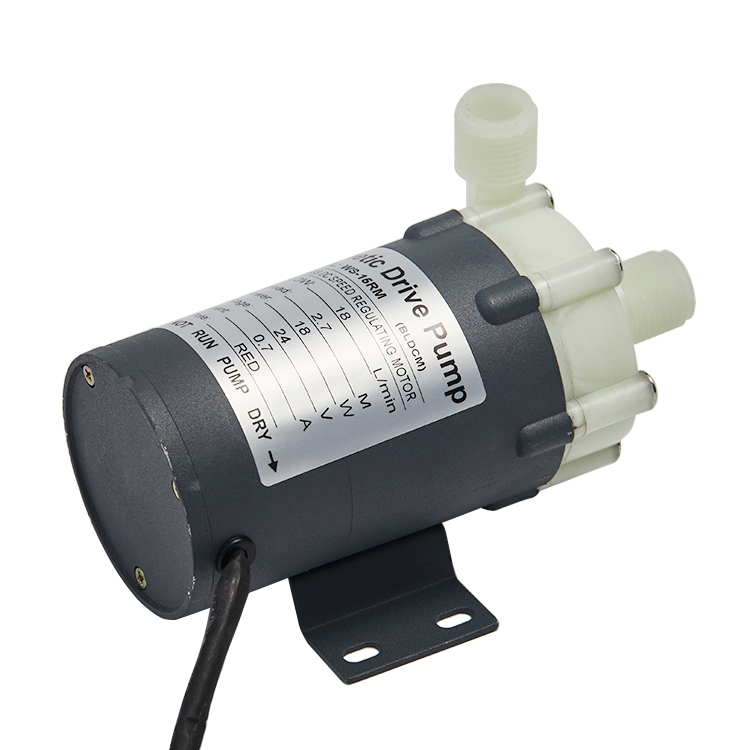
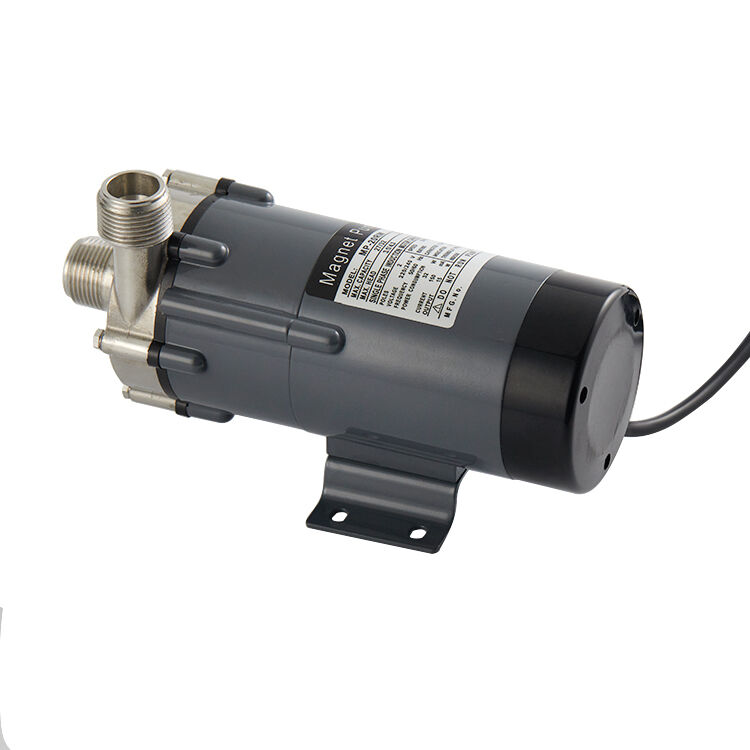
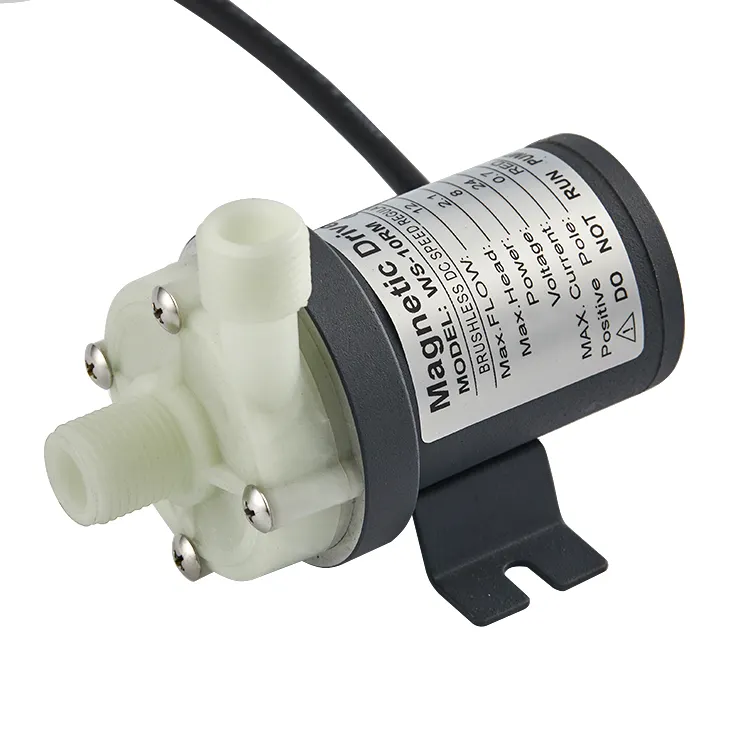
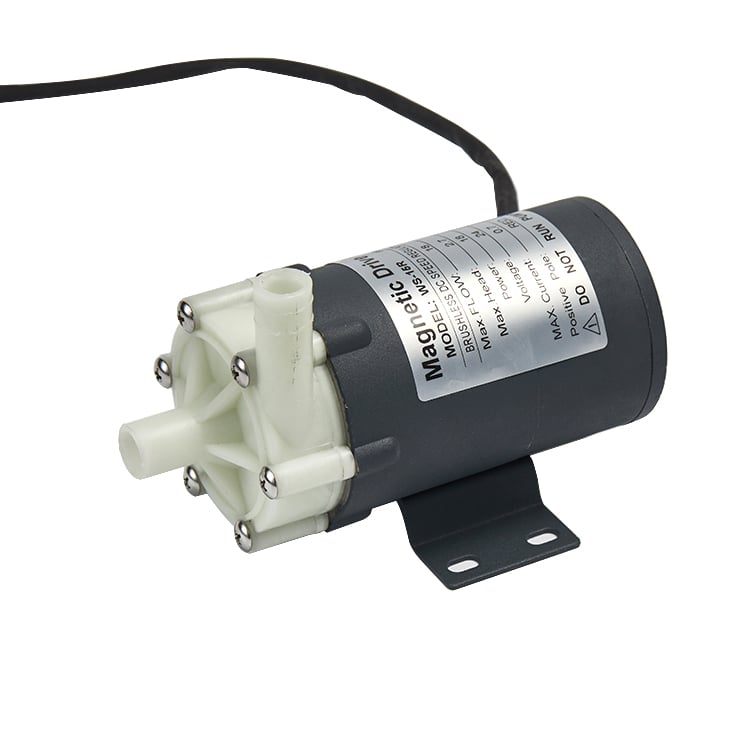
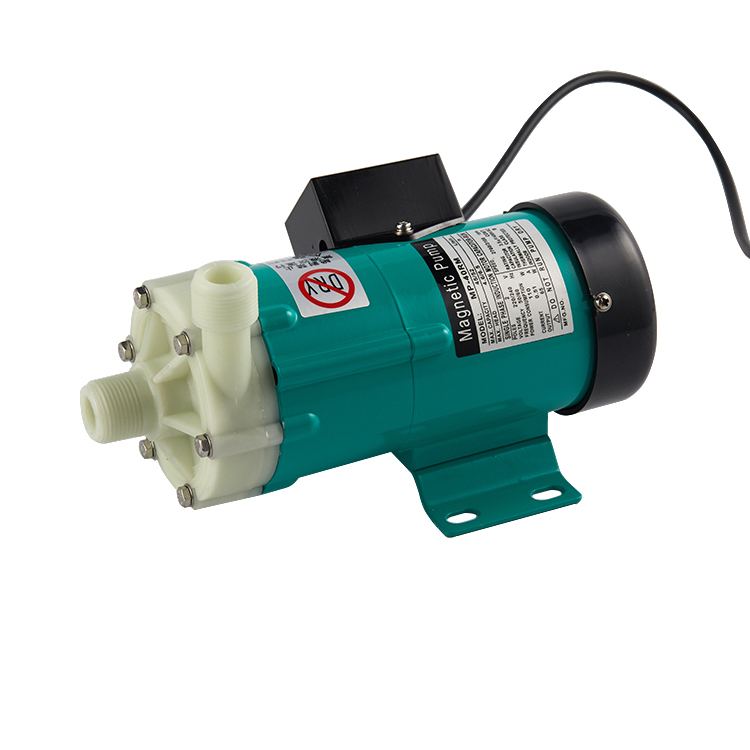
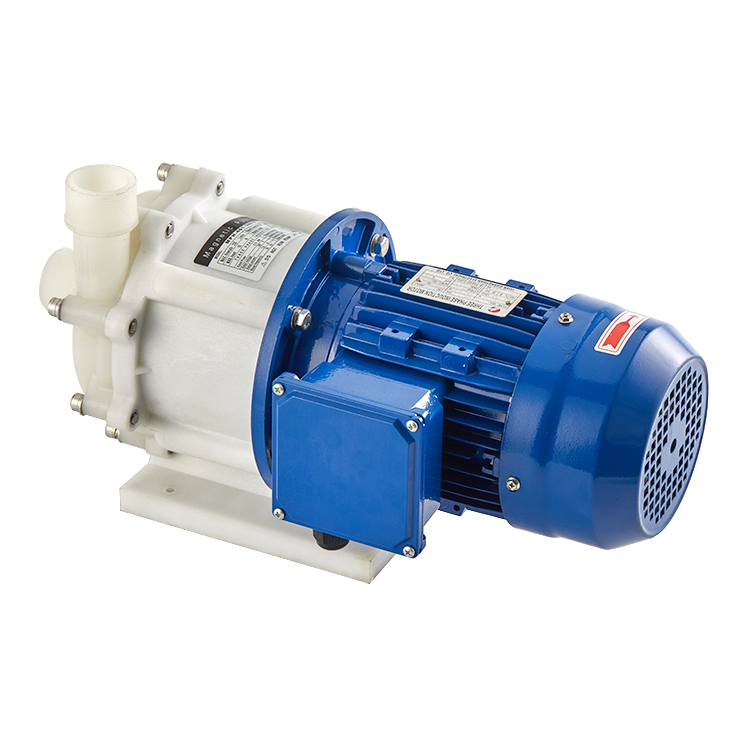
A chemical pump for corrosive liquids is a specialized pumping device engineered to handle aggressive, harsh substances that would damage standard equipment. This chemical pump for corrosive liquids transfers acids, alkalis, solvents, and other corrosive materials safely through industrial processes. The primary function of a chemical pump for corrosive liquids involves moving these dangerous fluids from storage containers to processing units while preventing leaks, contamination, and equipment degradation. Technologically, a chemical pump for corrosive liquids features specially selected materials such as polypropylene, fluoroplastics, and stainless steel alloys that resist chemical attack. These construction materials ensure the pump maintains structural integrity even when exposed to highly corrosive environments. Advanced sealing systems prevent hazardous fluid escape, while specialized impeller designs optimize flow rates without compromising durability. Applications of the chemical pump for corrosive liquids span multiple industries. Manufacturing facilities use these pumps in chemical production, pharmaceutical companies employ them in drug synthesis, water treatment plants utilize them for acid injection, and metal processing operations depend on them for pickling solutions. Food and beverage producers also rely on chemical pump for corrosive liquids technology for sanitization processes. The engineering behind a chemical pump for corrosive liquids ensures reliable performance in extreme conditions where conventional pumps would fail immediately. Proper selection of a chemical pump for corrosive liquids based on specific fluid properties guarantees operational safety and extended equipment lifespan.

New Product Recommendations

Investing in a chemical pump for corrosive liquids delivers substantial operational and financial benefits that directly impact your bottom line. The primary advantage lies in equipment longevity; because this specialized pump resists corrosive degradation, you avoid frequent replacements that plague standard pumps. Your maintenance costs drop significantly since a chemical pump for corrosive liquids requires less service intervention and fewer emergency repairs.

Safety improvements represent another critical buyer value when selecting a chemical pump for corrosive liquids. These pumps eliminate dangerous fluid leaks that endanger workers and contaminate facilities. The secure sealing mechanisms and robust construction mean your staff works in a safer environment while handling hazardous materials. Compliance with environmental regulations becomes straightforward since a chemical pump for corrosive liquids prevents accidental chemical releases.

Operational efficiency improves when you deploy a chemical pump for corrosive liquids in your processes. These pumps maintain consistent flow rates and pressure stability, resulting in better product quality and increased production reliability. Your processes run smoothly without unexpected downtime caused by pump failure. The chemical pump for corrosive liquids performs reliably across varying temperature ranges and diverse chemical compositions. Application suitability is another compelling reason to choose a chemical pump for corrosive liquids. Whether handling concentrated sulfuric acid, sodium hydroxide solutions, or aggressive cleaning chemicals, this equipment adapts to your specific needs. The versatility of a chemical pump for corrosive liquids makes it the intelligent choice across pharmaceutical manufacturing, industrial chemical production, and water treatment operations. Your investment in a chemical pump for corrosive liquids pays dividends through improved safety, reduced maintenance expenses, and enhanced operational performance that directly supports your business growth and profitability objectives.

Tips And Tricks

2026 BLDC Pump Guide: Top Models and Features

09

Jun

2026 BLDC Pump Guide: Top Models and Features

The bldc pump has emerged as one of the most technically advanced fluid-handling solutions available to engineers and procurement professionals entering 2026. Driven by brushless direct current motor technology, these pumps deliver a compelling combi...
View More
A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

09

Jun

A Buyer’s Guide to China Factory Audits for Industrial Pump Suppliers

Introduction For international B2B buyers, selecting a pump supplier in China is a critical decision that impacts long-term operational costs and product reliability. While high-quality marketing materials and competitive pricing are common, they do ...
View More
The Value of R&D Innovation in Reducing Total Cost of Ownership (TCO) for Pumps

09

Jun

The Value of R&D Innovation in Reducing Total Cost of Ownership (TCO) for Pumps

Introduction In the B2B procurement process, the initial purchase price of an industrial pump is often just the tip of the iceberg. Smart facility managers and procurement directors know that the true cost of a pump is revealed over its entire lifesp...
View More
How to Choose the Right Magnetic Pump for Corrosive Chemicals, High-Purity Fluids, and Explosive Environments

21

Jul

How to Choose the Right Magnetic Pump for Corrosive Chemicals, High-Purity Fluids, and Explosive Environments

Magnetic drive pumps are often selected for one reason: eliminating the shaft seal removes the most common leak path in an industrial pump. But not every magnetic pump is built the same way, and selecting the wrong configuration for corrosive, high-p...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

chemical pump for corrosive liquids

Superior Corrosion Resistance

Superior Corrosion Resistance

A chemical pump for corrosive liquids incorporates advanced material science that delivers exceptional corrosion resistance unmatched by conventional equipment. The construction utilizes engineered polymers and specialized alloys specifically selected to withstand aggressive chemical environments. When you choose a chemical pump for corrosive liquids with proper material specifications, you invest in equipment that maintains structural integrity for years, not months. The pump's internals remain protected from chemical degradation that typically destroys standard metallic components. This superior corrosion resistance means a chemical pump for corrosive liquids retains its performance capabilities even during extended exposure to harsh substances. Your operational reliability increases substantially because equipment failure due to material breakdown becomes virtually eliminated. The long-term cost savings from a chemical pump for corrosive liquids far exceed the initial investment, making it economically superior to replacing corroded standard pumps repeatedly.
Advanced Sealing Technology

Advanced Sealing Technology

The sealing systems integrated into a chemical pump for corrosive liquids represent cutting-edge engineering designed to prevent hazardous fluid leakage. Multiple seal stages within a chemical pump for corrosive liquids create redundant protection against escape of dangerous substances. This advanced design ensures compliance with strict environmental and occupational safety regulations while protecting your workforce. The sealing technology employed in a chemical pump for corrosive liquids prevents cross-contamination between different process stages, maintaining product purity and process integrity. Workers experience enhanced safety when operating equipment with a chemical pump for corrosive liquids because leak prevention eliminates dangerous exposure scenarios. Facility cleanliness improves dramatically since a chemical pump for corrosive liquids contains all corrosive materials within designated pathways. The sophisticated sealing mechanisms mean your chemical pump for corrosive liquids delivers reliable, leak-free operation across thousands of operational hours.
Versatile Material Handling Capacity

Versatile Material Handling Capacity

A chemical pump for corrosive liquids handles an impressive range of aggressive substances, making it the universal solution for diverse industrial applications. From concentrated mineral acids to potent alkaline solutions, a chemical pump for corrosive liquids processes virtually any corrosive liquid your operation requires. This versatility means a single chemical pump for corrosive liquids investment serves multiple process requirements rather than maintaining separate specialized equipment. The adaptable design of a chemical pump for corrosive liquids supports varying viscosity levels and temperature conditions without performance degradation. Industries from pharmaceutical manufacturing to metal processing rely on a chemical pump for corrosive liquids because it delivers consistent performance regardless of specific chemical composition. Your operational flexibility increases when you specify a chemical pump for corrosive liquids since process modifications require minimal equipment adjustments. The material handling versatility offered by a chemical pump for corrosive liquids represents practical value that translates directly into reduced capital expenditure and simplified maintenance protocols across your facility.
Chemical Pump for Corrosive Liquids

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000